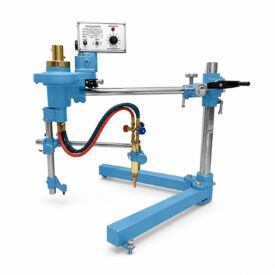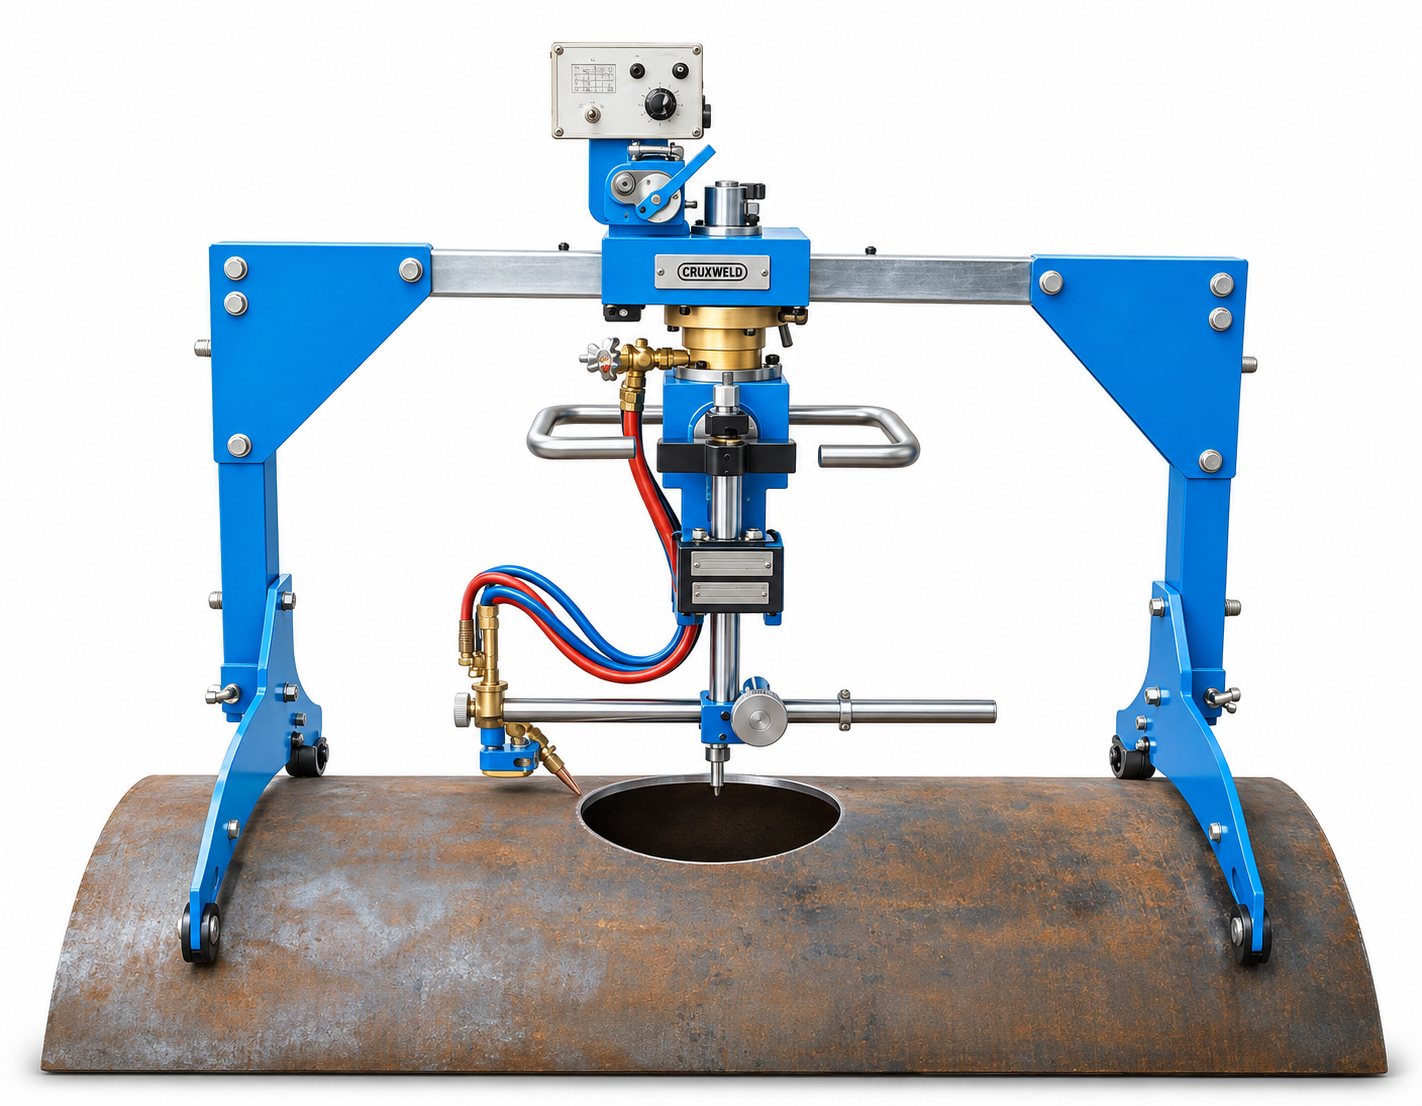
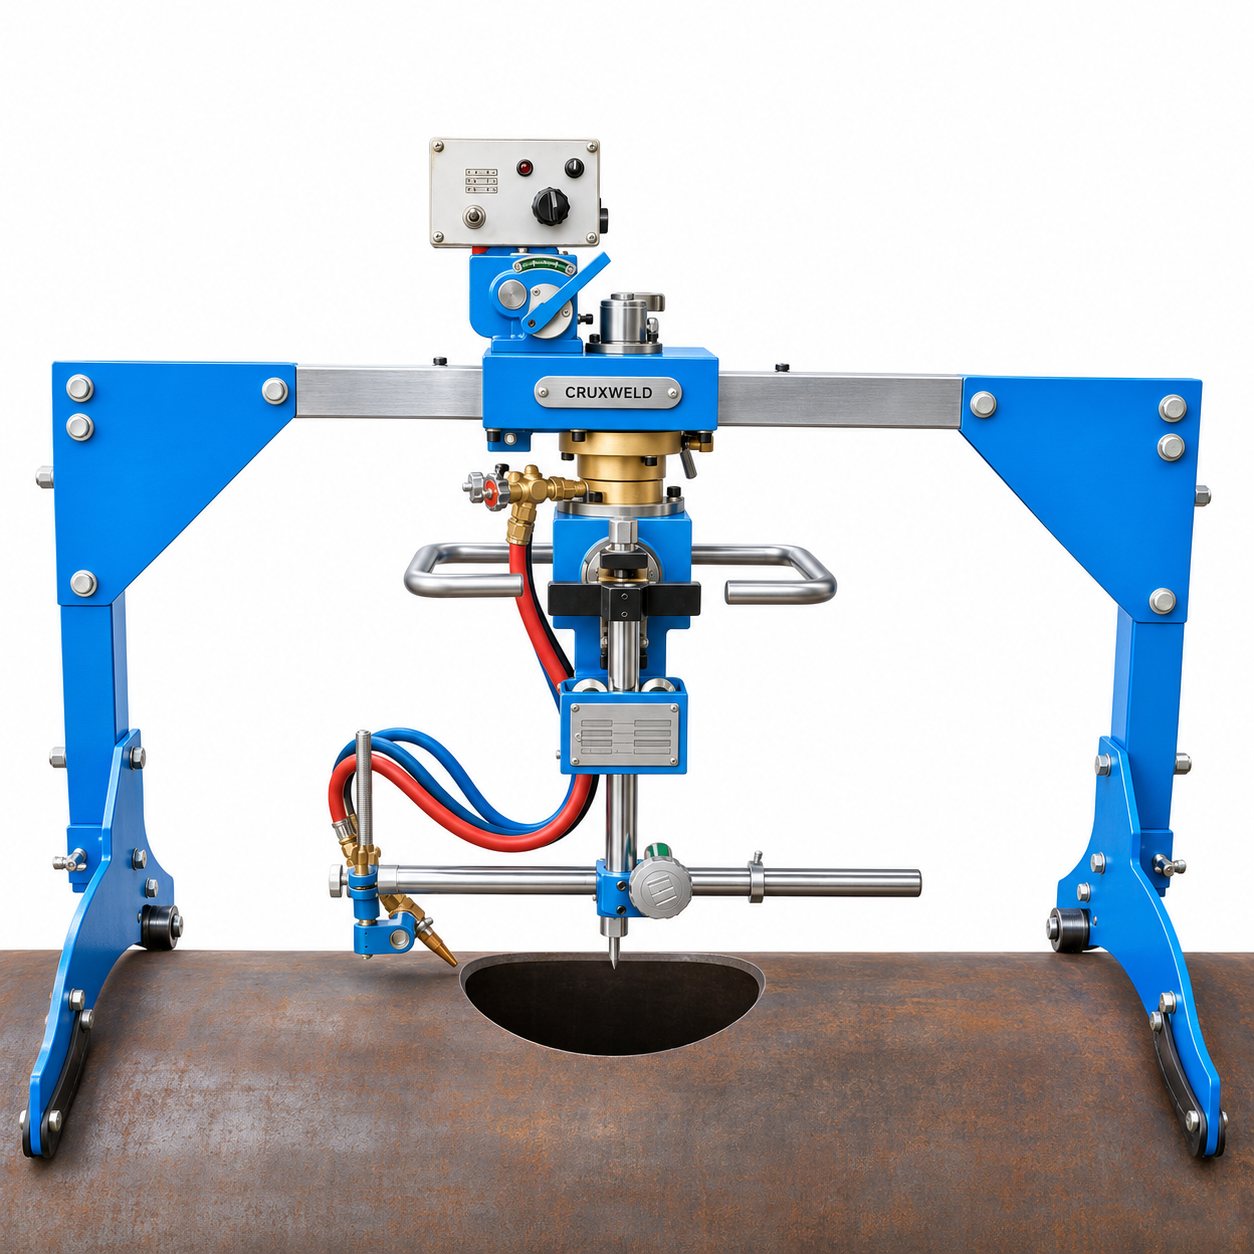
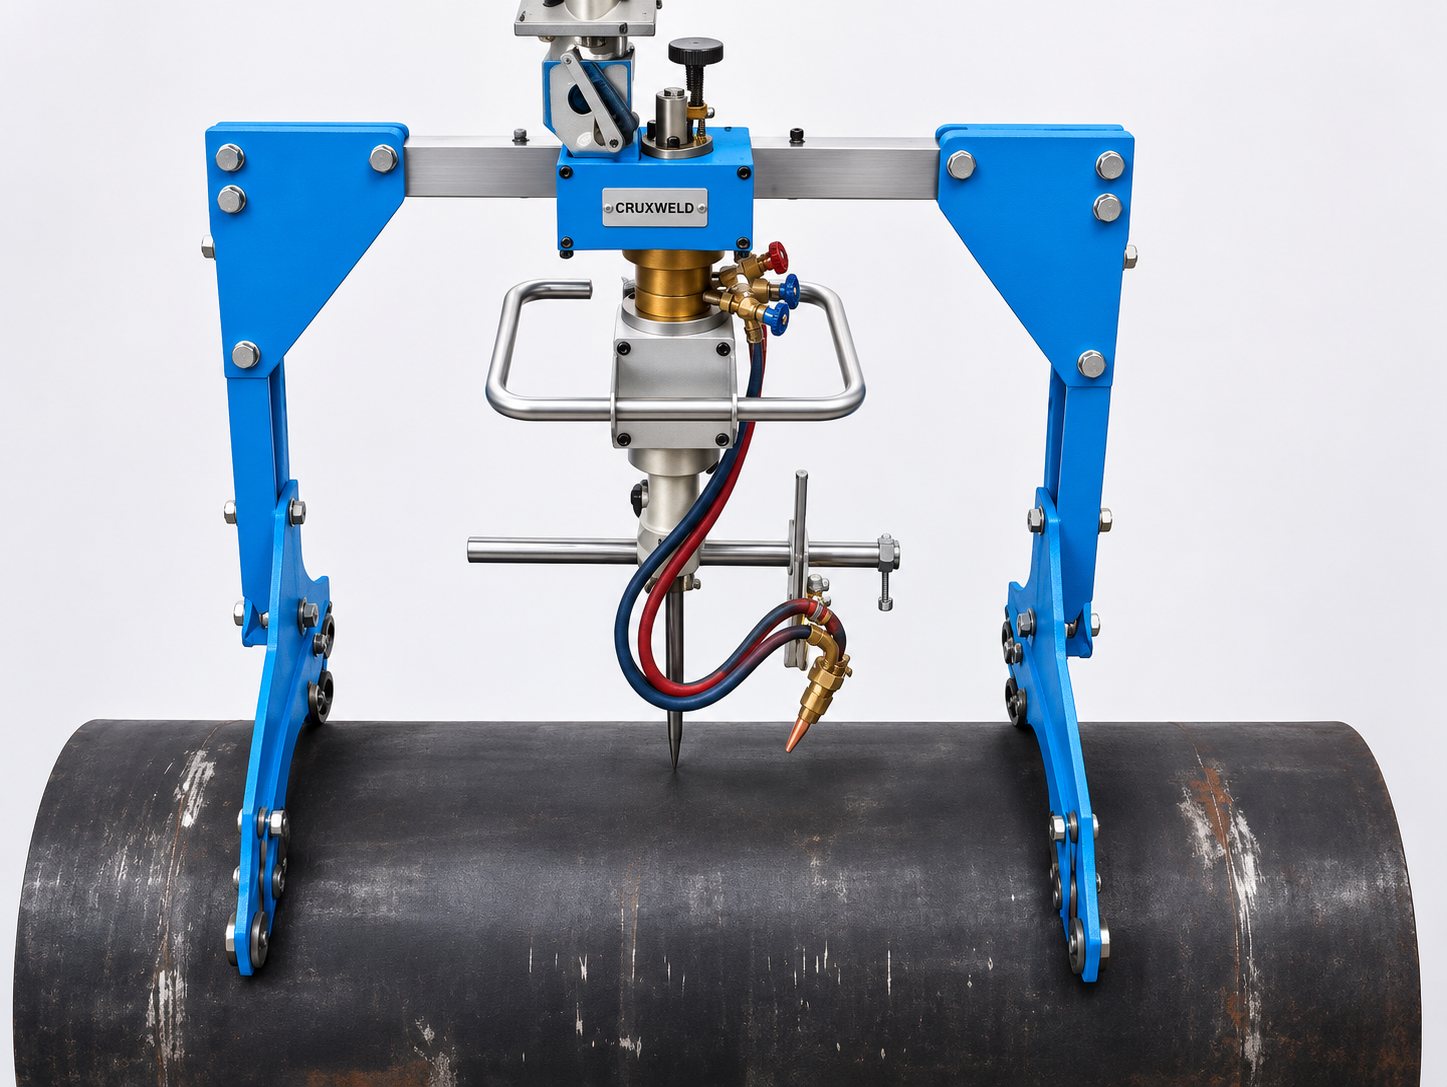
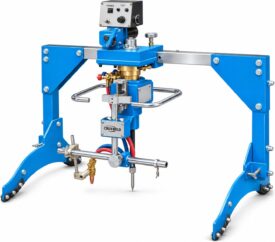
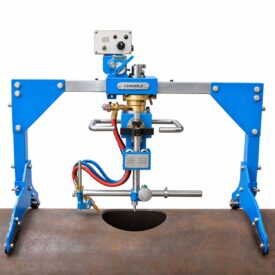
The CRUXWELD ORBICUT 600 is a portable automatic pipe hole cutting machine for branch openings in steel pipe and vessels. It sits on the pipe, an electric drive carries the oxy-fuel torch round a centre cone, and a mechanical saddle-following system lifts and lowers the torch so the flame follows the curve. Holes from Ø80 to Ø600 mm, in 5 to 50 mm steel, square or bevelled up to 45°.
Price, delivery & technical help — get a fast response.
A hole for a branch pipe looks round from above, but on a curved pipe wall its edge rises and falls like a saddle. Cut by hand, that takes marking out and a steady torch. The ORBICUT 600 does both movements at once: the drive turns the torch in a true circle while the saddle mechanism moves it up and down to keep the tip at the right distance from the steel.


See the torch travel round the centre cone and follow the pipe wall as the opening is cut.
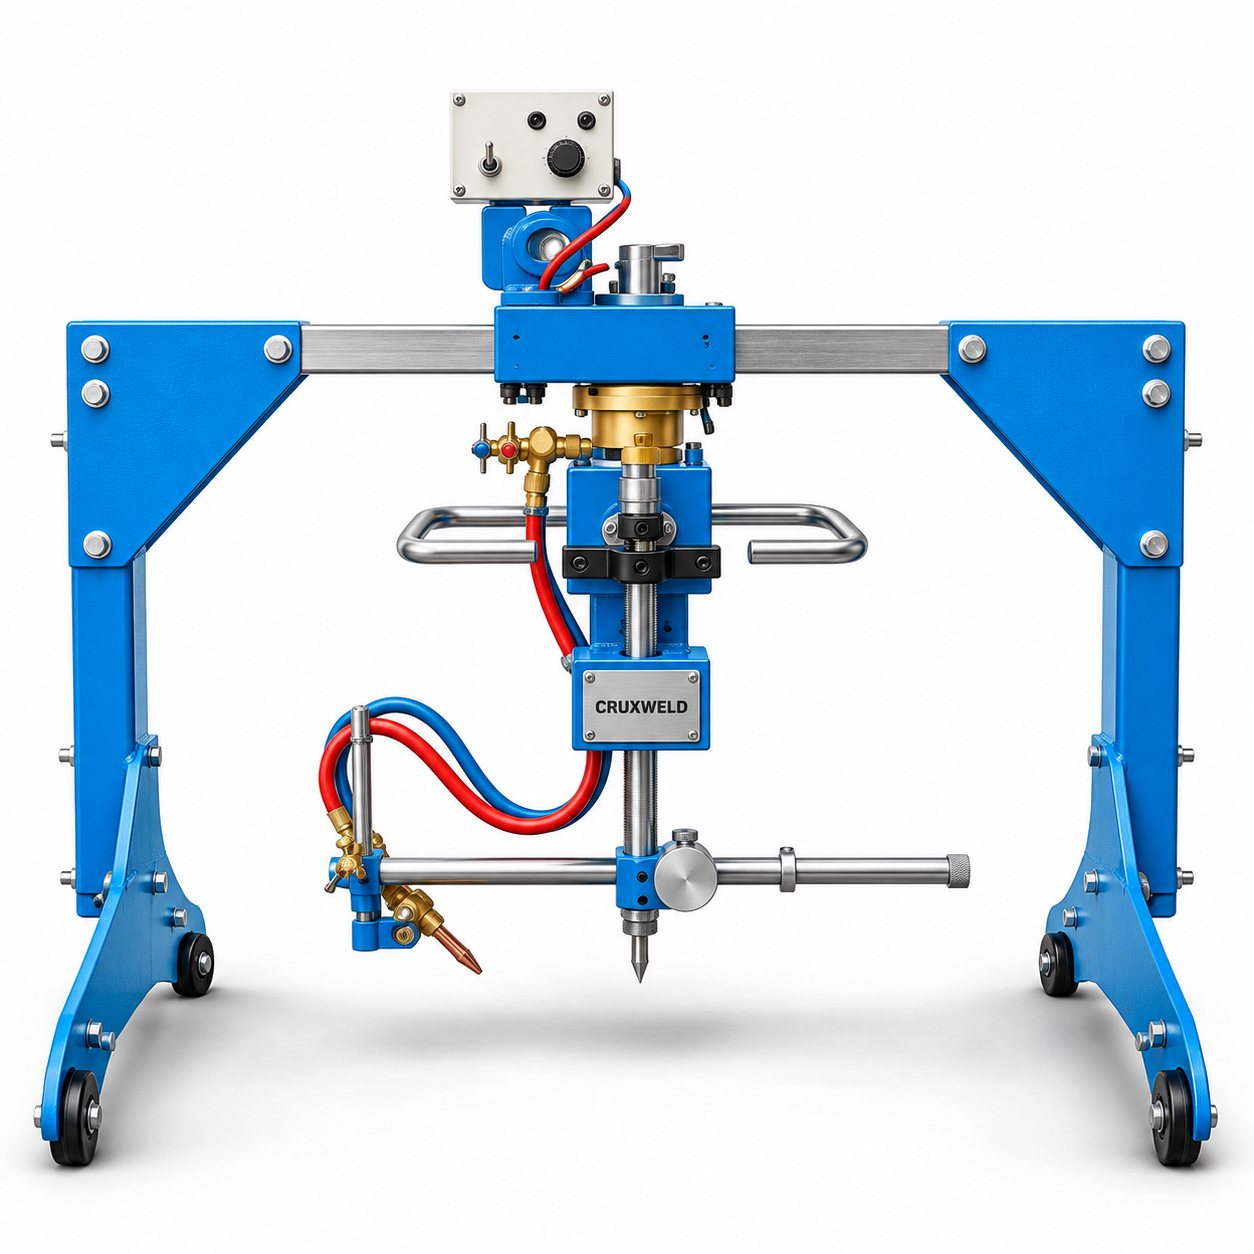
Eight assemblies, shown on the machine in the order they go on. Each one is highlighted on the photo with a close-up beside it.
Light aluminium-alloy frame. The two symmetrical legs sit on the pipe on rubber-covered feet and centre the machine over it. Standard legs suit pipe of Ø800 mm and above.
The electric drive turns the torch at 0.12 to 1.2 rpm. Release the clutch and the torch swings freely by hand to the start point.
Mounted on top where the operator can reach it: speed knob and normal/reverse switch, with SCR speed control. Supply AC 220 V.
Oxygen and fuel gas pass through a rotating joint, so the hoses do not twist however many turns the torch makes.
Raises and lowers the torch as it travels round, so the flame follows the curve of the pipe. Saddle height is set from 0 to 96 mm.
The handwheel moves the torch along the bar to set the cutting radius, for holes from Ø80 to Ø600 mm.
Points at the centre of the opening. The torch travels in a circle around it.
Oxy-fuel torch that tilts 0 to 45° for bevels. G02 tips for acetylene or G03 for propane; cuts 5 to 50 mm steel.
46.5 kg machine body. Set the saddle height and radius, connect oxygen and fuel gas, and cut the branch opening.
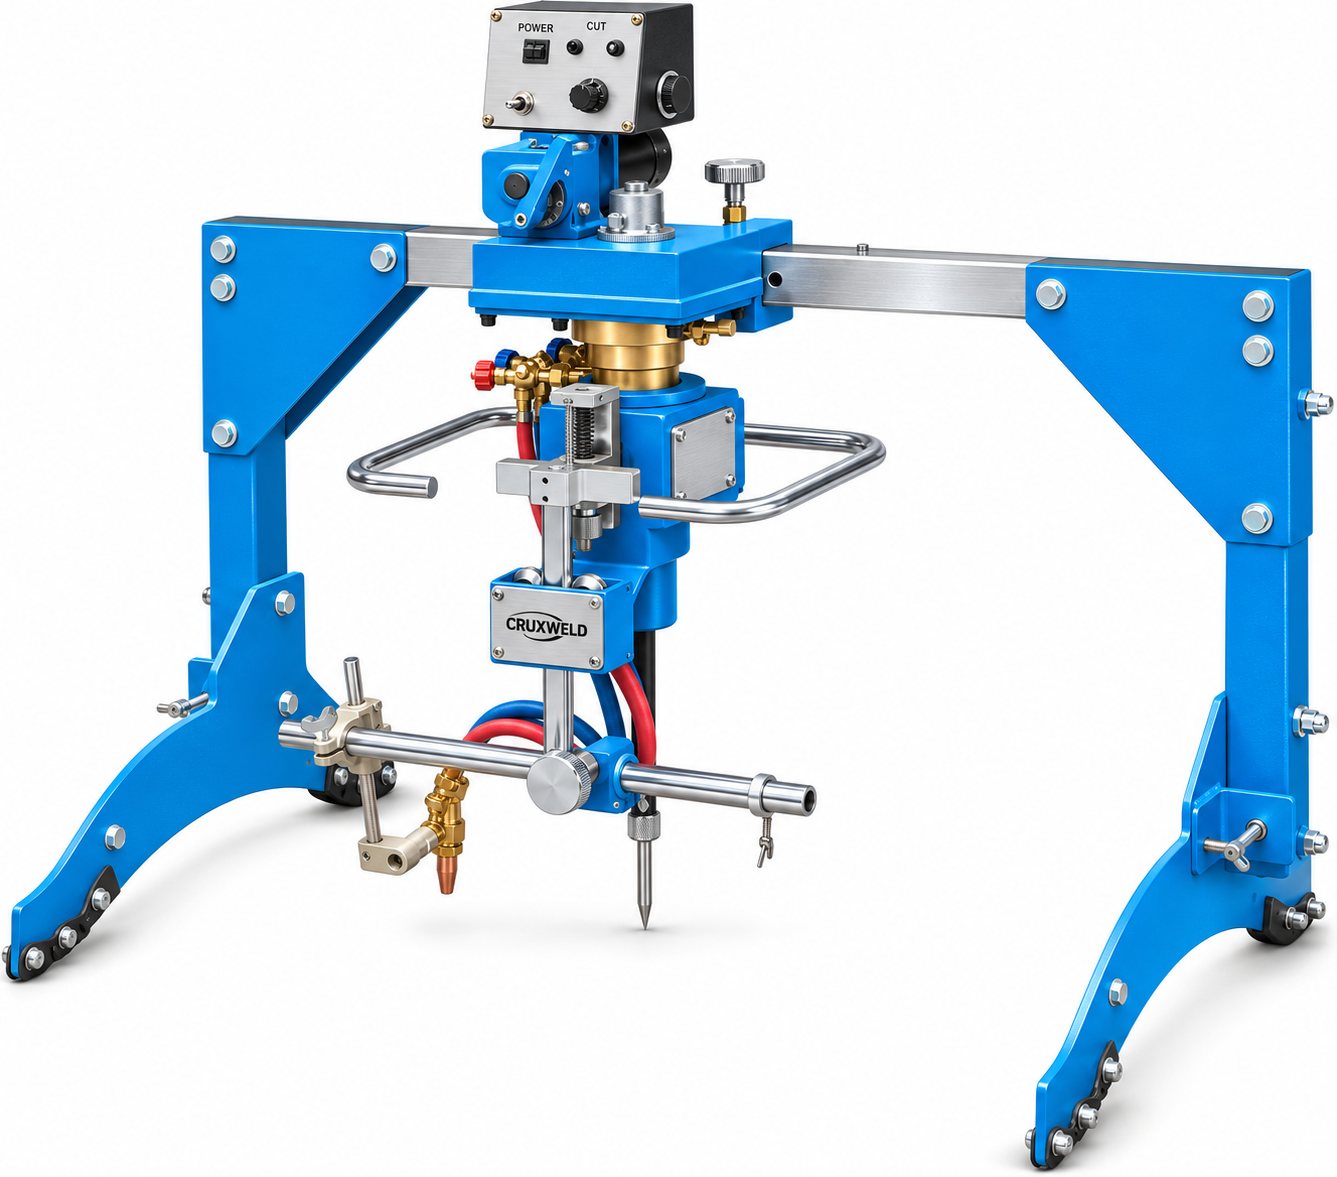
The thirteen parts an operator uses. The numbers on the drawing match the list beside it.
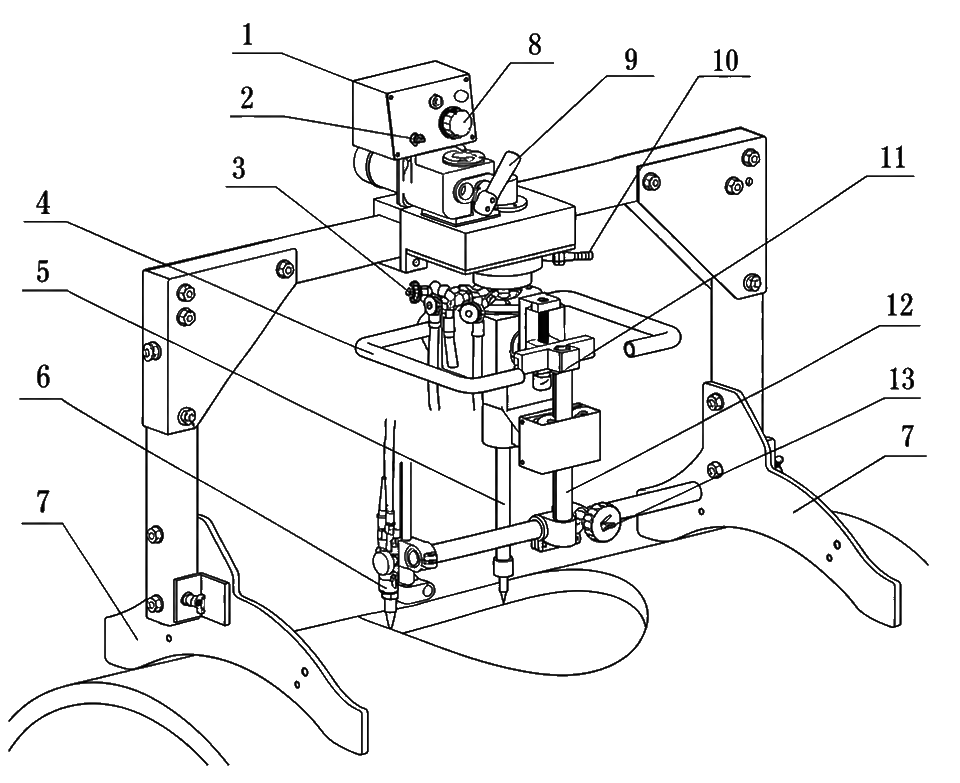
Once the saddle height is set, the mechanism raises and lowers the torch through every turn. The tip stays at working distance from crown to side of the pipe.
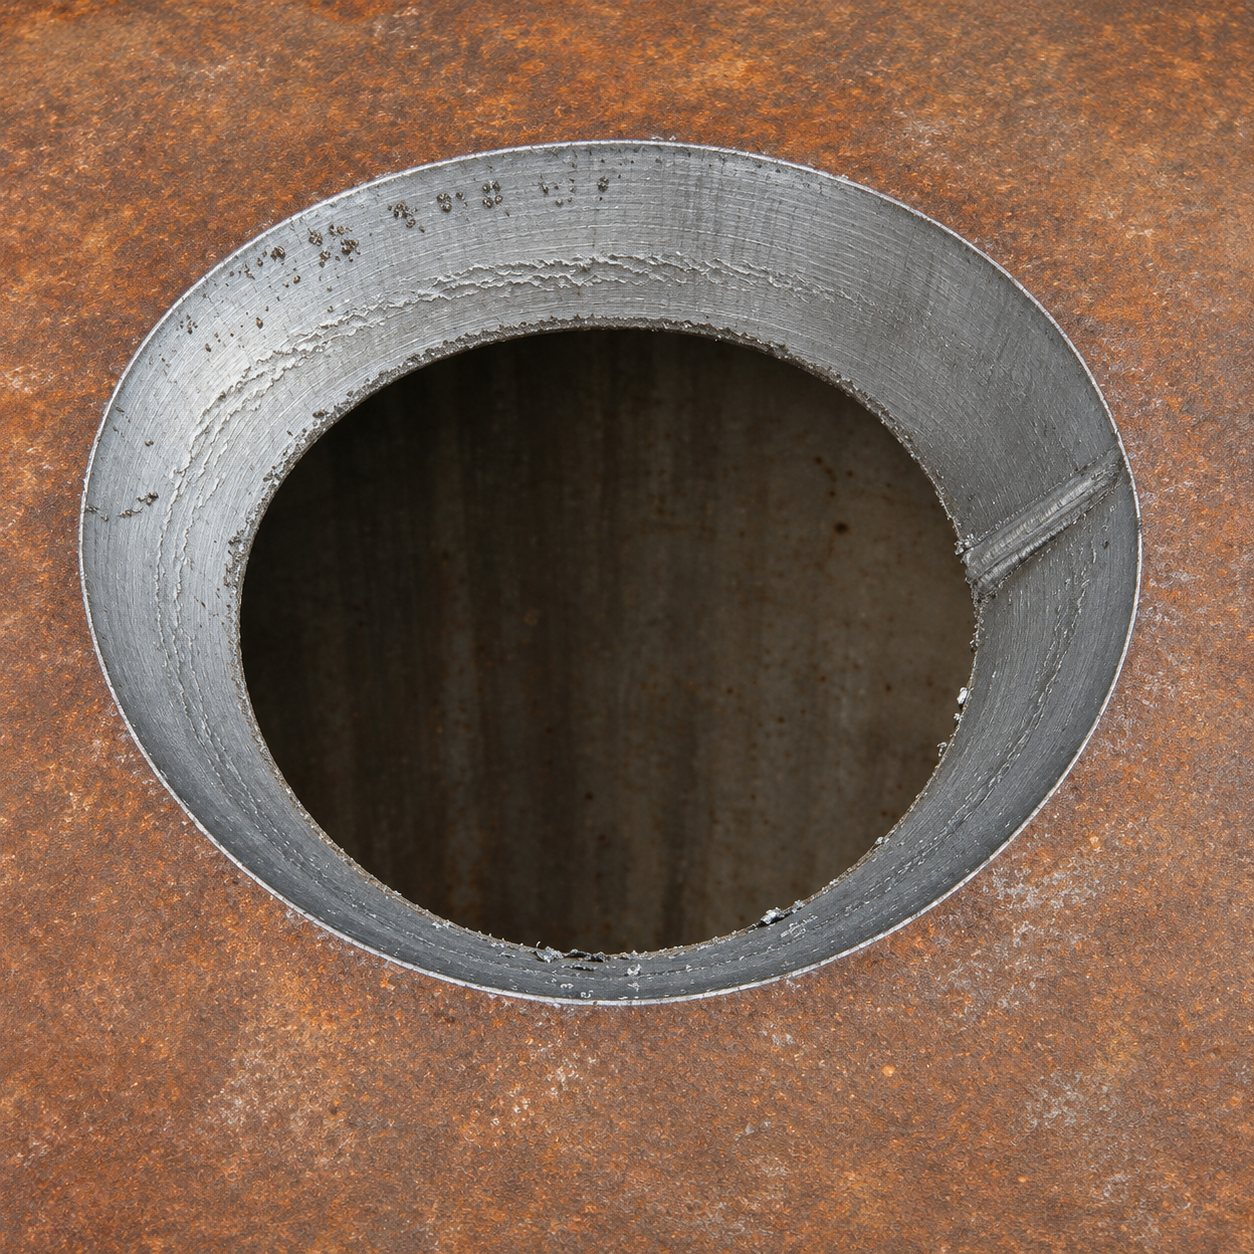
The torch tilts from 0 to 45°, so the opening can be cut with the bevel the weld needs. For bevels over 20° use the next tip size up.
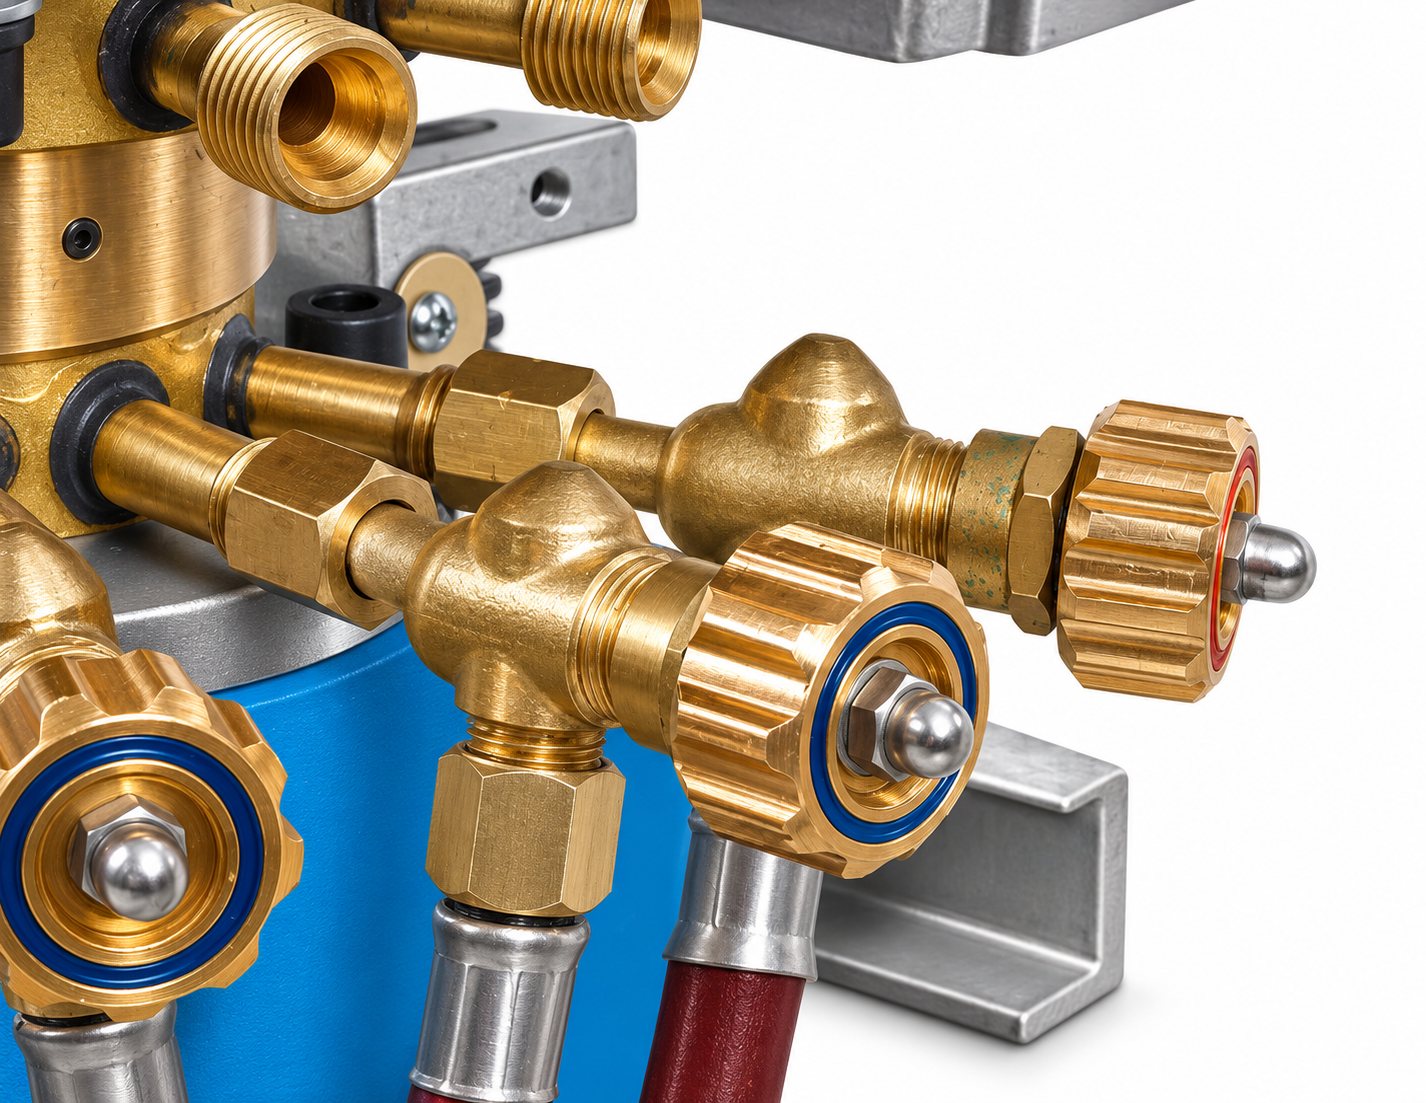
Oxygen and fuel gas feed through a rotating joint between the frame and the torch, so the hoses stay untwisted through any number of turns.
Release the clutch to move the torch round by the handle for positioning and a dry run, then engage it and let the drive make the cut.
The casing is mainly aluminium alloy to keep the weight down: 46.5 kg for the machine body. It stands on the pipe on four balanced feet.
With the saddle height set to zero it cuts plain circles and bevelled circles in flat plate, using the same centre cone and radius setting.
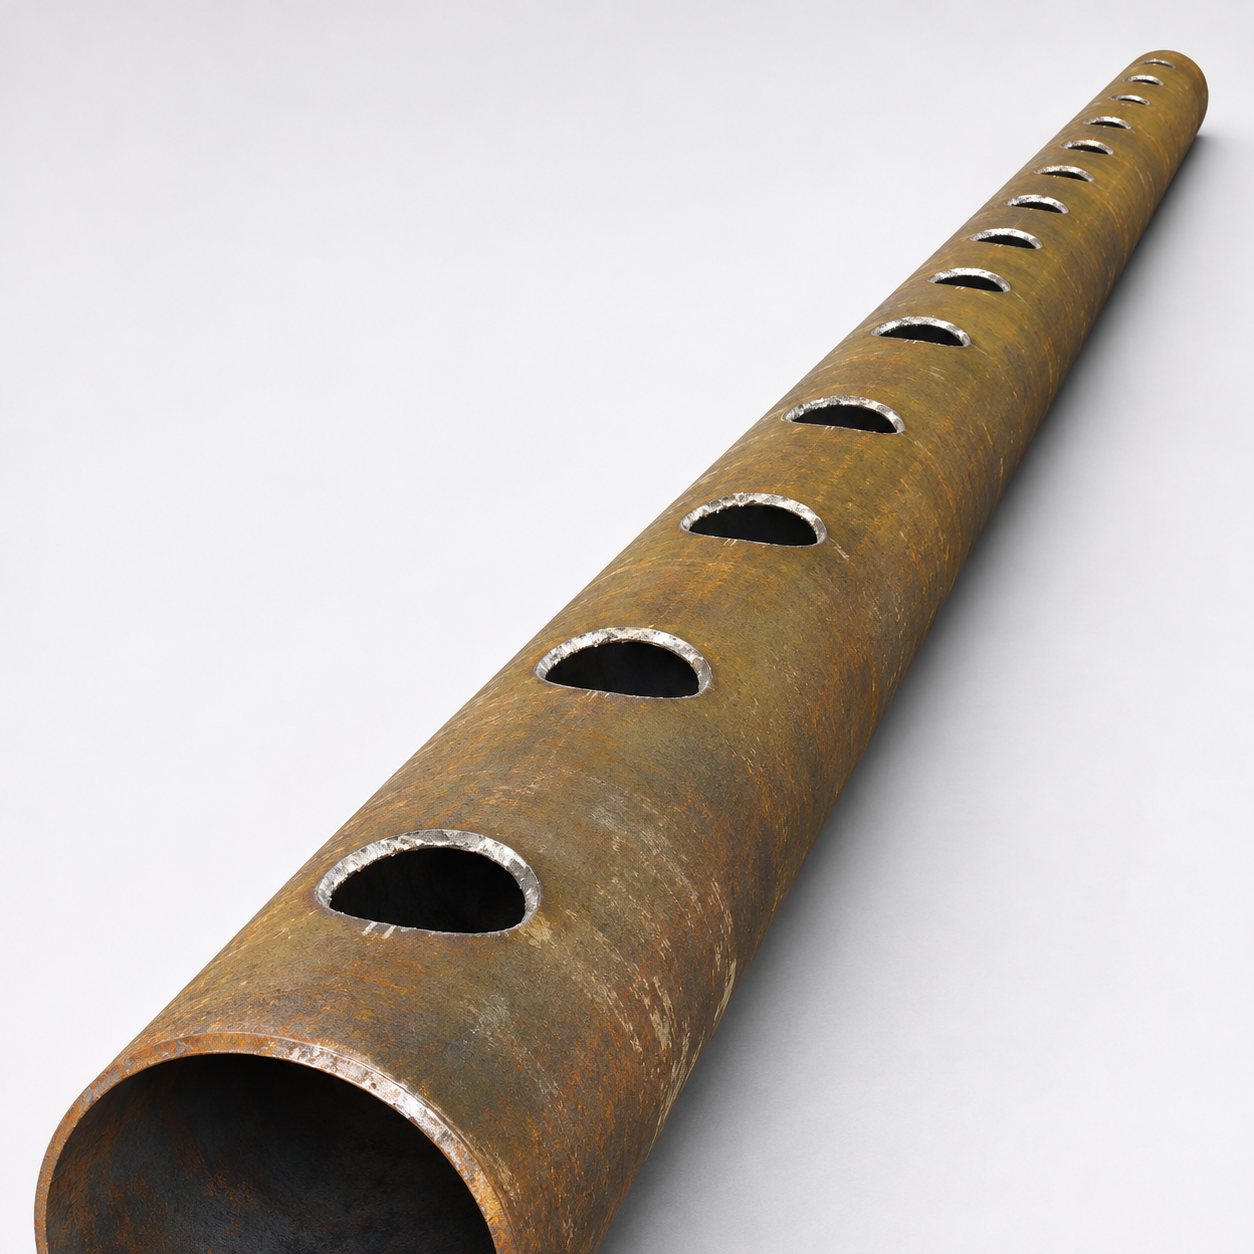
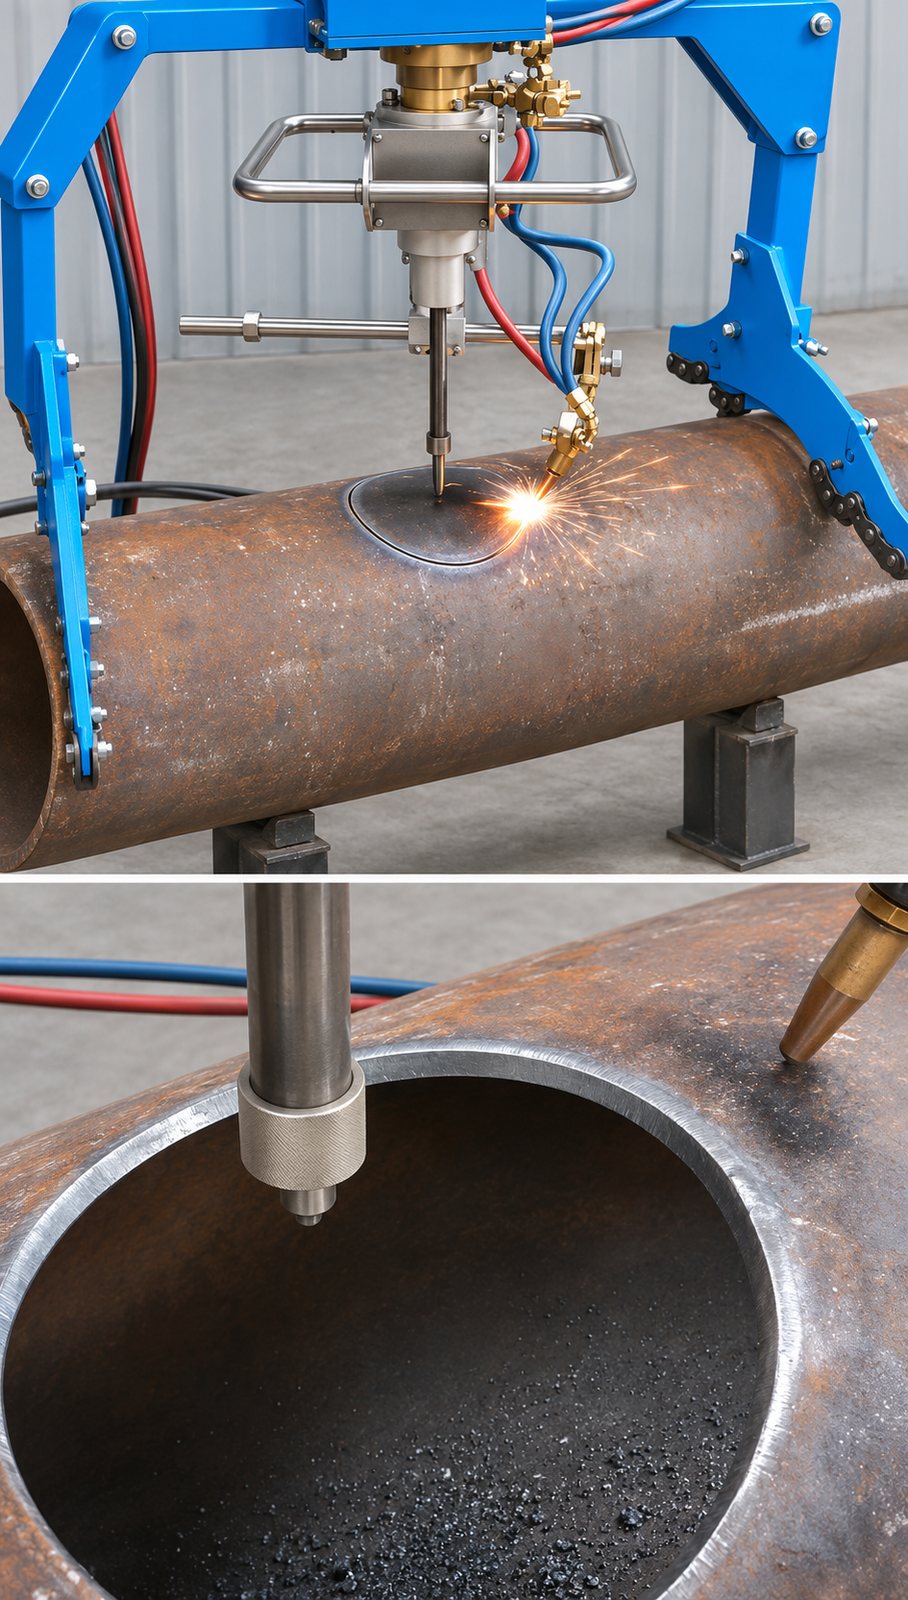 On the pipeThe torch circling the centre cone on a steel pipe.Bevelled openingA clean bevelled edge, ready for the branch weld.Repeat openingsA row of branch openings along one header pipe.
For a set-in branch, which passes into the main pipe, the hole matches the outside diameter of the branch. For a set-on branch, which sits on the main pipe, the hole matches its inside diameter. Tell us which you weld and our technical team will confirm the setting.
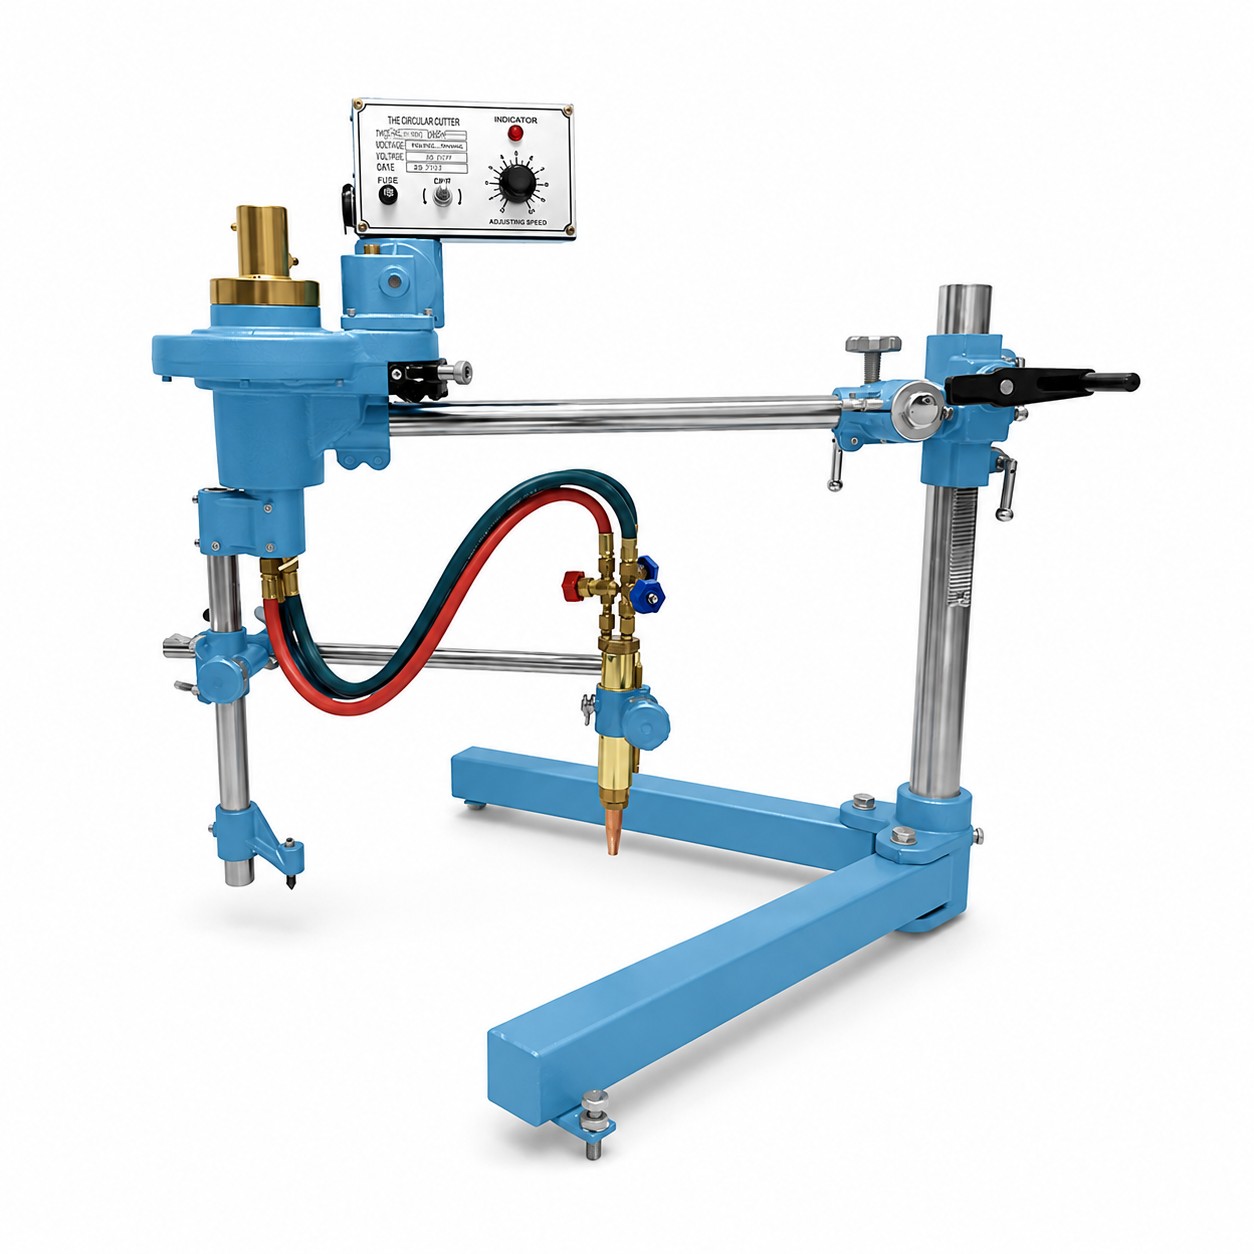
The ORBICUT 600 cuts openings in the pipe wall. These cut the pipe to length, the plate to size and the bevel on the pipe end.
Send the pipe outside diameter, wall thickness, hole diameter, bevel and fuel gas. Our technical team replies on WhatsApp with suitability, price and delivery.
Automatic pipe hole cutting machine
The 110 V rating is the internal drive motor; the machine is supplied from AC 220 V. Hole size, main-pipe diameter and saddle height must be considered together, so the full Ø80 to 600 mm range is not available on every pipe size. For carbon and mild steel suited to oxy-fuel cutting. Specifications as published by CRUXWELD.
The CRUXWELD ORBICUT 600 is a portable pipe hole cutting machine that cuts round branch openings in steel pipe, vessel shells and heat-exchanger shells with an oxy-fuel torch. The frame stands on the workpiece, a centre cone marks the middle of the opening, and an electric drive carries the torch round it at 0.12 to 1.2 rpm. Holes from Ø80 to Ø600 mm can be cut in steel from 5 to 50 mm thick.
What sets it apart from a circle cutter is the saddle-following mechanism. On a curved pipe wall the edge of a round hole rises and falls, and the mechanism lifts and lowers the torch through each turn to match, over a saddle height of 0 to 96 mm. The opening that results is the shape a branch pipe needs for a set-in or set-on joint.
The torch tilts from 0 to 45° to cut the weld bevel with the opening. With the saddle height set to zero the same machine cuts plain and bevelled circles in flat plate. Standard legs suit main pipe of Ø800 mm and above, and the small-pipe attachment supplied with the machine extends that down to Ø250 mm.
The casing is mainly aluminium alloy, the machine body weighs 46.5 kg and measures 1060 × 560 × 820 mm. A clutch lets the operator position the torch by hand, a rotating gas distributor stops the hoses twisting, and the control box on top carries the speed knob and the normal/reverse switch. It runs on AC 220 V with G02 tips for acetylene or G03 tips for propane.
The ORBICUT 600 sits in the Gas Cutting range beside the CIRCO 600 circle cutting machine, the TUBOCUT HG pipe cutting machine and the GLIDO 2T. Our technical team helps with set-up on WhatsApp and video call.