Troubleshooting guide › Fix it yourself, by machine › Gas cutting machines
A portable gas cutting machine is a small motor, a gearbox, a speed control and a torch. The torch faults are the same as any hand torch; the machine faults are the drive, the track and the hoses. This page is for the pug cutter, the trolley carriages, the circle cutter, the chain-type pipe cutters and the magnetic profile cutter.
Reviewed by the Cruxweld technical team, October 2026. Settings are starting points to confirm on a test piece; acceptance is decided by the code or drawing the job is built to. Checks marked “call” are for our technical team.
| What you see | Check yourself | If it persists |
|---|---|---|
| Machine will not run | Power and fuse; motor brush stuck (remove, dress the end, refit); clutch disengaged; gearbox key or pin missing | Motor or gearbox: call |
| Motor runs, machine does not move | Drive wheel lifted or slipping; all wheels in the track; track dirty | Gearbox: call |
| Speed uneven or will not adjust | Speed potentiometer; dirty track or wheels; hoses or cable dragging | Replace the potentiometer; clean; support hoses |
| Vibration and noise | Debris on the guide surface; worn worm wheel or burrs; motor | Replace worn parts: call |
| Cut wanders off line | Track 75-100 mm from the line and parallel; castor locked for straight cuts; all wheels seated | Reset the track |
| Cut face angled | Bevel scale at zero; torch holder tight | Square and tighten |
| Gas leak and flame at the torch joint | Poor contact at the 30-degree cone (dress lightly with fine emery); nozzle nut loose | Replace the nozzle or torch head |
| Flame unstable, popping | Nozzle orifice blocked (clean with the right size cleaner); supply pressure low; oxygen purity; nozzle overheated or too close | Replace the nozzle |
| Preheat flame uneven, oxygen jet split or bent | Nozzle damaged | Replace the nozzle |
| Circle cut does not close (CIRCO / radius bar) | Centre pin slipping; radius bar loose; hoses pulling the machine | Fix the pin; tighten; loop the hoses |
| Pipe cutter chain slips or binds (TUBOCUT) | Chain tension; pipe surface clean; drive sprocket worn; magnet face clean (MS) | Sprocket: call |
| Profile cutter (WING) tracer wanders | Template clean and secure; magnetic tracer pin clean; tracer speed | Call |
| Cut starts badly, slag sticks | See the gas cutting page: nozzle size, pressures, preheat, speed |
Only with the drive wheel lifted or the clutch disengaged. Pushing with the drive engaged damages the gearbox.
Yes, with the LPG nozzle for the plate thickness, a slightly higher fuel pressure and a nozzle height of 5-8 mm instead of 8-10 mm for acetylene. Expect a longer preheat.
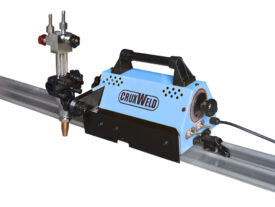 CPG-NM pug cutting machineSpecifications →
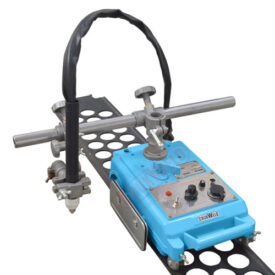 UNITRACK-45K welding and cutting carriageSpecifications →
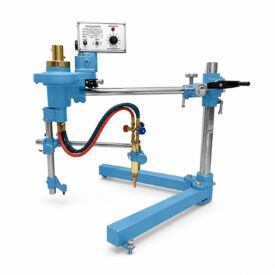 CIRCO 600 / 1000 circle cutterSpecifications →
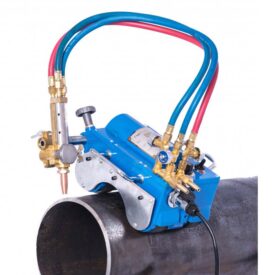 Magnetic pipe cutting machineSpecifications →
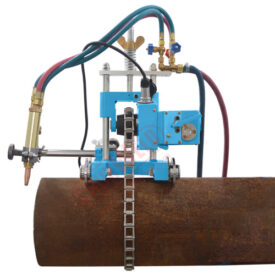 Portable gas pipe cutting machineSpecifications →
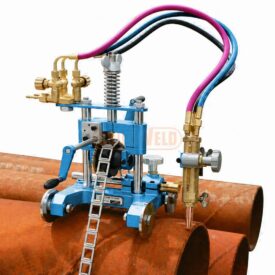 Hand-driven pipe gas cutting machineSpecifications →
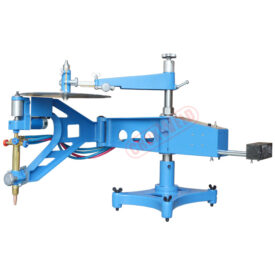 Profile cutting machineSpecifications →
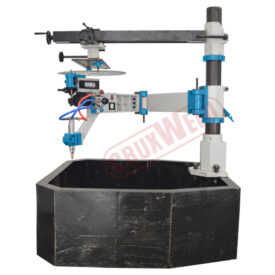 Pillar mounted profile cutterSpecifications →
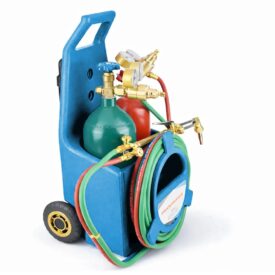 Oxy-acetylene cutting kitSpecifications →
Open your model for its specifications; the spares page lists the consumables for it.
If the machine runs but the weld or cut is wrong, the cause is usually settings, consumables or the material. Start here:
The machine gives a constant speed and height; the cut quality is then the nozzle, the pressures and the track. Keep two spare nozzles, a tip cleaner and a track cleaning brush with every machine.
Send a photo of the weld or cut, your machine model, consumable and plate thickness. Our technical team replies on WhatsApp with the likely causes and the next checks to make.
45+ years of welding expertise · GeM Registered OEM Manufacturer · Supported Worldwide

