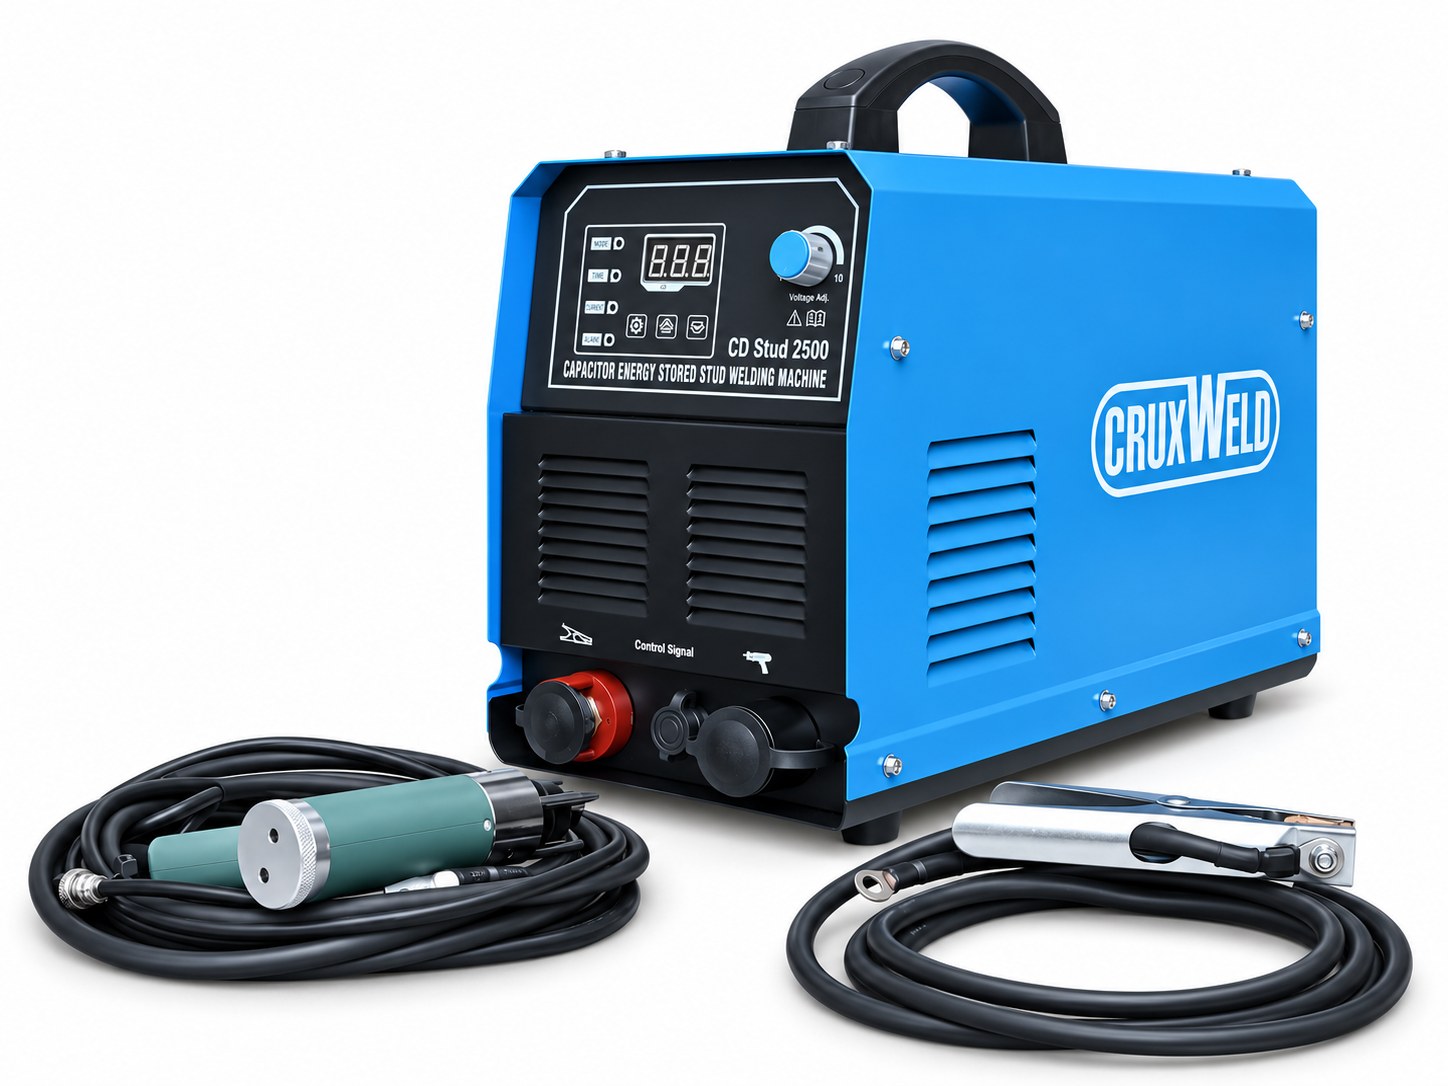
3500 Joules. Three Milliseconds. One Clean Stud, No Mark on the Back.
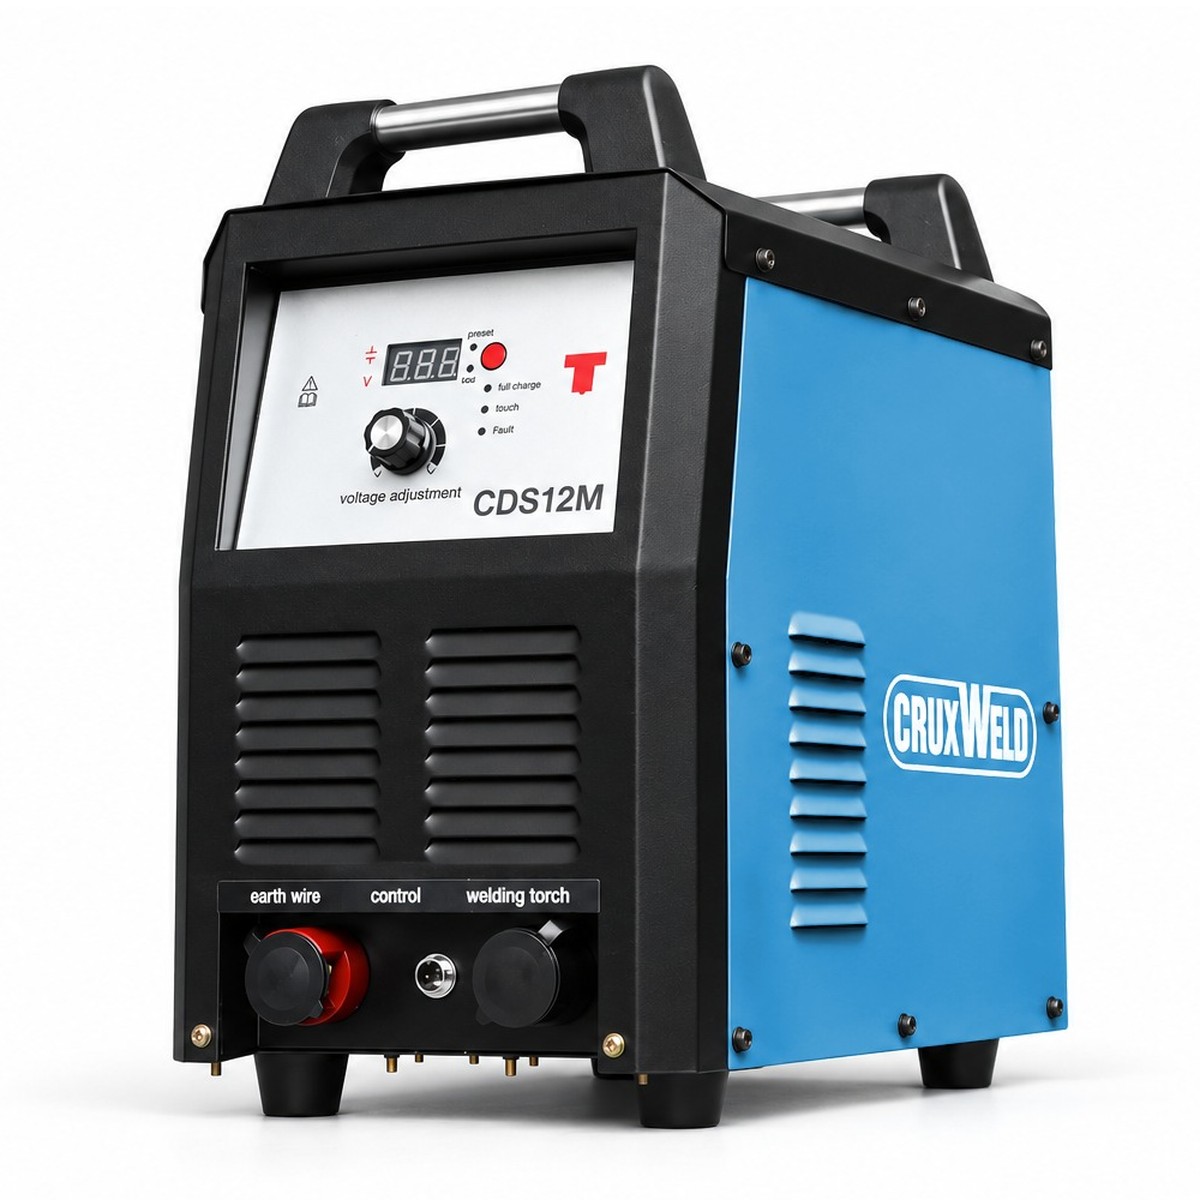
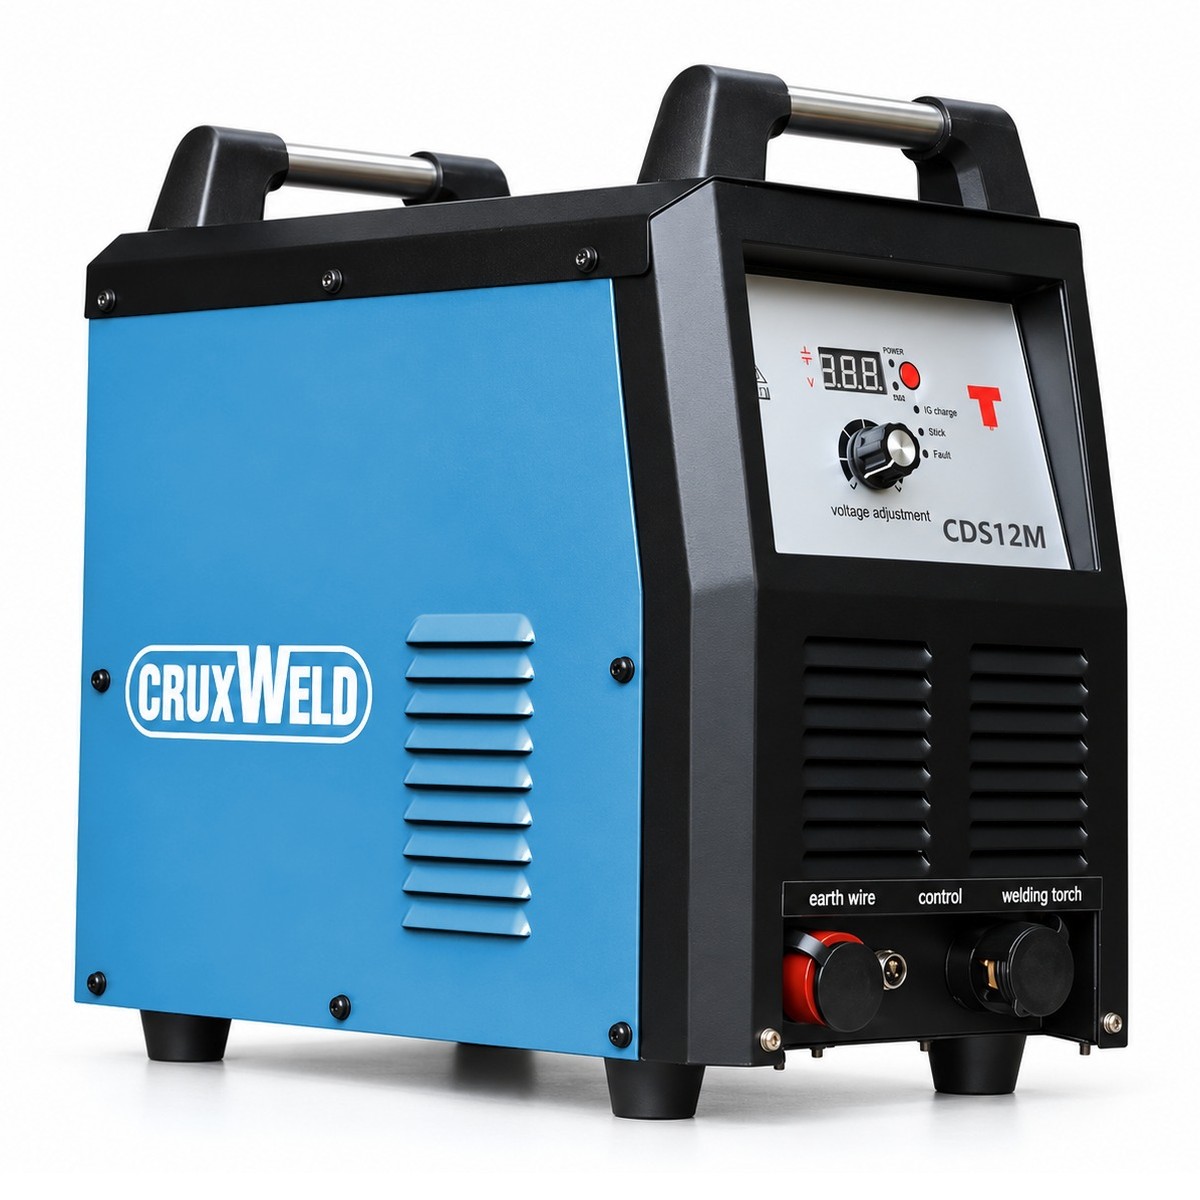
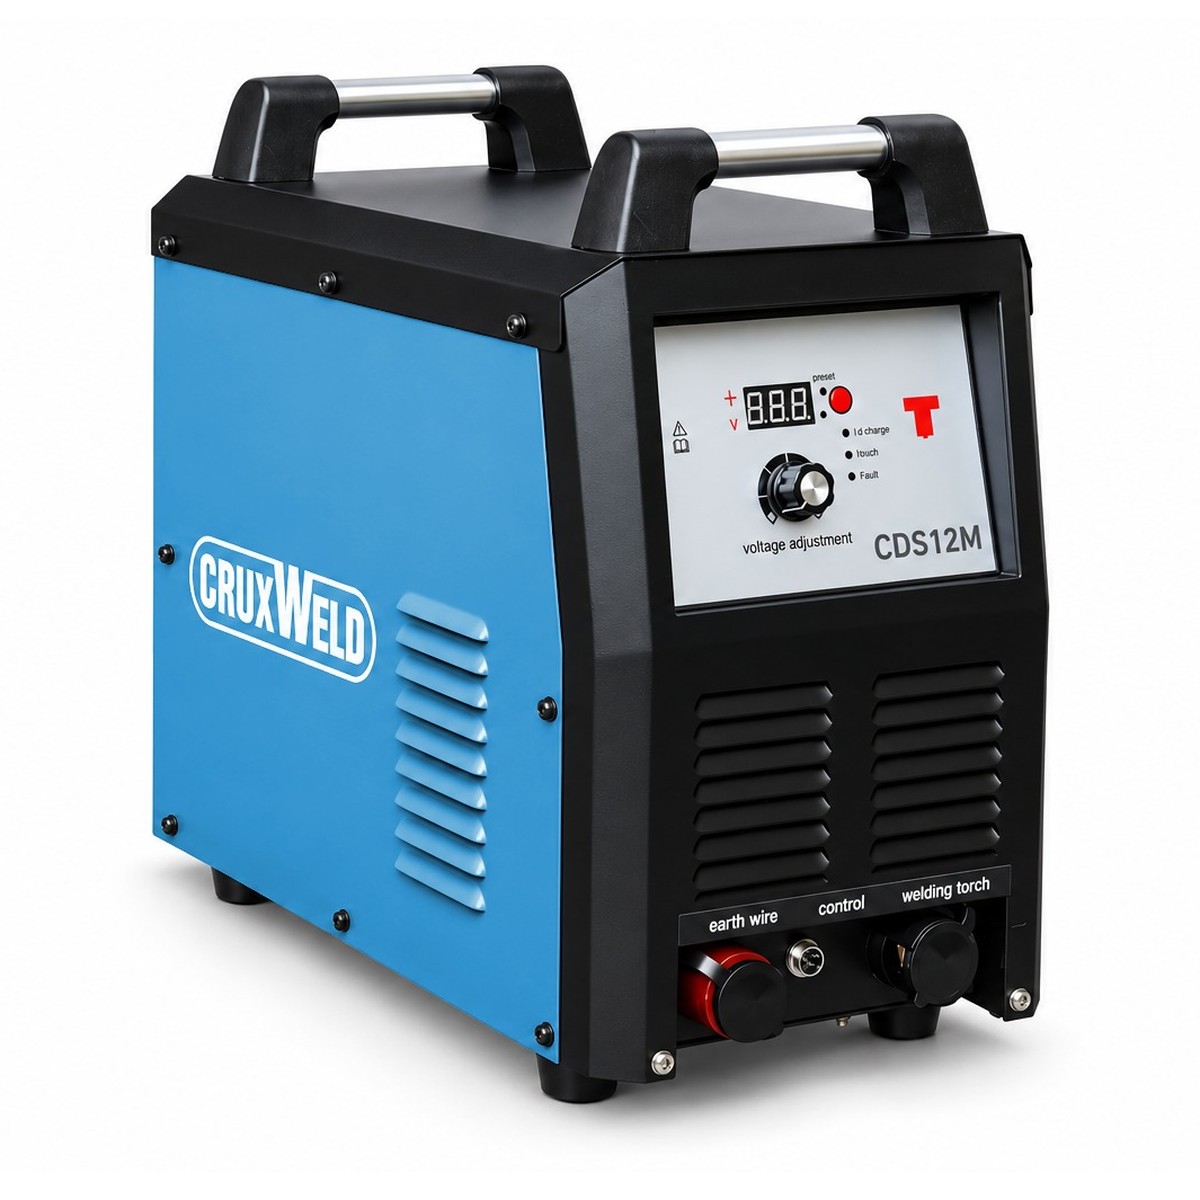
The CRUXWELD CDS12M is a CD stud welding machine that stores 3500 J in a 180,000 µF capacitor bank and releases it in a single 1–3 ms pulse — welding threaded studs, pins and bosses from M3 to M12 onto mild steel, stainless steel, aluminium and brass sheet. No gas, no flux, no drilling, and the show face stays flat.
Recharges in under 3 seconds — up to 40 studs a minute
A Threaded Fixing in Three Milliseconds, Without a Hole
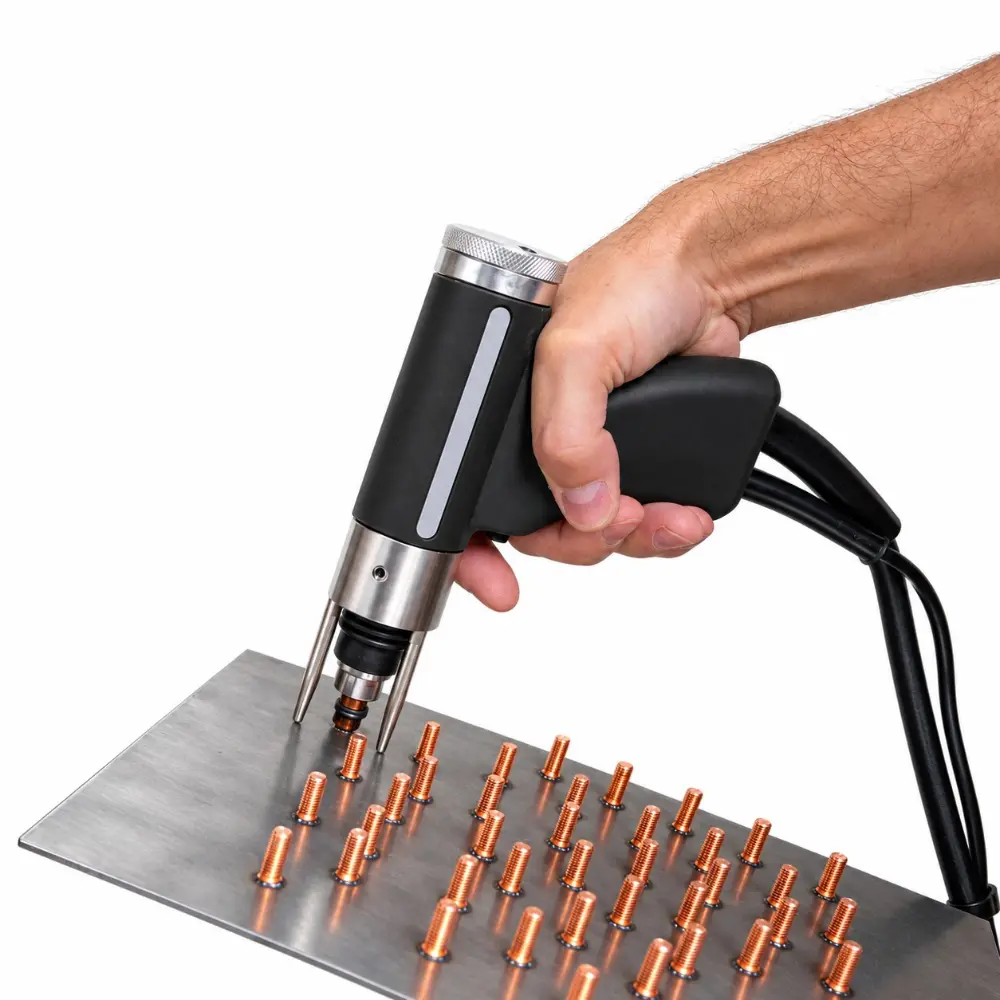
Drilling, tapping and a nut on the back is three operations and a mark on the show face. A CD stud welding machine does it in one trigger pull: the stud’s ignition tip touches the sheet, the capacitors discharge, the arc melts the full stud face, and the gun spring plunges it home before heat can travel through the sheet.
The CDS12M is the higher-capacity CRUXWELD CD model. 3500 J of stored energy reaches M12 studs on steel while the same dial turns down to M3 pins on thin aluminium, and a sub-3-second recharge keeps a production line moving at up to 40 studs a minute.
No mark on the back
1–3 ms weld time; painted, galvanised and polished sheet stays clean.
M3 to M12, four materials
Mild steel, stainless, aluminium and brass studs, pins and bosses.
No gas, no flux
The energy comes from the capacitors. Nothing to buy except studs.
Single-phase
110 V or 220 V, under 0.8 kW — bench or line.
Watch: CD stud welding on the shop floor
Three operations, or one trigger pullA drilled and tapped fixing needs a hole, a thread and a nut behind the sheet. A CD stud is welded in a single 1–3 ms pulse, with no hole, so the painted or polished face on the back stays clean.
02
How it works
Charge, Contact, Discharge, Plunge
1
Charge
The 180,000 µF bank charges to the set voltage (35–200 V DC) in under 3 seconds. One dial sets the energy for the stud size and material; the panel LED shows full charge.
2
Contact
Load a stud in the chuck, rest the gun’s two support legs on the sheet and press until the stud’s ignition tip touches the surface.
3
Discharge
On the trigger, 3500 J releases in 1–3 ms: the tip vaporises, an arc melts the whole stud face and a thin skin of the sheet.
4
Plunge
The gun spring drives the stud into the molten pool and the joint freezes at once — a full-face weld stronger than the stud itself. Load the next one.
Capacitor bank · 180,000 µF
High Power, Fast Charging
CHARGE
0 s35–200 V DC< 3 s
< 3 seconds
READY
DISCHARGE · 1–3 ms
Full-charge LED on — weld the next stud. Up to 40 a minute.
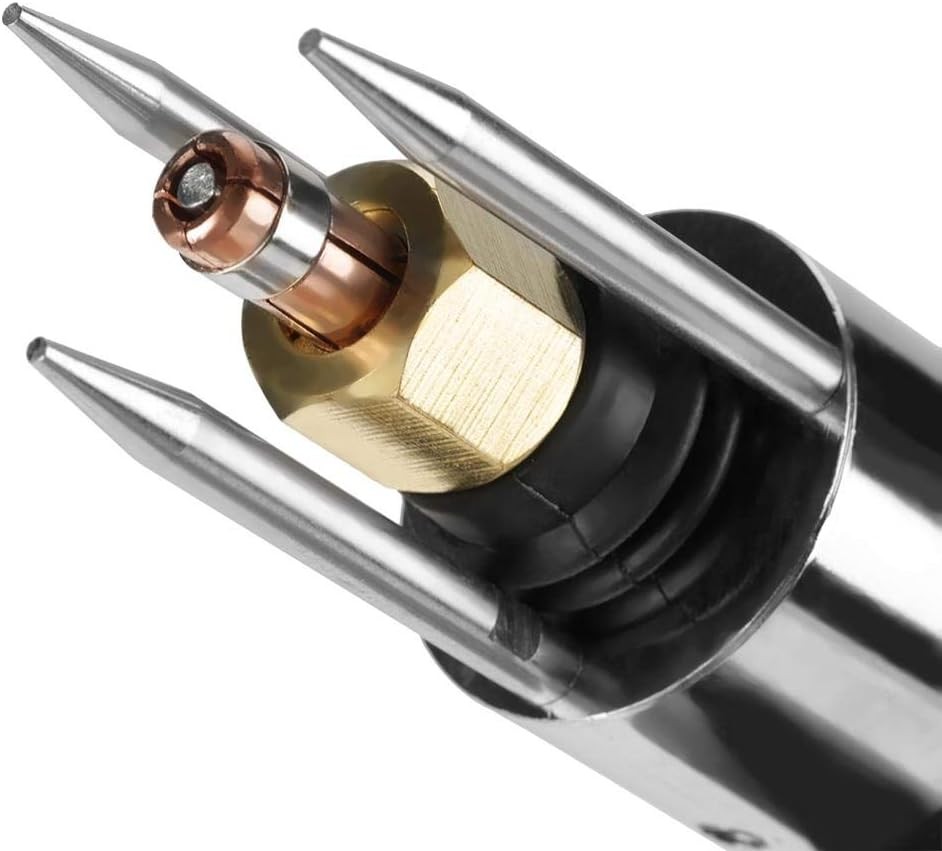
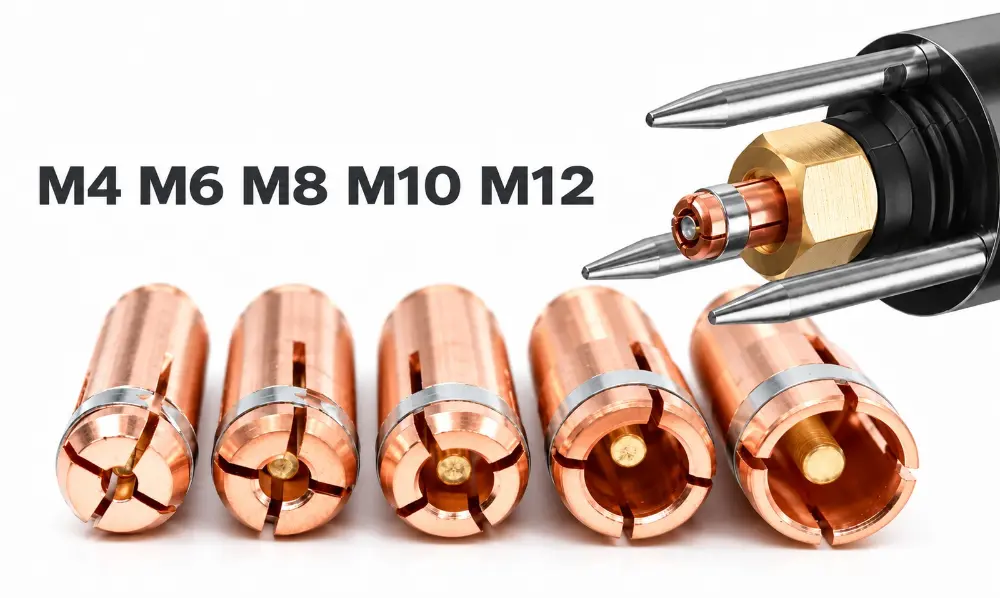
Collet, ignition-tip stud and the two support legs
One collet per stud size, M4 to M12
03
The weld
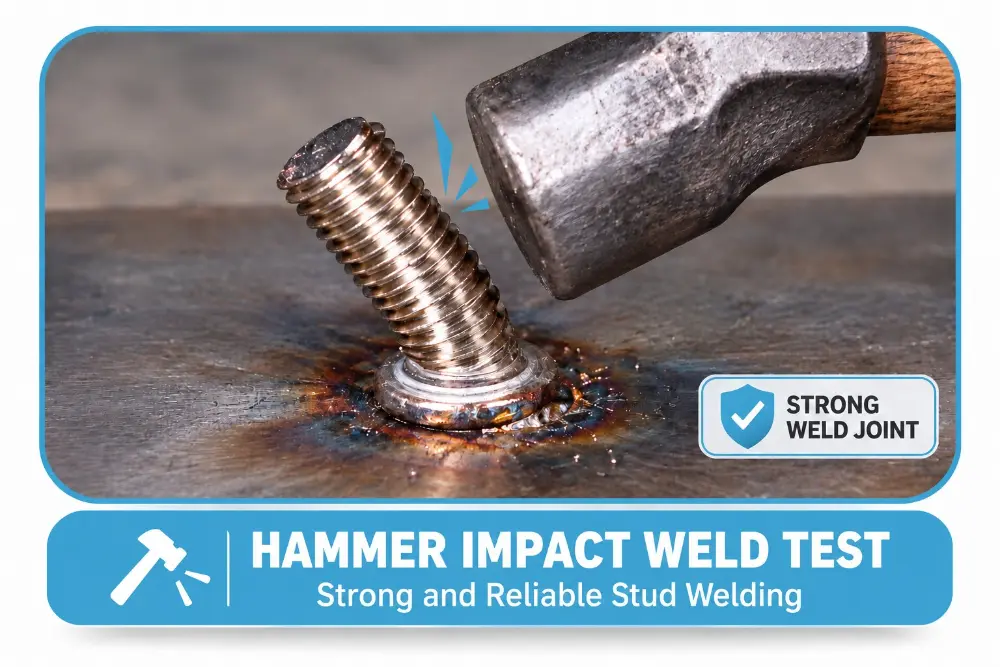
Bend It, Hit It, Pull It — the Stud Gives Before the Weld Does
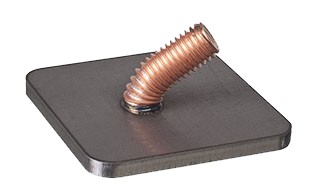
The quick check on the first stud of a batchSlip a tube over the stud and bend it 30°. The ignition tip melts the full stud face, so a good weld bends the stud, never the joint.
Hammer impact test — the stud bends, the weld holds
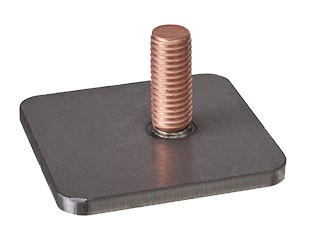
As welded
Bend test
The ignition-tip stud melts over its full face, so the fused area is the whole stud diameter. A bend test on the first stud of every batch — 30° over with a tube — is the quick check: a good weld bends the stud, never the joint.
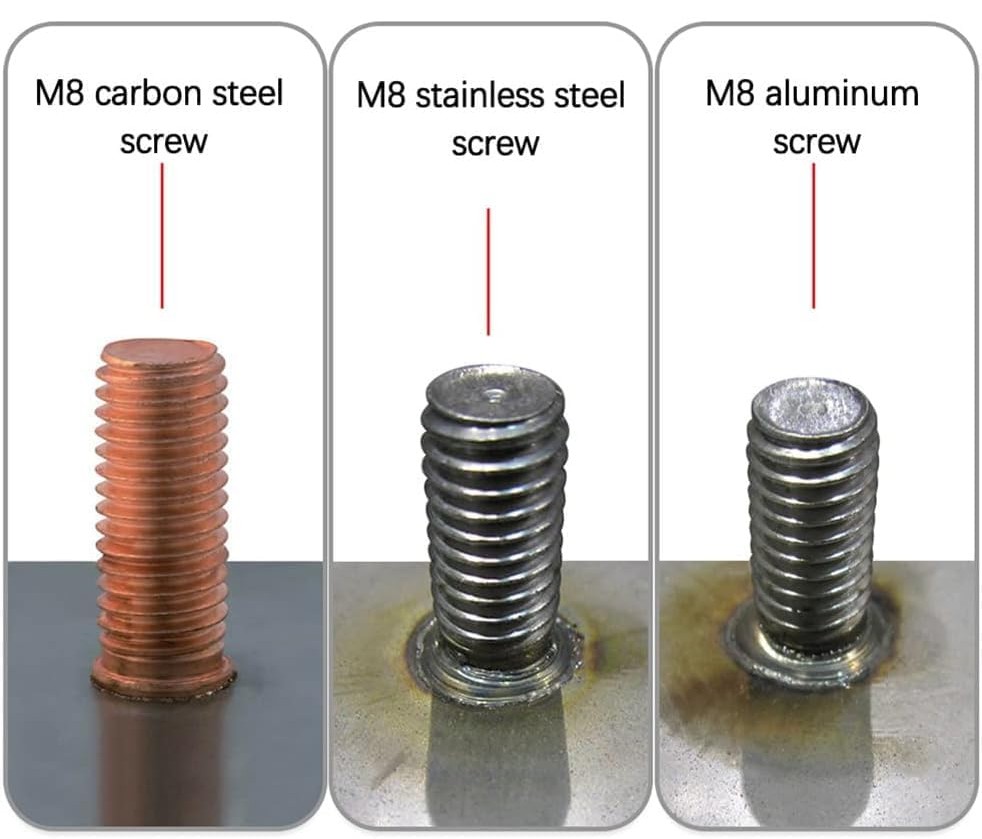
M8 on carbon steel, stainless and aluminium
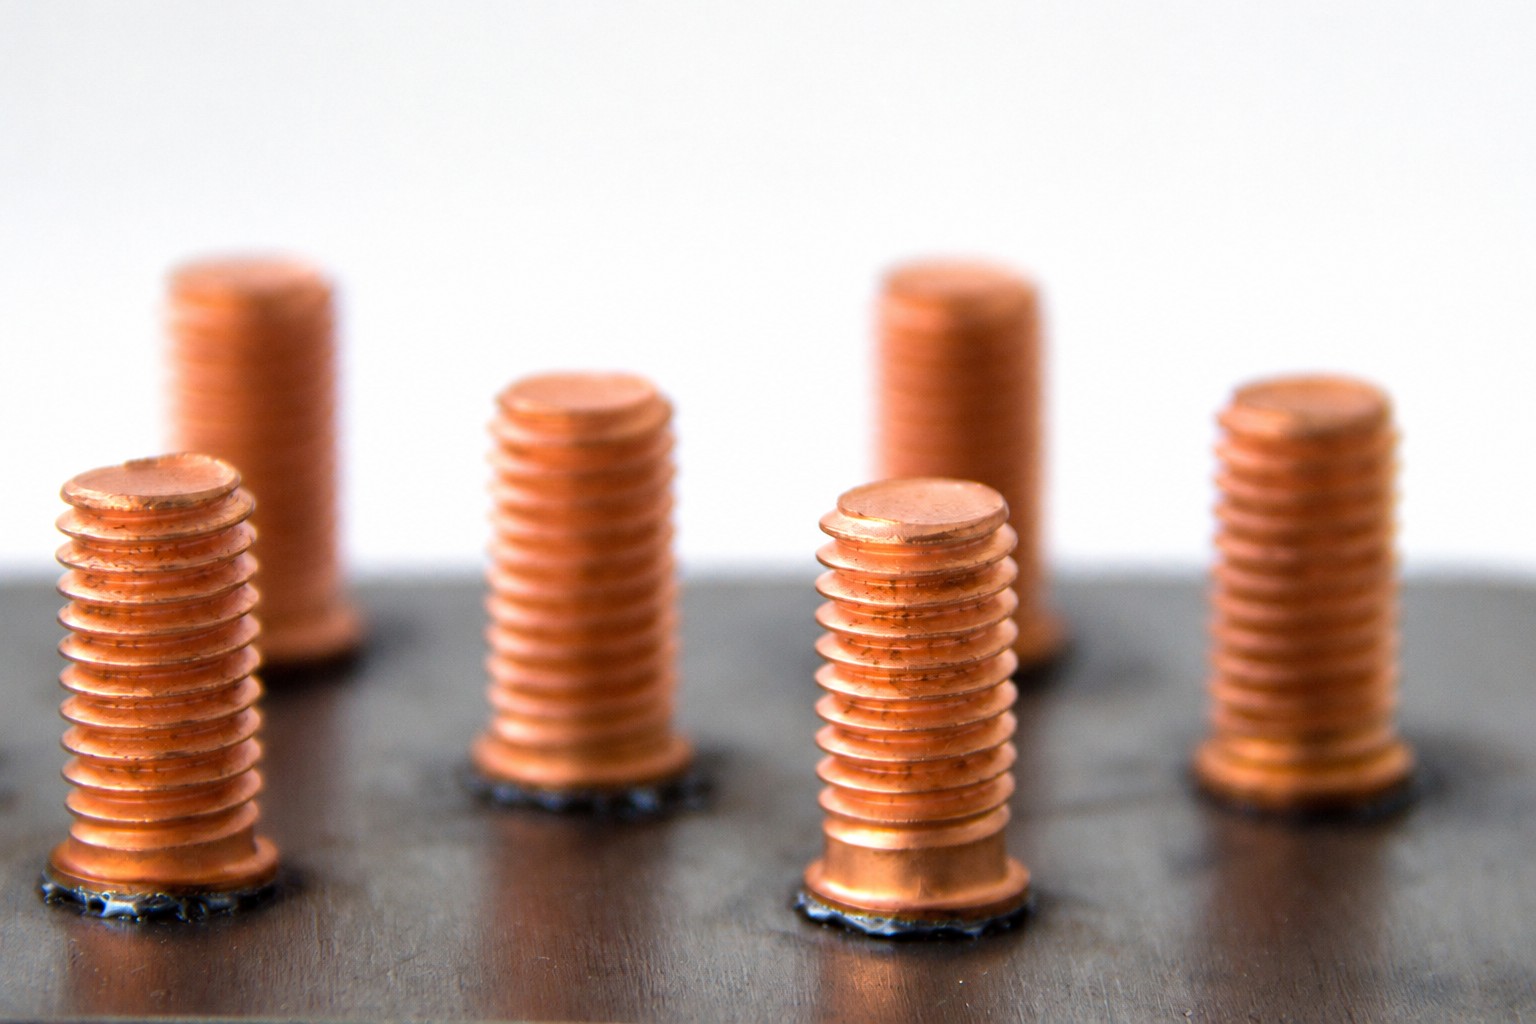
Copper-plated steel studs on sheet
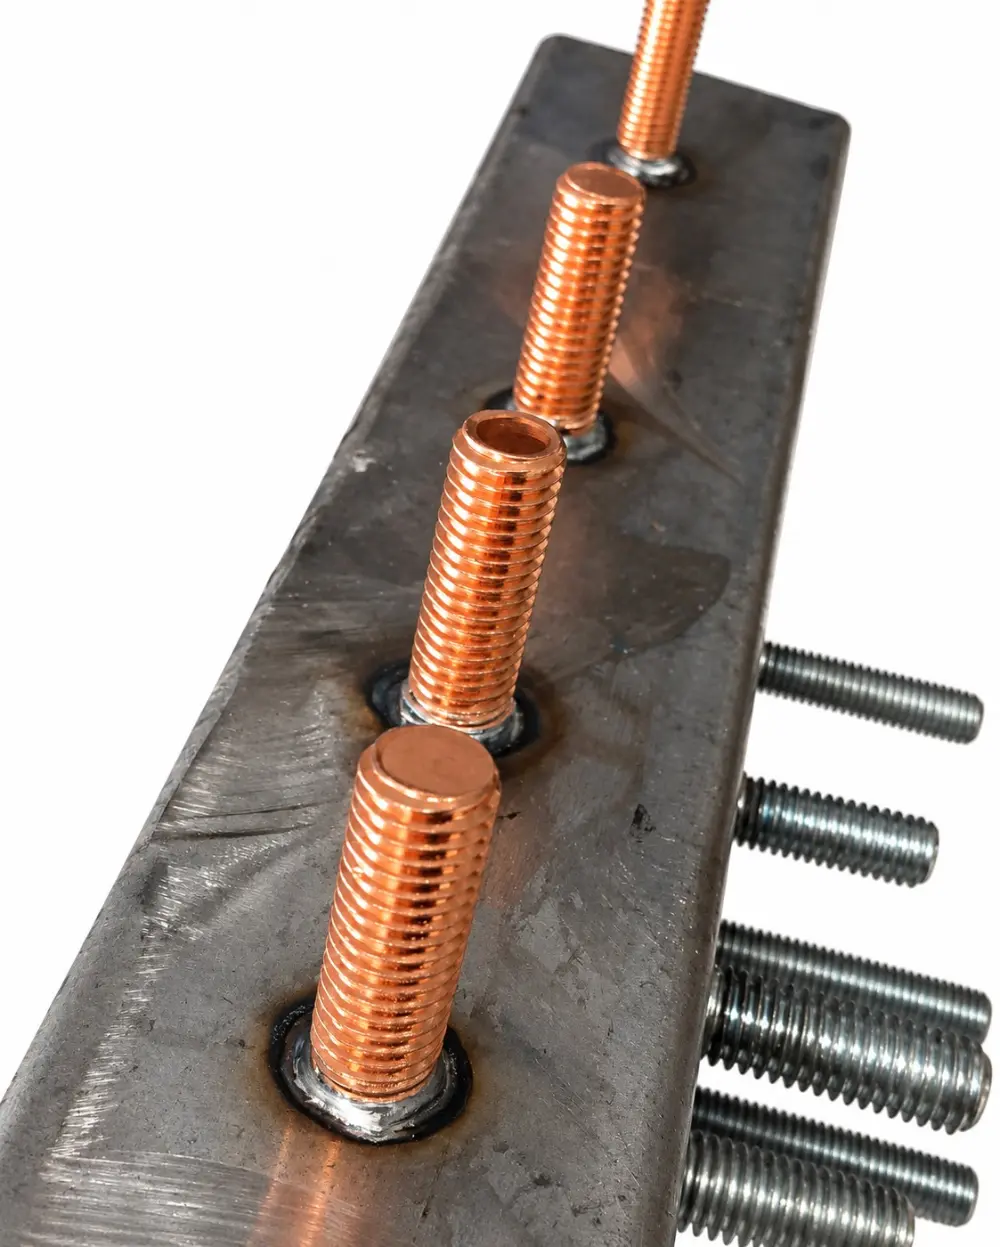
A row along a bar
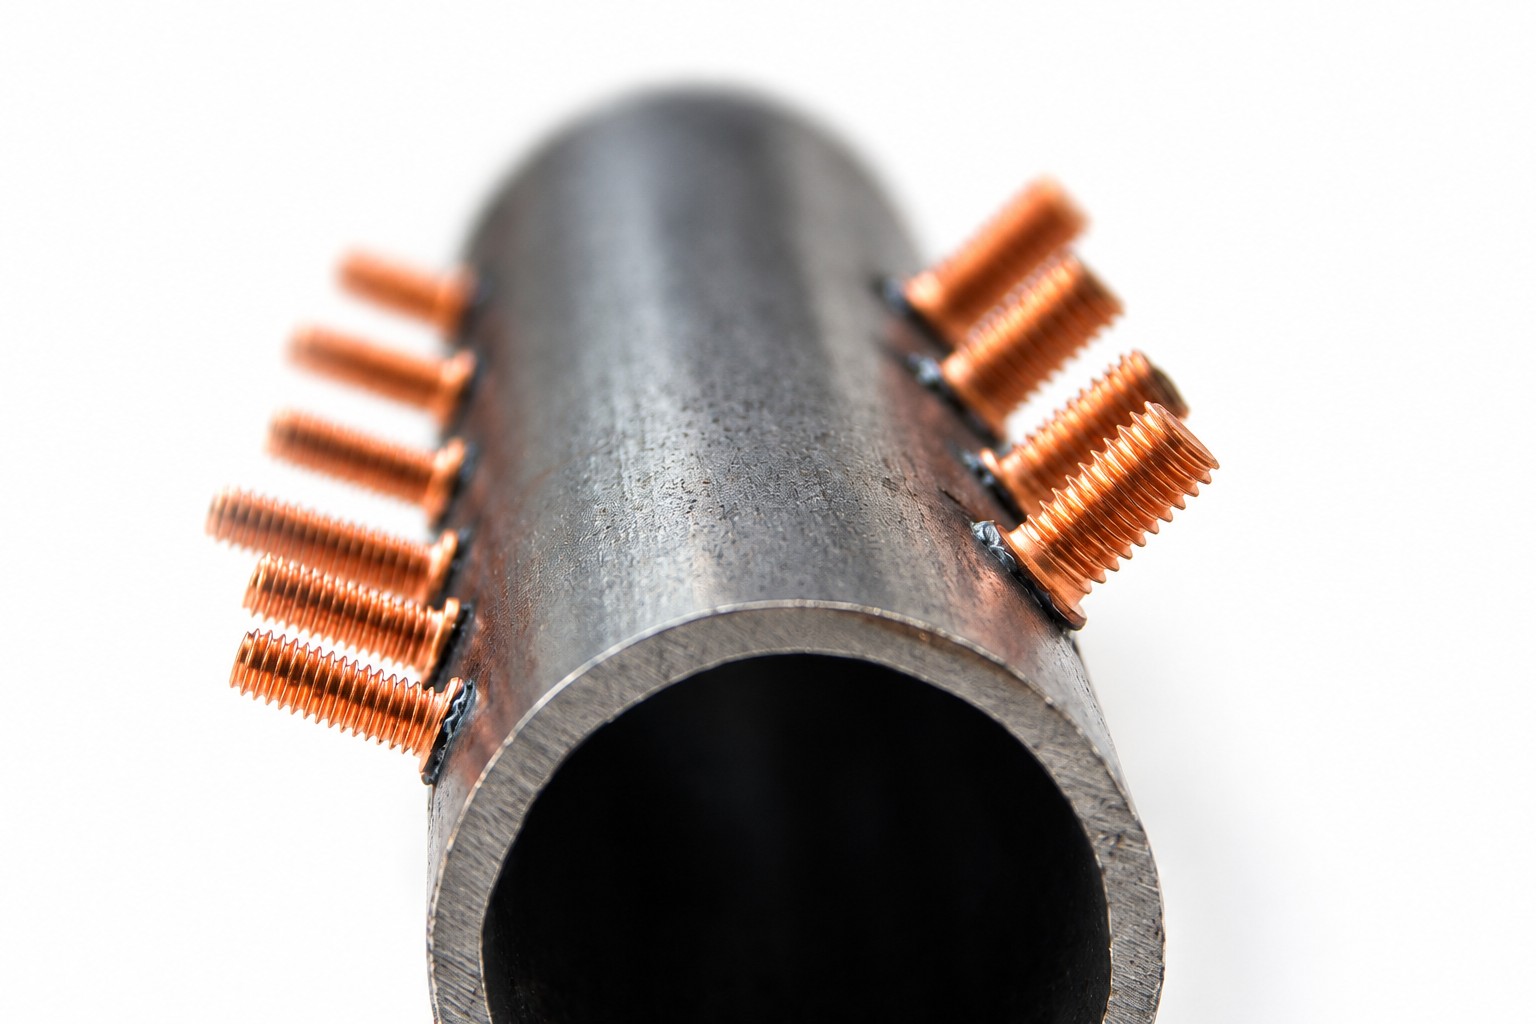
Around a pipe
04
What it welds
Studs, Bosses, Pins and Nails in Steel, Stainless, Aluminium and Brass
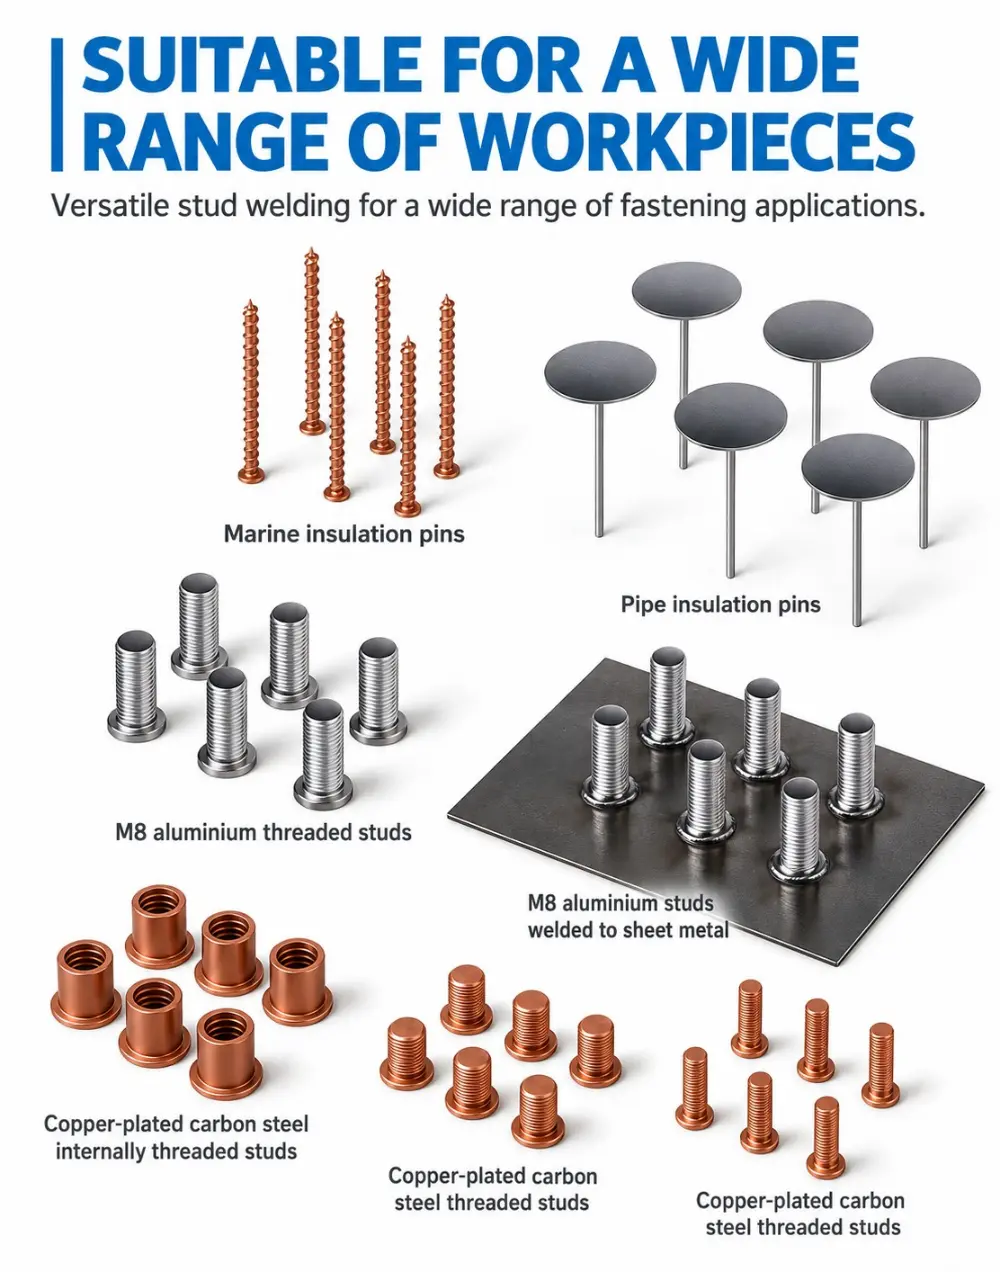
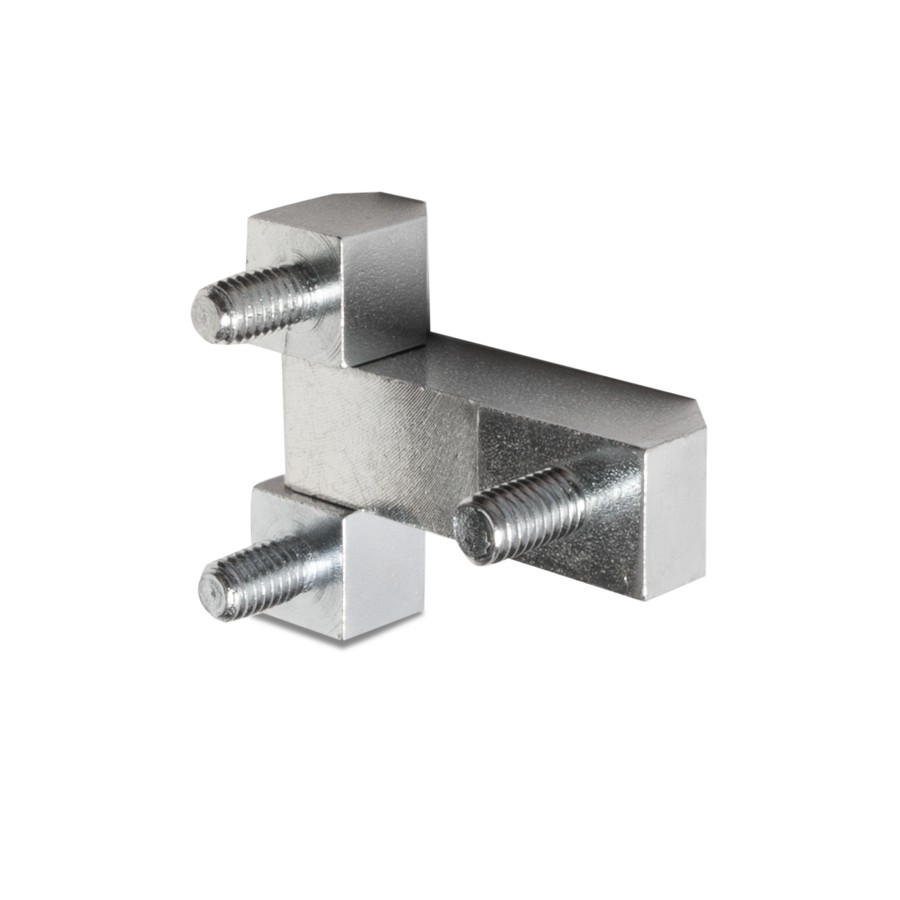
Threaded studs, tapped bosses, insulation pins and nails
A CD stud welding machine welds any stud that carries a small ignition tip on its weld face. The CDS12M takes the standard range in all four materials:
Steel from thin sheet upwards; aluminium and brass need a clean, oxide-free surface and the matching stud material. Send us a drawing or a photo and our technical team will confirm stud and chuck sizes.
On a machined bracket
On a stainless clip
05
The kit
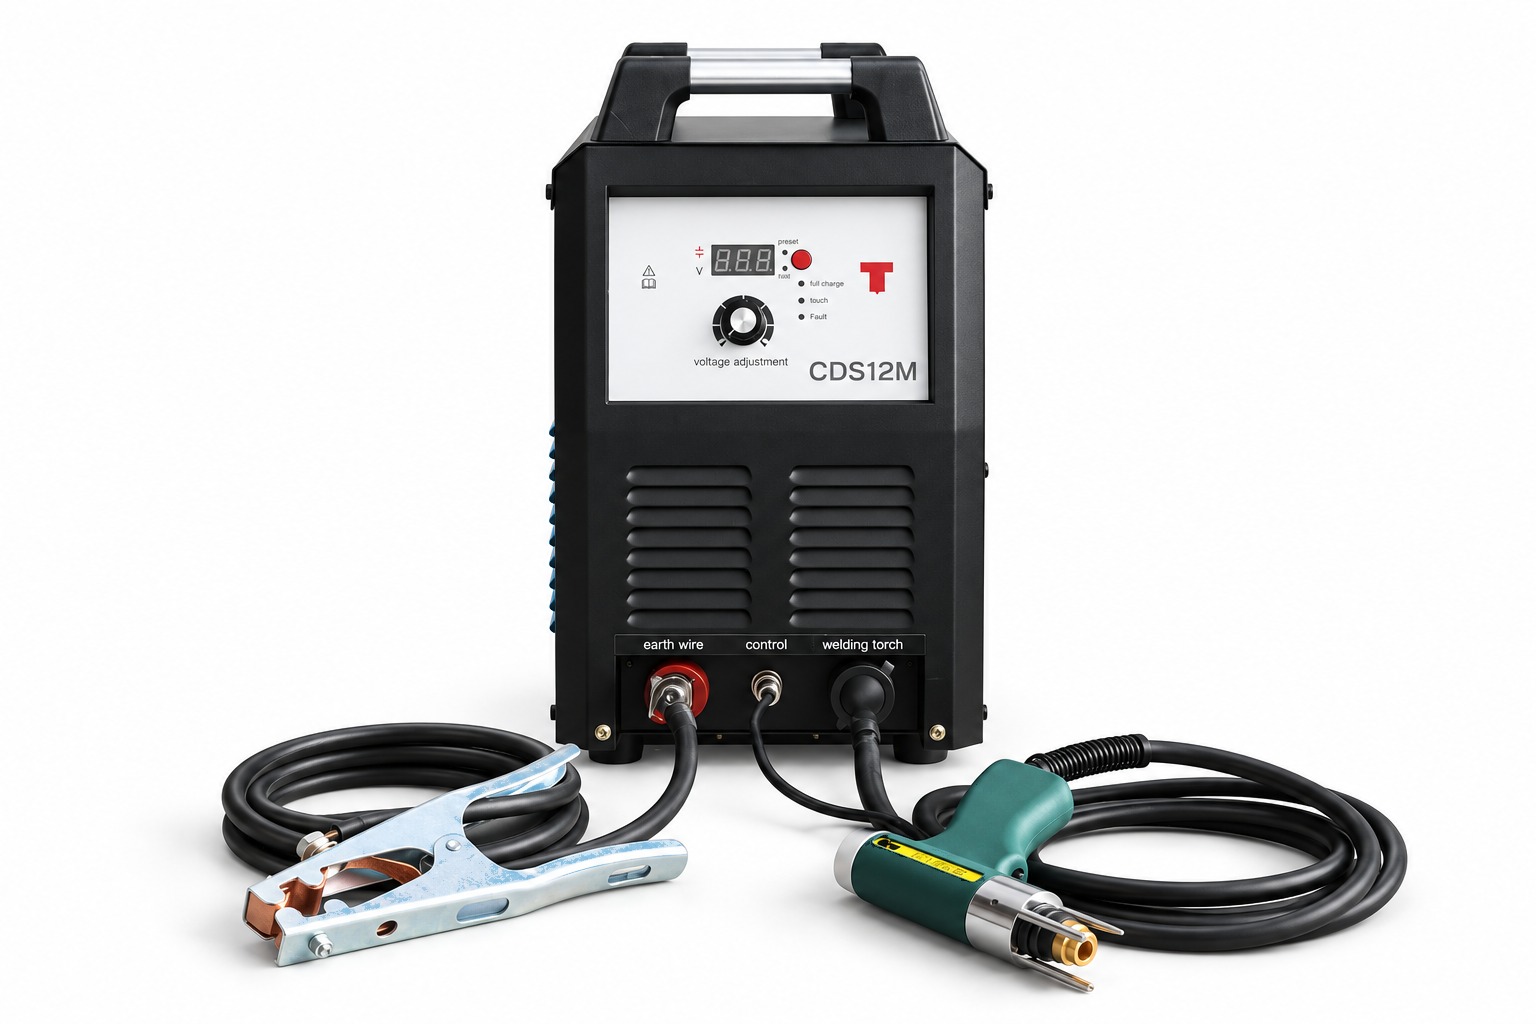
Machine, CSQ12 Gun, Earth Clamp, Five Chuck Sets — Ready on Day One
Voltage dial
One knob sets the charging voltage, 35–200 V DC, for every stud size and material.
Preset & status LEDs
Preset, full charge, touch and fault indicators tell the operator exactly where the cycle is.
CSQ12 gun
2.5 kg spring-loaded hand gun with adjustable support legs and interchangeable collets.
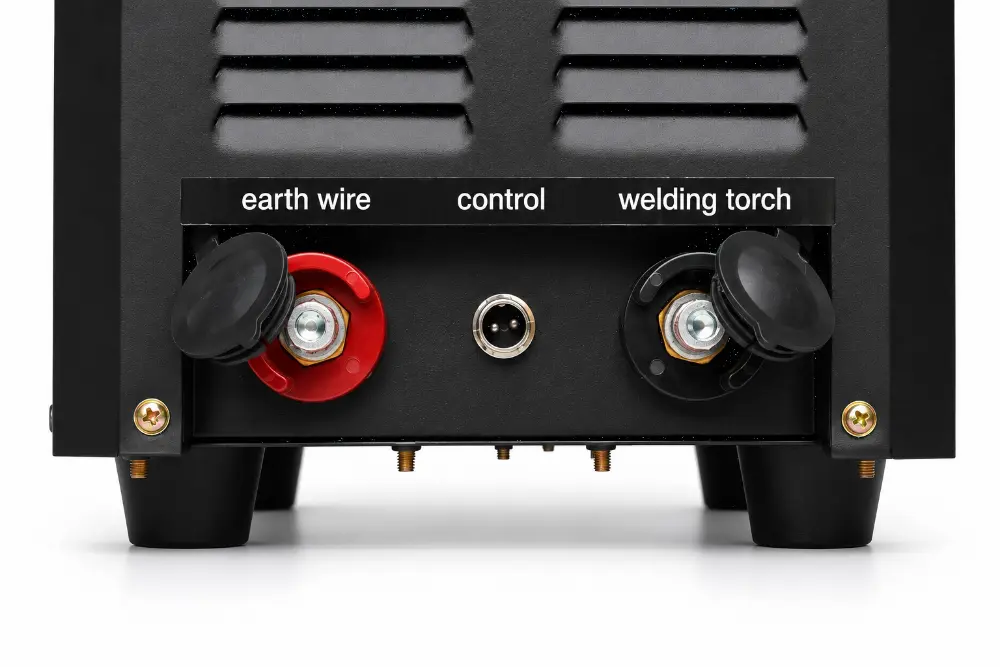
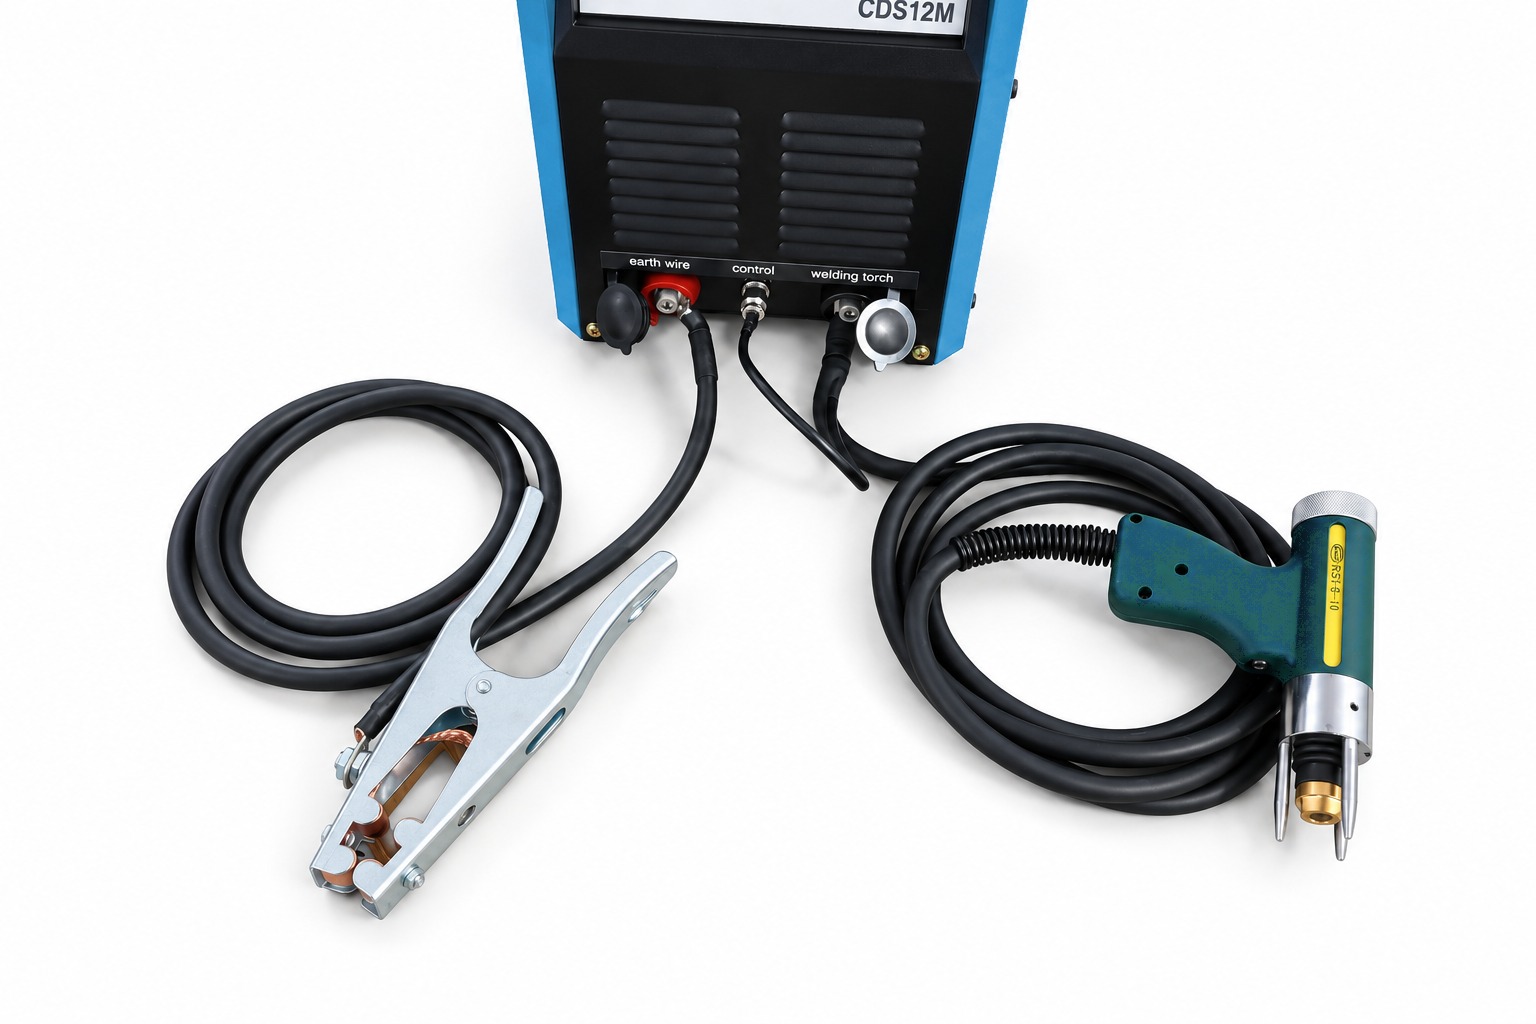
Earth, control, torch
Three front sockets with caps; cables lock in with a quarter turn.
Forced-air cooling
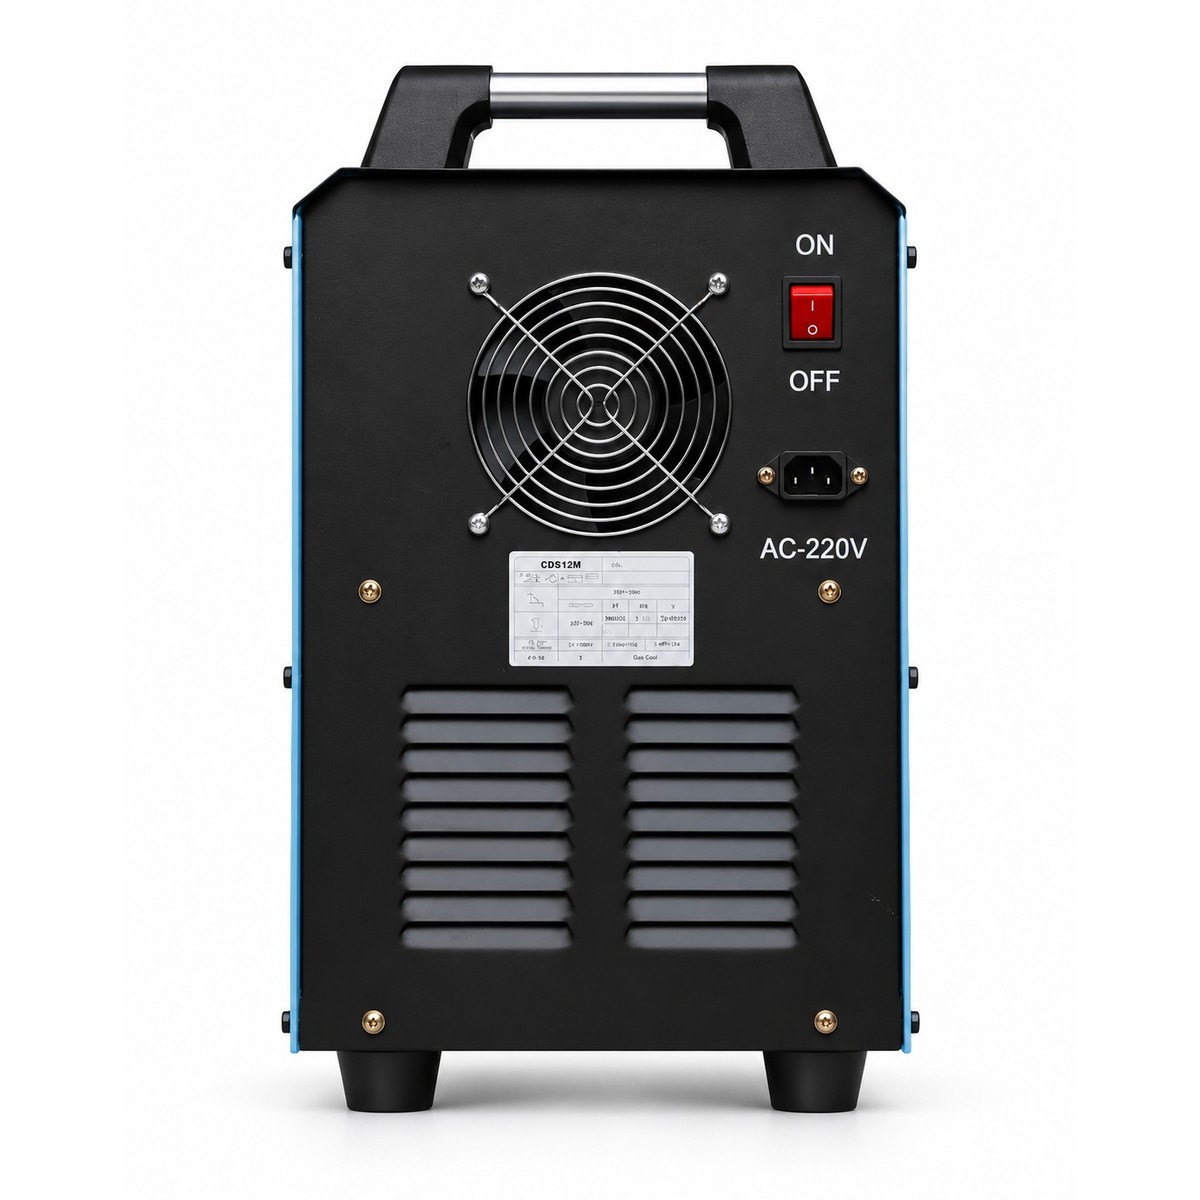
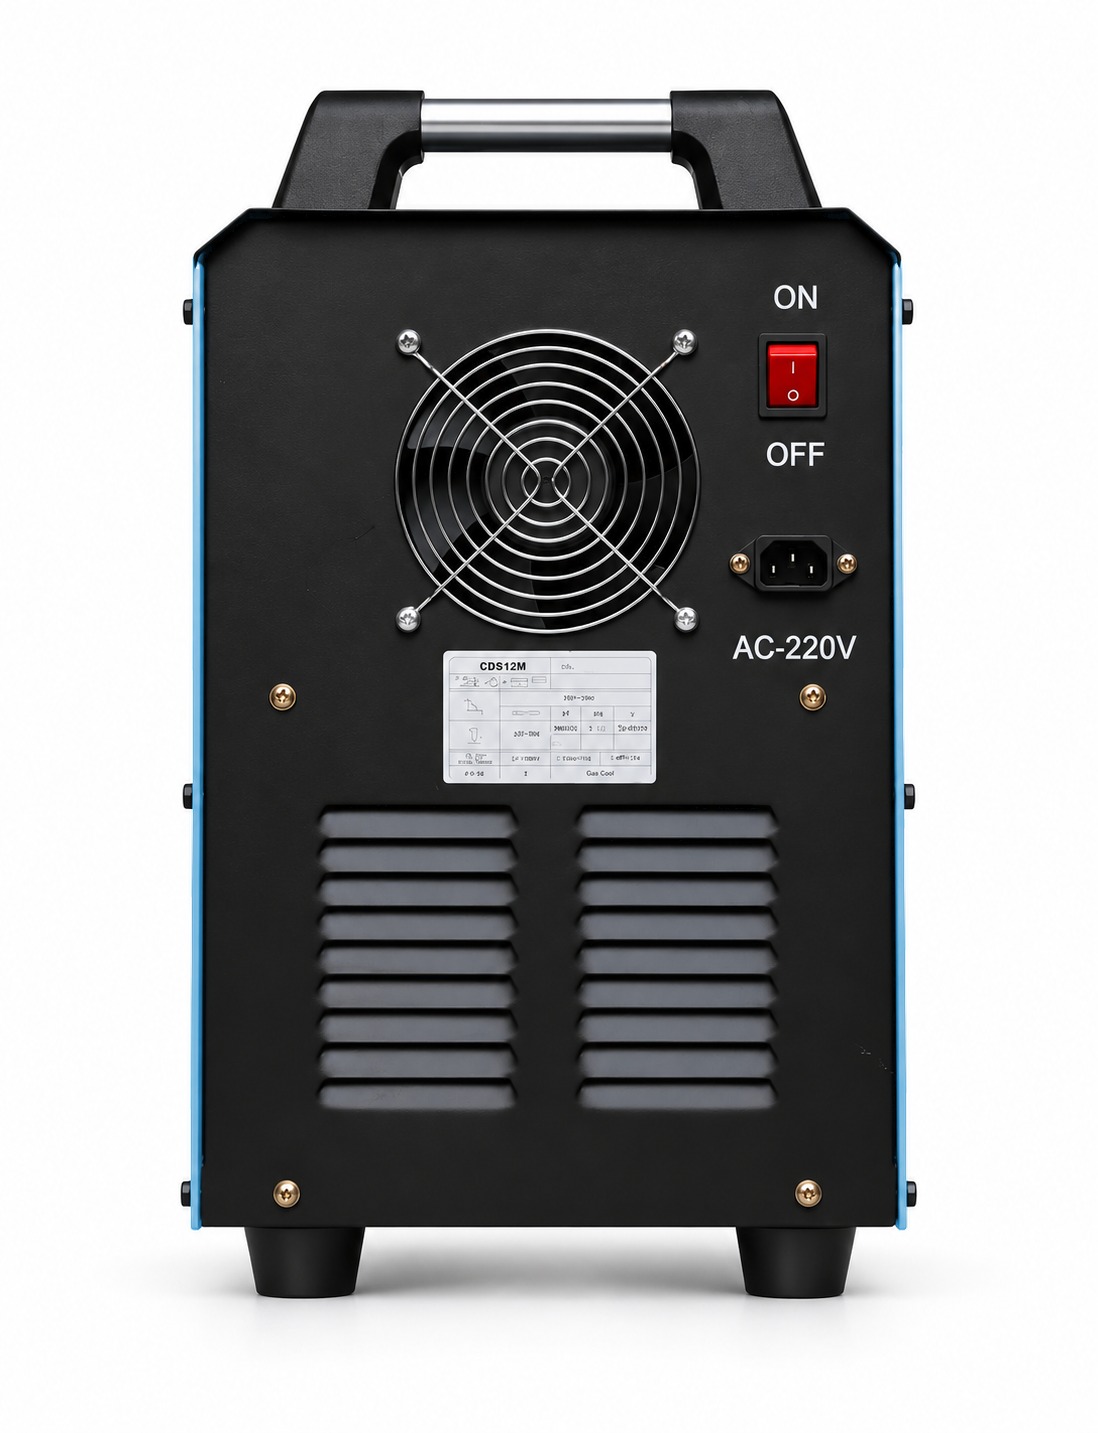
Fan and louvres front and rear; IP23, Class H insulation.
Single-phase inlet
IEC inlet and rocker switch on the rear; 20 A fusing.
Earth, control and torch sockets
Rear: fan, switch, mains inlet
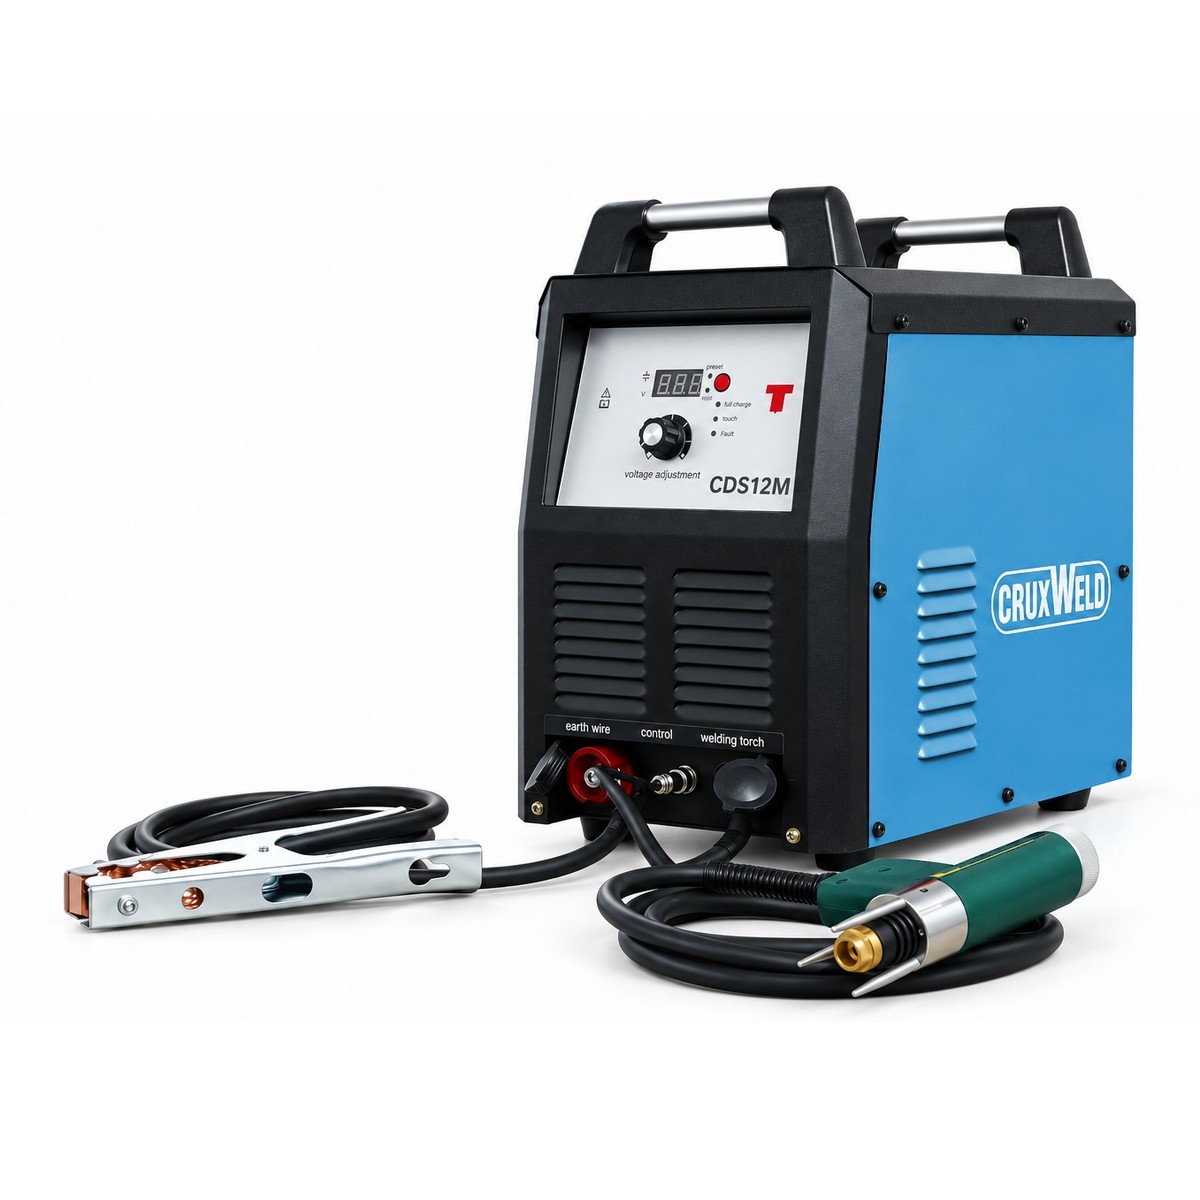
Gun and earth clamp with cables
Standard scope of supply: CDS12M stud welder, CSQ12 stud welding gun with cable, power cable, earth clamp with cable and 5 sets of stud chucks. Optional: additional chucks, extended cables, CD studs, pins and insulation nails.
06
Where it works
Enclosures, Kitchens, Ducting, Signage, Panels and Racks
Built for the production lineThe 180,000 µF bank recharges in under 3 seconds, so an operator can keep welding at up to 40 studs a minute from a 110 V or 220 V single-phase socket.
Electrical enclosures & switchgear
Earth studs, door studs and mounting bosses on painted or galvanised sheet.
Commercial kitchens & stainless
Blind fixings on polished stainless with no mark on the show face.
HVAC & insulation
Insulation pins and nails on ducting, pipes and panels.
Signage & architectural metal
Fixings on aluminium and brass letters, cladding and facades.
Automotive & appliances
Trim, bracket and earth studs on body panels and white-goods cabinets.
Electronics & racks
PCB stand-offs and tapped bosses on chassis and 19-inch racks.
Specifications from the CRUXWELD CDS12M datasheet; subject to improvement without notice. The quotation and test certificate supplied with the machine are the governing documents. Warranty terms are stated on the quotation / invoice.
A capacitor discharge (CD) stud welding machine stores energy in a capacitor bank and releases it in a few milliseconds to weld a stud, pin or boss onto sheet metal. The weld is complete before heat can pass through the sheet, so the reverse side stays unmarked. The CDS12M stores 3500 J and welds M3 to M12 studs.
What is the difference between the CDS10M and the CDS12M?
The CDS10M (2500 J) welds M3–M10 at 10–25 studs per minute. The CDS12M (3500 J) welds M3–M12 at up to 40 studs per minute. Choose the CDS12M for M12 studs or for production-line speed.
Which materials can the CDS12M weld?
Mild steel, stainless steel, aluminium and brass studs onto sheet of the same family. Aluminium and brass need the correct CD stud with ignition tip and a clean, oxide-free surface.
Does it need gas or flux?
No. CD stud welding uses the stud’s own ignition tip and the stored capacitor energy — there is no shielding gas, flux or ferrule to buy.
What power supply does the CD stud welding machine need?
A standard 110 V or 220 V, 50/60 Hz single-phase socket. Rated power is 500 W with an input capacity under 0.8 kW and 20 A fusing, so no three-phase connection is required.
How fast can it weld?
The capacitor bank recharges in under 3 seconds and each weld takes 1–3 milliseconds, giving a maximum of 40 studs per minute depending on stud size and handling.
How do I check the weld quality?
Bend the first stud of a batch about 30° with a tube or hit it sideways with a hammer. A correct setting bends the stud without cracking the weld. If the weld breaks, raise or lower the voltage one step and test again.
What is supplied with the machine?
The CDS12M stud welder, CSQ12 stud welding gun, power cable, earth clamp and 5 sets of stud chucks. Chuck sizes for your studs are confirmed on the quotation.
How do I get the price and delivery time?
Request a quote on this page or message +91 88008 82983 on WhatsApp with your stud sizes, material and monthly quantity. You will receive a GST quotation with delivery time, usually the same working day.
Tell us your stud sizes and material — we will confirm the chucks and quote today.