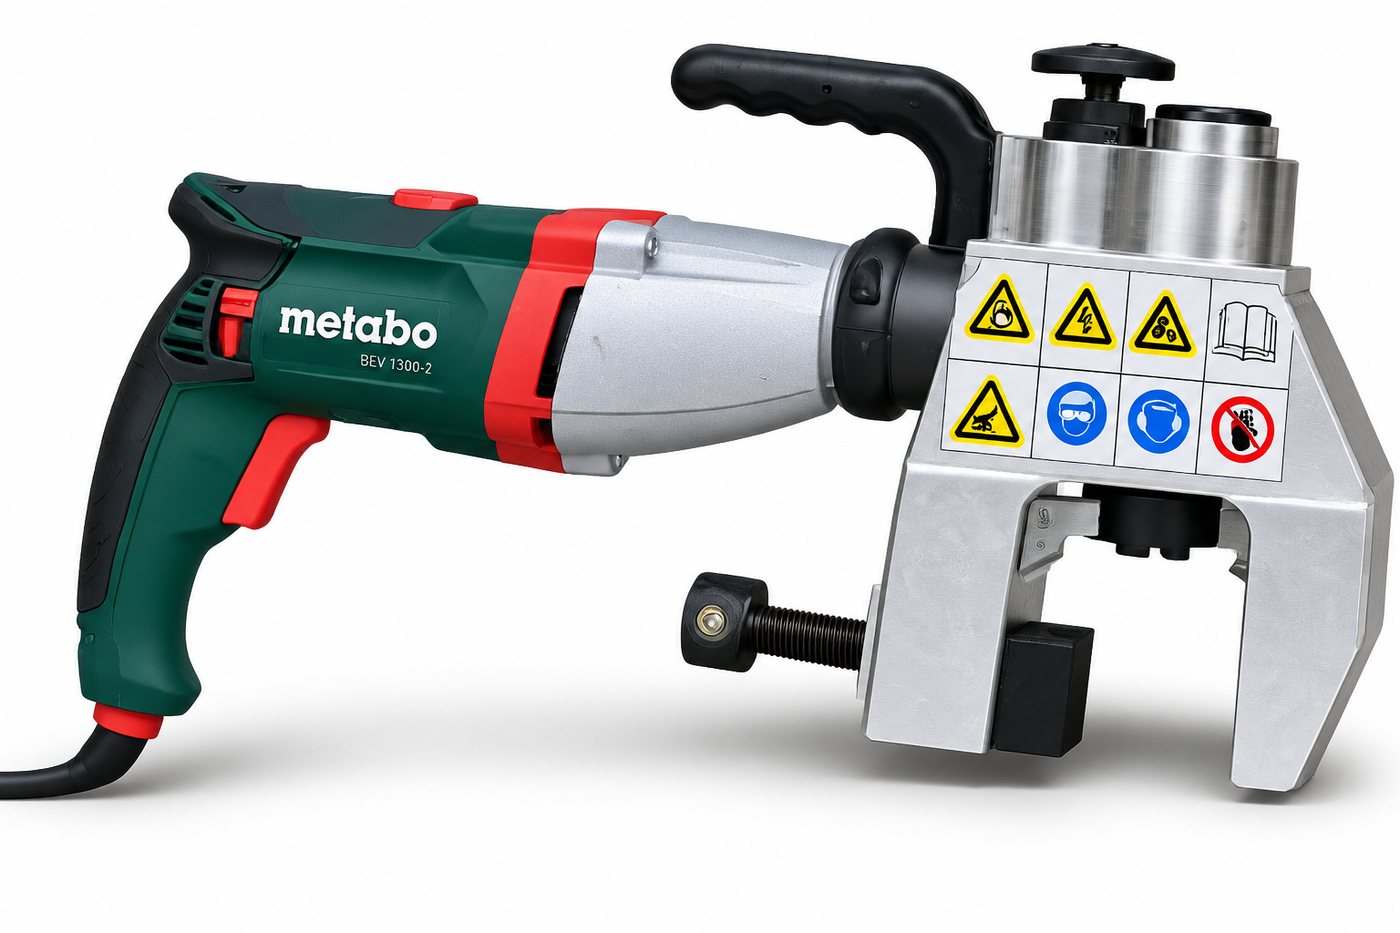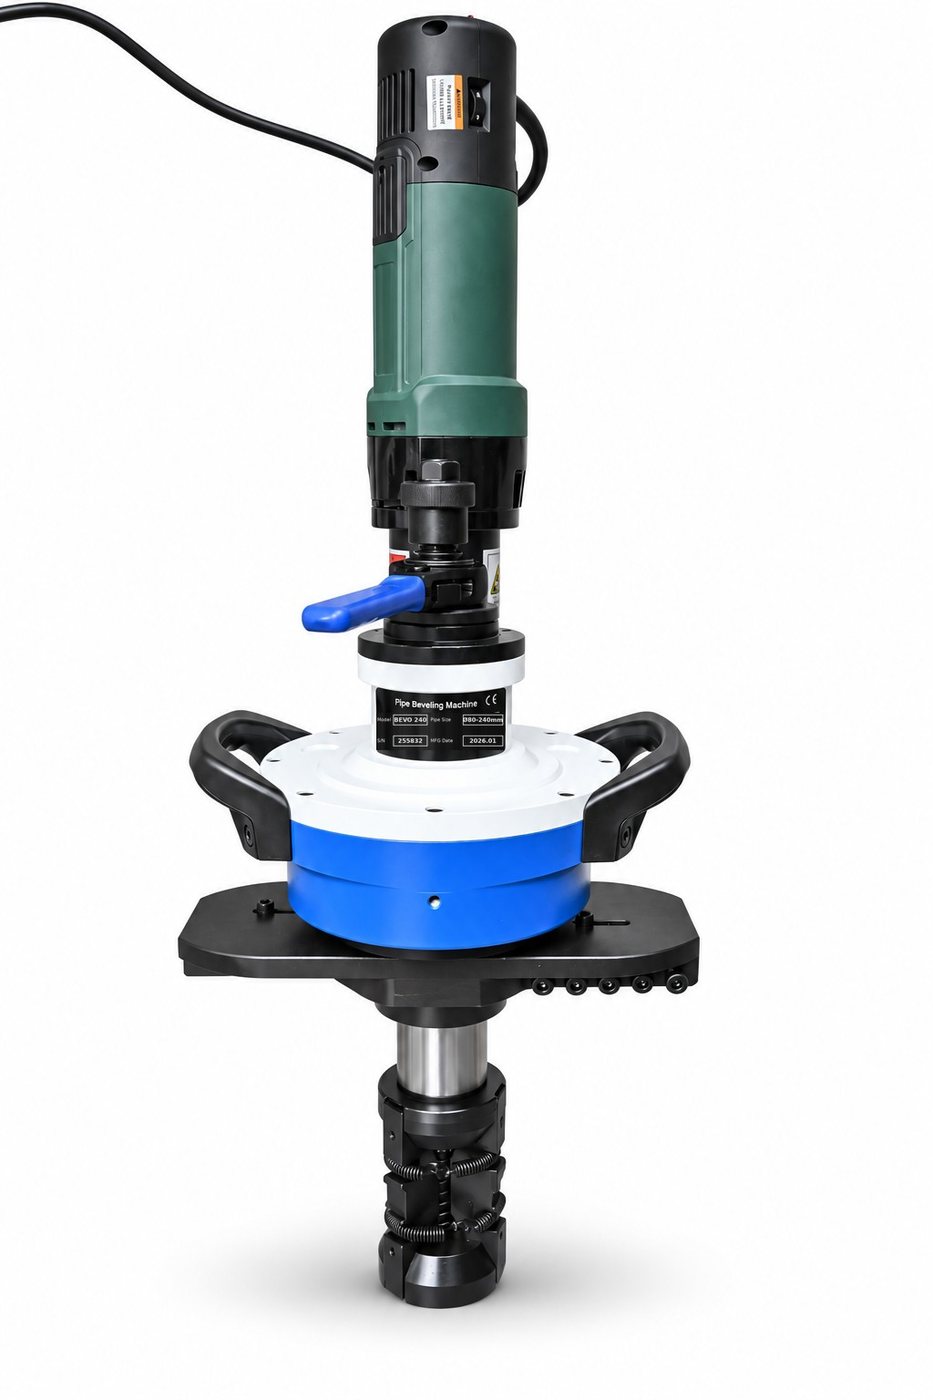
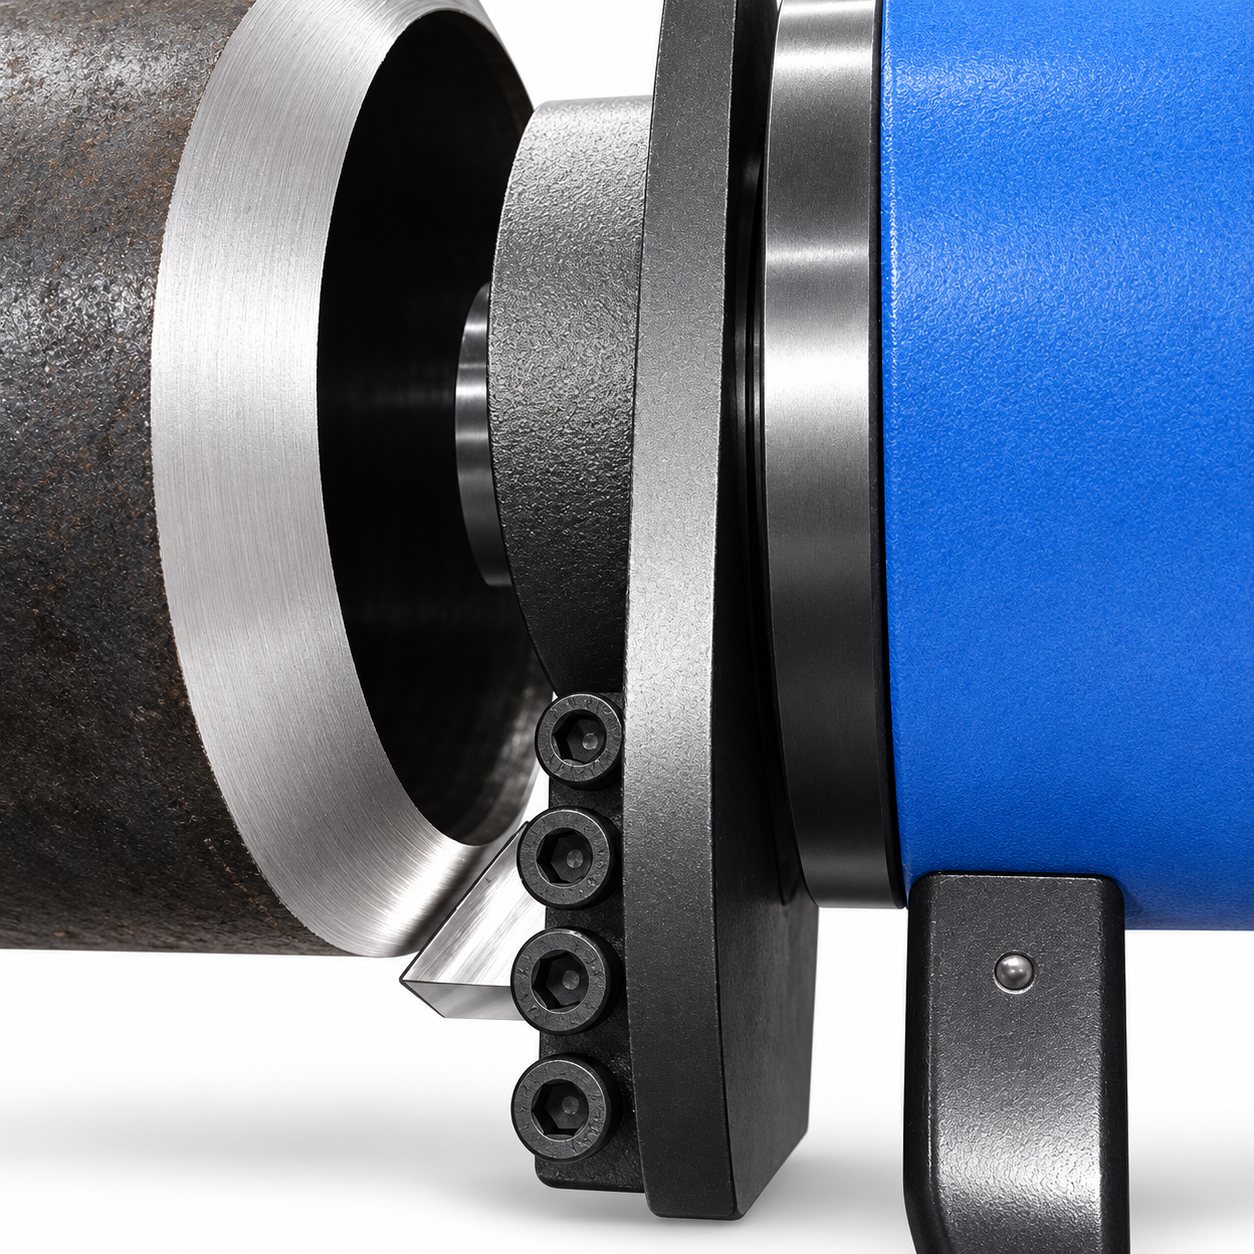
The CRUXWELD BEVO 240 is a portable ID mounted pipe beveling machine for pipe with an inside diameter of 80 to 240 mm and walls up to 20 mm. An expanding mandrel locks it inside the bore and centres it on the pipe, an 1800 W motor turns the tool head at a slow, steady 16 r/min, and the feed handwheel takes the tool bit into the pipe end. The result is a cold, machined 0°, 30° or 37.5° end prep, square to the pipe and ready for the root pass.
GeM Registered OEM Manufacturer · Supported Worldwide · 45+ years of welding expertise
Price, delivery & technical help — get a fast response.
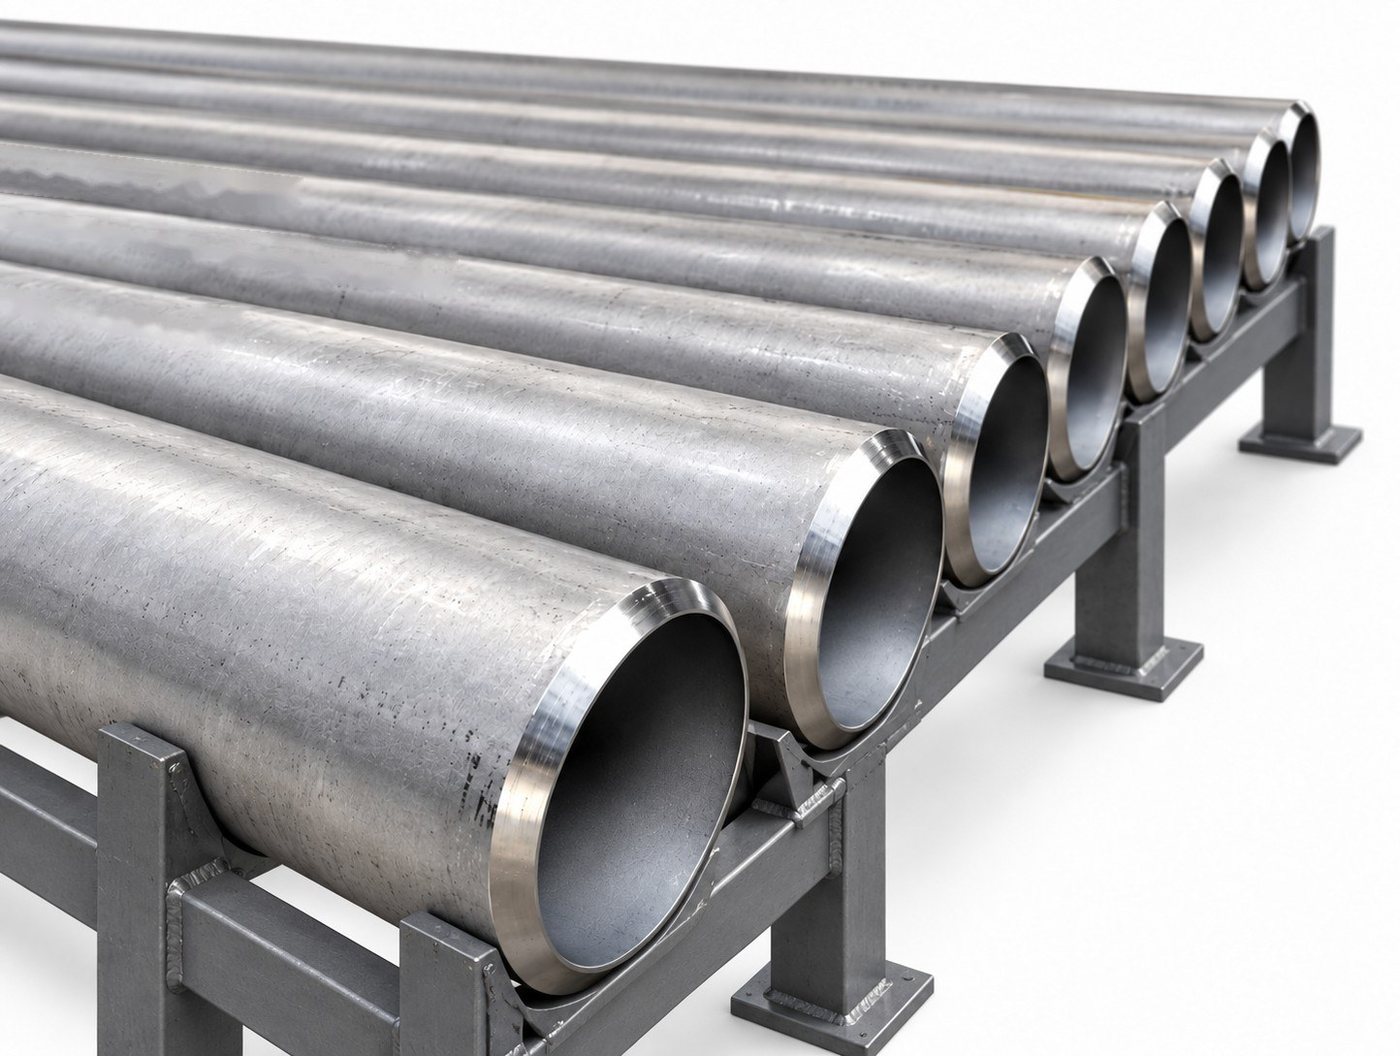
A good butt weld on pipe starts with an end prep that is square to the pipe, at the right angle, with an even root face. A grinder cannot hold that all the way round, and a gas-cut bevel needs grinding back to clean metal.
The BEVO 240 ID mounted pipe beveling machine machines the end instead. Because it centres on the bore, the bevel runs concentric with the pipe and the outside surface stays free for the tool head.
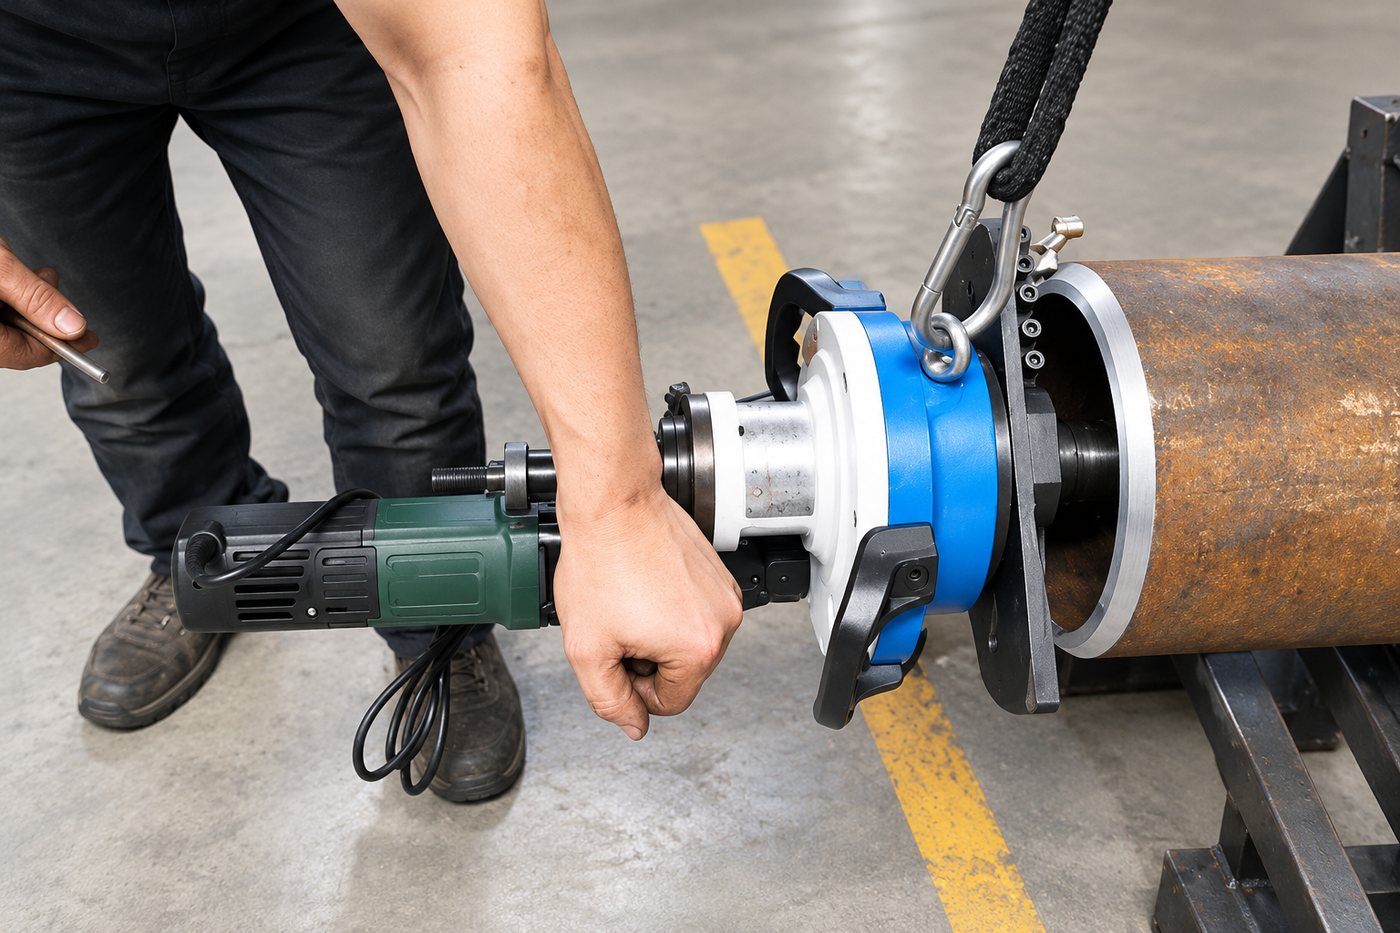
It is made for pipe spool shops, power and process plant maintenance, pipelines and pressure-part fabrication, where pipe from 3″ to 10″ has to be prepared joint after joint. One operator sets the mandrel, fits the tool bit and feeds the cut. For small-bore boiler tubes, see our BEVEX 63 pipe beveling machine.
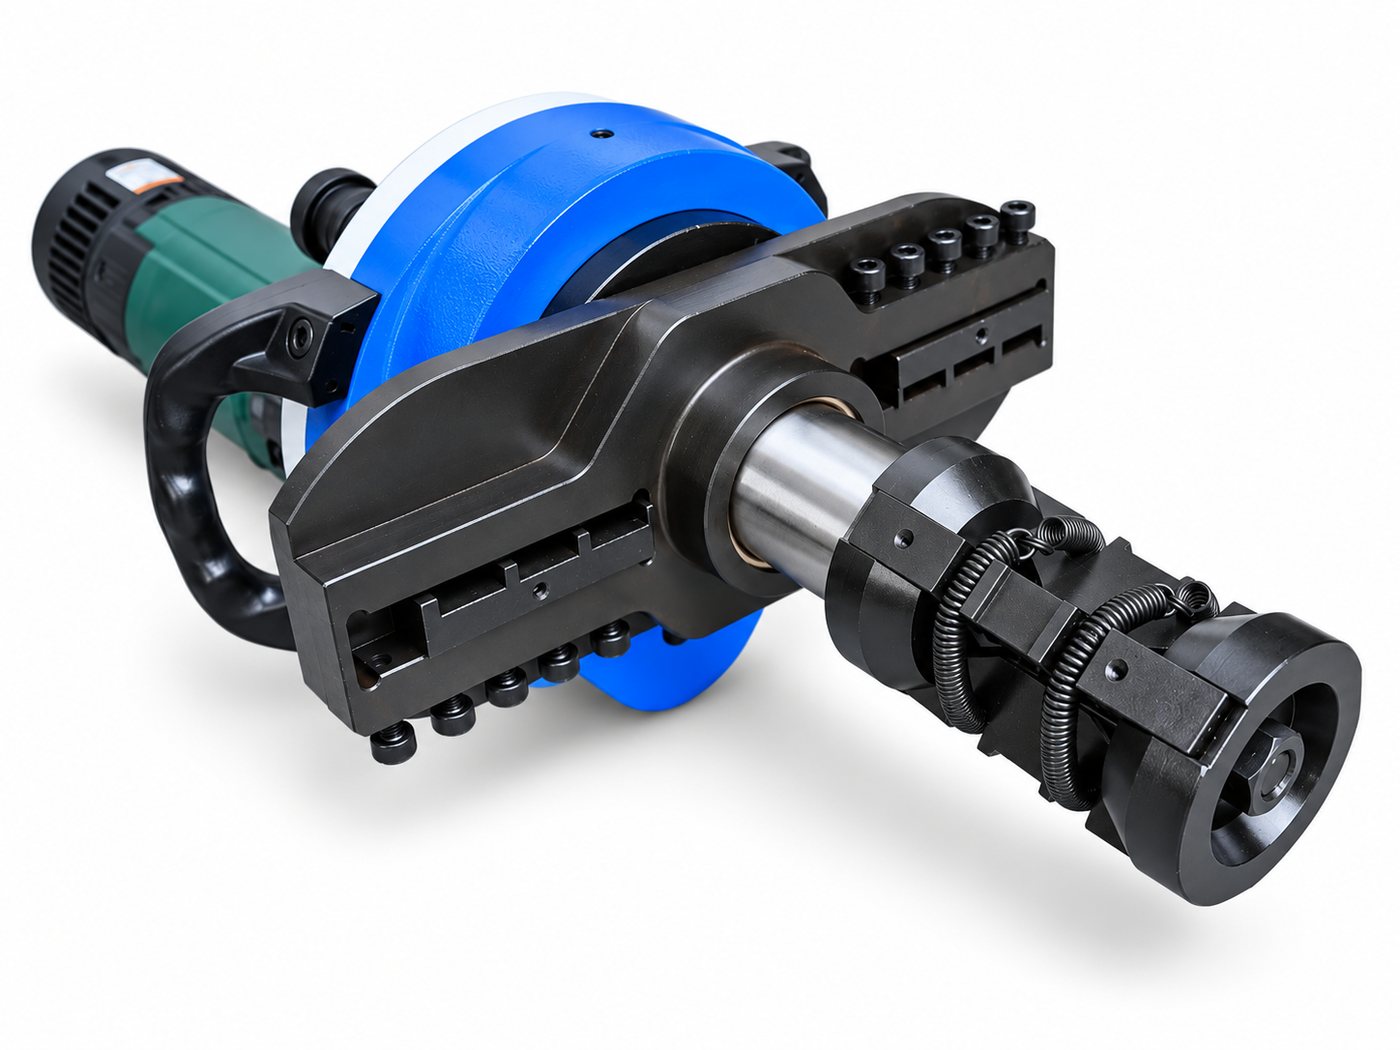
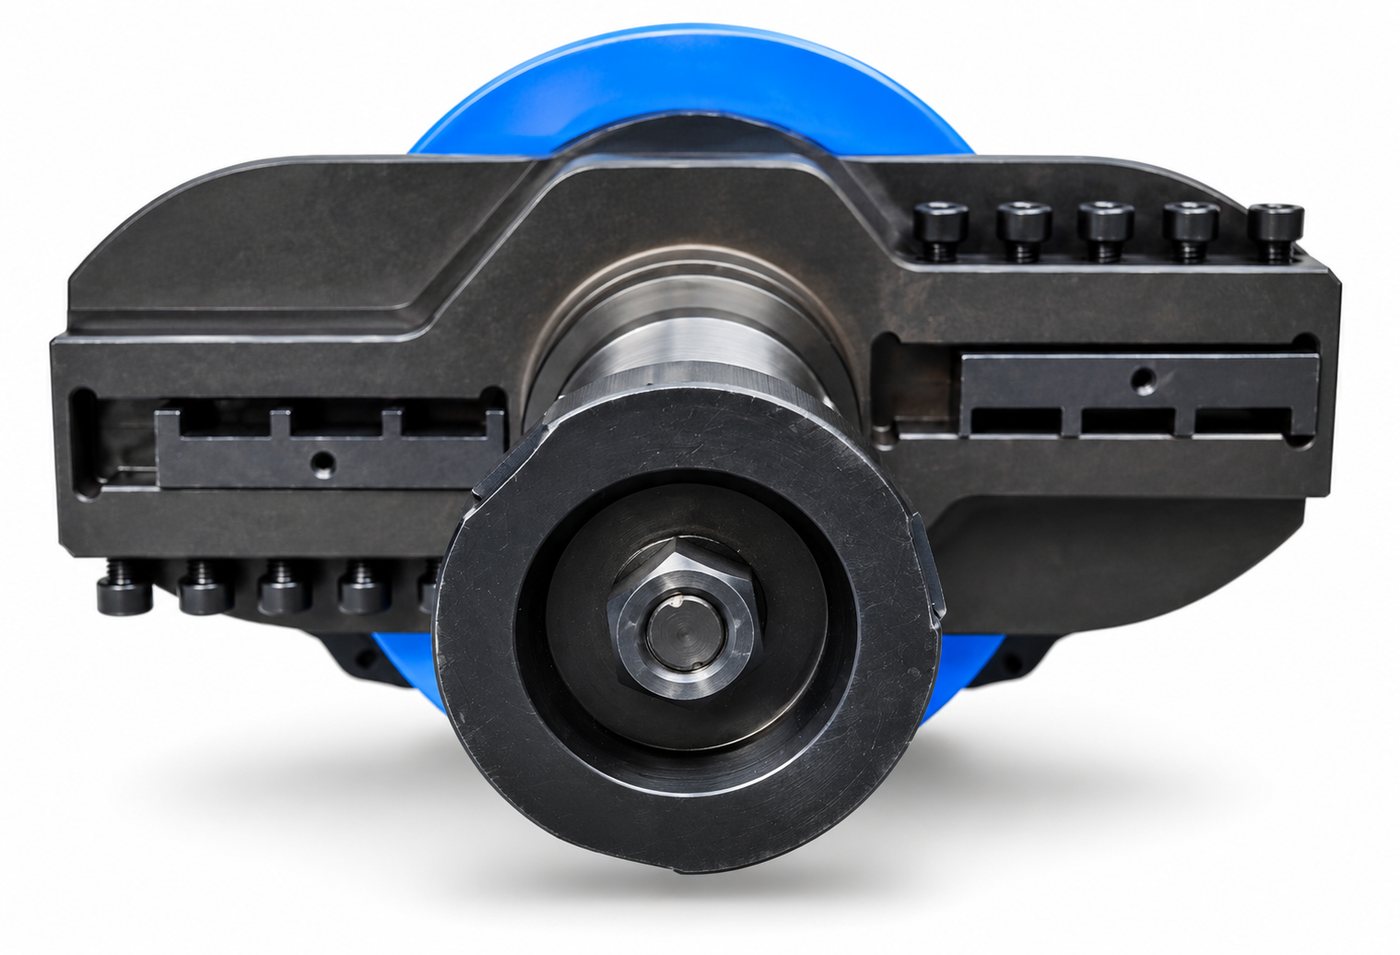
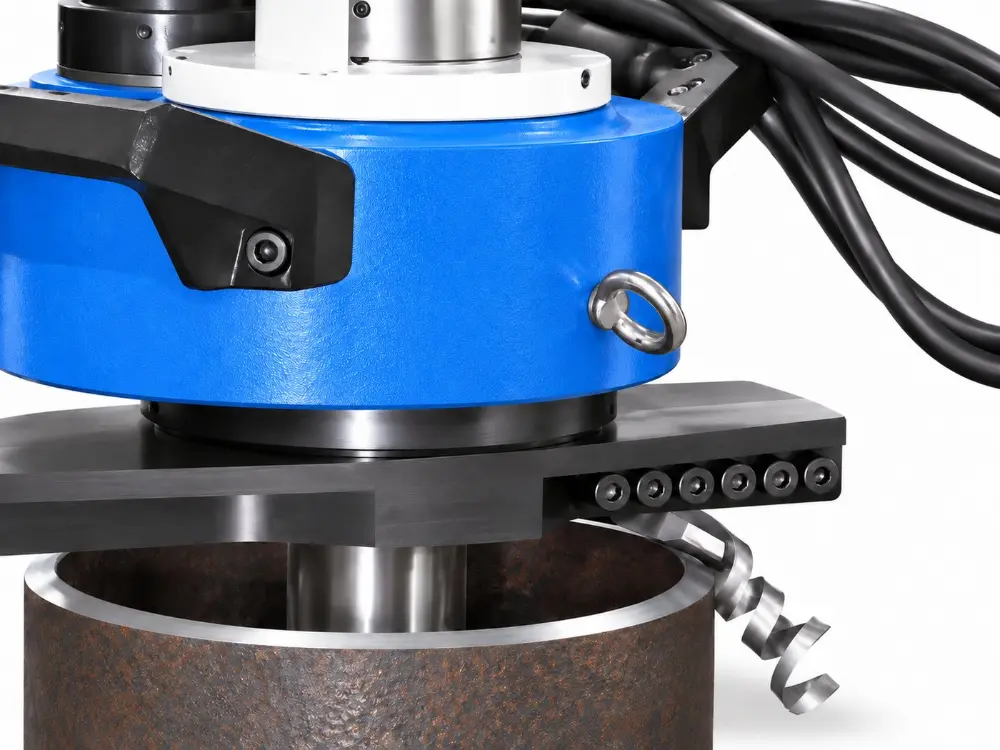
The mandrel slides into the pipe and its expansion jaws are drawn out against the inside wall until the machine is locked and centred on the bore. The tool head then rotates around that centre line, so the bevel and the root face are cut concentric with the pipe, even if the outside surface is out of round or carries coating.
Example bores across the 80–240 mm range: the jaws open to meet the wall.
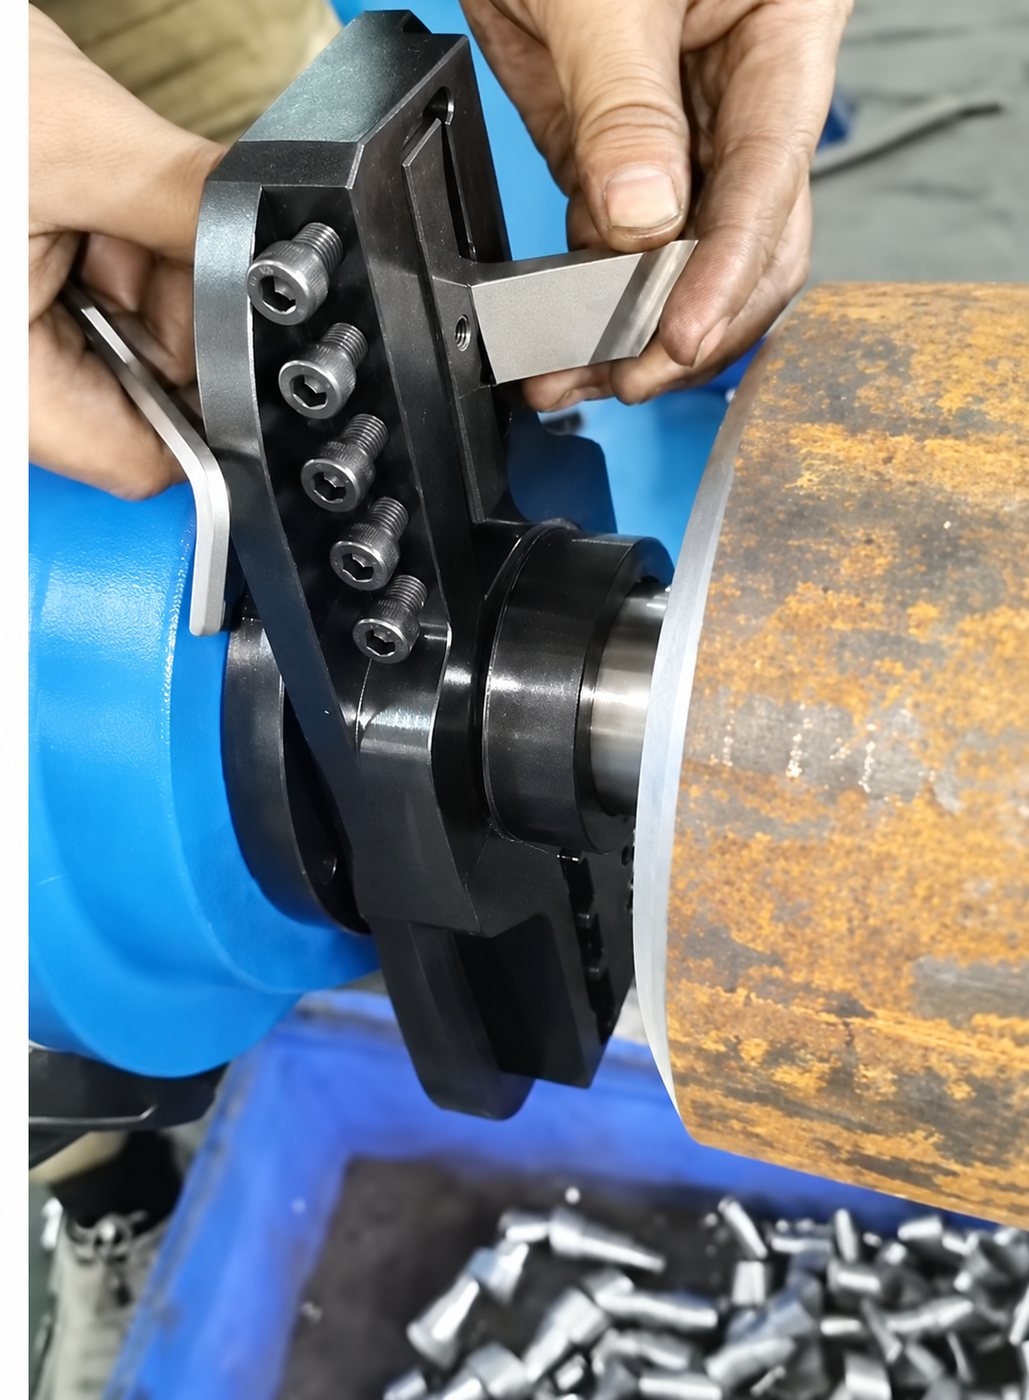
Tap a tool bit to see the end prep it cuts and the groove two ends make when they meet.
Squares the pipe end and cuts the root face (land).
A common bevel for butt welds on many pipe joints.
Two ends at 30° make a 60° groove for the root, fill and cap passes.
The standard pipe weld bevel used on most piping jobs.
Two ends at 37.5° make a 75° groove for the root, fill and cap passes.
Need a different angle, a J-prep or a counterbore? Tell our technical team the joint you need when you enquire.
No grinder bevels
A hand-ground bevel changes with every operator. The BEVO 240 cuts the same angle and root face on every joint.
Fewer root repairs
An even groove and constant root face give the welder a steady gap for a sound root pass.
No heat, no scale
Gas-cut ends leave oxide and a heat-affected edge. A machined bevel is bright metal, ready to weld.
Goes to the pipe
Clamps inside the pipe where it lies (on a rack, in a trench or on site) instead of moving pipe to a lathe.
One machine, 3″–10″
Change the jaw set, not the machine, across the 80–240 mm ID range.
Runs on 220 V
A single-phase 220 V, 50 Hz socket on site or in the shop is all it needs.

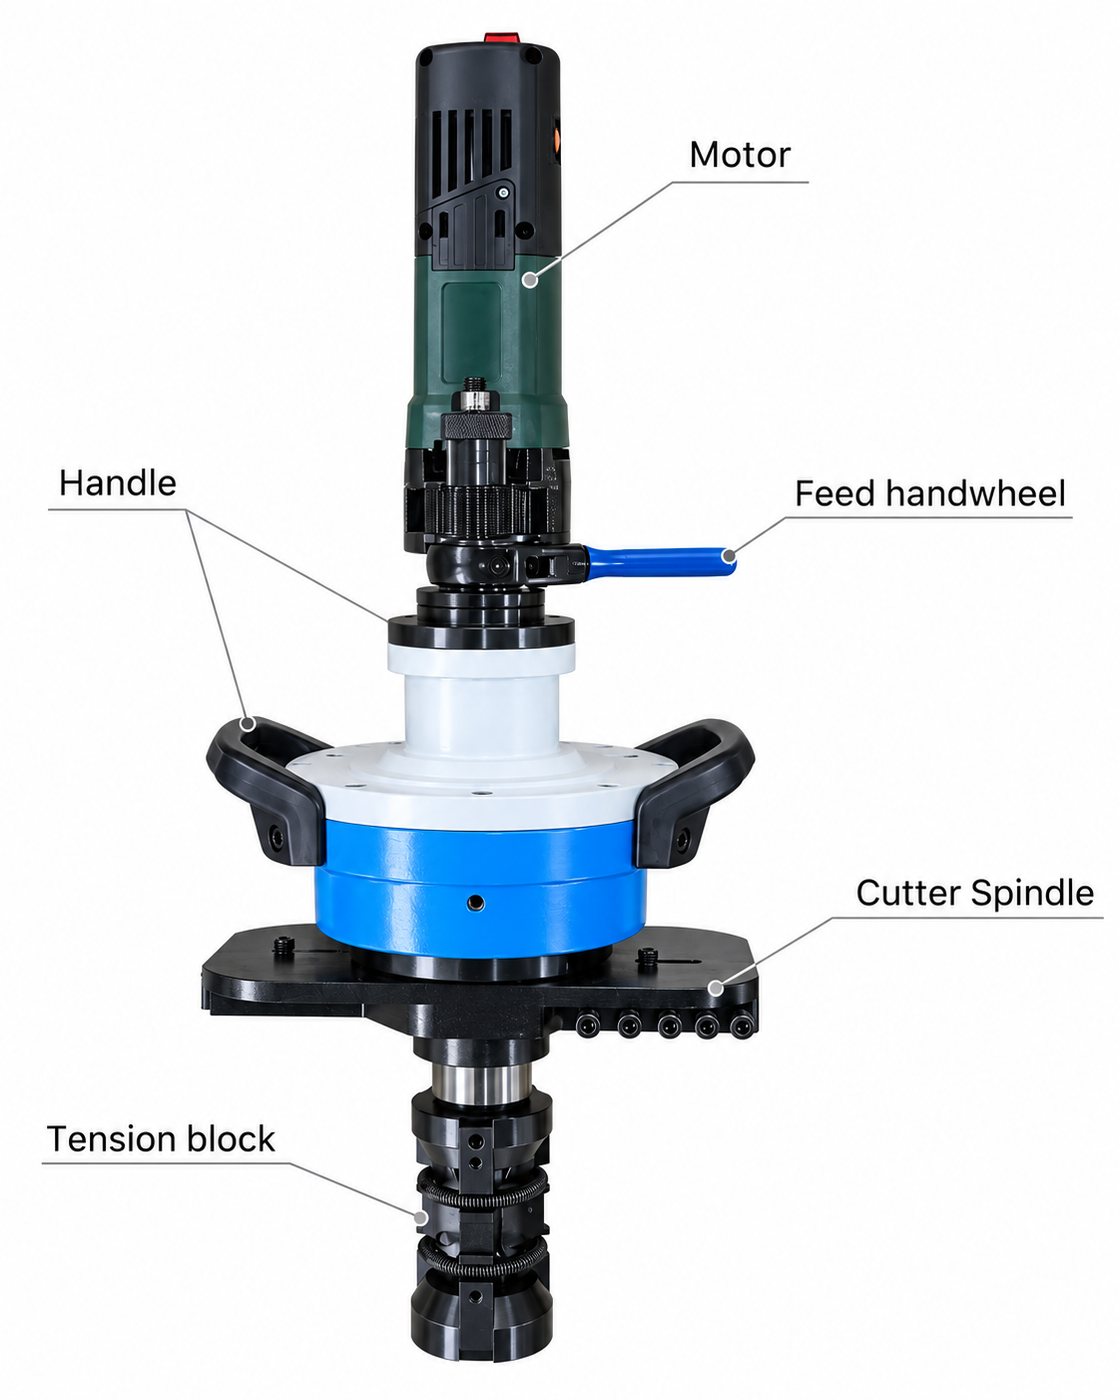
Five parts do the work. The motor on top drives the cutter spindle, the feed handwheel advances the tool bit, the two handles position and steady the machine, and the tension block on the mandrel expands the jaws to lock the machine in the bore.
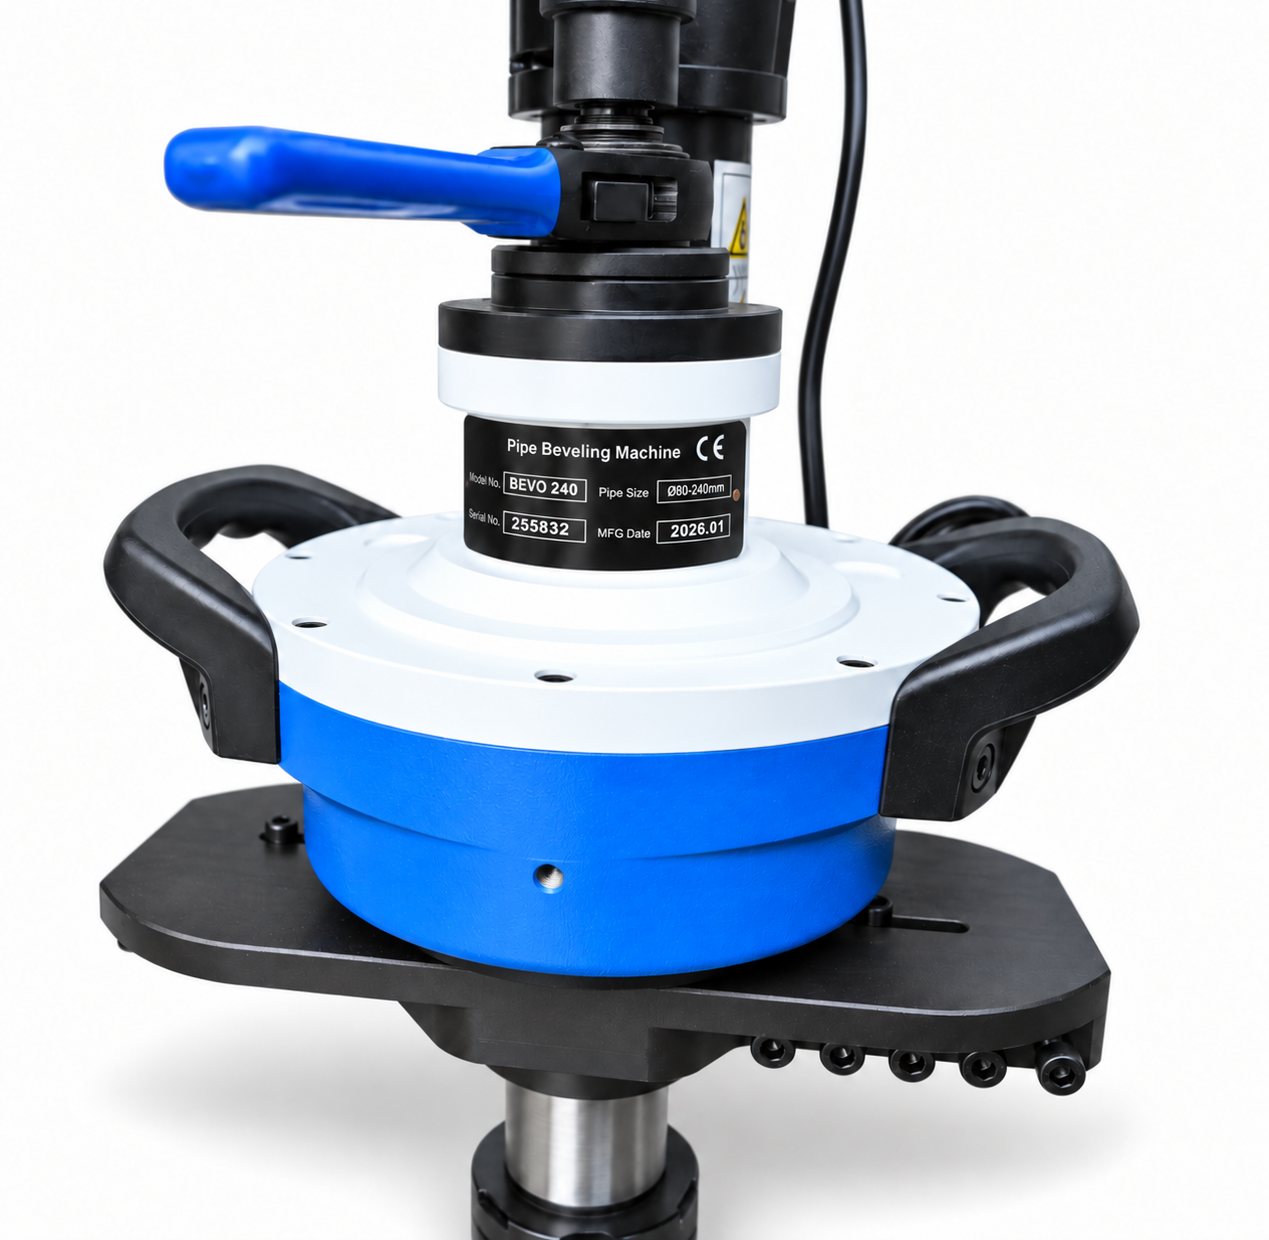
Rigid two-arm tool headCE marked
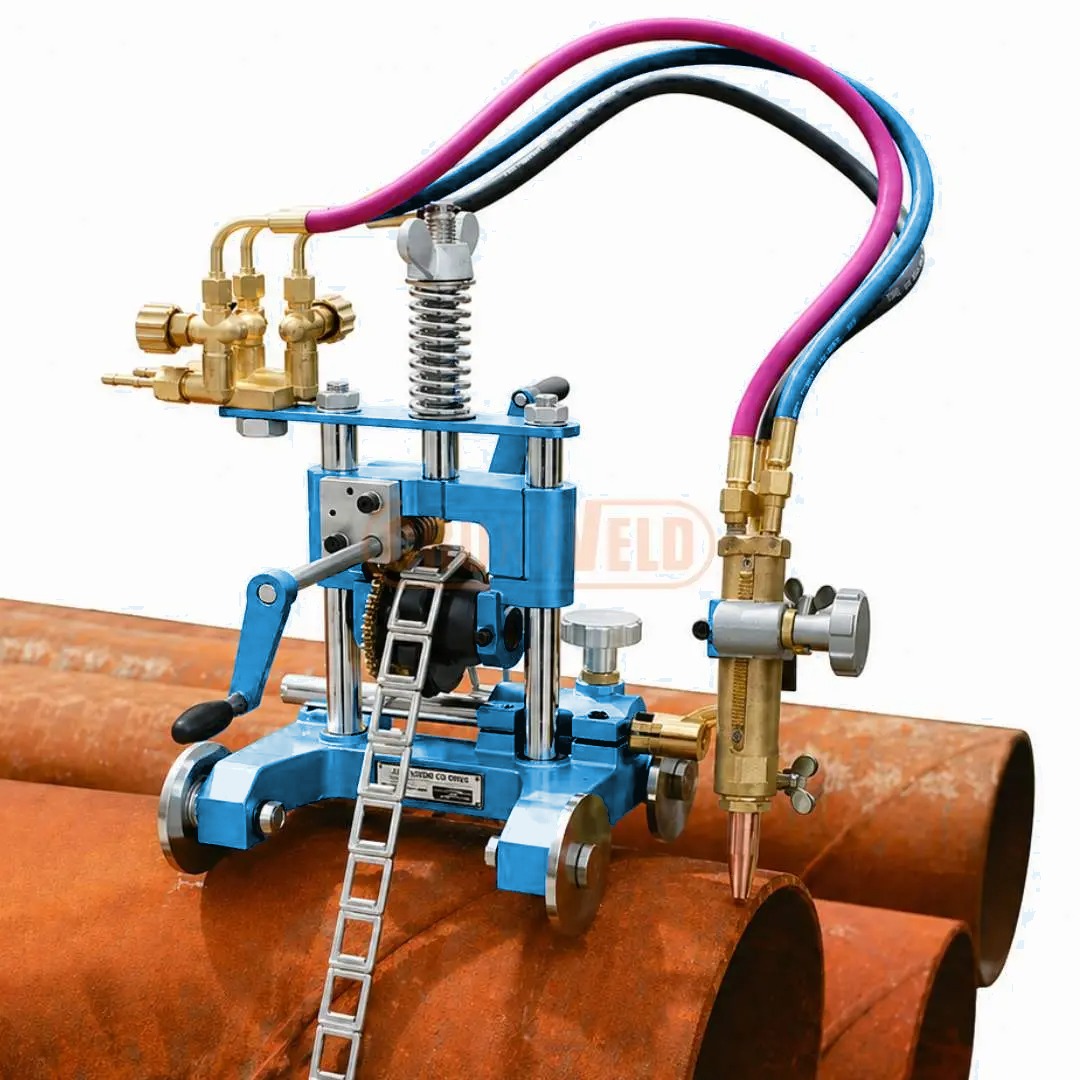
Cutting the pipe before you bevel it? See our portable gas pipe cutting machine and the magnetic pipe cutting machine. For welding the prepared joints, look at the WeldOrbit 360 carriage.
The exact scope is confirmed on the quotation. Ask for spare tool bits and extra jaw sets with your order. See the full range of welding and cutting equipment.
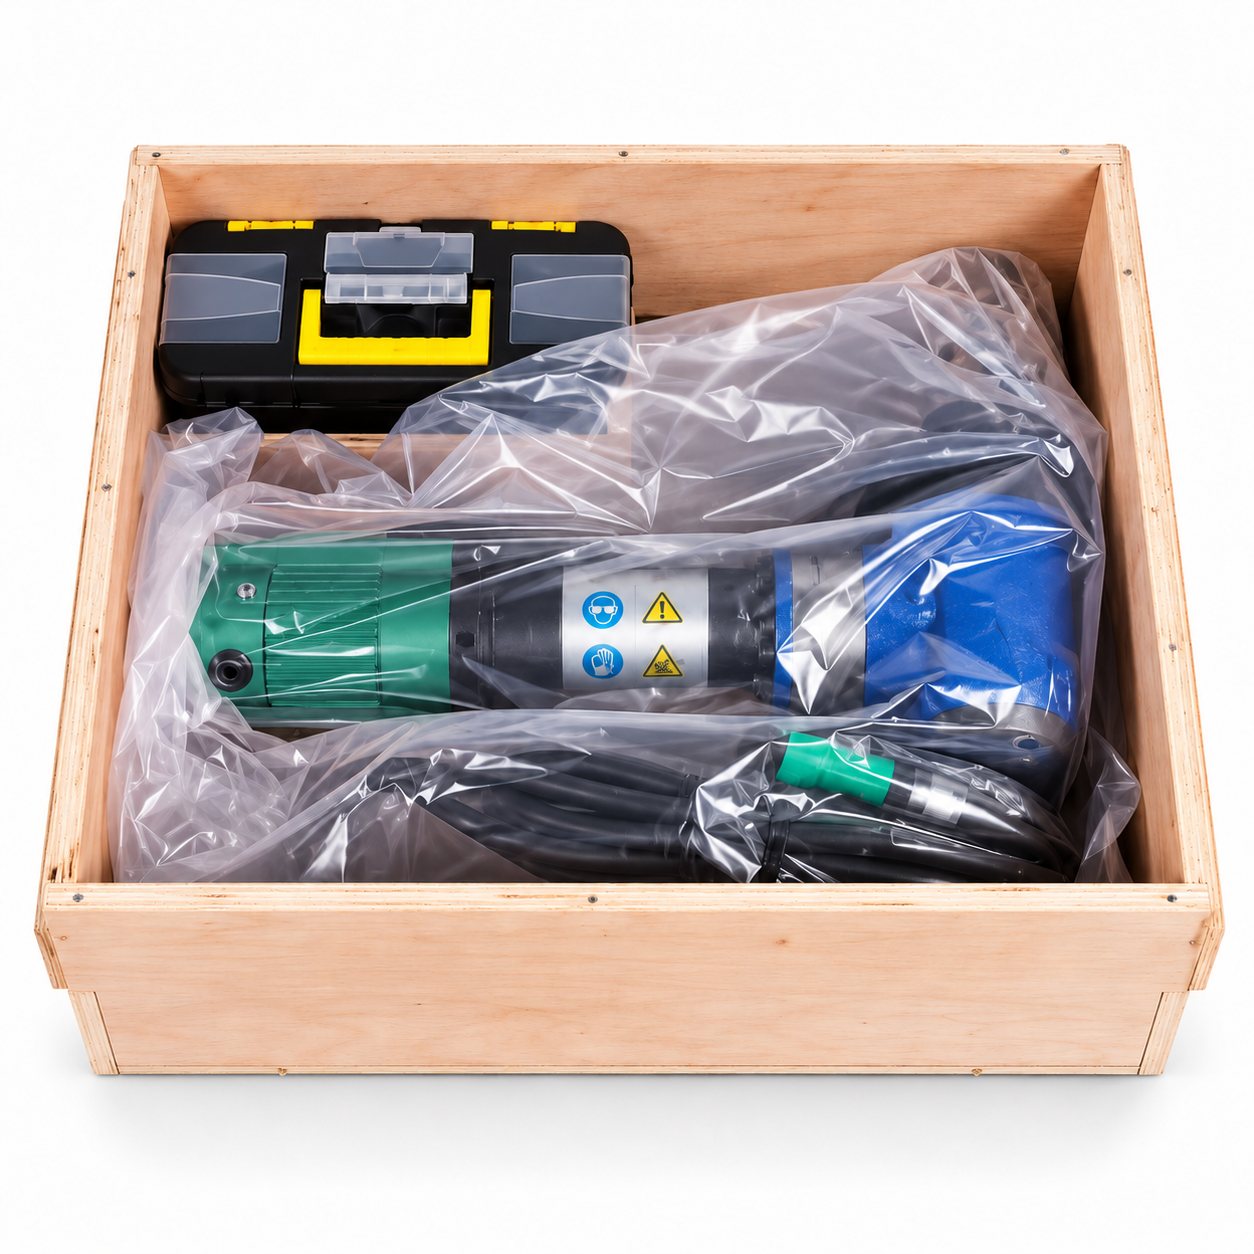
Send us your pipe ID, wall thickness and the bevel you need: we will confirm the jaw sets and send a quotation.