Weld, Anneal and Grind a Bandsaw Blade in One Place. Back on the Saw in Minutes.
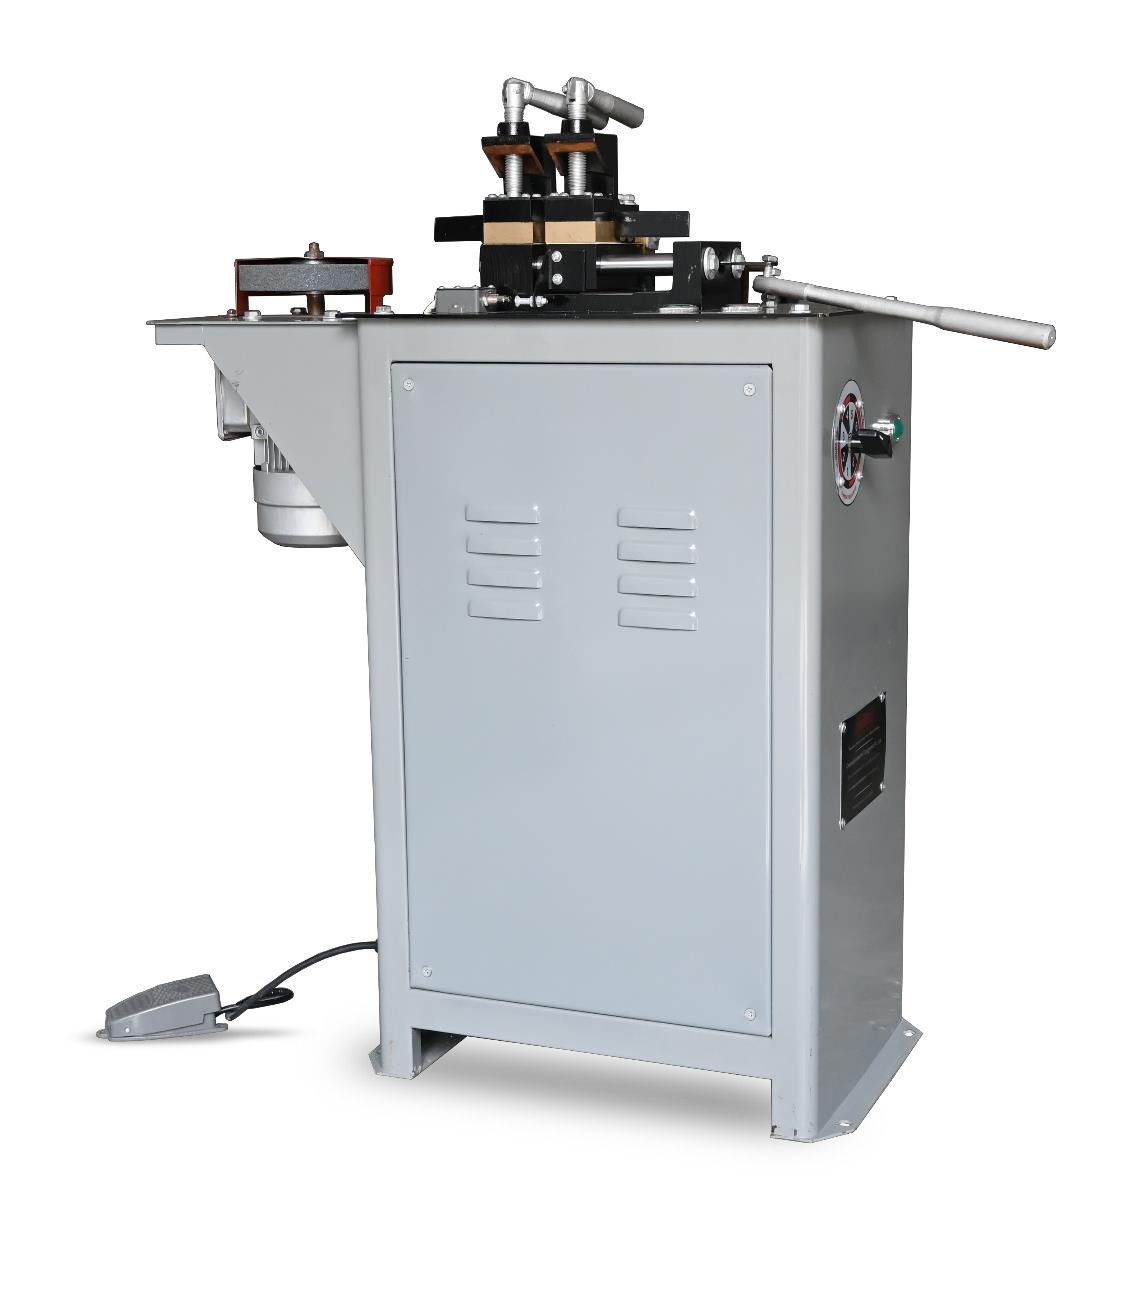
The CRUXWELD UltraFlex 520 is a 12 kVA bandsaw blade butt welder for bimetal and carbon-steel blades from 7 to 52 mm wide and 0.4 to 2.0 mm thick. Dual copper jaw clamps hold the blade ends square, a 6-step secondary voltage matches the heat to the blade, the built-in annealing cycle restores strength and flexibility, and the integrated grinder — worked by foot switch — finishes the seam flush. Table-mounted, 400 V supply.
Bandsaw Blade Butt Welder for Bimetal and Carbon-Steel Blades
A broken or custom-length bandsaw blade should not stop the saw. The UltraFlex 520 bandsaw blade butt welder joins the two blade ends by resistance butt welding: the ends are clamped in dual copper jaws, current flows across the joint, and the upset pressure forges the heated ends together. There is no filler and no flame — the joint is the parent metal itself.
What makes a blade weld last is what happens next. The UltraFlex 520 anneals the weld zone in the same clamps, so the hard, brittle weld becomes tough and flexible again and the blade is ready to run immediately. The seam is then ground flush on the built-in wheel. Three operations, one machine, one operator — for sawmills, metal-cutting shops, blade distributors and maintenance departments.
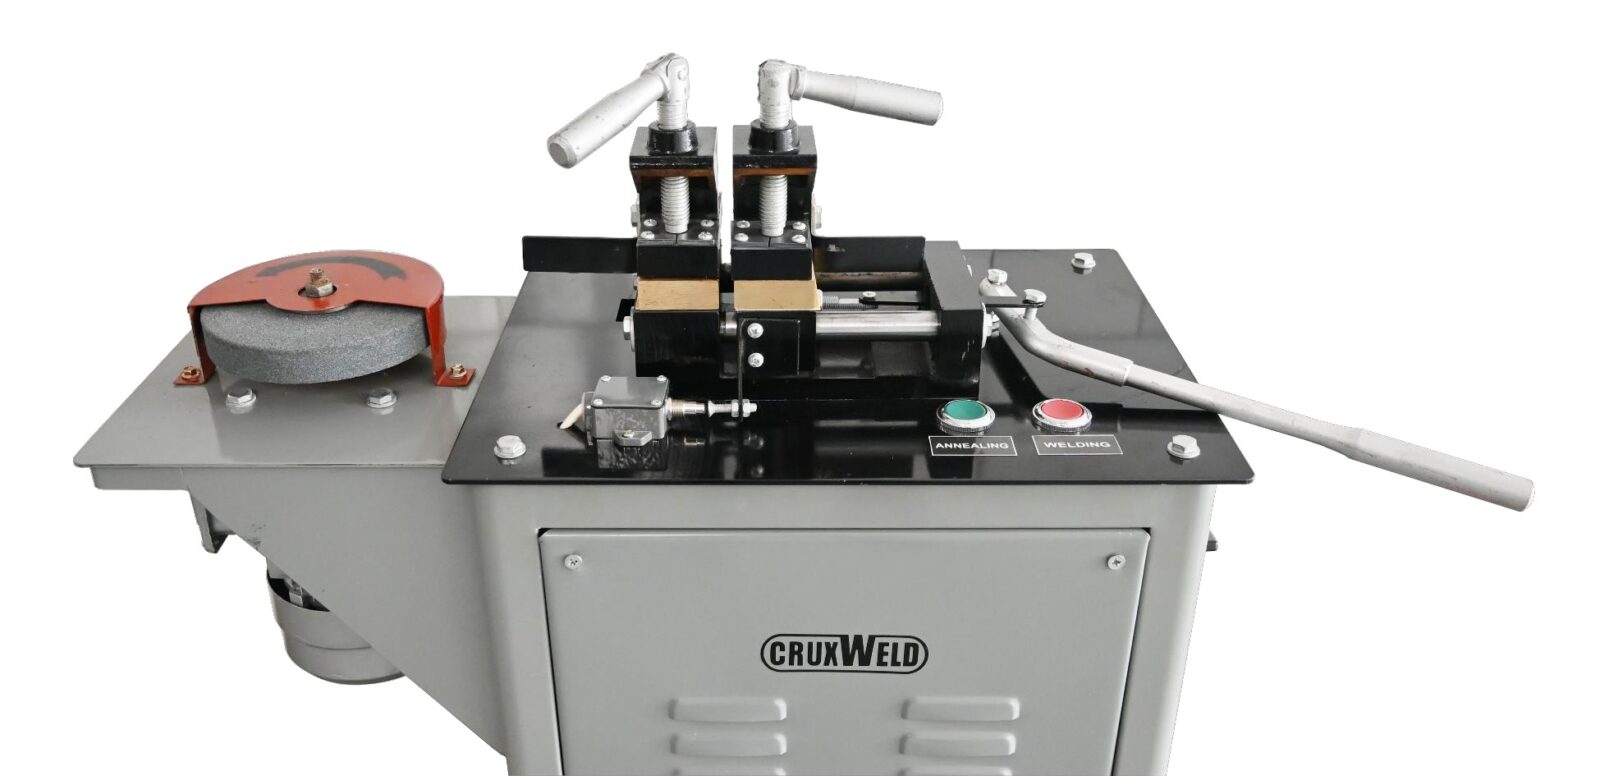
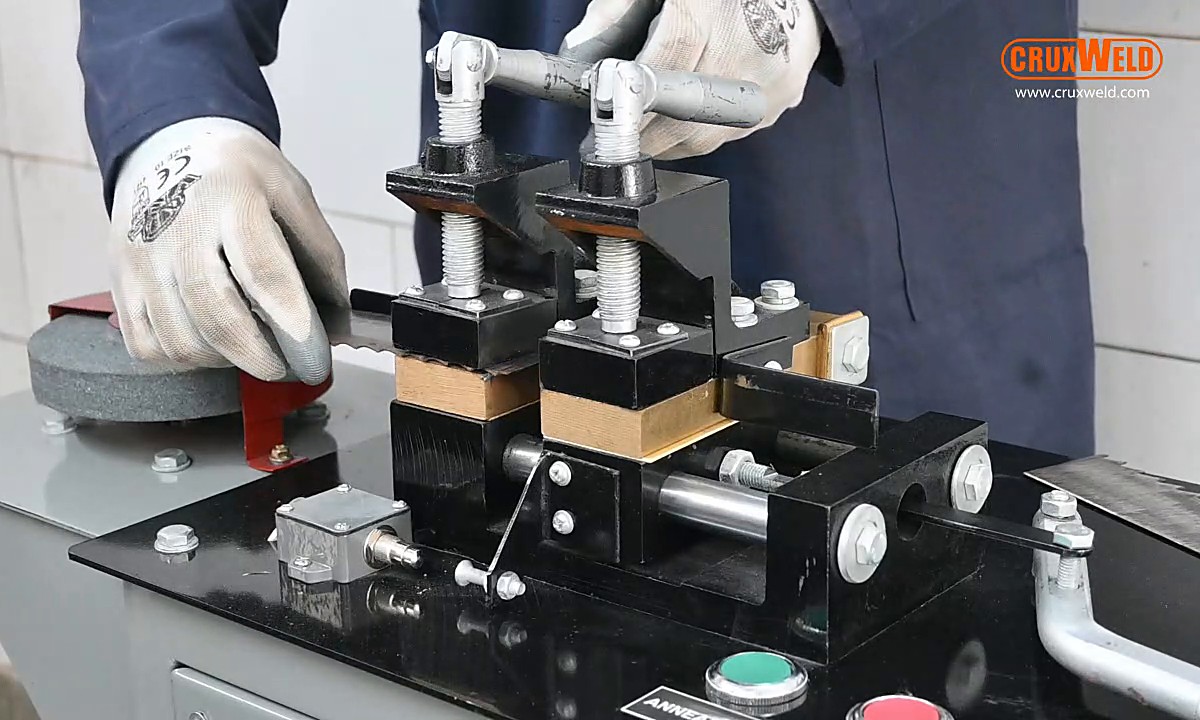
Dual copper jaws, Anneal / Weld buttons and the built-in grinding wheel.
01
Up to 52 mm wide
Bimetal and carbon-steel blades 7–52 mm wide, 0.4–2.0 mm thick — from small shop saws to production band saws.
02
Annealing built in
A controlled annealing cycle restores strength and elasticity; the blade goes straight back on the saw.
03
Hands-free grinding
Foot-switch operated grinder finishes the weld seam flush without taking the blade to another station.
04
Dual copper jaws
High-conductivity clamps hold the ends square and carry the welding current evenly for a uniform joint.
Blade ends squared and clamped in the dual copper jaws.
2
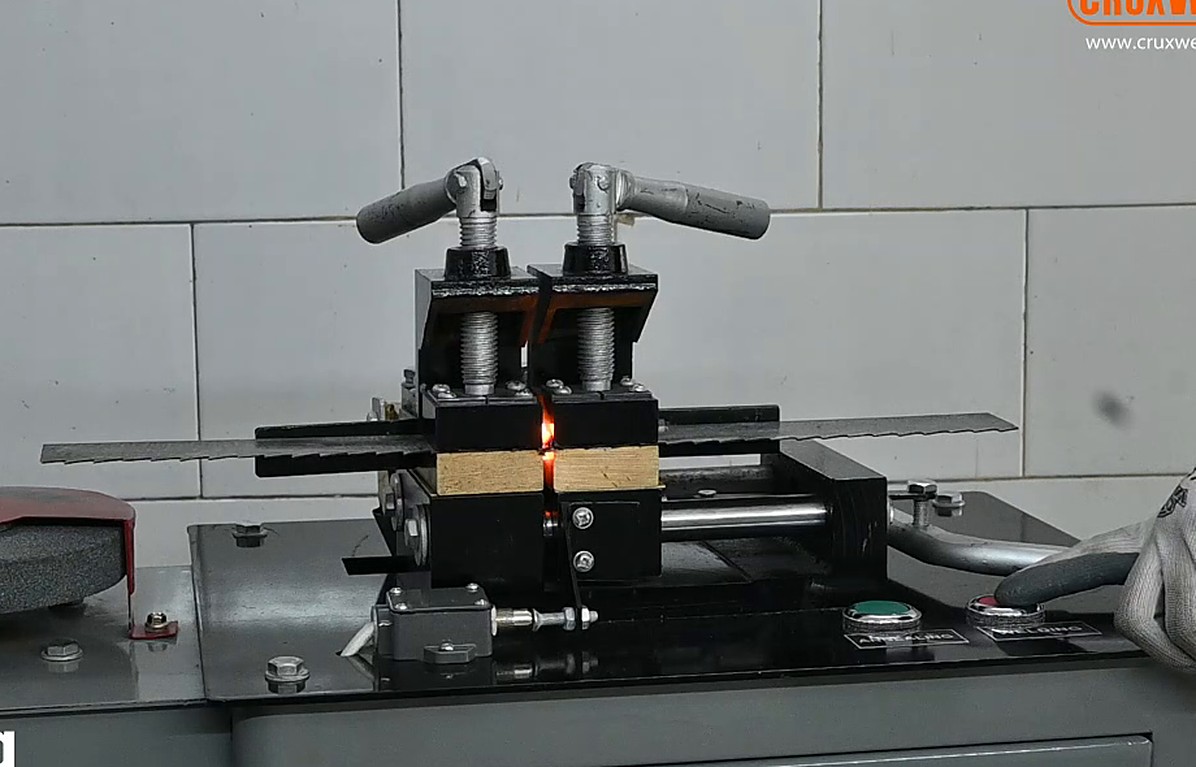
The weld: a short burst of current and the upset pressure forges the ends together.
3
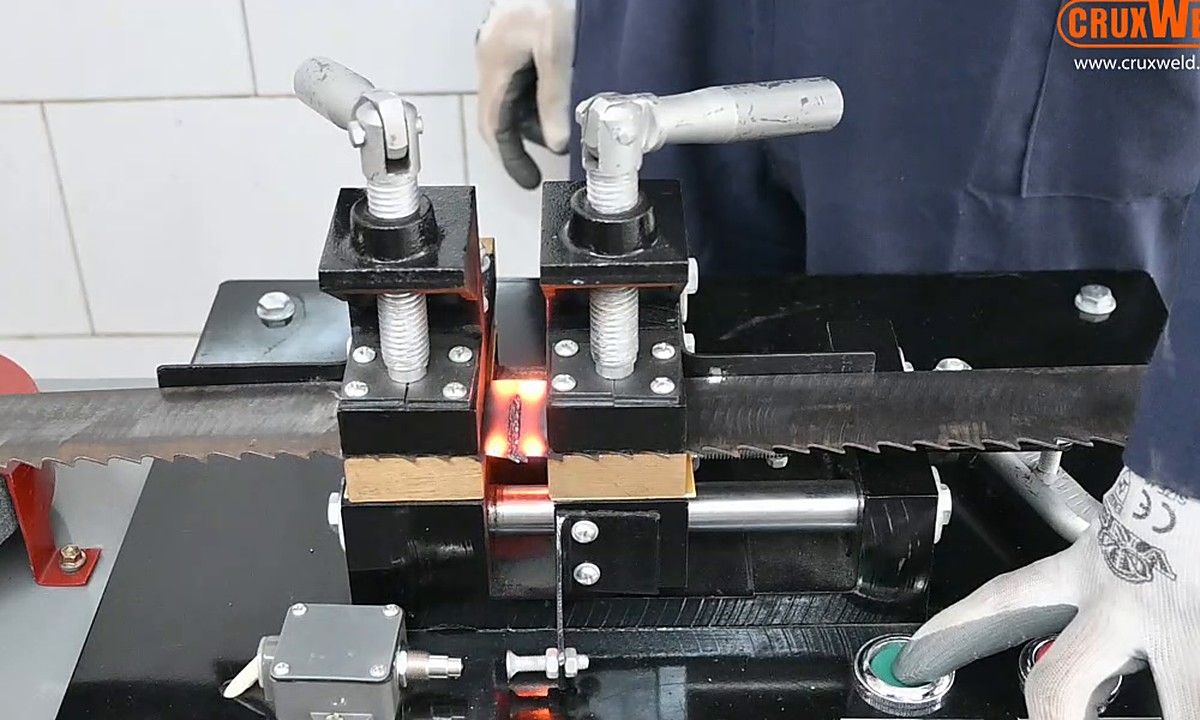
Annealing: the weld zone glows cherry-red and cools under control, restoring flexibility.
4
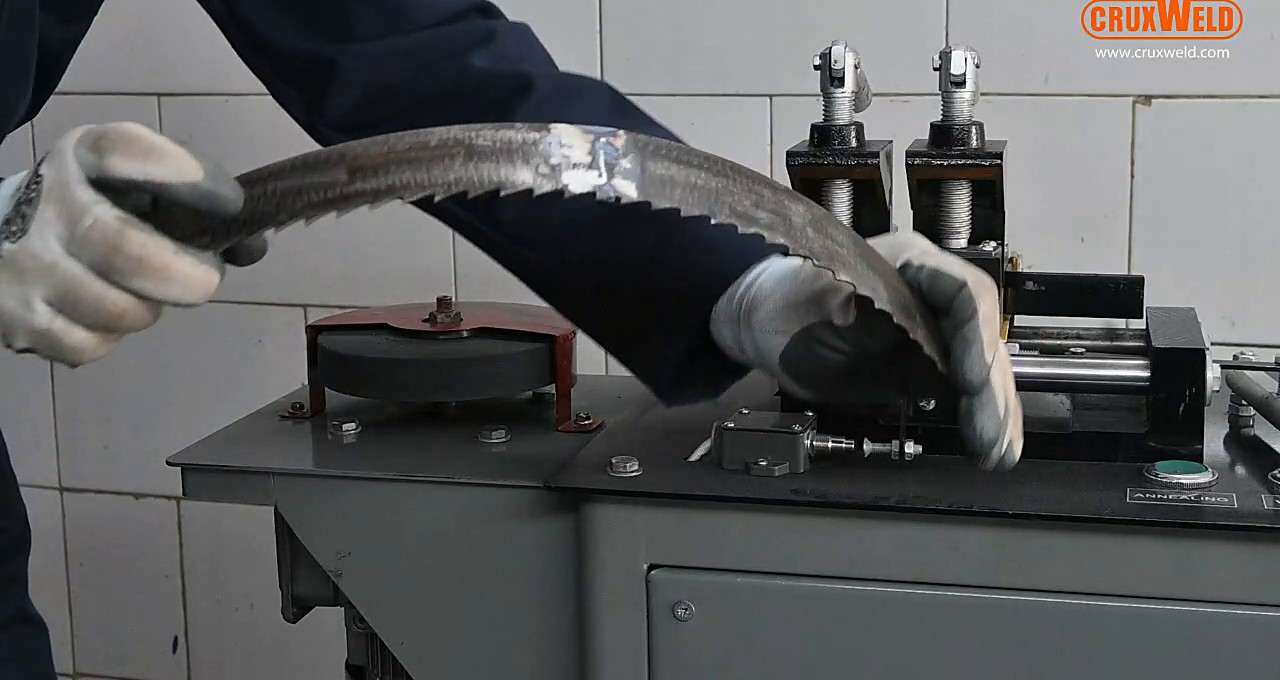
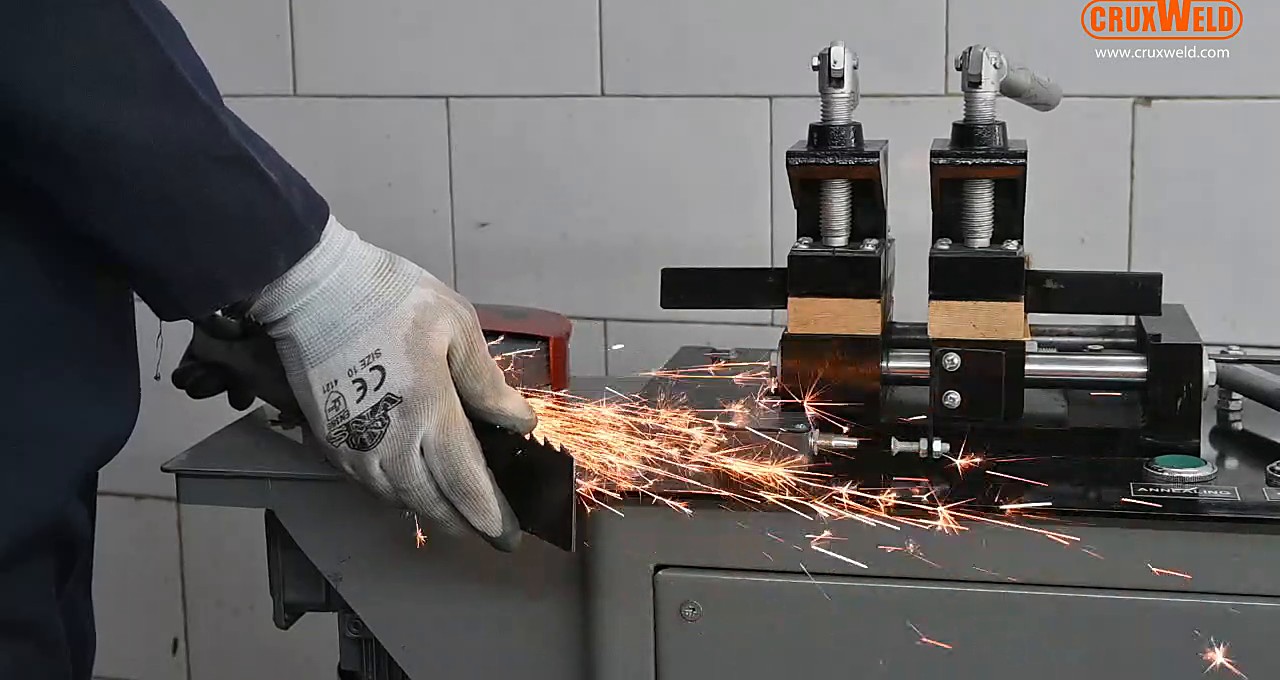
Grinding the seam flush on the built-in wheel, then the flex test on the finished blade.
Filmed on a production UltraFlex 520. Ask us on WhatsApp for a live demonstration on your own blade.
How it works
Four Steps from Broken Blade to Running Blade
1Clamp
Square the two blade ends and lock them in the dual copper jaw clamps. Clamping width 60 mm; set the secondary voltage (6 steps) for the blade width and thickness.
2Weld
Press Weld. Current flows across the joint, the ends reach forging temperature and the 200 N upset pressure pushes them together into one solid seam.
3Anneal
Press Anneal. The weld zone is reheated and cooled in a controlled cycle, turning the hard weld back into tough, flexible blade steel.
4Grind
Step on the foot switch and dress the seam flush on the built-in grinding wheel. The blade runs through the saw guides as if it were new.
Resistance butt welding is the standard way bandsaw blades are made into loops and repaired, because the joint is parent metal with no filler to fail at the gullets.
Why buyers choose it
What the UltraFlex 520 Fixes on the Shop Floor
The flex test: an annealed weld bends with the blade instead of cracking.
✓Blade stock cost: buy coil and weld your own loops to any length instead of stocking every finished size.
✓Downtime: a broken blade is repaired at the saw in minutes, not sent out for days.
✓Weld failures: integrated annealing removes the brittle zone that makes an unannealed weld snap at the gullet.
✓Operator skill: six voltage steps and push-button Weld / Anneal cycles give the same result from any operator.
✓Safety and speed: foot-switch grinding keeps both hands on the blade; stable table-mount base.
Need wider blades? The CBS175 welds strips up to 75 mm. For small shop blades the compact CBS040 is the entry model.
Key features
What Makes This Bandsaw Blade Butt Welder Different
01
12 kVA nominal capacity
Enough power for 52 mm bimetal blades at 2.0 mm thickness, with reserve for fast cycles.
02
6-step secondary voltage
Match weld heat to blade width and thickness with one selector — no guesswork.
03
Dual copper jaw clamps
High-conductivity jaws, 60 mm clamping width, hold the ends square and carry current evenly.
04
Integrated annealing
Push-button annealing cycle in the same clamps; blades are ready to run with no further treatment.
05
Built-in grinder, foot switch
Finish the seam flush hands-free; the operator keeps control of the blade.
06
Robust table-mount design
800 × 810 × 870 mm, 110 kg — a stable platform for consistent welds, year after year.
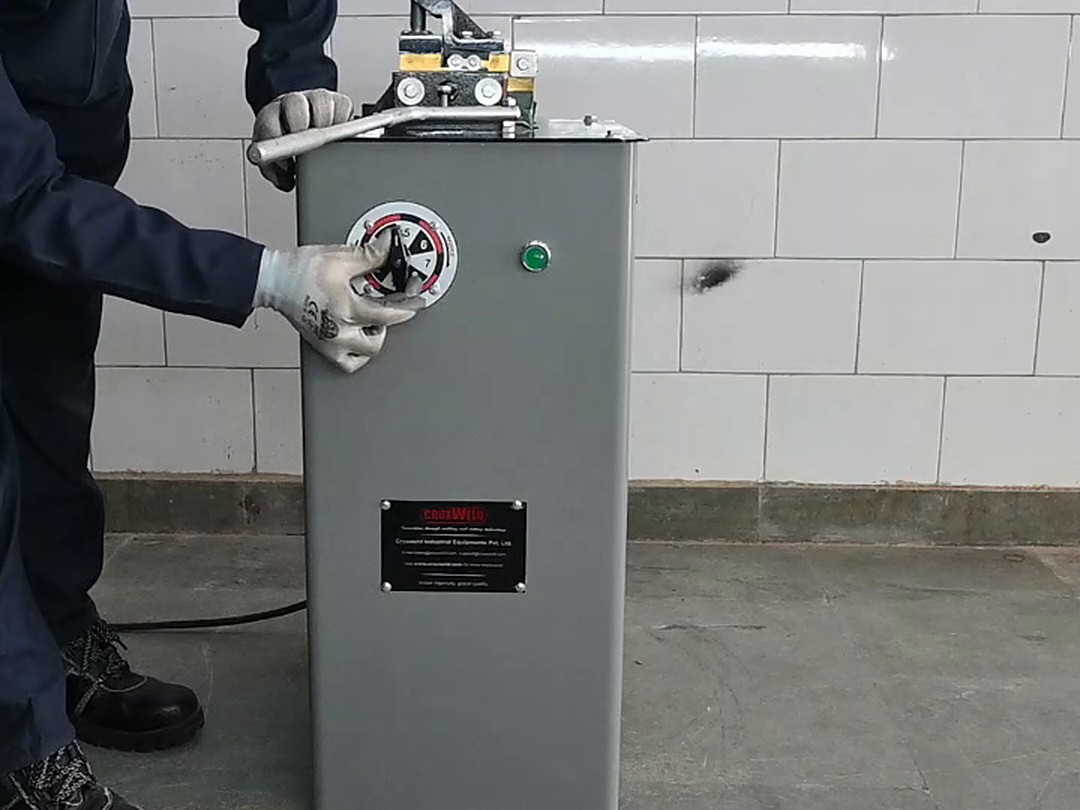
Six secondary voltage steps on the front panel.
Weld heat is chosen on the front selector. Thin carbon-steel blades take a low step; wide bimetal blades a high one. Once the step is found for a blade type it is simply repeated — the bandsaw blade butt welder gives the same joint on the first blade and the hundredth.
✓Input supply 400 V ±15%, rated 380 V, input current 40 A
✓Upset pressure 200 N
✓Weld, anneal and grind controls on one panel
What it welds
Blades, Widths and Materials
The UltraFlex 520 welds bimetal and carbon-steel bandsaw blades from coil or broken loops:
Bimetal (M42 / M51 type) bladesCarbon-steel bladesWidth 7 – 52 mmThickness 0.4 – 2.0 mmMetal-cutting band sawsWood & timber band sawsFood & meat band sawsCustom loop lengths from coil
Send us your blade width, thickness and type — we will confirm the voltage step and a sample weld on this bandsaw blade butt welder before you buy.
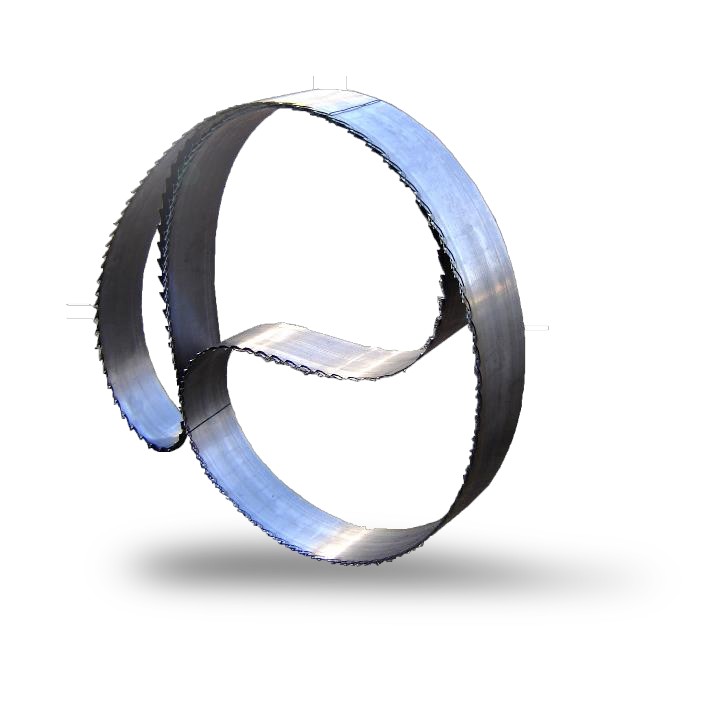
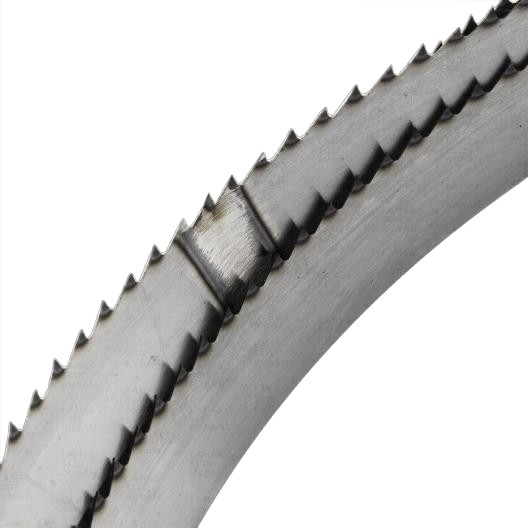
A finished blade loop welded from coil stock.
Applications
Who Uses the UltraFlex 520
Bandsaw blade distributors
Weld loops to order from coil stock with a bandsaw blade butt welder that handles every width to 52 mm.
Steel service centres & fabricators
Repair broken blades on the metal-cutting band saw in minutes.
Sawmills & timber yards
Keep wood-cutting band saws running with in-house welding and annealing.
Maintenance departments
One machine covers all the band saws in the plant.
Tool rooms & machine shops
Custom-length blades for vertical and horizontal saws.
Training institutes
Teach resistance butt welding and blade preparation on a safe, push-button machine.
Scope of supply
What Arrives with the UltraFlex 520
✓UltraFlex 520 bandsaw blade butt welder, table-mount, 110 kg
✓Dual copper jaw clamps fitted
✓Integrated annealing control
✓Built-in grinding attachment with foot switch
✓Operation manual and test certificate
The bandsaw blade butt welder is supplied ready to connect to a 400 V supply; the exact scope is confirmed on the quotation. See the full range on our products page.
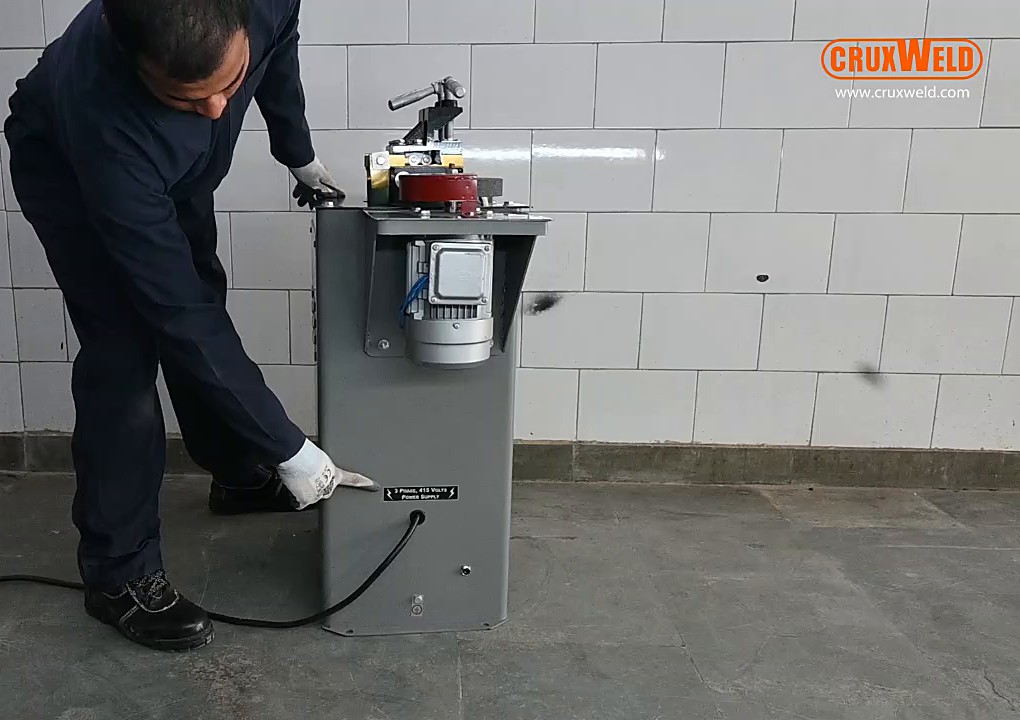
Table-mount machine with foot-switch grinding.
Why buy from CRUXWELD
Engineered, Assembled and Tested in India
45+ years of welding expertise
This bandsaw blade butt welder is designed, built and tested by CRUXWELD engineers in India; our technical team answers on WhatsApp.
ISO 9001:2015
Every machine is load tested and inspected before dispatch.
GeM Registered OEM Manufacturer
Tender-ready documentation for government, PSU and institutional buyers.
Pan-India supply, export ready
Dispatched across India and exported; copper jaws and spares in stock.
Width and thickness set what the jaws can hold — 7 to 52 mm wide and 0.4 to 2.0 mm thick covers the great majority of metal-cutting and timber blades. Six secondary voltage steps are how the bandsaw blade butt welder matches heat to the blade section. Upset pressure of 200 N forges the heated ends into one piece. The annealing and grinding functions are built in, so no second machine is needed.
Specifications from the CRUXWELD UltraFlex 520 datasheet; subject to improvement without notice. The quotation and test certificate supplied with the machine are the governing documents. Warranty terms are stated on the quotation / invoice.
A resistance welder that joins the two ends of a bandsaw blade. The ends are clamped in copper jaws, current heats the joint to forging temperature and upset pressure pushes the ends together into one seam. The UltraFlex 520 also anneals and grinds the joint on the same machine.
Which blades can the UltraFlex 520 weld?
Bimetal and carbon-steel bandsaw blades from 7 to 52 mm wide and 0.4 to 2.0 mm thick — coil stock welded into loops, or broken blades repaired.
Why does the weld need annealing?
The weld zone cools fast and becomes hard and brittle. The built-in annealing cycle reheats and slowly cools it, restoring strength and elasticity so the blade flexes around the saw wheels instead of cracking at the joint.
How is the weld seam finished?
On the built-in grinding wheel, operated by foot switch so both hands stay on the blade. The seam is dressed flush to the blade so it passes through the saw guides freely.
What power supply does this bandsaw blade butt welder need?
400 V ±15% (rated 380 V), 12 kVA nominal capacity, 40 A input current. Dimensions 800 × 810 × 870 mm, gross weight 110 kg, table-mount design.
How do I set the machine for different blades?
Choose one of the six secondary voltage steps for the blade width and thickness. Once the step is found for a blade type it is repeated for every weld of that type.
I need to weld blades wider than 52 mm — which model?
The CRUXWELD CBS175 bandsaw blade welding machine handles strips up to 75 mm. For small shop blades, the compact CBS040 is the entry model.
How do I get the price and delivery time?
Request a quote on this page or message +91 88008 82983 on WhatsApp with your blade width, thickness and type. You will receive a GST quotation with delivery time, usually the same working day.
Tell us your blade width, thickness and type — we will confirm the setting and send a quotation today.