Learning MIG Welding Aluminium

Aluminum Welding: The Aluminum is a very reactive metal thus lead on to the formation of oxide layers in a few moments although this oxide layer act as a protective layer against the corrosion leading on to longer life of the metal The MIG welding aluminum may be little difficult as it is altogether different from MIG welding of mild steel. If you are planning to weld aluminum by MIG with your wire feed welder then you have to master the technique of MIG welding of mild steel first. The MIG welding aluminum uses the same gun angle and gas flow rate as with the mild steel welding by MIG welding technique.
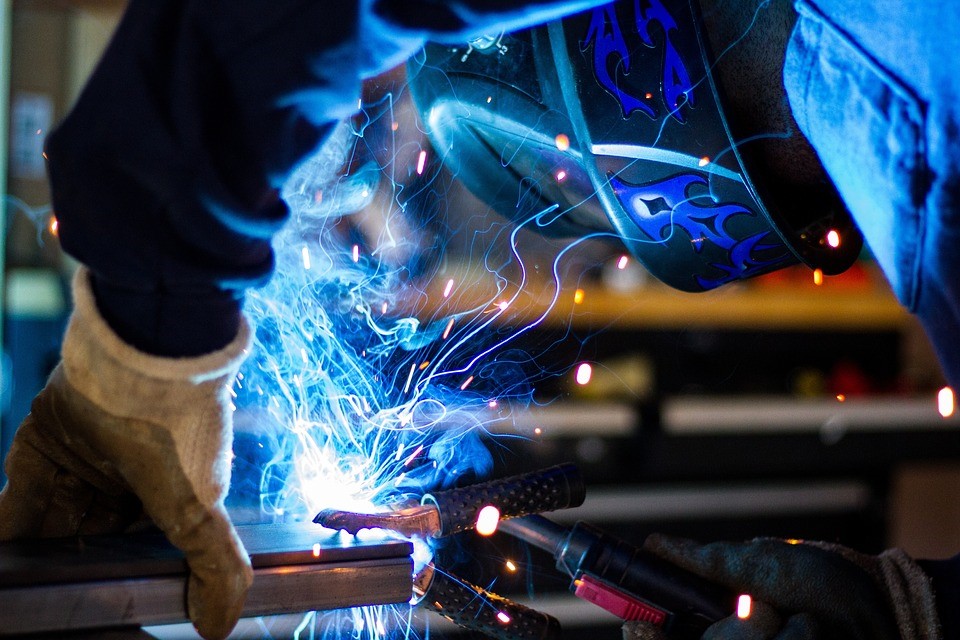
Welding Tips & Tricks: It is a tricky metal to weld with MIG welder with wire feeder as it takes more heat than mild steel. The minimum thickness recommended here with MIG is 14 to 18 ga. The choice of welding thinner than this size always need a TIG welding machine. This welding process of aluminum welding is notorious for the burn through unexpectedly as weld puddle may fall through the metal piece making the process not useful for thin pieces.
1. Travel speed of Mig Aluminum weld-
The voltage setting for the mild steel should be the same as with aluminum but one has to double the travel speed in aluminum welding with Mig welder. In the initial stage, it may be a little uncomfortable as a fast process of welding until one is used to it. The Mig welding mild steel use the short circuit transfer technology where the wire electrode drops into molten weld puddle by a short circuit at the desired welding joint. While in aluminum spray transfer technology is the available welding technique where tiny particles o aluminum wire are sprayed in the weld puddle.
2. Oxide Clean –
The oxide has twice the available melting point so if not removed before welding it may lead on to nonjoining of your joint. The surface of aluminum should be thoroughly cleaned by degreasing of the surface by aluminum wire brush, not steel wire brush.
3. Appropriate Gas Mixture –
The 100% argon shielding gas is the choice for aluminum Mig welding as this is a nonferrous metal to complete the spray process of transfer. The thicker aluminum of more than 1/2″ the helium is being added in the ratio of 25 to 75% for the deeper penetration in the aluminum workpiece.
4. Spool Gun or Wire feeder option –
The aluminum wire or the Mig is very soft and may lead on to birds nesting inside the liner. The wire is not stiff enough as mild steel wire for which spool gun with small lb. roll is a better option.
5. The filler material –
The filler wire available in general are 4043 and 5356 but 4043 flow better and suits minimum in a maximum of the cases. The 5356 may be required in cases where post-weld anodizing is required. The thickness of the wire should be maximum for a better result.
6. The welding process –
The spray transfer for Mig welding aluminum with a short stick out and longer stick out required depending on the situation.

CRAZY IN LOVE WITH WELDING. Ramakant has a diversified background with industrial experience in welding and production management. He holds a master's degree (M.Tech.) in metallurgy and welding technology from SLIET University. He has experience in a number of industries, including power generation, defense, construction, mining equipment, and heavy engineering fabrication. He holds the positions of welding engineer, quality and inspection officer as well as general management. He has written technical welding articles, contributed to the various welding committees. For the past eight years, Ramakant has been a technical consultant, trainer, and spokesperson for Cruxweld.