Advanced MIG 500 Water Cooled Welding System | Cruxweld

CWMIG500P
Water-cooled · 500 A · MIG/MAG · FCAW · MMA
500 Amps That Stay Cool Through the Long Shift.

The CRUXWELD CWMIG500P is a MIG 500 water cooled welding system for heavy fabrication: an IGBT inverter power source, a built-in cooling unit for the water-cooled torch and a 4-roll wire feeder, all on one trolley. MIG/MAG, flux-cored and stick from the same machine.

50–500 A
MIG current
15.5–50 V
welding voltage
1.0–1.6 mm
wire
4-roll
wire feeder
✓Water-cooled torch for high-amp work
✓Dual digital volt and amp displays
✓Trolley carries the gas cylinder

Full specifications →

Price, delivery & technical help — get a fast response.

Overview

01
The system

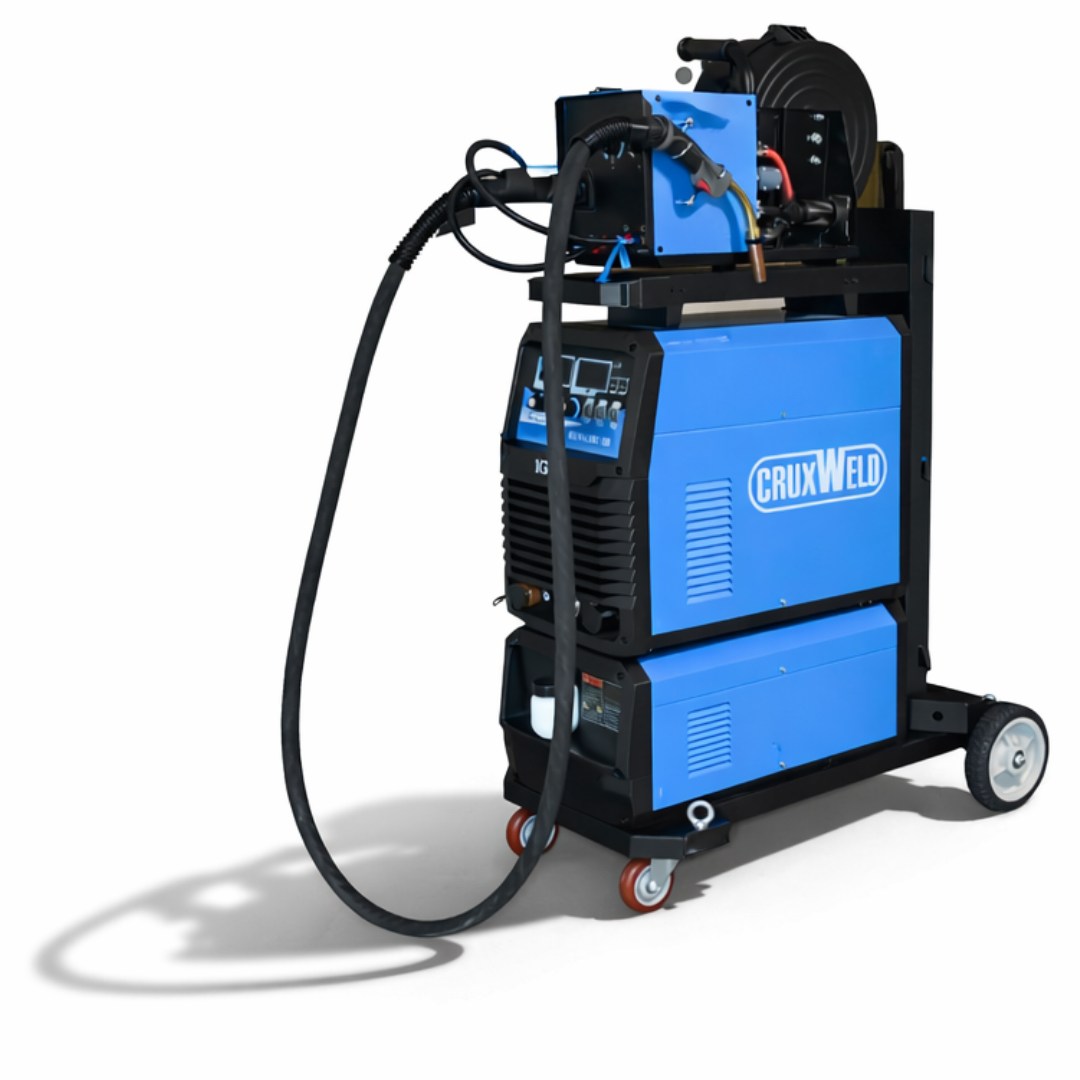
One Trolley, Four Modules, Built for 500 A

At 300, 400, 500 A an air-cooled torch runs hot, and the welder stops before the job does. The CWMIG500P sends coolant through a water-cooled torch, so you can keep the arc on heavy plate, multi-pass fillets and flux-cored runs for the whole shift.

Everything stacks on one trolley — feeder on top, inverter power source in the middle, cooling unit below, gas cylinder on the back — so the whole station rolls to the job as one unit.
TOP TO BOTTOM
Wire feeder
4-roll drive, 1.5–22 m/min, current and voltage knobs, spools up to 18 kg
Power source
IGBT inverter, 50–500 A, dual digital displays, 2T/4T, MIG/MMA
Cooling unit
Pumps coolant through the water-cooled torch
Trolley
Wheels and castors, platform for the gas cylinder
CRUXWELD CWMIG500P MIG 500 water cooled welding machine on its trolley with torch

CWMIG500P complete system
02
Module 1 · Wire feeder

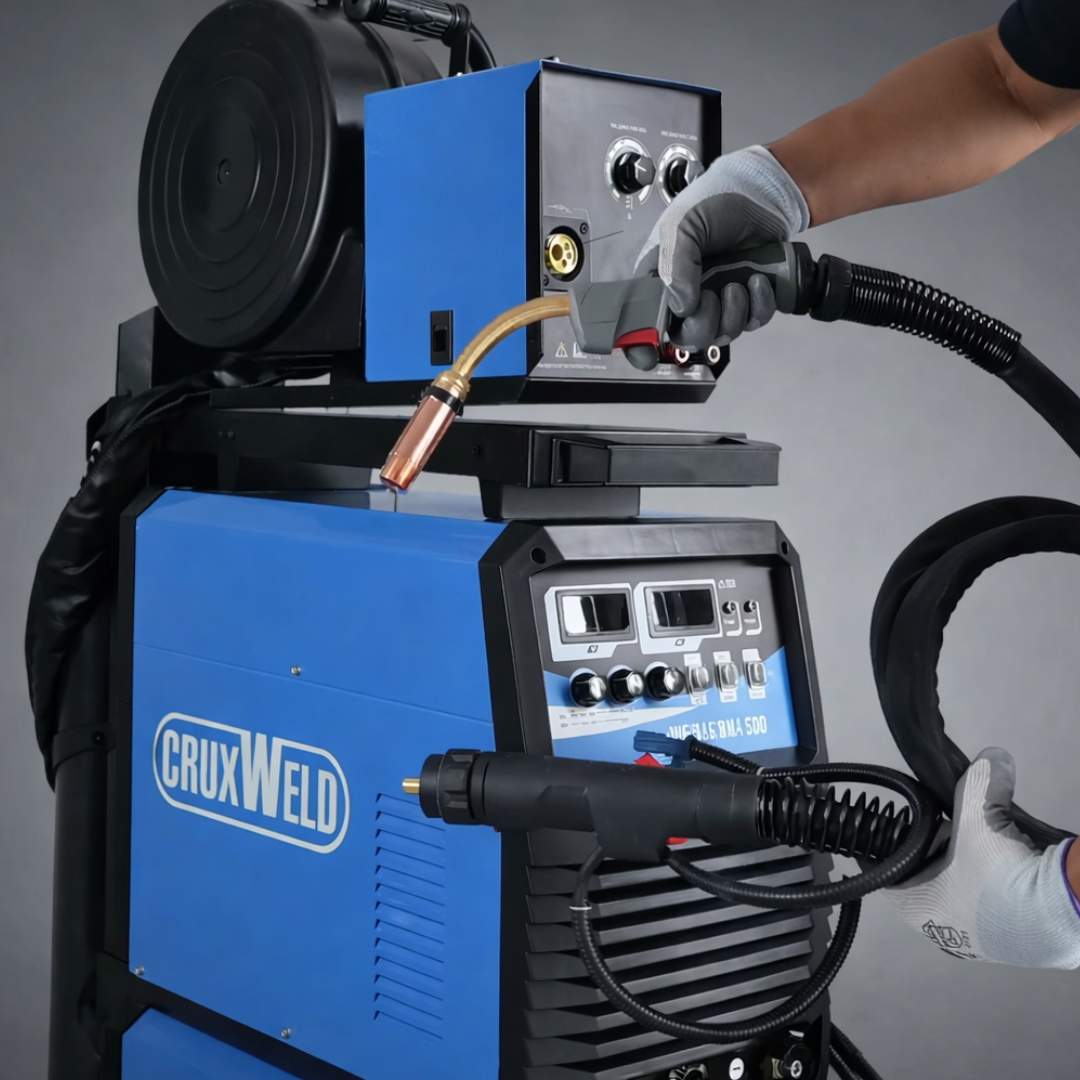
Four Rolls Push the Wire Without Slipping

4-roll drive
Grips solid and flux-cored wire evenly for a steady feed.
1.5–22 m/min
Wire feed speed range.
1.0–1.6 mm wire
Solid and flux-cored, on spools up to 18 kg.
Set at the feeder
Current knob sets wire speed, voltage knob sets arc voltage.
Gas check / wire check: purge the gas line and set flow, or inch the wire through the torch with no welding voltage — then return the switch to centre.
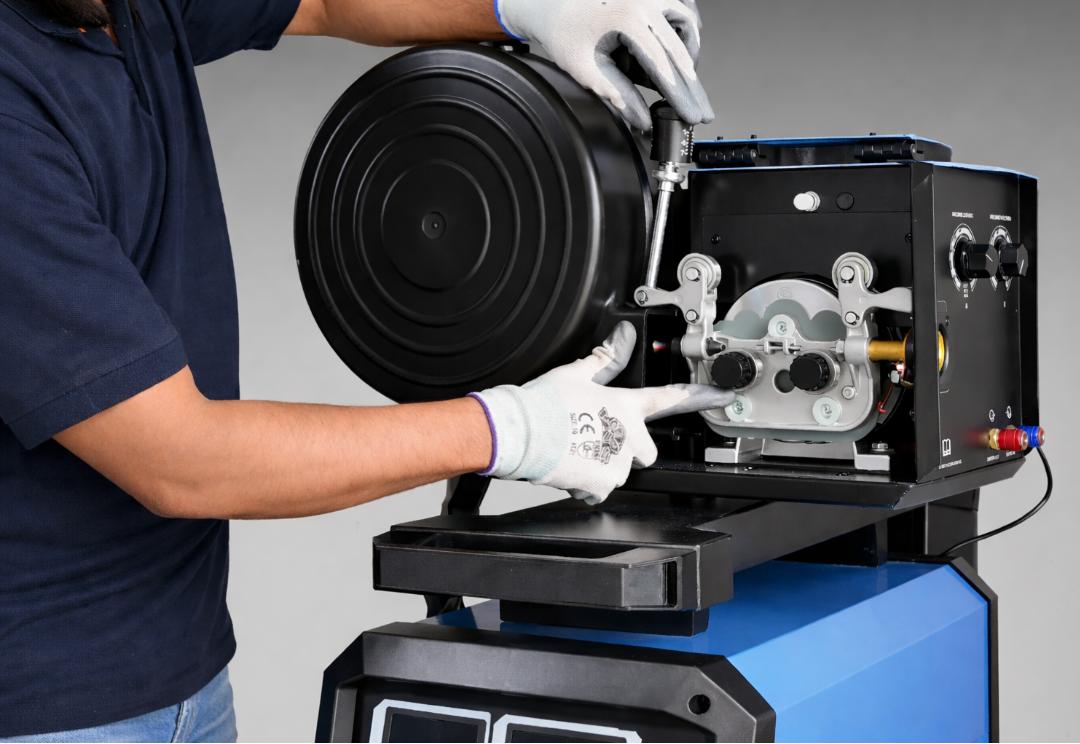
Adjusting the 4-roll wire feeder on the CWMIG500P

Feeder controls
Loading a wire spool into the CWMIG500P wire feeder

Spool up to 18 kg
03
Module 2 · Power source

IGBT Inverter With the Controls Welders Actually Use

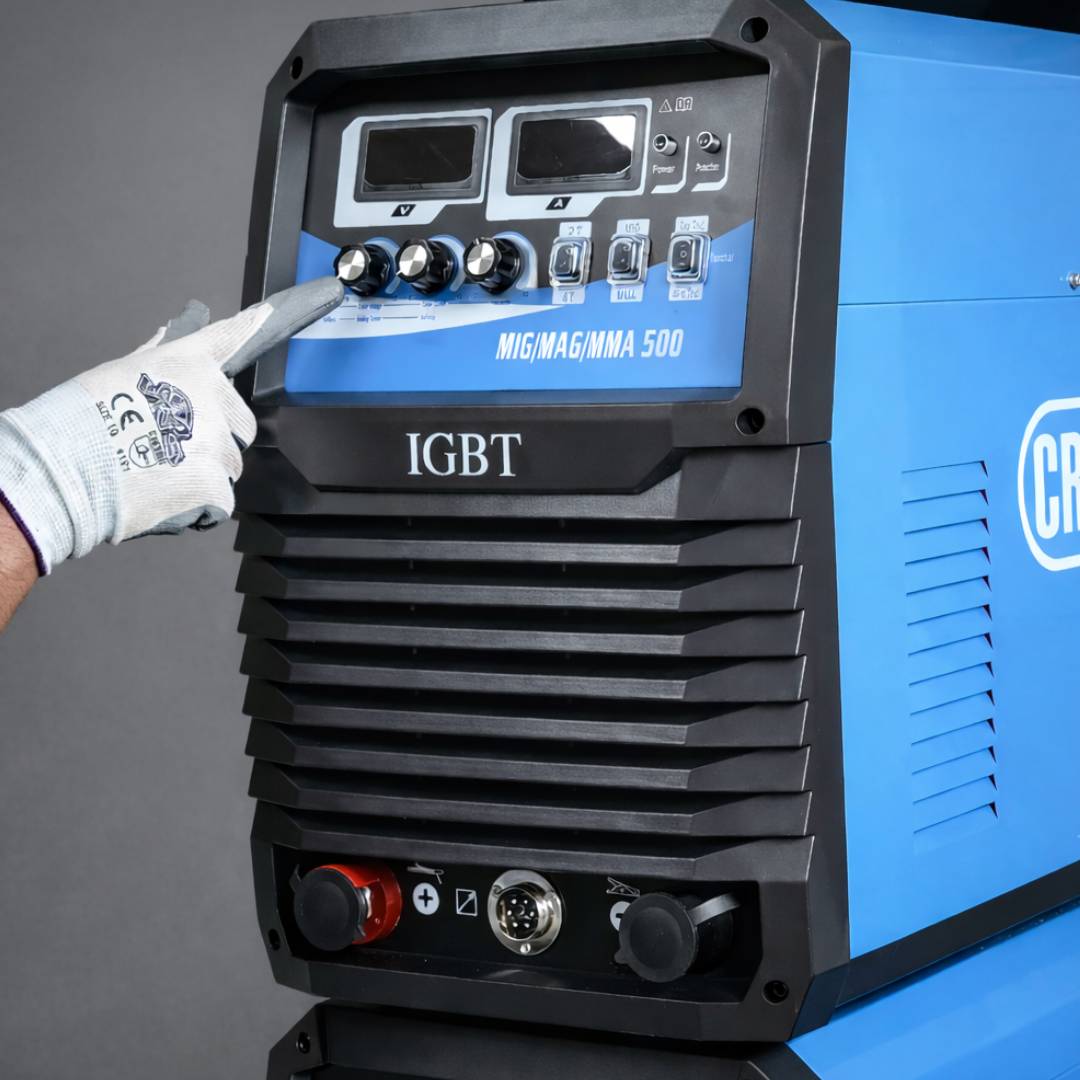
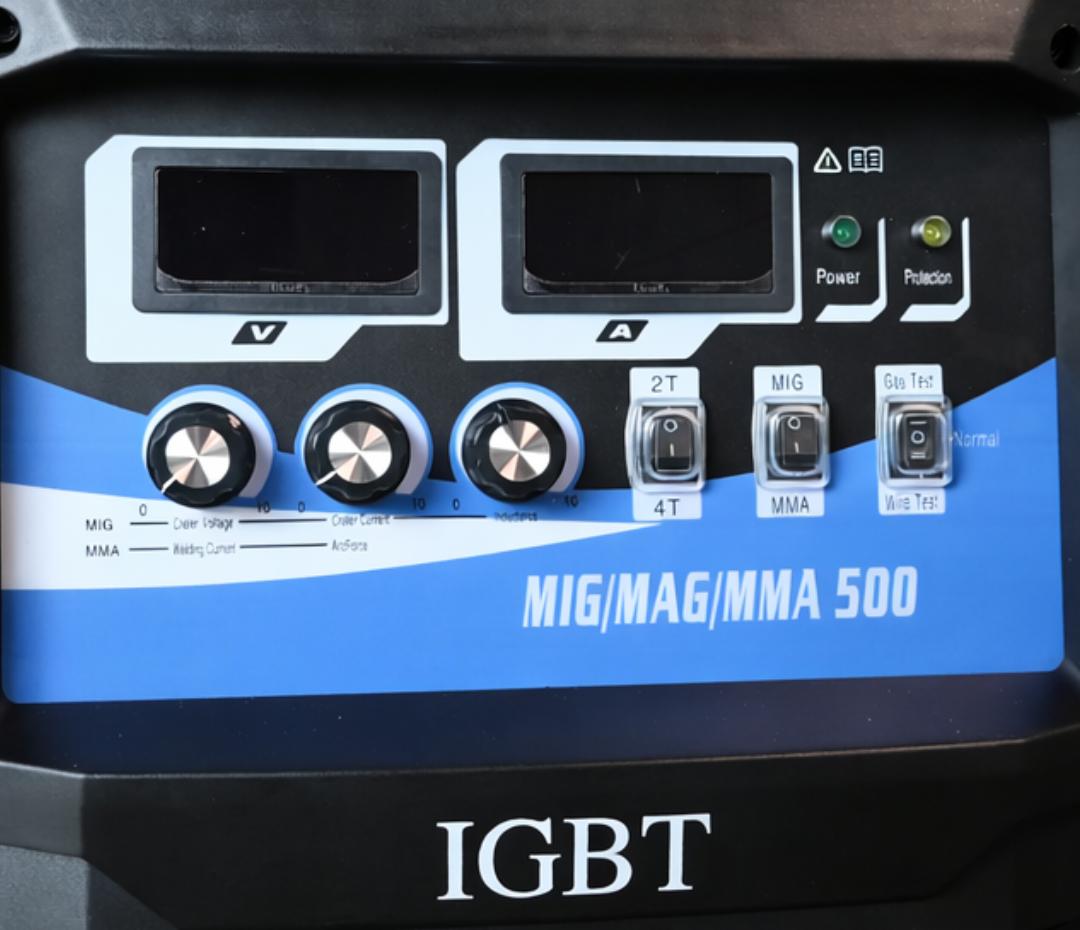
CWMIG500P front panel with dual digital displays, inductance, crater and mode switches

Front panel
30–500 A
MMA current
70–80 V
open circuit
91%
efficiency
V / A displaysPreset values before welding, actual values while welding
2T / 4TTrigger mode for short welds or long runs
Crater voltage & currentFill the crater at the end of the weld (4T)
InductanceLow: harder, focused arc. High: softer, wetter bead, less spatter
MIG / MMAProcess switch; in MMA the knobs set current and arc force
Protection lampLights on overheat, overload or bad supply; output off until cleared
36 V heater socketPowers a CO2 regulator heater
04
Module 3 · Cooling unit

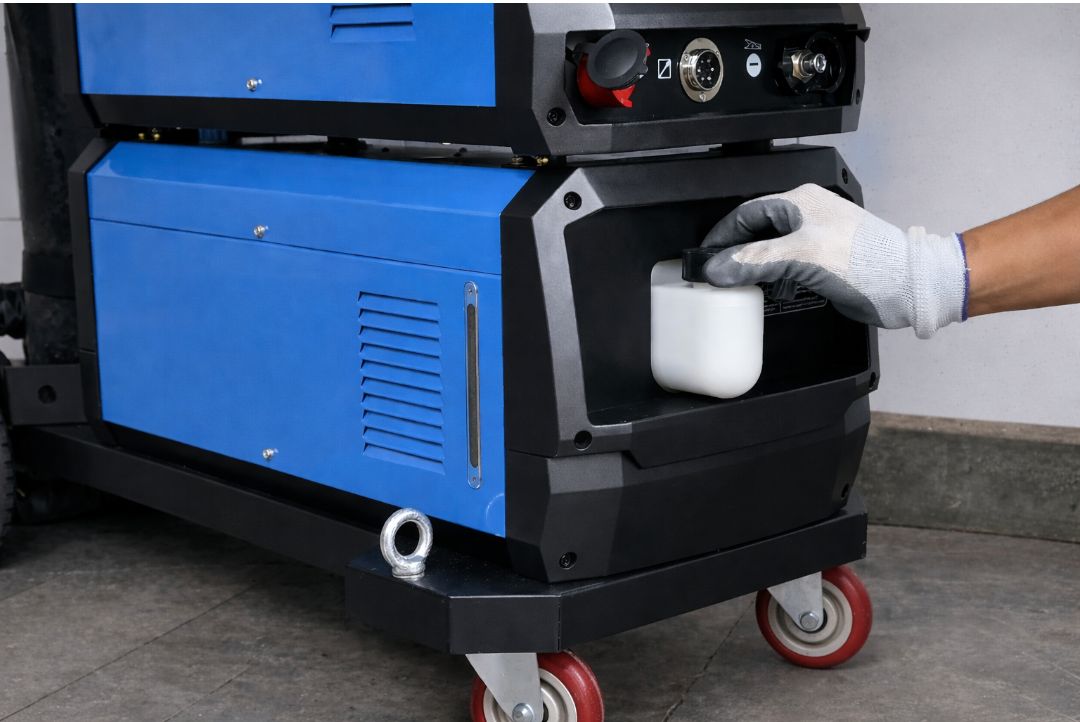
Coolant Through the Torch, Not Just Air Over It

Filling the CWMIG500P cooling unit tank with coolant

Fill to the max mark
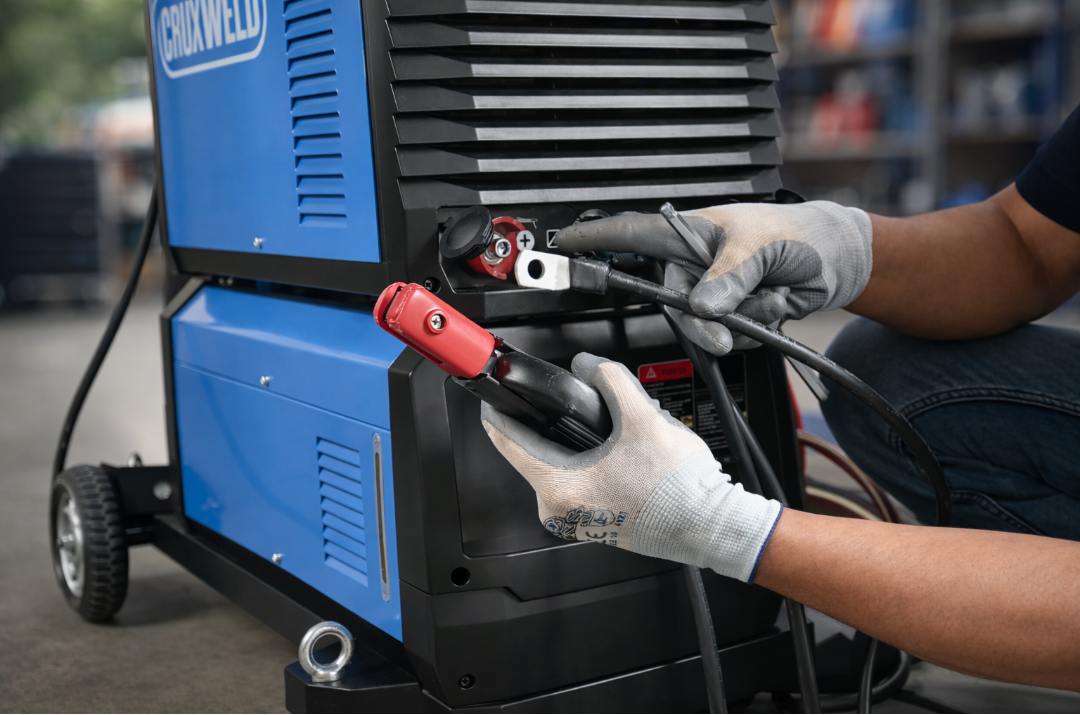
Connecting the water-cooled MIG torch on the CWMIG500P

Torch connection

The built-in cooling unit circulates coolant through the torch and back, carrying away the heat that a 500 A arc puts into the neck and cable. Red and blue quick couplings on the feeder make the hose connections simple: blue to blue, red to red.

✓Fill with distilled or de-ionised water, or ready-mixed welding coolant
✓Below 0 °C, use a water and ethylene-glycol mix
✓Keep the level between the min and max marks; change the coolant once a year
Never weld with the tank empty or the hoses disconnected — a water-cooled torch can be damaged within seconds.
05
Settings guide

Where to Start for Mild Steel

MIG, CO2 or mixed gas, mild steel
CurrentVoltageWire
80–130 A18–21 V1.0 mm
130–200 A20–24 V1.0 mm
200–250 A24–27 V1.0 / 1.2 mm
250–350 A26–32 V1.2 / 1.6 mm
350–500 A31–39 V1.2 / 1.6 mm
✓Gas flow 15–20 L/min up to 250 A; 20–25 L/min above
✓Stick-out 10–15 mm for solid wire, 15–25 mm for flux-cored
✓Torch 10–20° from vertical; about 45° on fillets
Which gas?
GasUse
100% CO2Mild steel — deep penetration, economical
Argon + 15–25% CO2Mild and low-alloy steel — smoother arc, less spatter
Argon + 2% O2 or 2–3% CO2Stainless steel
100% argonAluminium, with aluminium wire and U-groove rolls or a spool gun

These are starting points — confirm with a trial weld. For your plate and joint, send the details on WhatsApp and our technical team will suggest settings.
06
Applications

Heavy Plate, Long Runs, Many Metals

Structural steel
Beams, columns, base plates and multi-pass fillets.
Shipbuilding
Long seams and heavy sections, shift after shift.
Heavy engineering
Frames, vessels and machinery bases.
Oil & gas fabrication
Skids, supports and structural work.
Transport
Trailers, chassis and body fabrication.
Automation
Pairs with CRUXWELD welding carriages for mechanised runs.
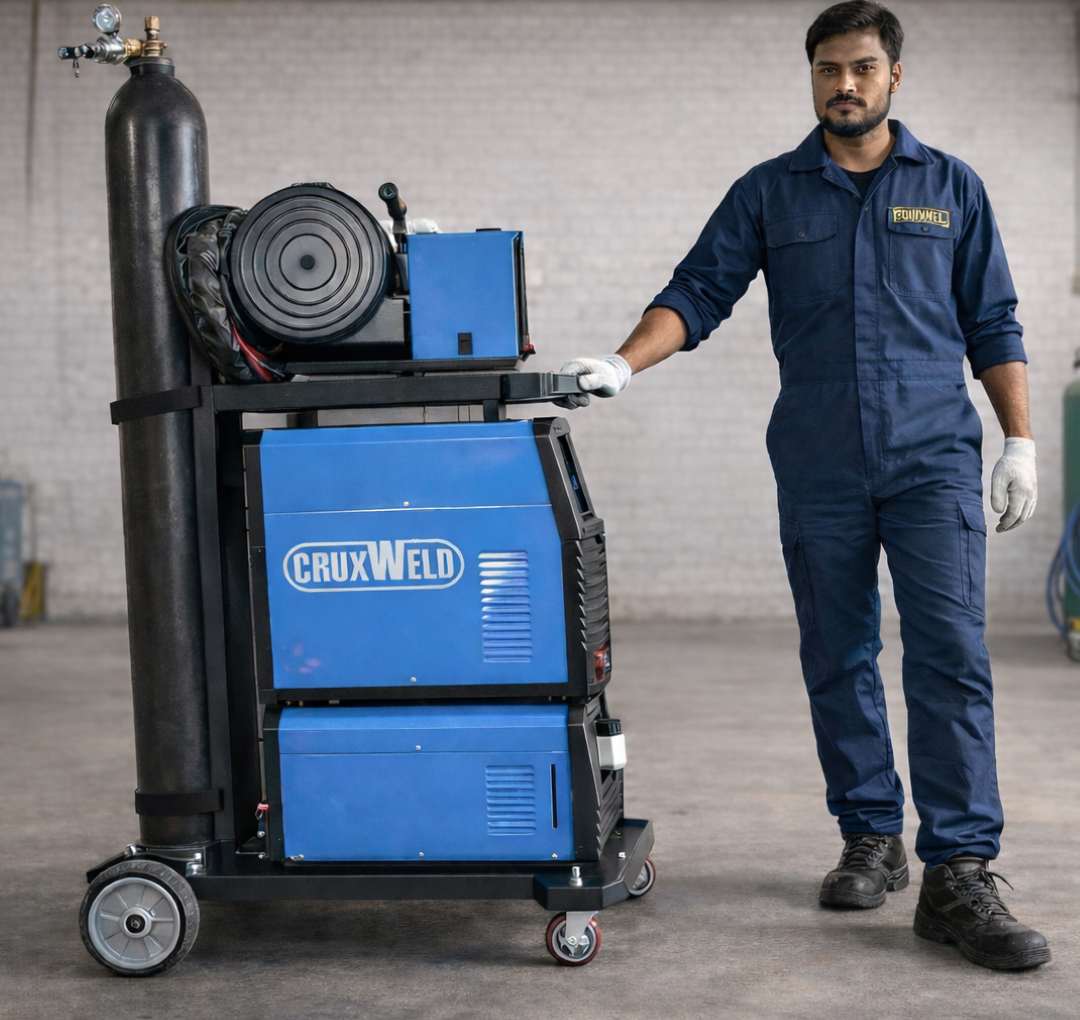
Welder standing next to the CRUXWELD CWMIG500P water cooled MIG welding machine

A full-size workshop station: feeder, power source and cooling unit on one trolley
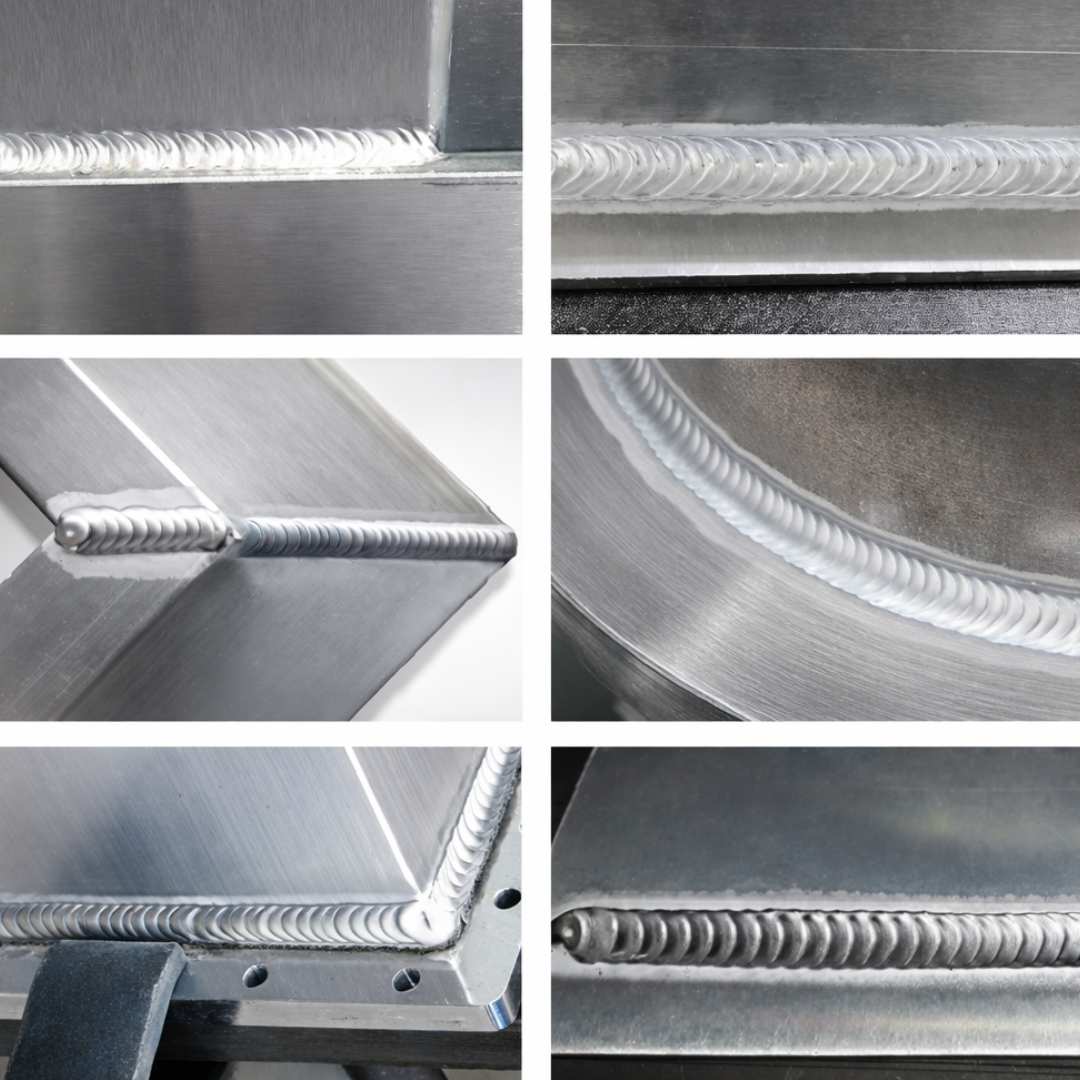
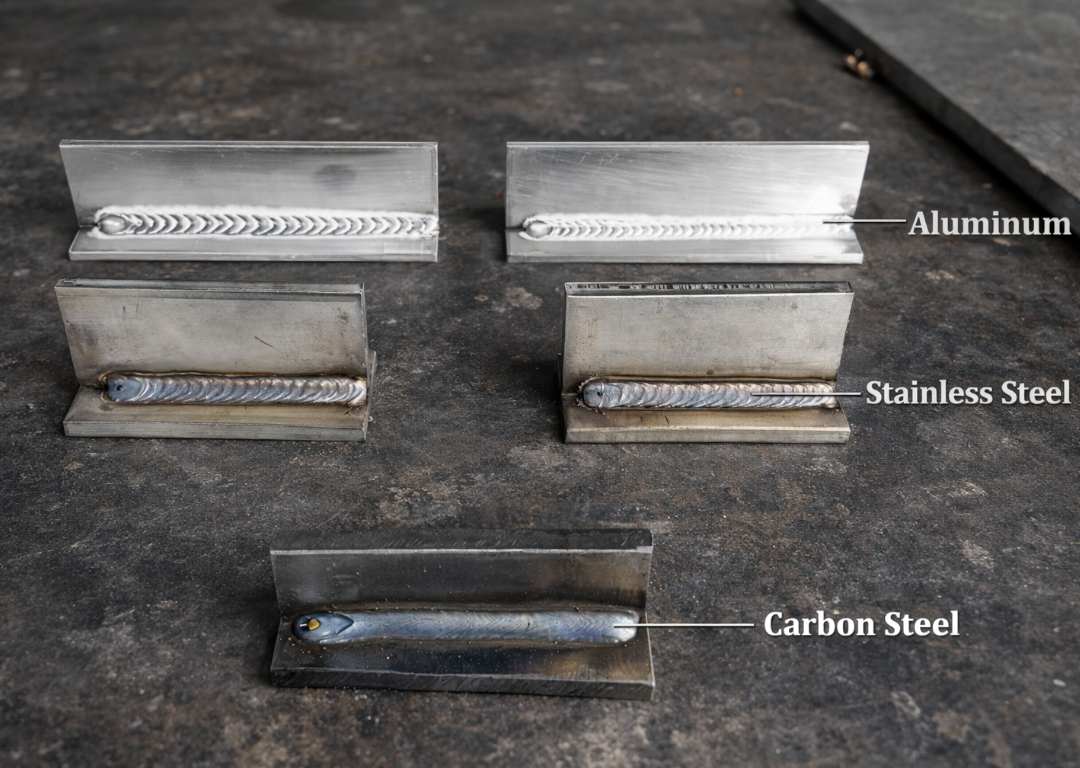
MIG welds on aluminium, stainless steel and carbon steel

Carbon steel, stainless, aluminium
Fillet and butt weld beads made with the CRUXWELD MIG 500

Bead quality on fillets and butts
07
Installation & range

What Your Shop Needs, and Which MIG to Choose

Site requirements
Supply3-phase 400 V ±15%, 50/60 Hz; no missing phase
Input24.2 kVA, 37 A rated
Isolator / breaker63 A
Supply cableAt least 6 mm², 4-core copper
EarthMachine must be earthed
Clearance50 cm front and rear, 20 cm at the sides
Working temperature−10 to +40 °C
Wind at the arcNot more than 1 m/s; screen outdoors
Which CRUXWELD MIG?
Heavy plate, long shifts, water-cooledCWMIG500P ✓
Built-in feeder, light fabricationWeldEasy MIG 250 →
250 A workshop MIGMIG 250 →
400 A industrial MIGMIG 400 →
600 A MIGMIG 630 →

Automating long welds? Mount the torch on a WeldyFi fillet carriage or a DynaTwin 200M dual-torch carriage.

08
Why buy from CRUXWELD

Industrial Welding Support from People Who Weld

45+ years of welding expertise
Help with wire, gas and settings for your job from our technical team on WhatsApp and video call.
GeM Registered OEM Manufacturer
Tender-ready documentation for government, PSU and institutional buyers.
Tested before dispatch
Every machine is checked and run before it ships.
Supported Worldwide
Dispatched across India and exported, with spares and consumables on request.

Specifications

09
Specifications

MIG 500 Water Cooled Welding Machine CWMIG500P — Technical Data

PARAMETERCWMIG500P
Input
ModelCWMIG500P
Mains voltage3-phase 400 V ±15%
Frequency50 / 60 Hz
Rated input power24.2 kVA
Rated input current37 A
Efficiency91%
Power factor0.93
Output
Welding processesMIG/MAG (GMAW), FCAW, MMA
Output current, MIG50 – 500 A
Output current, MMA30 – 500 A
Welding voltage range15.5 – 50 V
Open circuit voltage70 – 80 V
Rated duty cycle100%
Trigger modes2T / 4T
Wire & gas
Wire feeder4-roll drive
Wire feed speed1.5 – 22 m/min
Wire diameter1.0 – 1.6 mm (solid and flux-cored)
Wire spool capacityUp to 18 kg
Shielding gasCO2, argon, argon mixtures
Heater socketAC 36 V, 3.5 A
Cooling & build
Torch coolingWater, integrated cooling unit
DisplaysDual digital (V and A)
Overload protectionAutomatic shutdown
Insulation classH
Protection classIP21S
Working temperature−10 to +40 °C
Dimensions (L × W × H)1040 × 515 × 1415 mm
WeightApprox. 110 kg (without gas cylinder)

Specifications are subject to improvement without notice; the quotation and test certificate supplied with the machine are the governing documents. Warranty terms are stated on the quotation / invoice.

Video

Question & Answers

10
FAQ

MIG 500 Water Cooled Welding Machine — FAQs

What is the CRUXWELD MIG 500 water cooled welding machine?
The CWMIG500P is a 500 A IGBT inverter MIG welding system with a built-in cooling unit, a water-cooled torch and a 4-roll wire feeder on one trolley. It welds MIG/MAG, flux-cored (FCAW) and MMA.
Why choose a water-cooled MIG welder?
At high current an air-cooled torch heats up quickly. The cooling unit circulates coolant through the torch, so it stays at a workable temperature on heavy plate, multi-pass welds and long shifts.
What current and voltage range does it have?
MIG output is 50–500 A and MMA output 30–500 A, with a welding voltage range of 15.5–50 V. Current and voltage are set on the wire feeder and shown on the dual digital displays.
Which wire sizes and gases can I use?
Solid and flux-cored wire from 1.0 to 1.6 mm on spools up to 18 kg. Shielding gas can be 100% CO2, argon/CO2 mixes, argon with 2% O2 for stainless, or 100% argon for aluminium.
What power supply does it need?
A 3-phase 400 V ±15%, 50/60 Hz supply rated for 24.2 kVA (37 A rated input current), with a 63 A isolator, a supply cable of at least 6 mm² 4-core copper and a proper earth.
What coolant should I use?
Distilled or de-ionised water, or ready-mixed welding coolant, filled between the min and max marks. Below 0 °C use a water and ethylene-glycol mix. Change the coolant once a year, and never weld with the tank empty.
Does it have 2T/4T and crater fill?
Yes. A 2T/4T switch selects the trigger mode, and in 4T the crater voltage and crater current knobs set the end-of-weld crater fill. An inductance knob tunes the arc from hard and focused to soft with less spatter.
How do I get the CWMIG500P price and delivery time?
Request a quote on this page or message +91 88008 82983 on WhatsApp with your plate thickness, wire and application. You will receive a GST quotation with delivery time, usually the same working day.
Tell us your plate, wire and job — we will confirm the set-up and quote today.

Leave a comment

Your email address will not be published. Required fields are marked *

Advanced MIG 500 Water Cooled Welding System | Cruxweld

WhatsApp chat