Troubleshooting guide › Specialised welding › Seam welding
A resistance seam weld is a row of overlapping spot nuggets made by two wheel electrodes while the sheet moves. For a leak-tight seam every nugget must overlap the one before it, which ties four settings together: current, weld time, cool time and wheel speed. Change one without the others and the seam looks fine on the outside and leaks on test. This page is for longitudinal and circumferential seam welders on tanks, drums, cans and ducting.
Reviewed by the Cruxweld technical team, October 2026. Settings are starting points to confirm on a test piece; acceptance is decided by the code or drawing the job is built to. Checks marked “call” are for our technical team.
Nugget spacing = wheel speed x (weld time + cool time). For a leak-tight seam the nuggets must overlap by about 25-50 %, so the spacing must be less than the nugget length. Raise the speed and you must shorten the cycle (or raise current to make bigger nuggets); lengthen the cool time and the nuggets separate. For a non-pressure-tight stitch seam the cool time can be long and the nuggets spaced.
| Setting | Too low | Too high |
|---|---|---|
| Current (heat) | Small or no nuggets, seam peels | Expulsion, burn-through, pickup on the wheels |
| Weld time | Small nuggets | Overheating, indentation |
| Cool time | Continuous heating: wheels and sheet overheat, wrinkling | Nuggets separate: leaks |
| Wheel speed | Slow production, overheating | Nuggets separate, skipped welds |
| Force | Expulsion, pickup, inconsistent | Deep wheel tracks, thin seam |
Nuggets not overlapping: speed too high for the cycle, cool time too long, current too low; or a gap in the overlap where the sheets were not in contact (fit-up).
Wheel contact lost on a wavy or dirty sheet; wheel pickup insulating the face; controller in discontinuous mode when continuous was wanted; force too low.
Current too high or force too low at the start of the seam; galvanised or dirty sheet; wheels dry (no cooling) or worn.
Too much heat in a long seam: cool time too short, current too high, speed too low; thin sheet with no hold-down.
Current too high; speed too low; sheets not in contact (gap) so the current concentrates; edge of the lap too narrow.
Force too high; wheels too narrow; weld time too long.
Guide not set; sheet feeding at an angle on a longitudinal machine; drum not concentric on a circumferential machine.
Wheels and transformer heating up; water flow low; mains sagging.
Longitudinal for straight seams on open sheet and the side seam of a cylinder before it is closed; circumferential for the ends of drums, tanks and cans where the part rotates against the wheels. Many shops need both for a tank.
Yes, with a little more current and force, frequent wheel dressing, and good extraction for the zinc fume. Expect more pickup on the wheels than with bare steel.
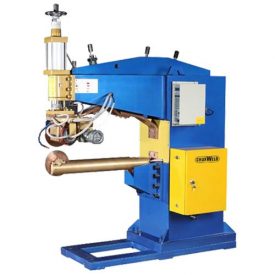 Longitudinal seam welderSpecifications →
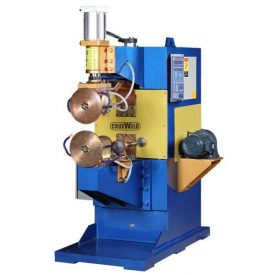 Circumferential seam welderSpecifications →
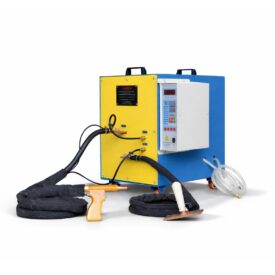 DuoFlex 20K spot and seam welderSpecifications →
Open your model for its specifications; the spares page lists the consumables for it.
If the machine runs but the weld or cut is wrong, the cause is usually settings, consumables or the material. Start here:
A seam welder needs a controller that times weld and cool cycles against wheel speed (the DuoFlex 20K sets pre-pressure, squeeze, weld, interval and hold in 20 ms cycles and stores them as specification numbers), water-cooled wheels and a drive that holds a constant speed. Longitudinal machines weld straight seams on open sheet; circumferential machines rotate a closed drum or tank end against the wheels.
Send a photo of the weld or cut, your machine model, consumable and plate thickness. Our technical team replies on WhatsApp with the likely causes and the next checks to make.
45+ years of welding expertise · GeM Registered OEM Manufacturer · Supported Worldwide

