Pneumatic Spot Welding Machine ProSpot 3500 | 35 kVA Spot & Projection Welder

ProSpot 3500
Pneumatic spot & projection welder • 35 kVA • Model ProSpot 3500

One pedal. One clean spot. Every time.

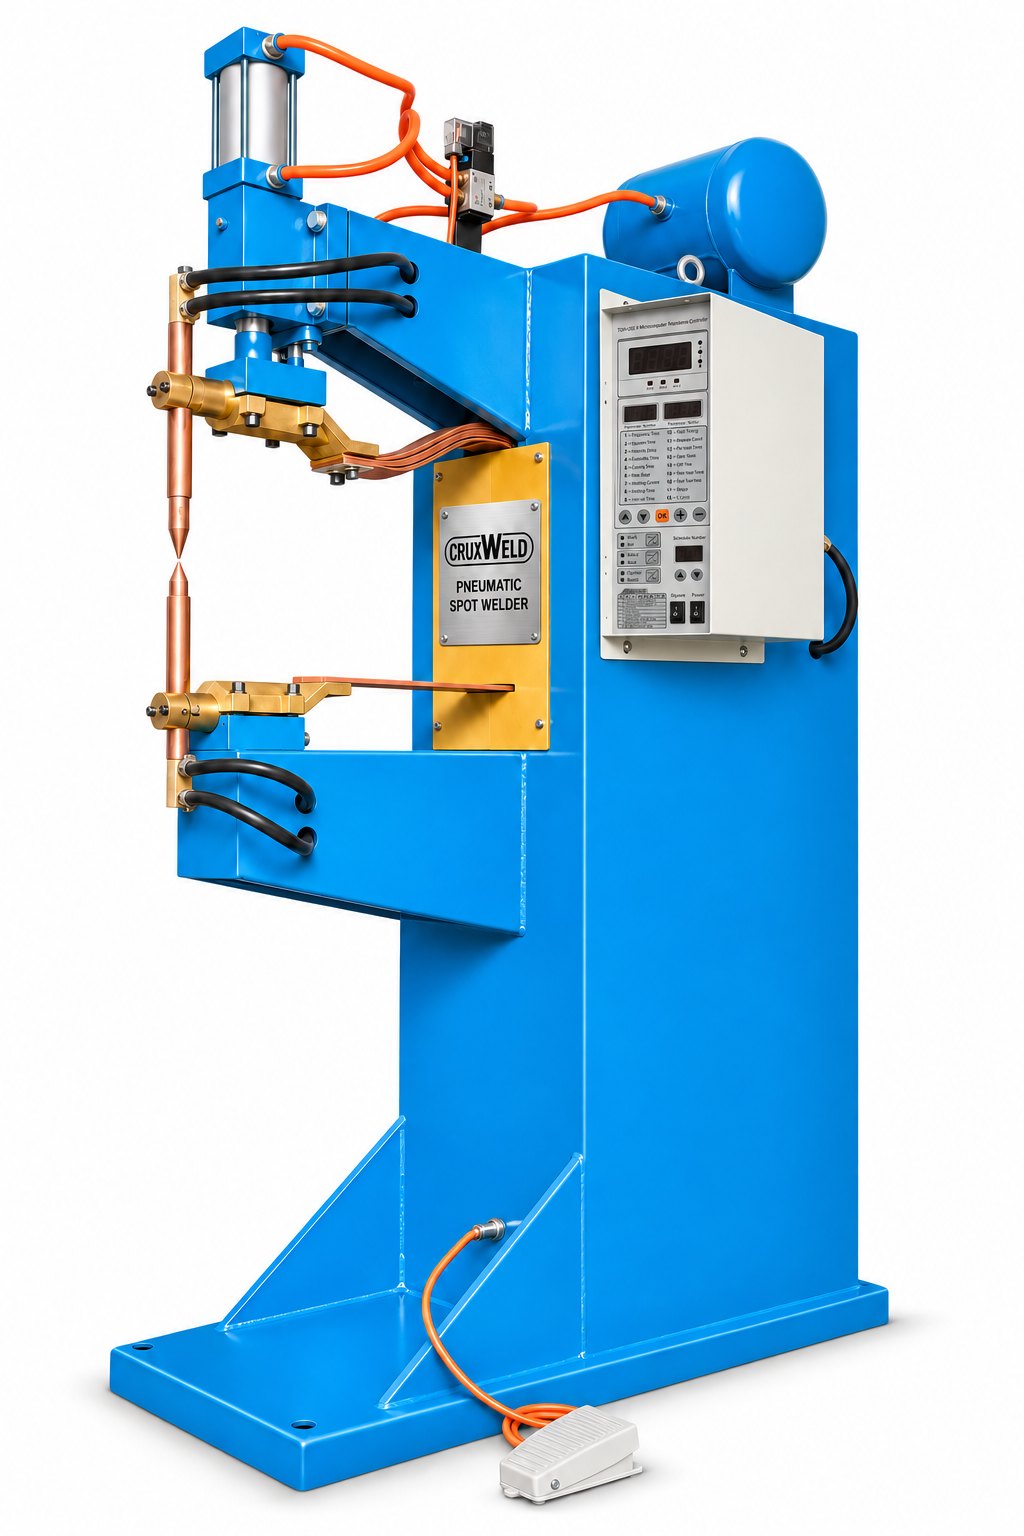
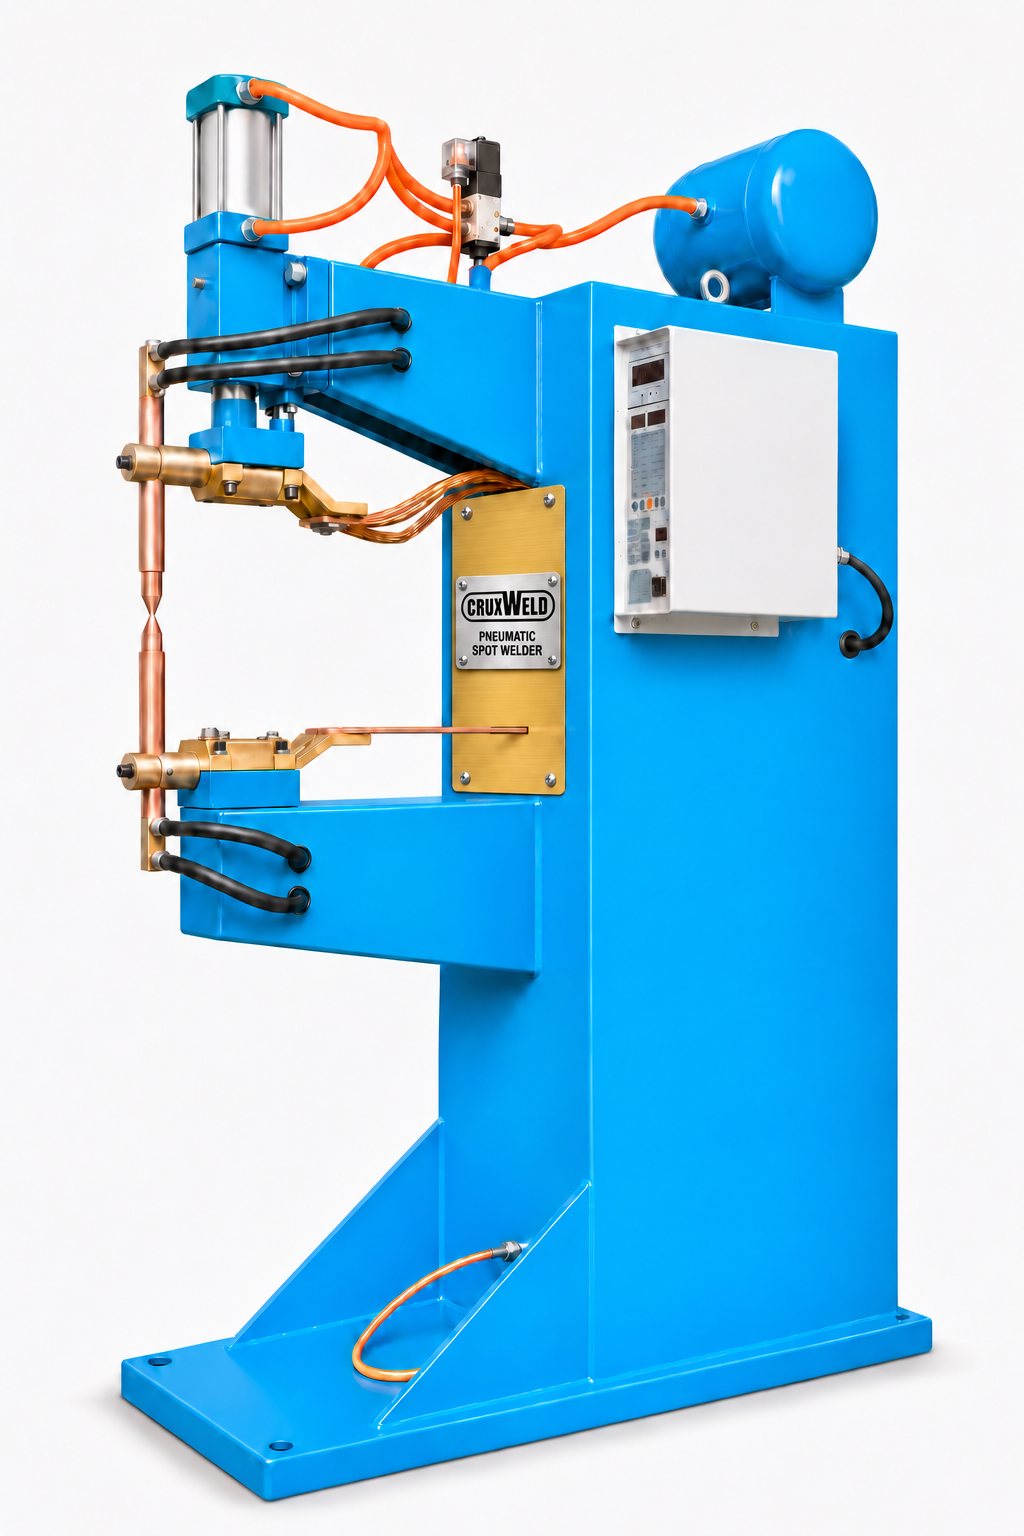
The CRUXWELD ProSpot 3500 is a 35 kVA pedestal pneumatic spot and projection welding machine for production shops. A pneumatic cylinder puts the same electrode force on every weld, a microcomputer controller times every stage of the cycle, and water-cooled arms keep it welding all shift. Flat, pointed and projection electrodes swap in minutes, so sheet, wire mesh, nuts and bolts all run on the one machine.

35 kVARated power
16,000 AMax welding current
3 + 3 mmMild steel capacity
6200 NElectrode force
🎮

Microcomputer controlSqueeze, weld, hold and off timed in cycles; 16 stored schedules
💨

Compressor and tank built inAir tank, solenoid valve and F.R.L. unit on the machine
💬

WhatsApp + video supportSettings and electrode advice from our technical team

Price, delivery & technical help — get a fast response.

Overview

How it works

Squeeze, weld, hold, release. The controller does the counting.

Resistance spot welding joins two sheets with pressure and current alone. The electrodes clamp the sheets, a high current flows through the small contact area for a few cycles, the metal melts into a nugget, and the force is held until it freezes. On a pedal machine the operator supplies the force and the timing; on the ProSpot 3500 the cylinder and the controller do both, so every weld on the shift looks like the first.

The ProSpot 3500 weld cycle: squeeze, weld, hold, releaseCRUXWELD16.0kA • Schedule 01SQUEEZEWELDHOLDOFFfoot pedal1. SQUEEZEPedal down. The cylinder brings theupper electrode onto the sheets andbuilds full force before any current.2. WELDCurrent flows for the set cycles, upto 16,000 A, and the sheets melttogether at one spot. No filler, no gas.3. HOLDForce stays on while the nuggetfreezes under pressure. Hold time iswhat gives the weld its strength.4. RELEASEElectrodes open, the part comes out,and in repeat mode the next weldstarts as soon as you move along.Why pneumatic mattersSame force on every weld, set once atthe regulator, not by how hard theoperator presses the pedal.
01

Set the scheduleChoose one of 16 stored schedules on the controller, or set squeeze, weld and hold cycles and the current for a new job. Adjust mode lets you close the electrodes with no current to check alignment.
02

Place the part, press the pedalThe sheets sit on the lower electrode. The foot pedal starts the cycle; the solenoid valve sends air to the cylinder and the upper electrode comes down with the force set on the regulator.
03

The machine welds and holdsCurrent flows for the set cycles, up to 16,000 A, then stops while the force stays on for the hold time. Pre-heat, slope up, slope down and temper current are there for coated and thicker sheet.
04

Release and move alongThe electrodes open and the part comes out. In repeat mode the machine runs the next cycle as soon as the pedal is pressed again, which is how mesh and long seams of spots get done fast.
Watch it work

Spot and projection welding on the ProSpot 3500

Play video
From the CRUXWELD Tech channel

One machine for spot and projection welding

Our technical team runs the ProSpot 3500 through sheet, mesh and nut welding, swaps the electrodes and walks through the controller settings.

  • Pneumatic head and foot-pedal cycle
  • Pointed, flat and projection electrodes
  • Setting squeeze, weld and hold on the controller
Walk around it

What is on the machine

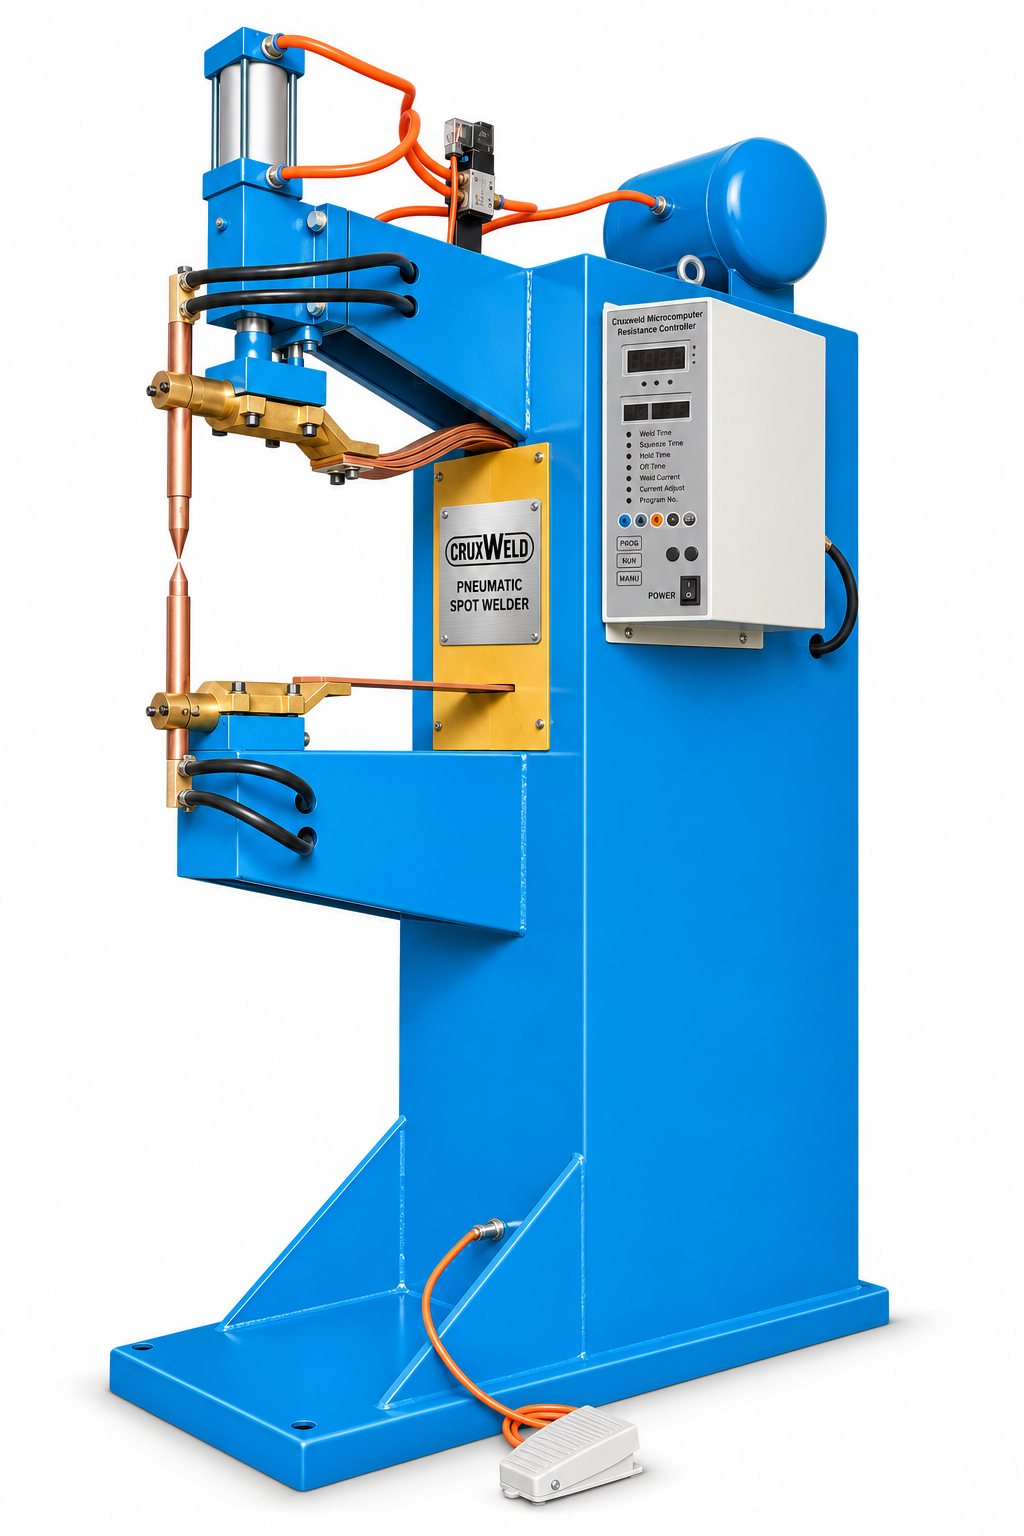
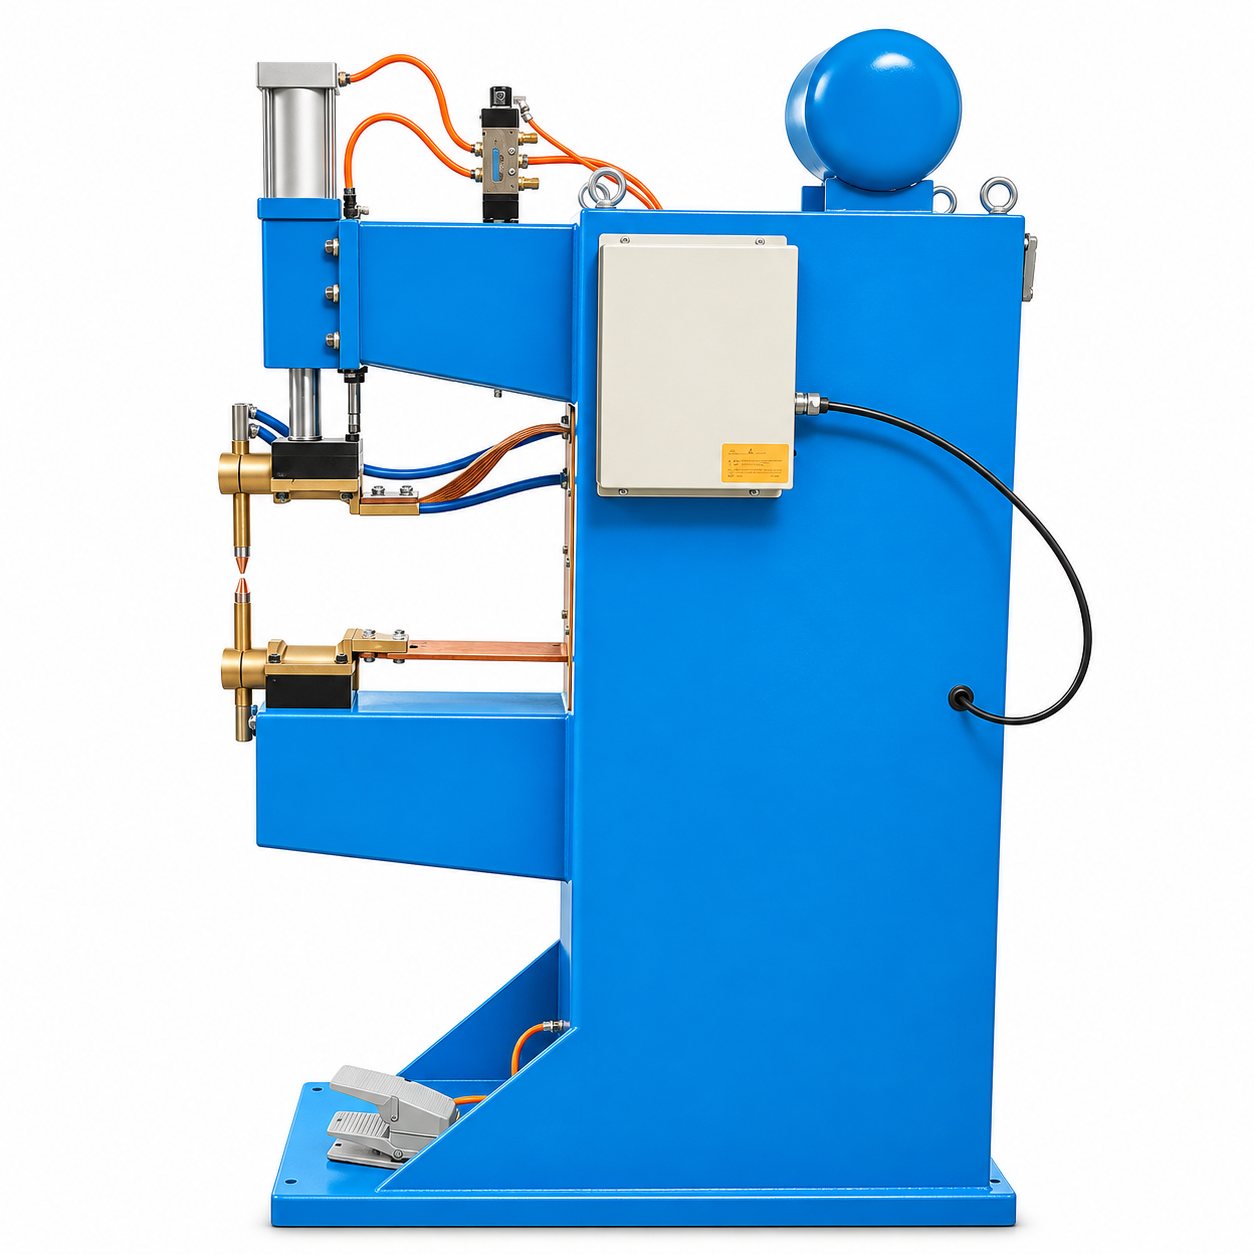
ProSpot 3500 pneumatic spot welding machine, side view, with pneumatic cylinder, air tank, controller and foot switch

Pneumatic cylinder
Solenoid valve
Compressed air tank
Weld controller
Water-cooled arms
Flexible copper shunt
Copper electrodes
Foot switch
Built for production

Everything a spot welder needs, on one base

The transformer sits in the steel column; the arms, cylinder, air tank, filter-regulator-lubricator unit and controller are all mounted on it. Connect power, water and the drain line, and it is ready to run.
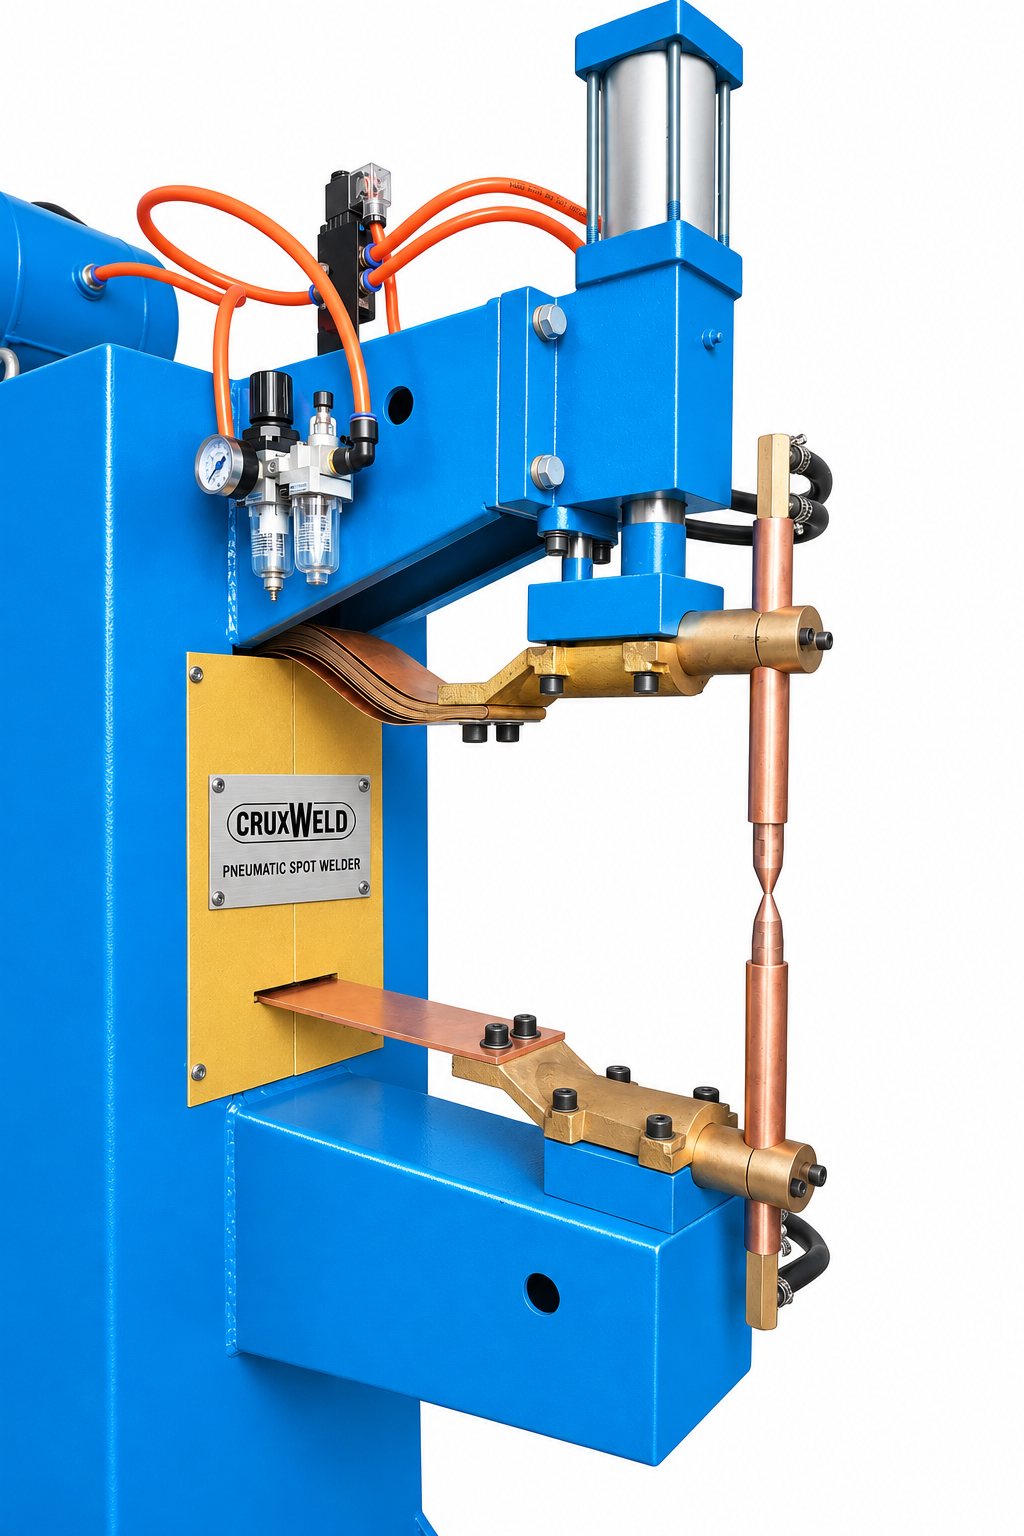
  • Pneumatic cylinder with 60 mm stroke, solenoid valve and inbuilt compressor with air tank
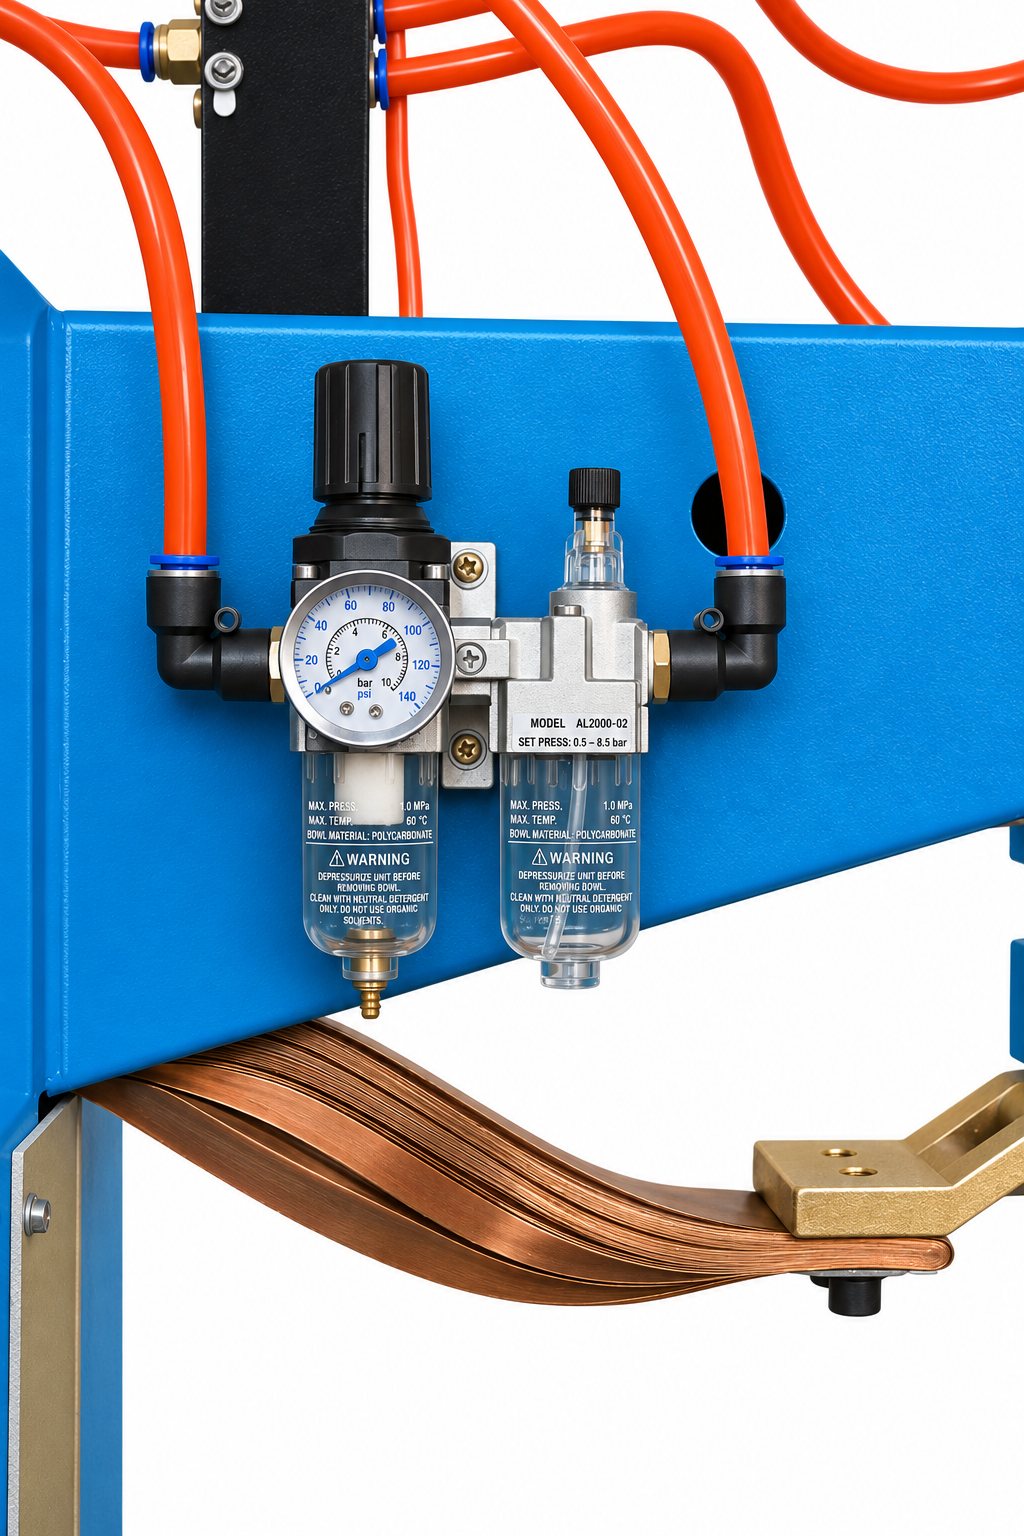
  • F.R.L. unit: filters the air, sets the electrode force, oils the cylinder
  • Water-cooled electrode holders and arms, 50 mm arm diameter, 25 mm holders
  • Lifting eyes on top; 350 kg, 940 × 640 × 1560 mm
  • Microcomputer resistance weld controller in its own enclosure on the column
380 V50 / 60 Hz, 35 kVA
0.5 MPaair, from the inbuilt tank
3.5 L/mincooling water, minimum
940 × 640mm floor space
Why fabricators pick it

What makes the ProSpot 3500 a production machine

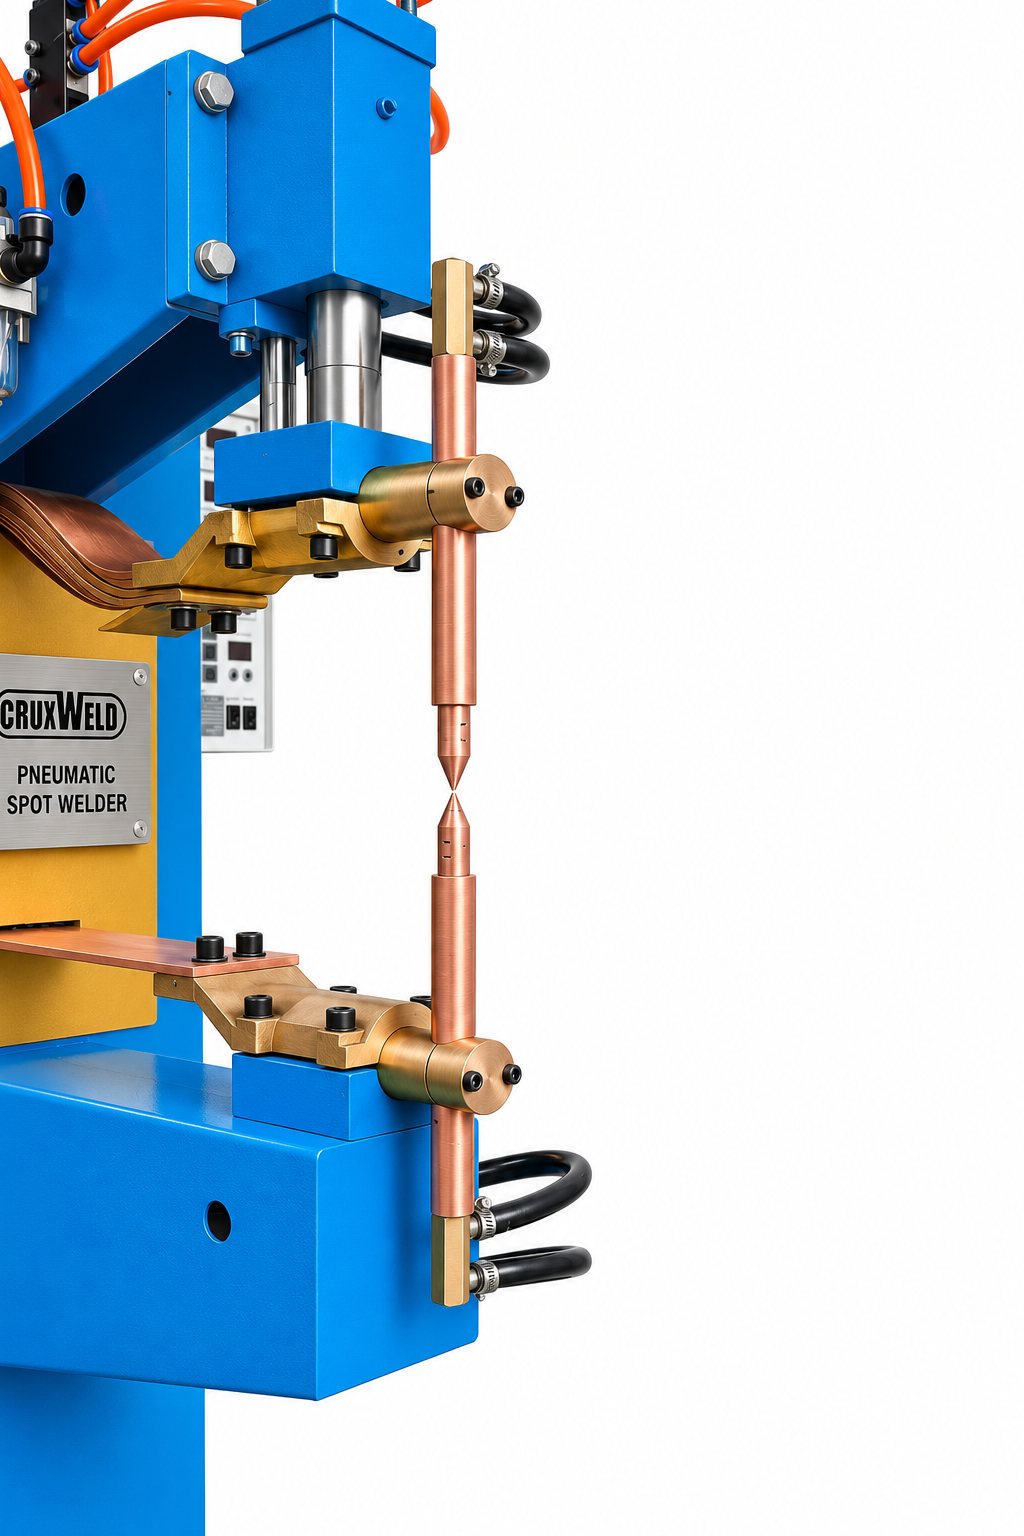
ProSpot 3500 pneumatic spot welder: Constant force, set at the regulator
Pneumatic head

Constant force, set at the regulator

A pneumatic cylinder on the upper arm brings the electrode down with the same force every time, up to 6200 N. Nugget size stops depending on who is on the pedal, which is what makes spot welds repeatable enough for inspection.
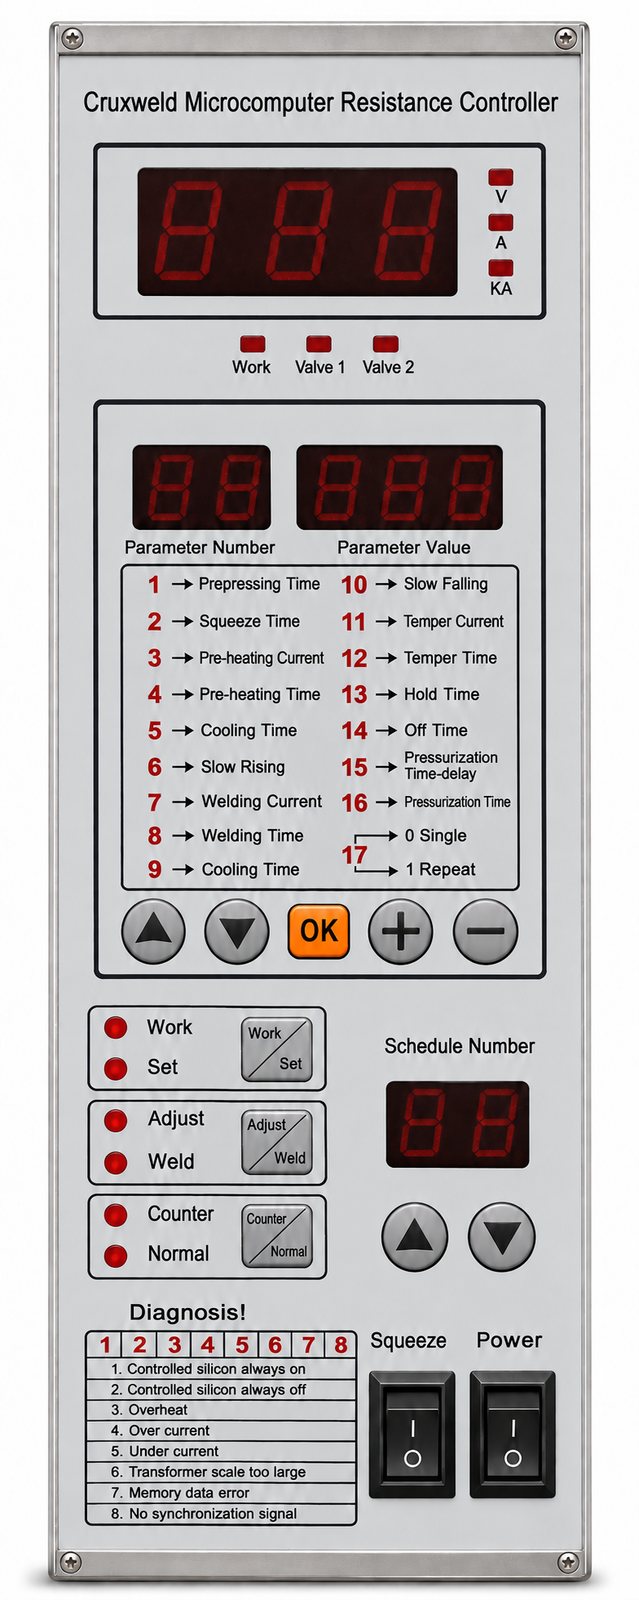
ProSpot 3500 pneumatic spot welder: Every stage timed in cycles
Microcomputer controller

Every stage timed in cycles

Seventeen parameters cover pre-pressing, squeeze, pre-heat, slope up, weld, slope down, temper and hold, all counted in mains cycles. Sixteen schedules are stored, a counter logs the welds, and a fault code tells you why it stopped.
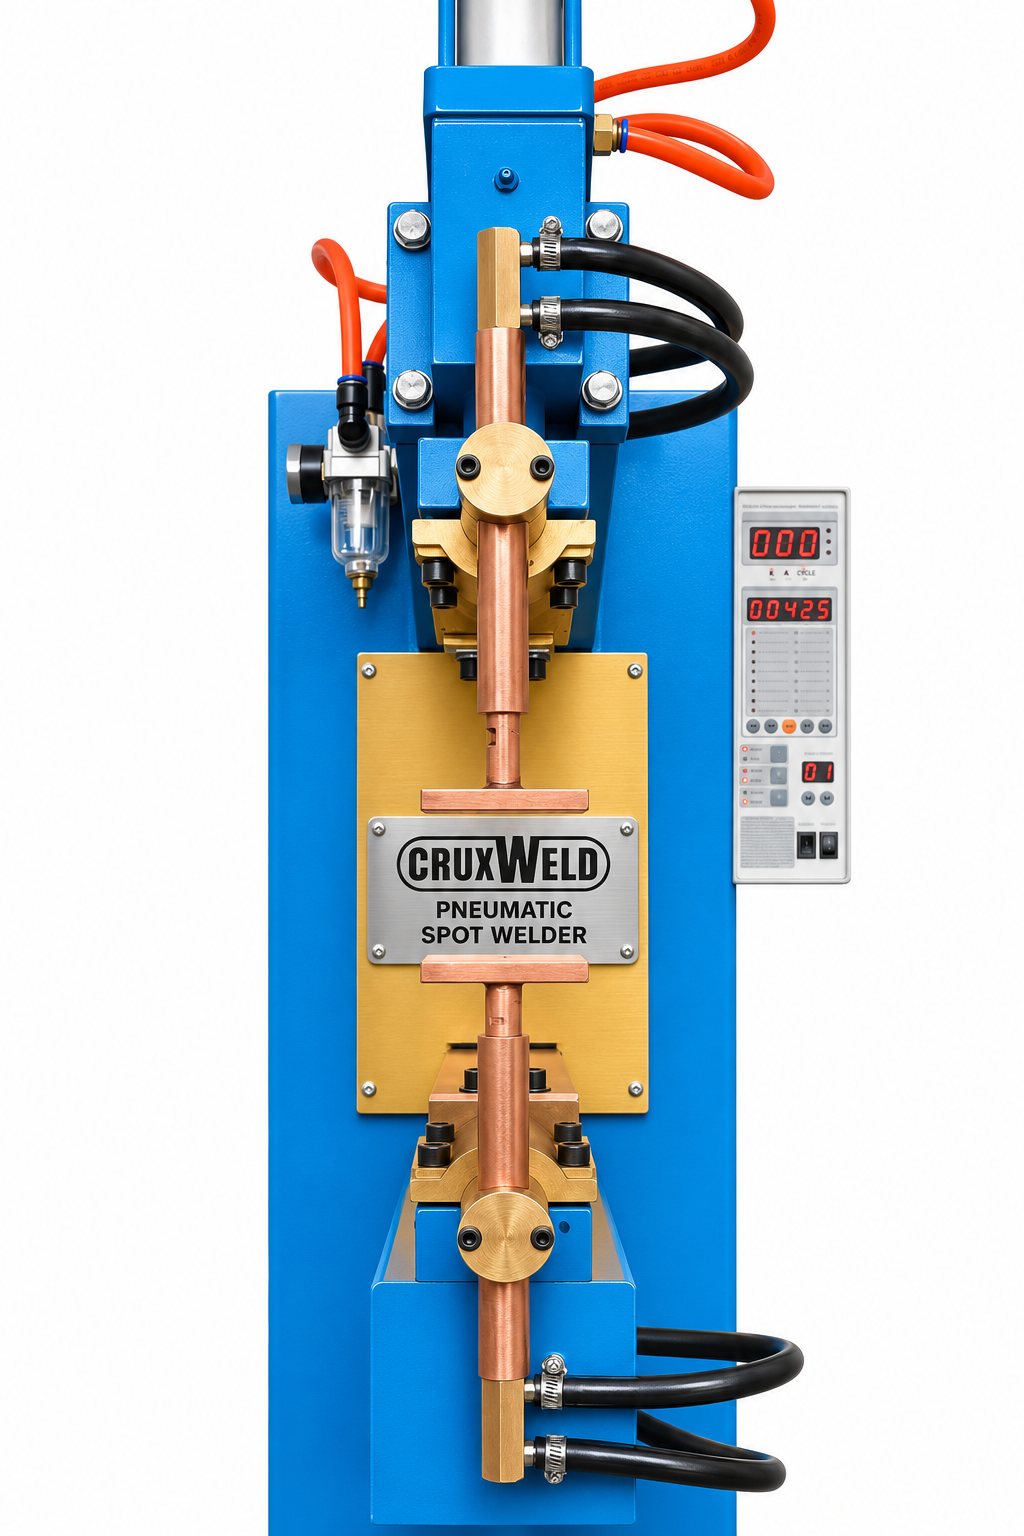
ProSpot 3500 pneumatic spot welder: Pointed, flat or projection dies
Interchangeable electrodes

Pointed, flat or projection dies

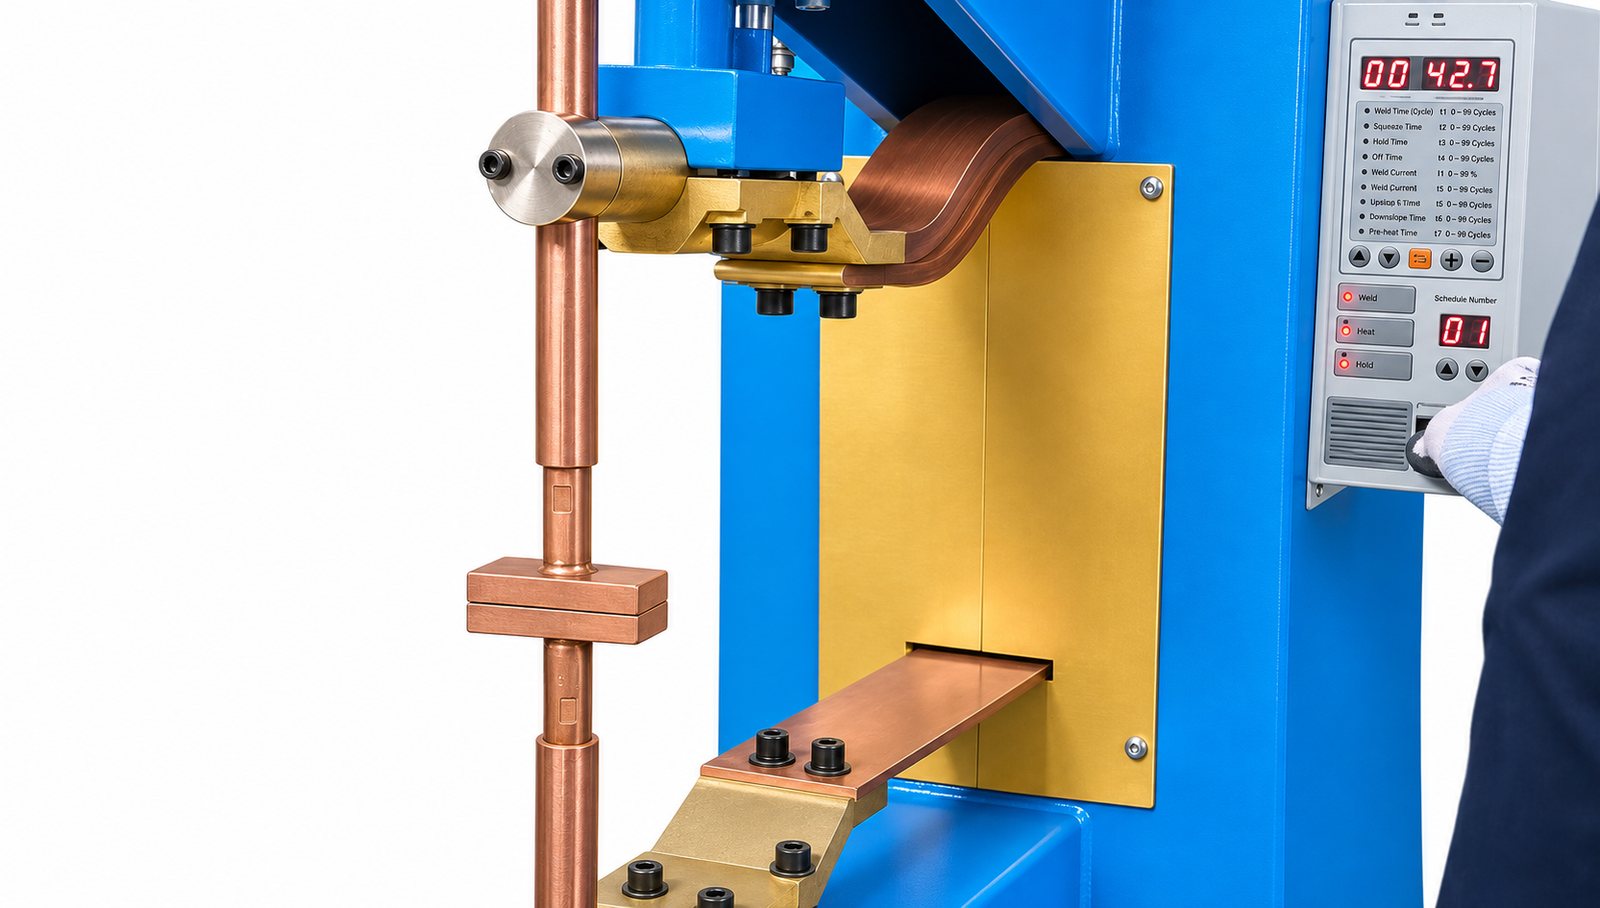
Standard 25 mm holders take pointed tips for sheet, flat bars for wire and mesh, and die sets for nuts and bolts. Changing over is a matter of loosening the holder clamps.
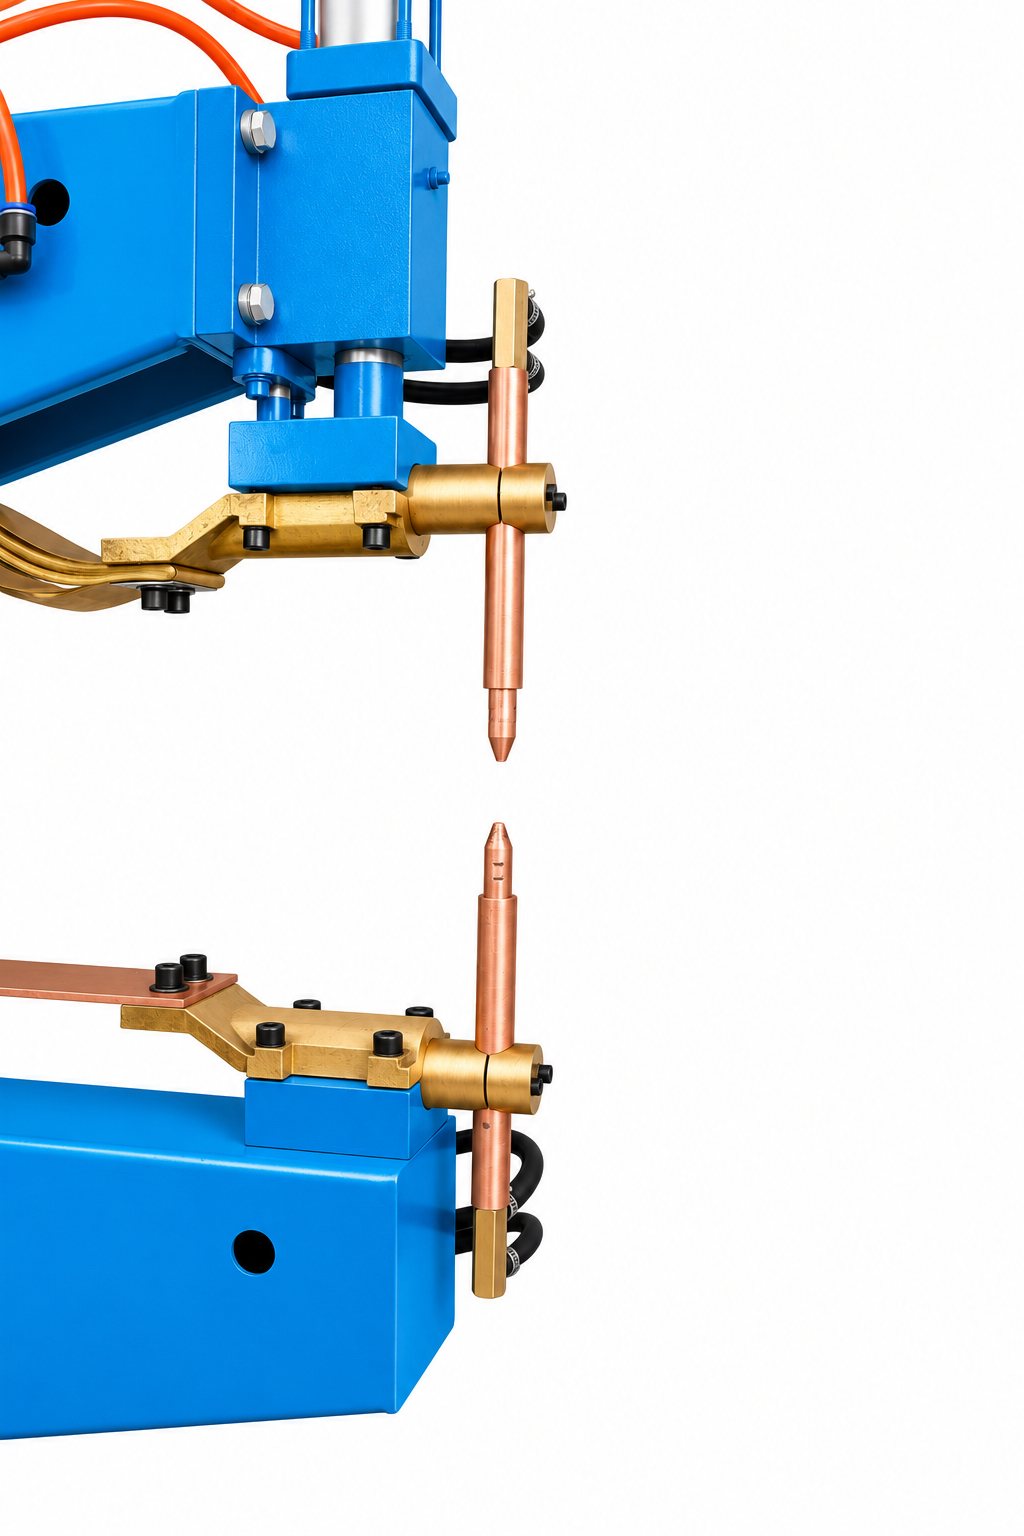
ProSpot 3500 pneumatic spot welder: Keeps welding all shift
Water-cooled arms

Keeps welding all shift

Cooling water runs through both electrode holders and arms at 3.5 litres a minute or more. Tips stay hard, the transformer stays cool and the machine keeps its rating through a full shift of repeat welds.
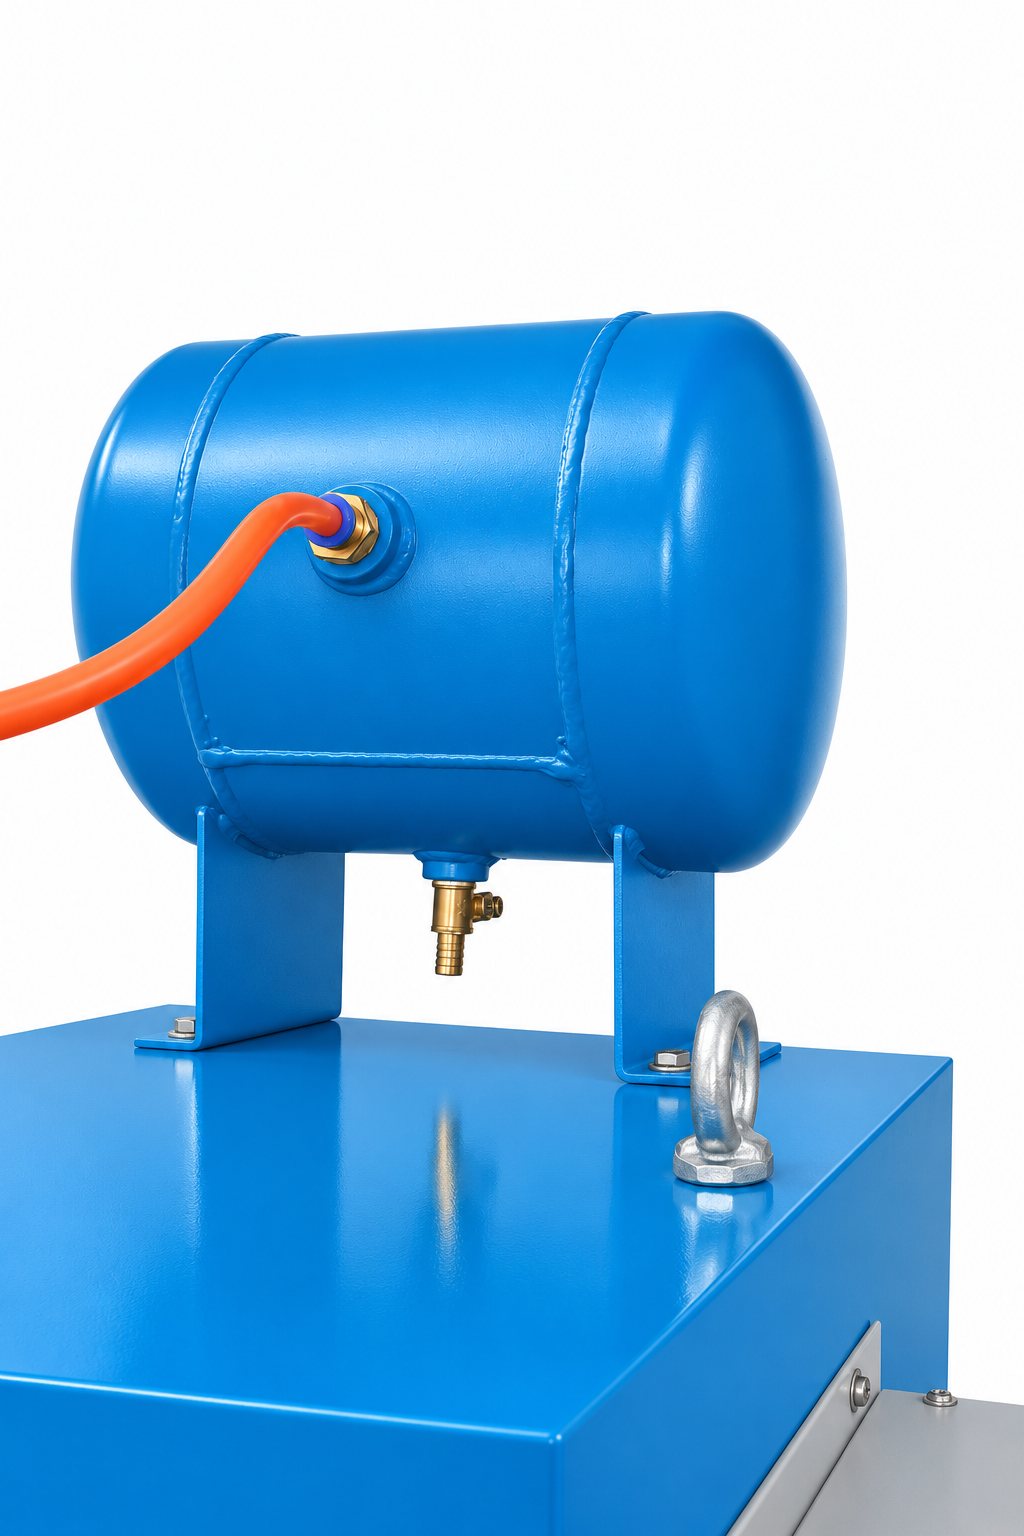
ProSpot 3500 pneumatic spot welder: No shop air line needed
Compressor and air tank built in

No shop air line needed

The air tank on top of the column stores compressed air for the cylinder, so pressure is steady from one weld to the next even on fast repeat work. A drain valve under the tank takes the condensate out.
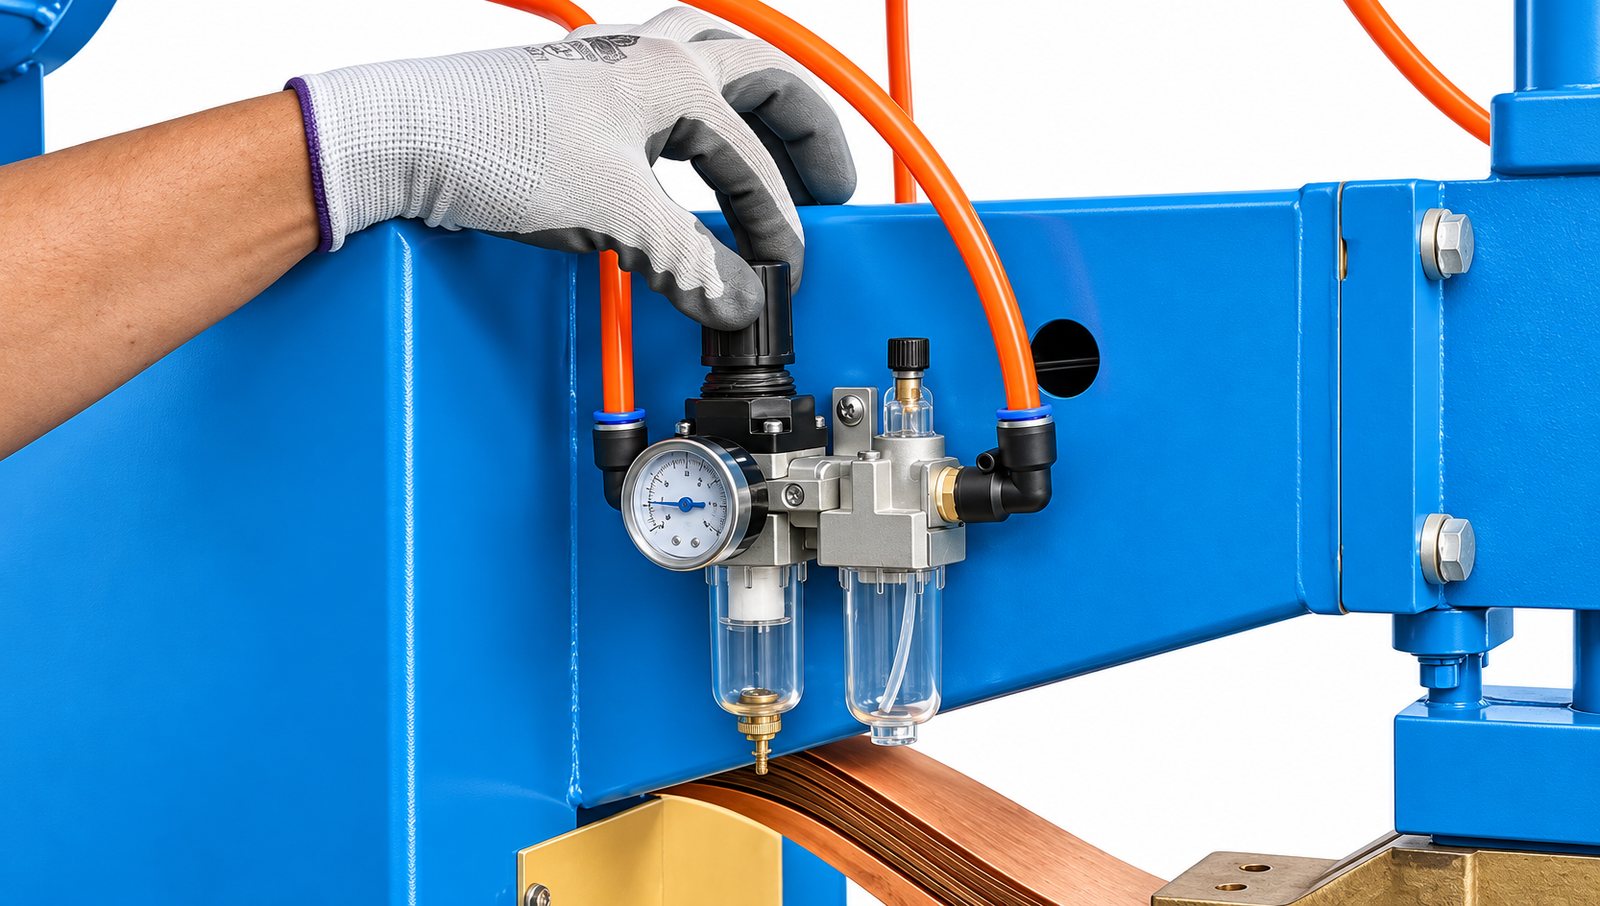
ProSpot 3500 pneumatic spot welder: Clean air, set pressure, oiled cylinder
F.R.L. unit

Clean air, set pressure, oiled cylinder

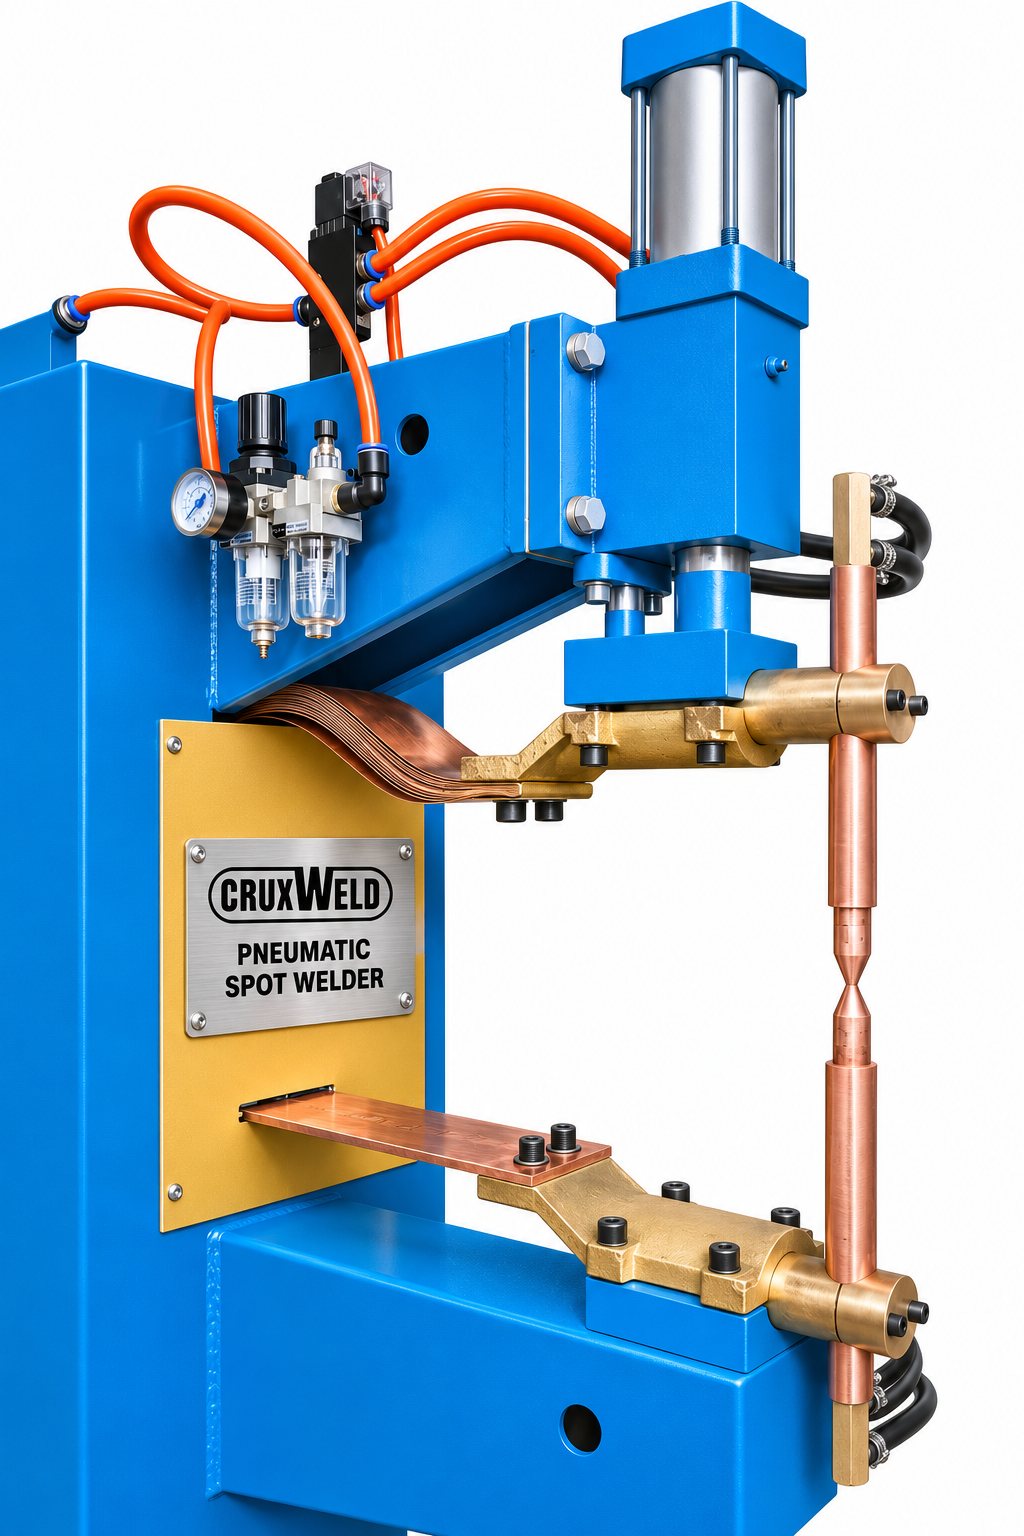
The filter-regulator-lubricator on the arm housing cleans the air, sets the working pressure (0.5 MPa input) and mists oil into the cylinder. The gauge on it is where electrode force is dialled in.

At a glance

The four numbers that matter

35 kVA

16,000 A maximum welding current, 15 kA short-circuit.

3 mm + 3 mm

Mild steel sheet, two layers, in one spot.

6200 N

Maximum electrode force from the pneumatic cylinder.

Water cooled

Arms and holders, 3.5 L/min or more, insulation class H.

Electrode guide

Three electrode set-ups, one machine

The arm and holder geometry stays the same; only the copper at the tip changes. That is why one ProSpot 3500 covers sheet-metal, wire products and fastener welding in the same shop.
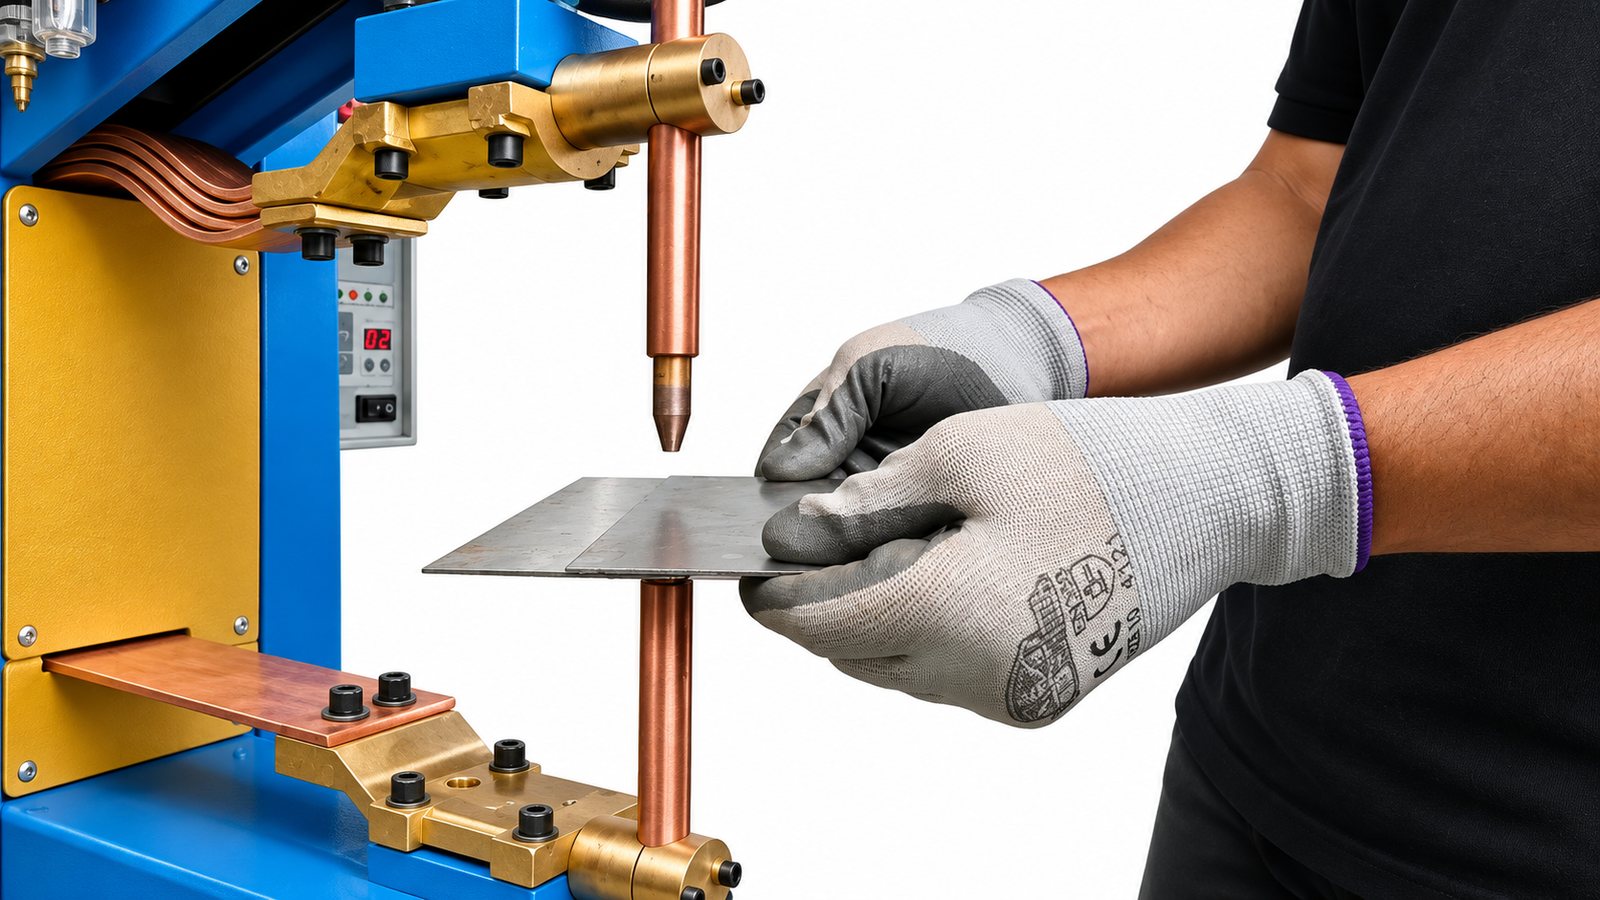
ProSpot 3500 pneumatic spot welder: Sheet to sheet

Pointed tips

Sheet to sheet

Standard spot welding of two sheets up to 3 mm each: enclosures, brackets, panels, ducting. The pointed tip concentrates current into one nugget.
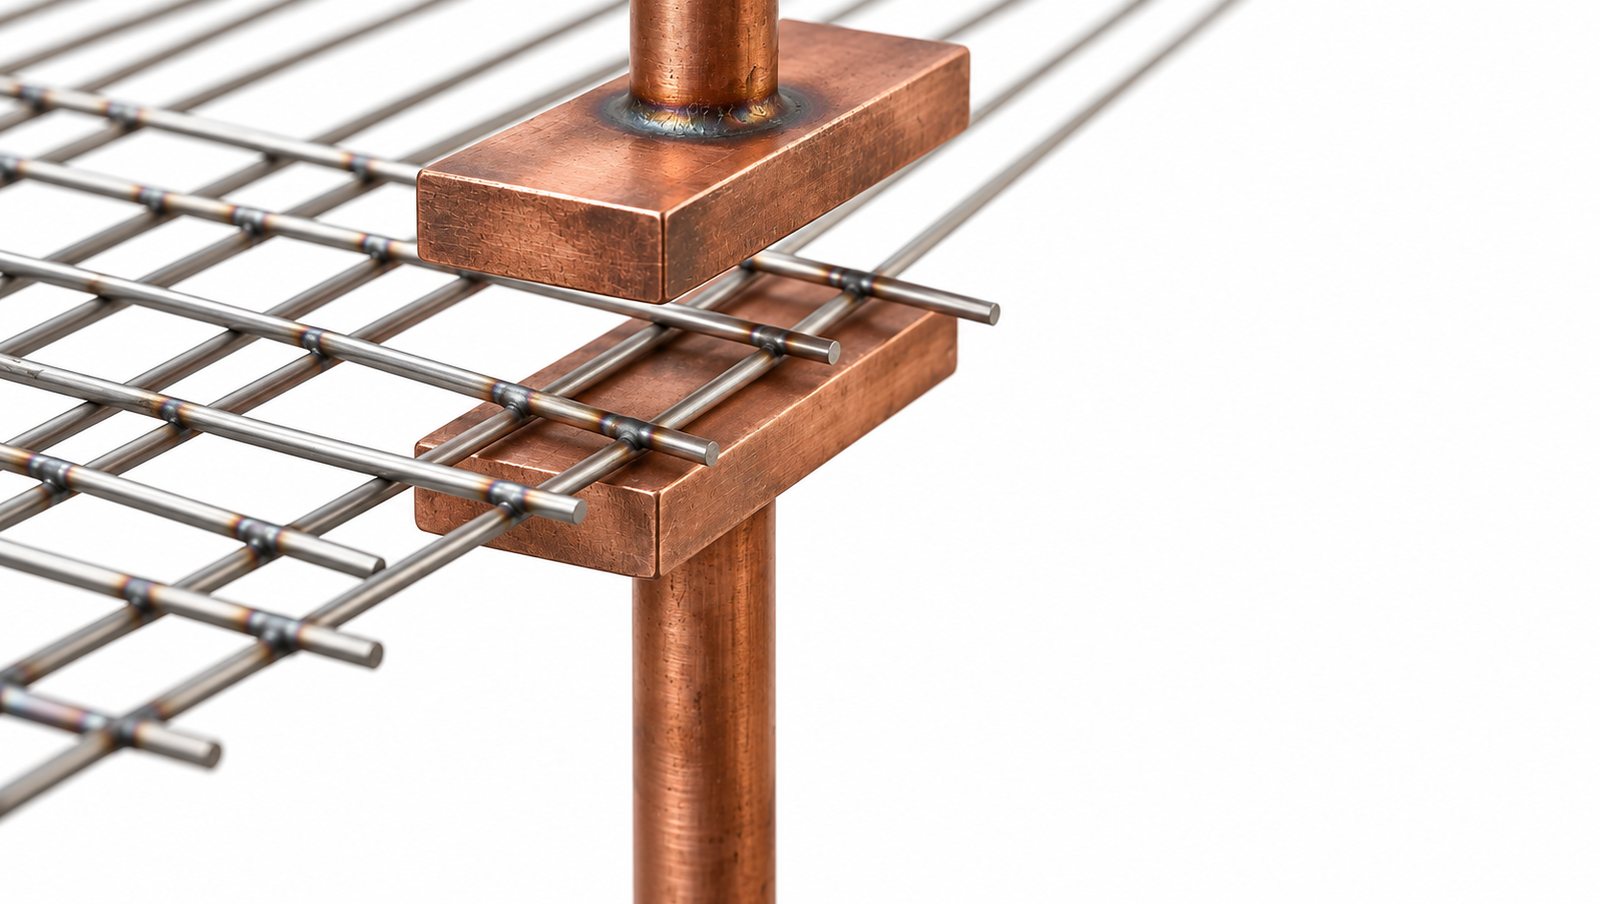
ProSpot 3500 pneumatic spot welder: Wire, rod and mesh

Flat electrodes

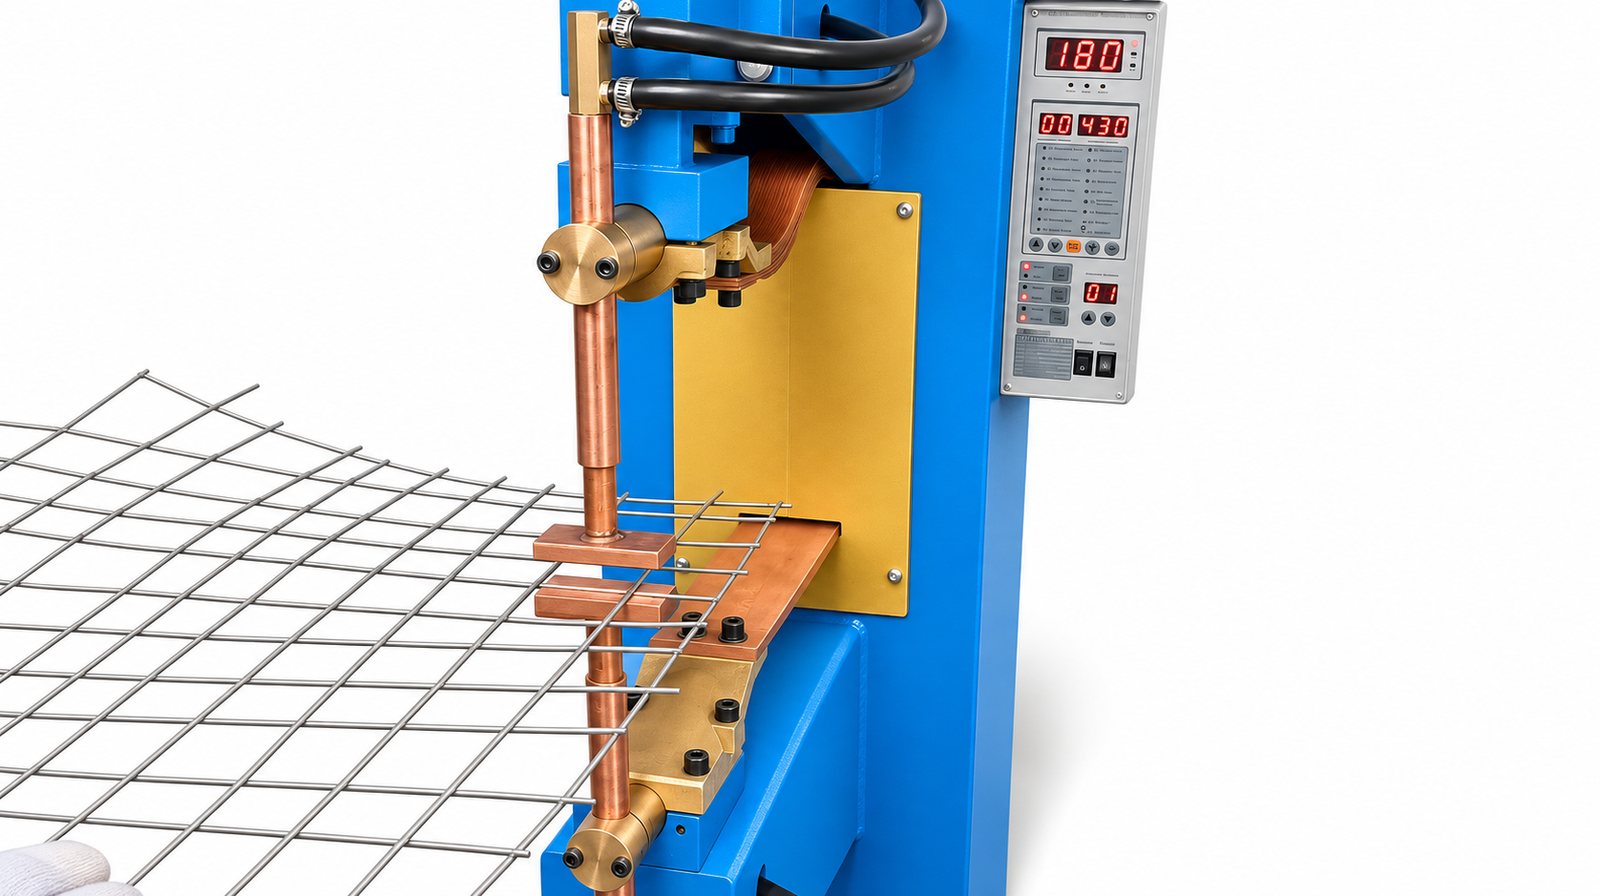
Wire, rod and mesh

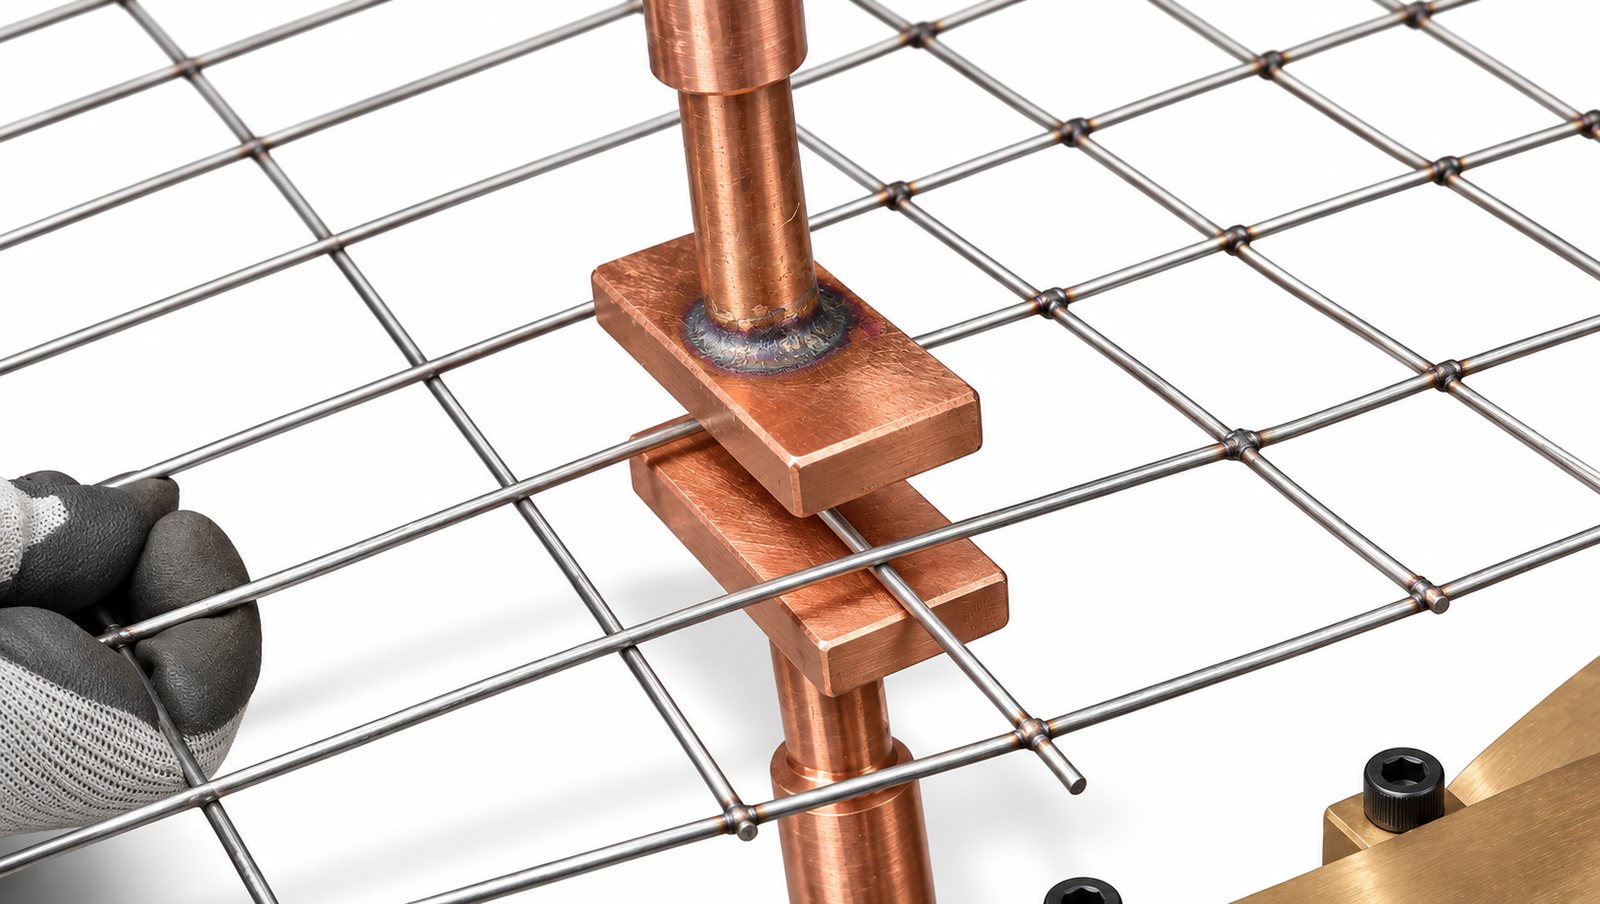
Broad flat bars spread the force over crossing wires, so several wires can be welded in one press. Mesh panels, baskets, grills and trays.
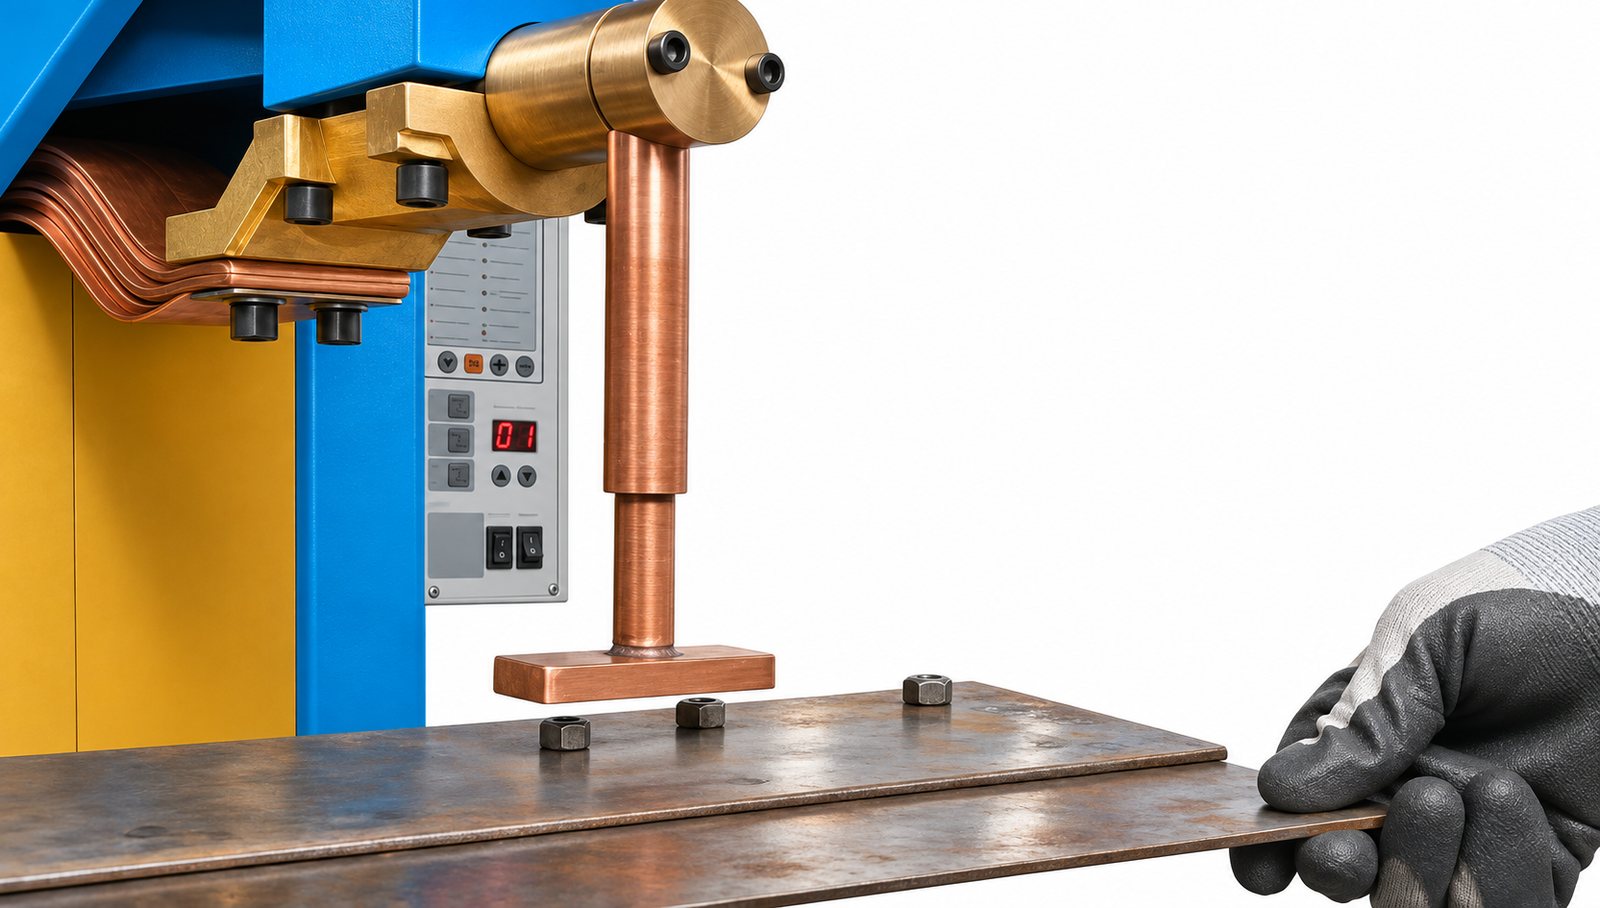
ProSpot 3500 pneumatic spot welder: Nuts, bolts and studs

Projection dies

Nuts, bolts and studs

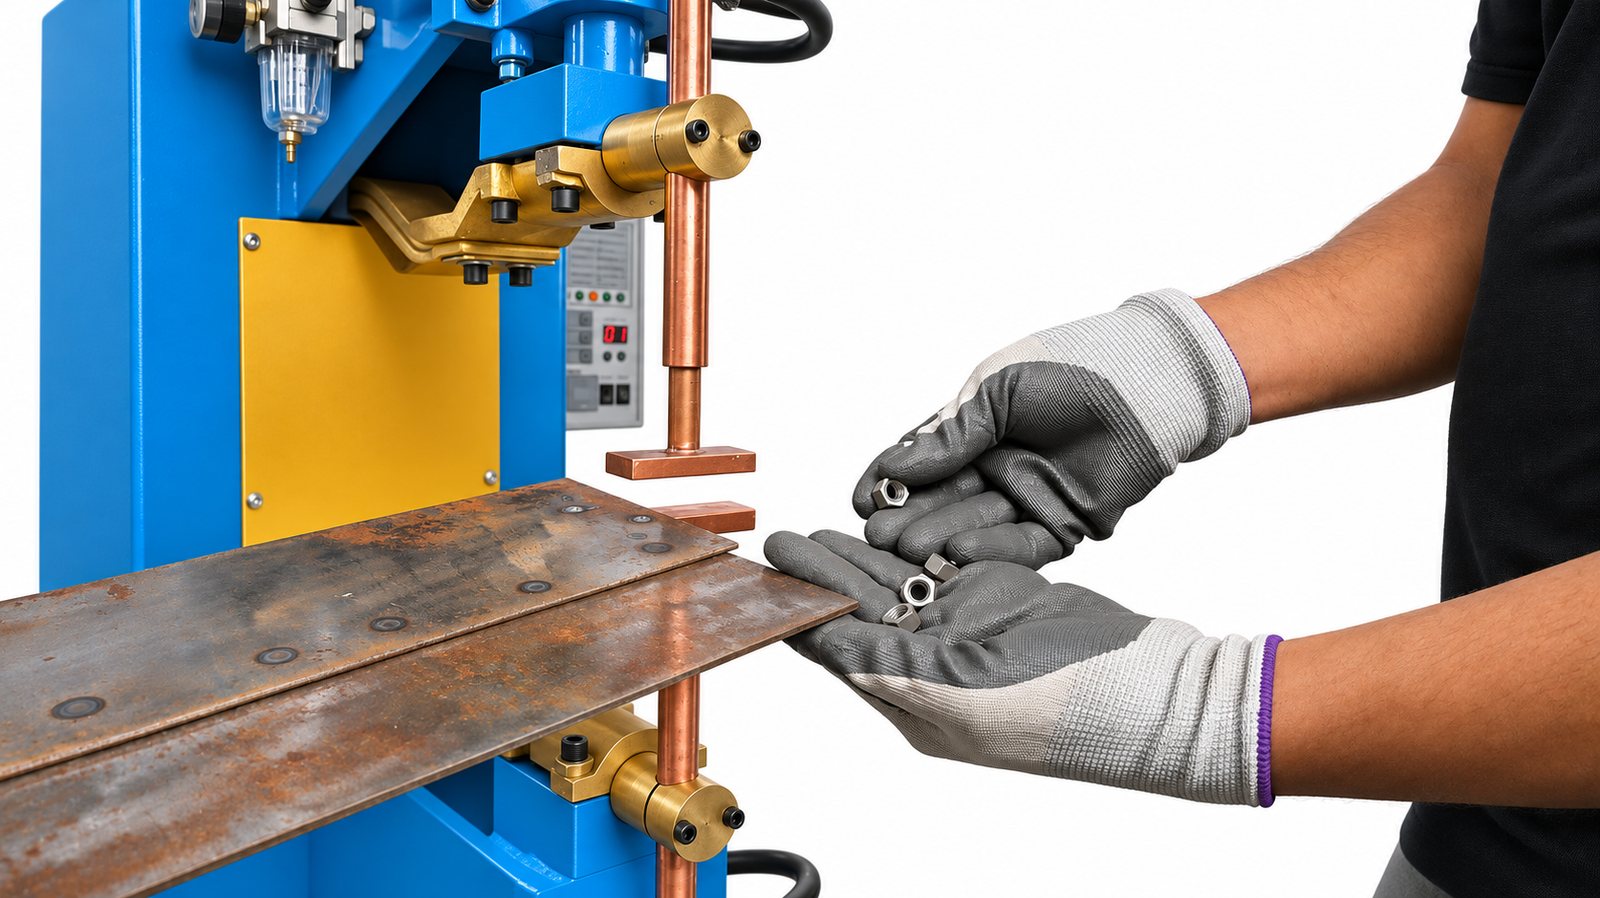
The projections on a weld nut carry the current, so a flat die welds the nut to the sheet in one shot without marking the show face. Needs a die set for the fastener.
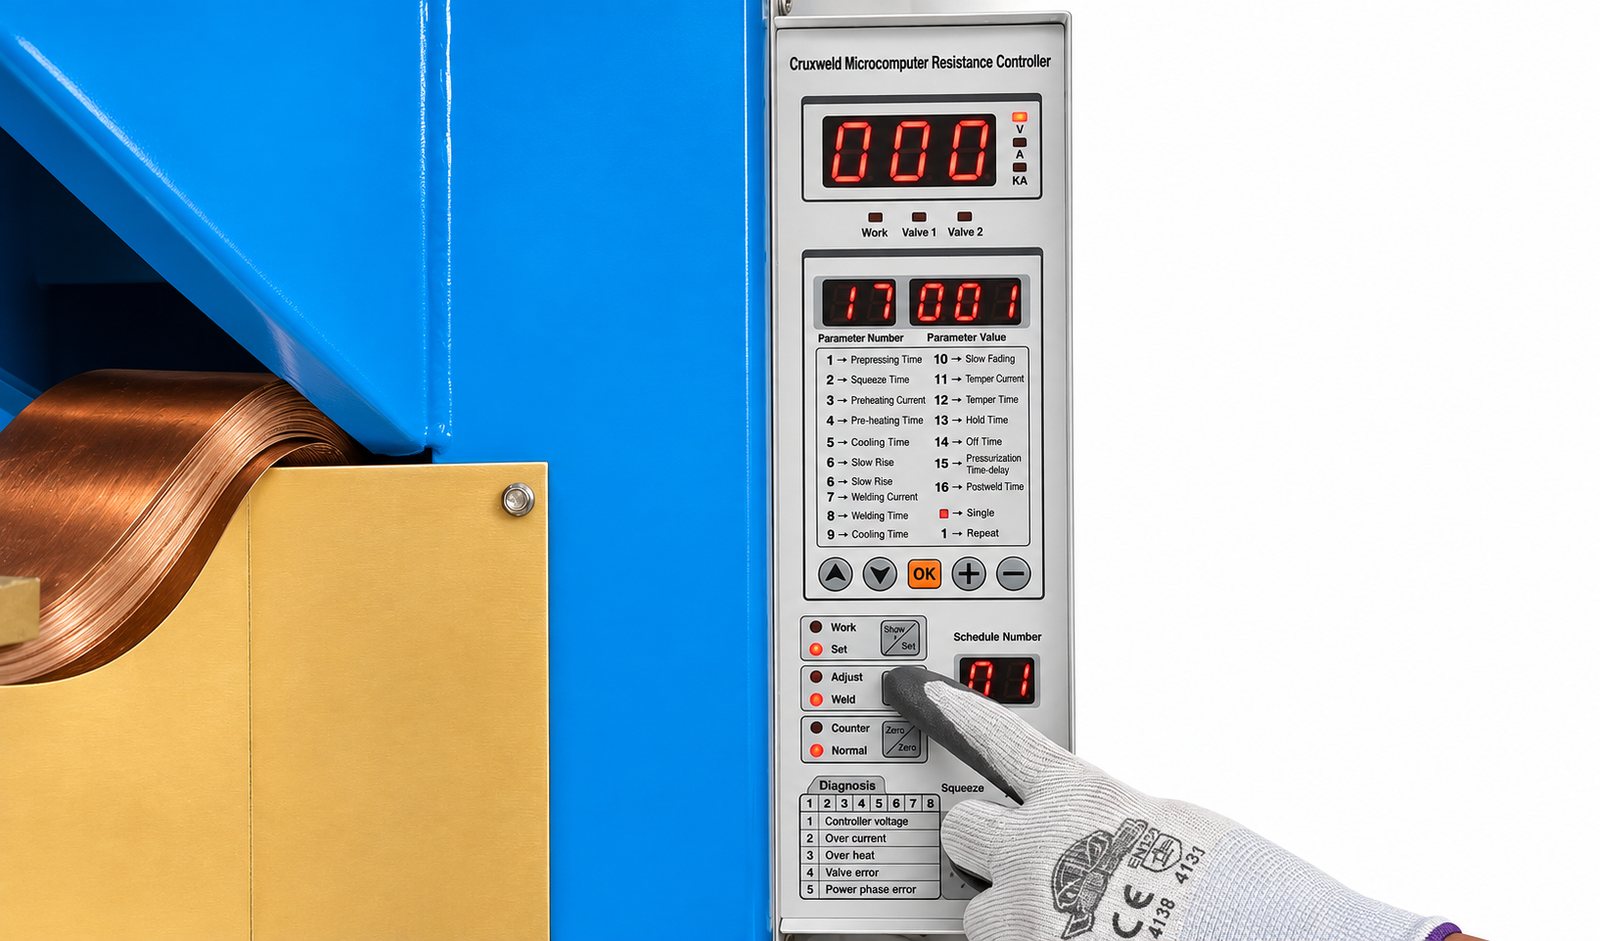
The controller

Set it in cycles, store it, repeat it

Setting a parameter on the ProSpot 3500 microcomputer resistance weld controller

Cruxweld microcomputer resistance controller

Two displays: the top one shows welding current or voltage, the lower pair shows the parameter number and its value. Press the pedal in Work mode and the stored schedule runs; switch to Set mode to edit it.

  • 17 parameters: pre-pressing, squeeze, pre-heat current and time, cooling, slow rise, weld current and time, slow fall, temper current and time, hold, off, pressurisation delay and time, single or repeat
  • 16 stored schedules, selected by number on the panel
  • Constant-current or constant-voltage control: the controller corrects the firing angle so current stays where you set it as the mains and the arms heat up
  • Adjust mode closes the electrodes without current, for lining up tips and fixtures
  • Weld counter for production tally; eight fault codes with automatic shutdown (silicon on or off, overheat, over or under current, no sync)
  • Single and repeat welding; squeeze switch on the panel for manual clamping
Up close

Every angle

ProSpot 3500 pneumatic spot welder: Front, pointed tipsFront, pointed tips
ProSpot 3500 pneumatic spot welder: Controller on the columnController on the column
ProSpot 3500 pneumatic spot welder: Flat electrodes fittedFlat electrodes fitted
ProSpot 3500 pneumatic spot welder: F.R.L. unit and copper shuntF.R.L. unit and copper shunt
ProSpot 3500 pneumatic spot welder: Flat bars on wire meshFlat bars on wire mesh
ProSpot 3500 pneumatic spot welder: Loading weld nutsLoading weld nuts
ProSpot 3500 pneumatic spot welder: Several wires in one pressSeveral wires in one press
What comes off it

Parts our customers weld on the ProSpot 3500

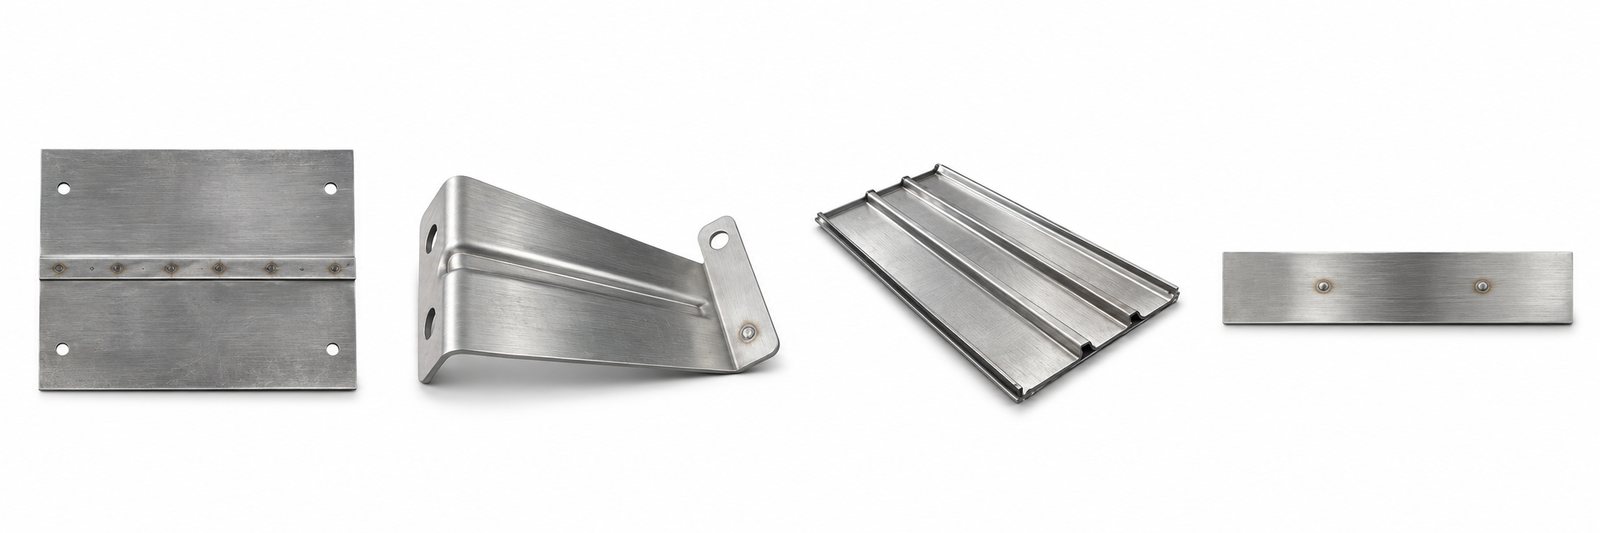
Spot welded sheet brackets, panels and traysSheet brackets, panels and trays
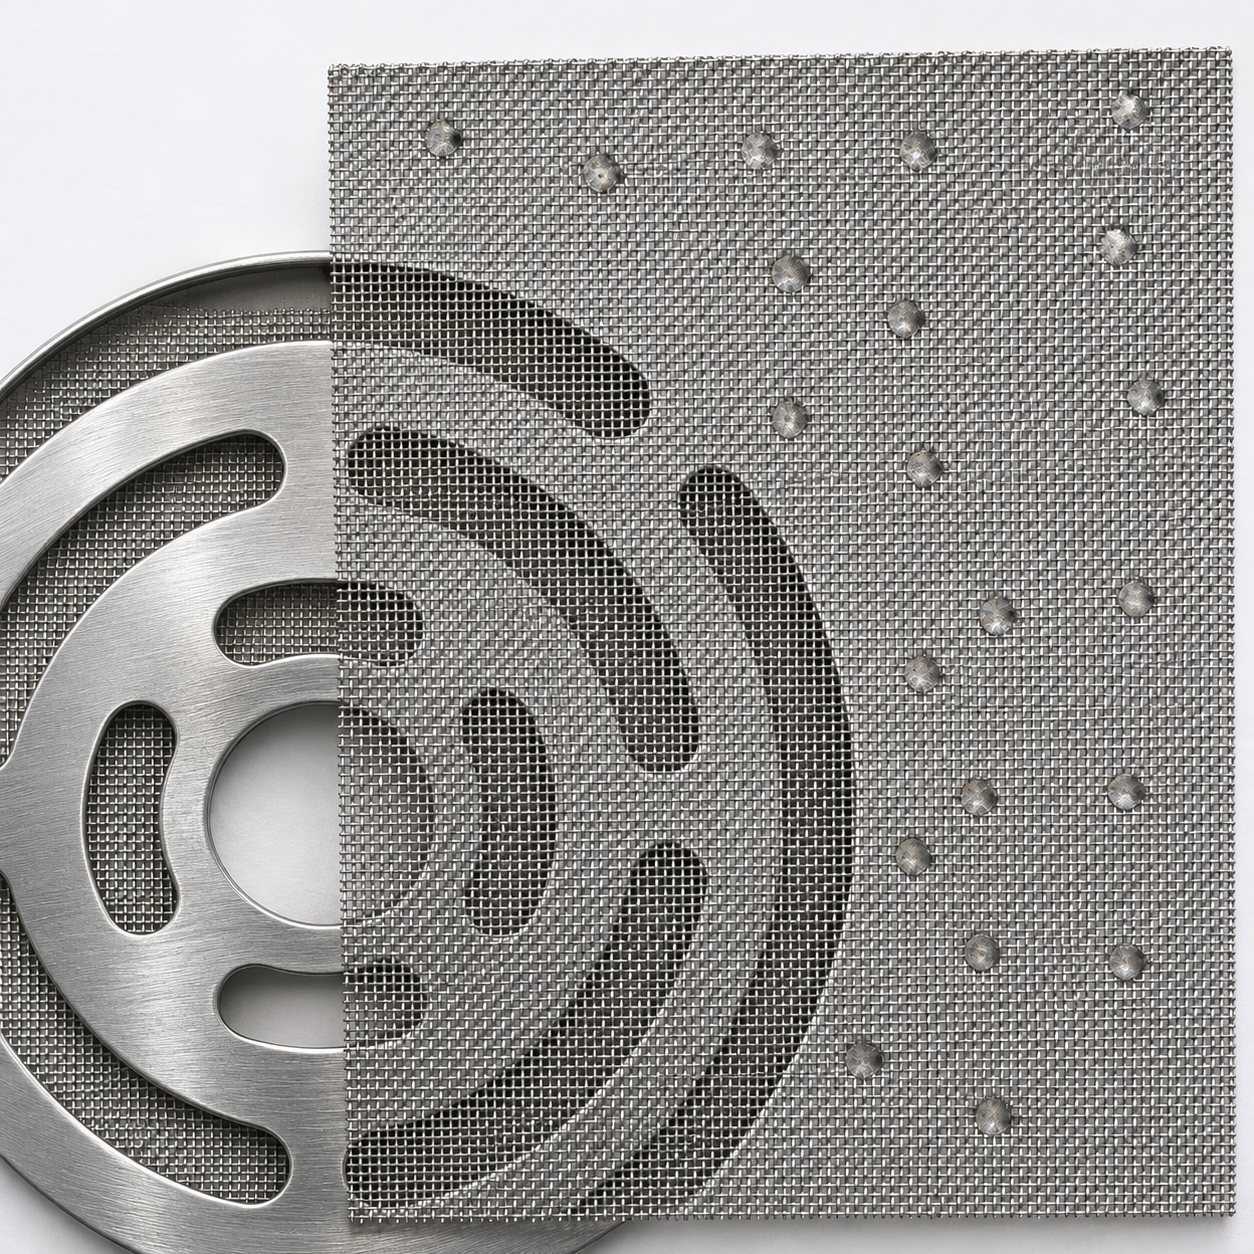
Spot welded mesh and perforated sheetMesh and perforated sheet
Spot welded wire grills and basketsWire grills and baskets
Applications

Where a 35 kVA pneumatic spot welder earns its keep

📦

Sheet-metal enclosuresControl panels, cabinets and ducting in 1 to 3 mm CRCA and GI.
🧺

Wire mesh and basketsStorage baskets, fryer baskets, grills and display racks with flat electrodes.
🔧

Weld nuts and studsProjection welding of M6 to M12 nuts onto brackets and chassis parts.
🚗

Automotive componentsBrackets, seat frames, exhaust shields and two-wheeler parts on repeat cycles.
🍴

Kitchen and stainlessSinks, hoods and trolleys in stainless sheet with timed, repeatable welds.
🪑

Furniture and racksSteel chairs, shelving and lockers where every spot must look the same.
Good practice

Getting consistent welds from it

Dress the electrode tips regularly; a mushroomed tip spreads the current and the nugget shrinks.
Set the electrode force at the F.R.L. regulator first, then set current and weld cycles; do not chase a weak weld with current alone.
Keep the cooling water flowing at 3.5 L/min or more whenever the machine is switched on, and drain the air tank daily.
Make a test weld and peel it: a good spot tears a slug out of one sheet instead of parting at the interface.
Use the Adjust mode to line up new electrodes or a fixture before switching to Weld.
Keep hands clear of the electrodes when the pedal is pressed; the cylinder closes with full force.
Pairs with

Round out the resistance welding line

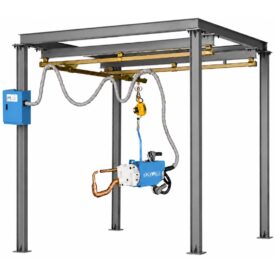
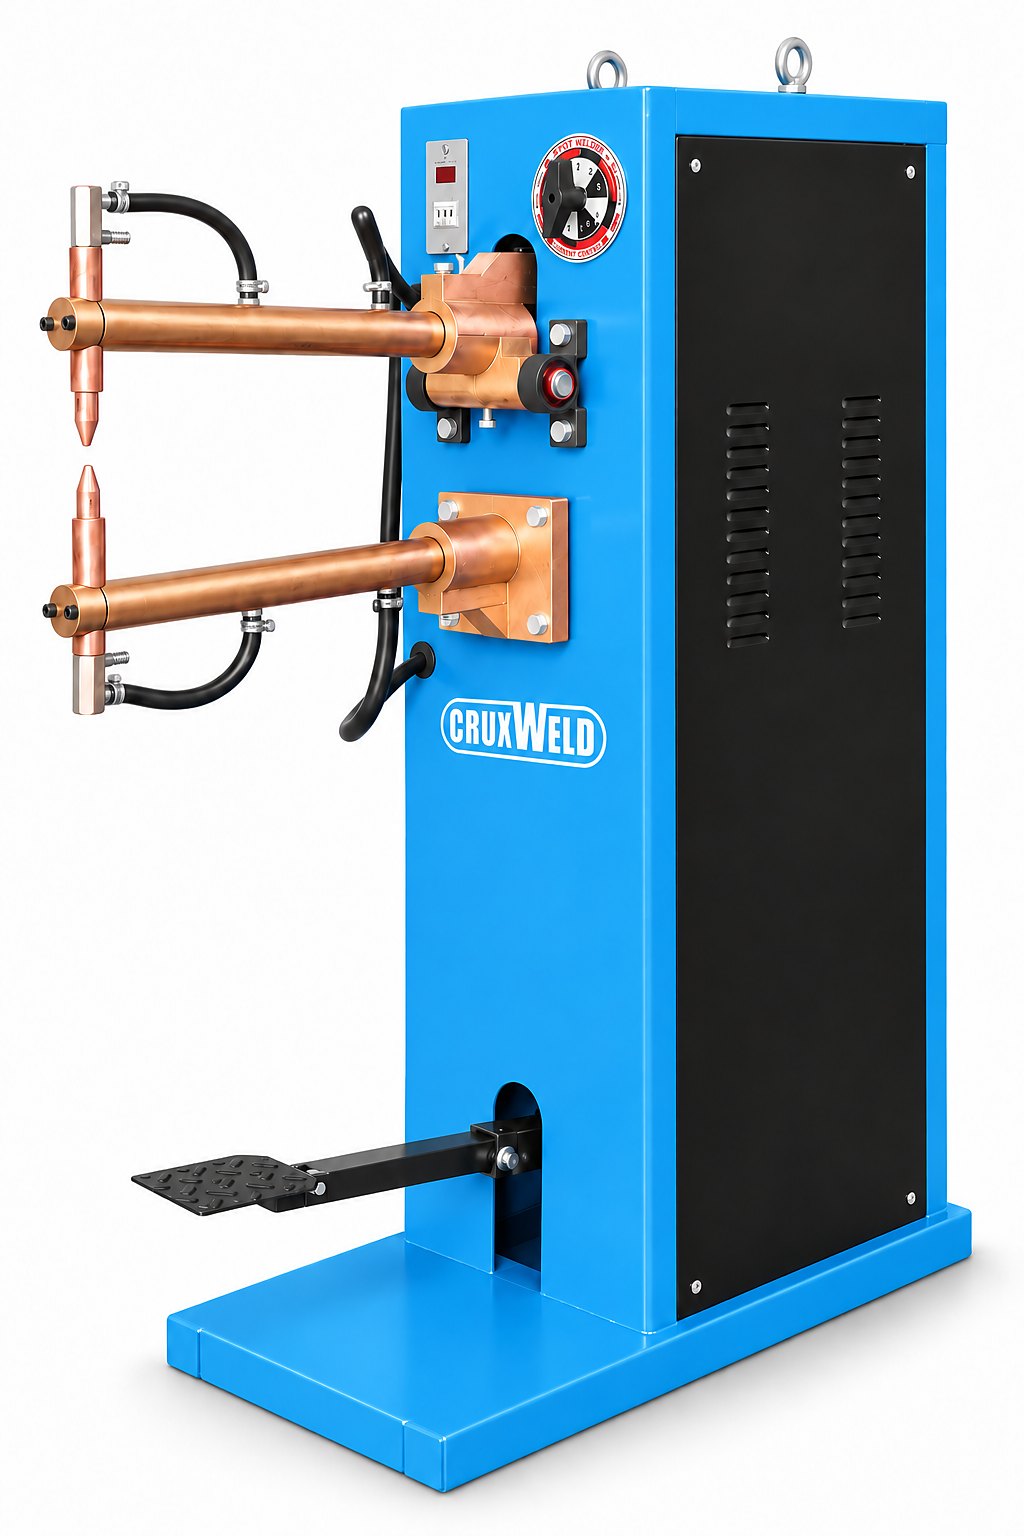
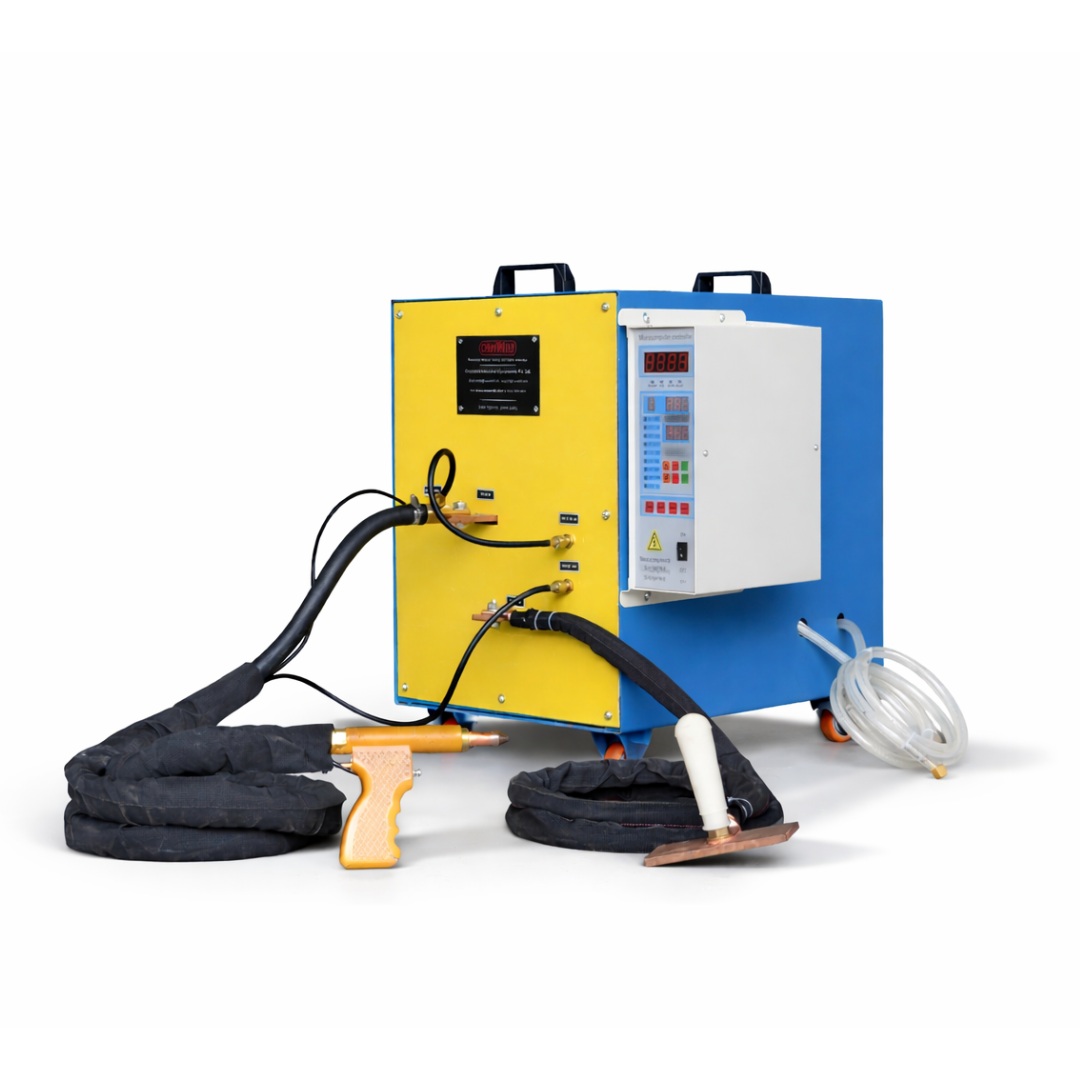
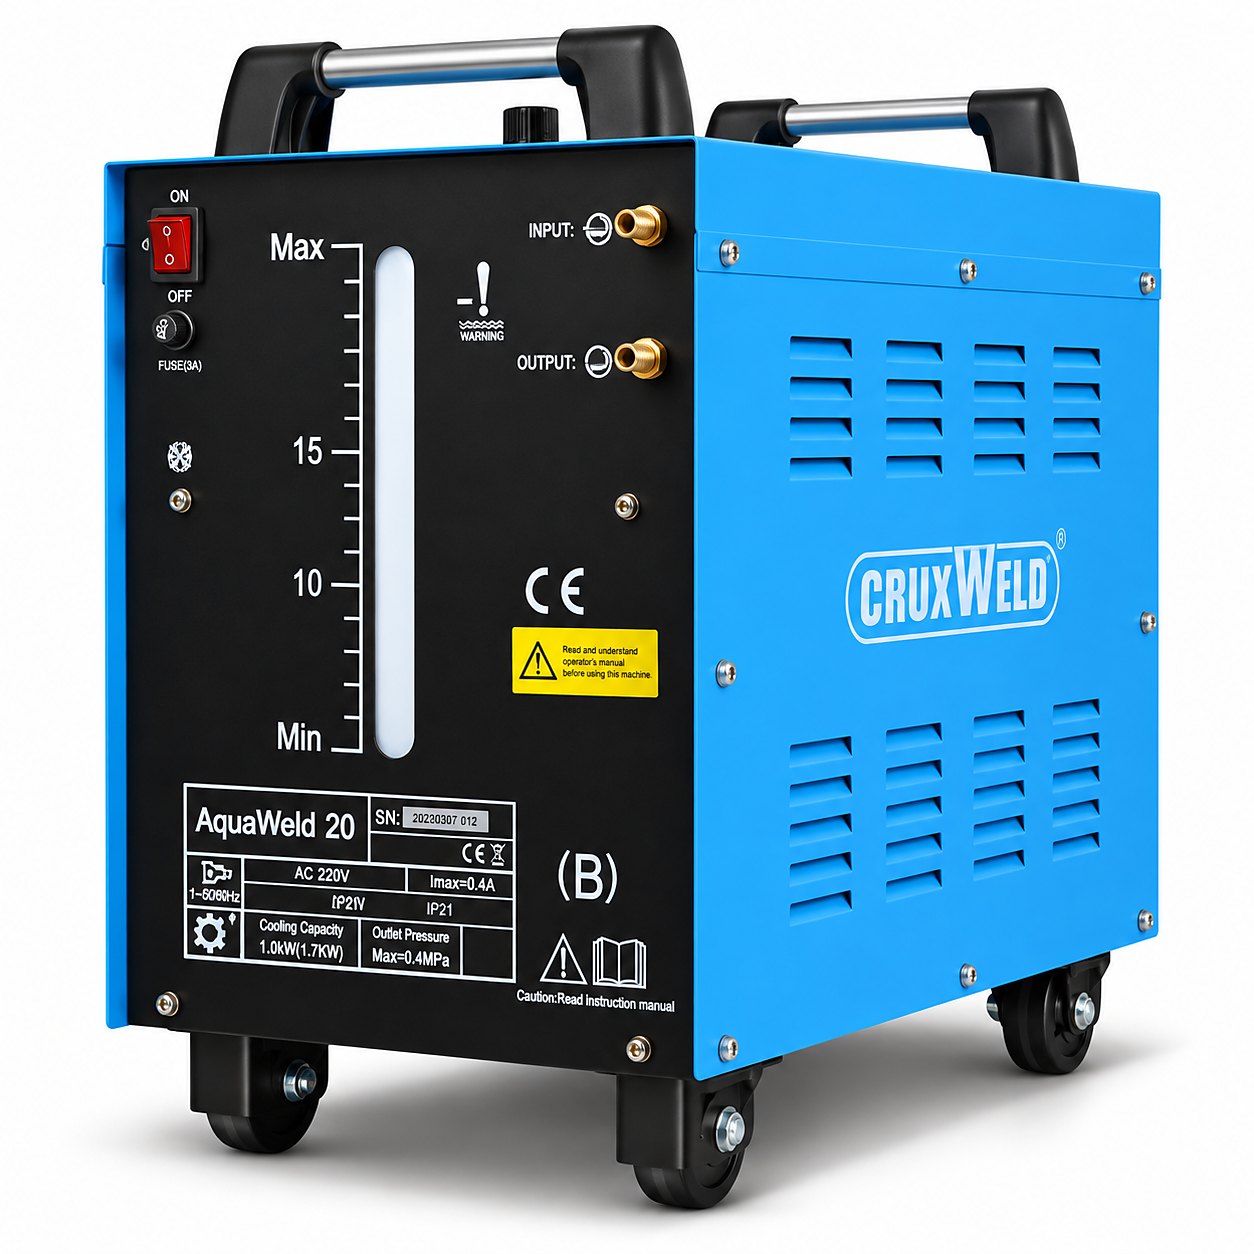
The ProSpot 3500 is the production machine; these cover the lighter, the hanging and the seam jobs, and the cooling water it needs.

Tell us the part. We will set up the ProSpot 3500 for it.

Send a photo or drawing of the job, the sheet thickness or wire size, and your city. Our technical team replies on WhatsApp with the electrode set-up, price and delivery.

Specifications

ProSpot 3500 Technical Data

Pneumatic spot and projection welder, 35 kVA

General
Model
ProSpot 3500
Type
Pedestal pneumatic spot and projection welding machine
Control
Microcomputer resistance weld controller, 16 schedules
Electrical
Rated power
35 kVA
Input voltage
380 V
Frequency
50 / 60 Hz
Maximum welding current
16,000 A
Maximum short-circuit current
15 kA
Insulation class
H
Welding
Welding capability
Up to 3.0 mm + 3.0 mm mild steel
Maximum electrode force
6200 N
Arm dimensions
220 × 420 mm
Electrode arm diameter
50 mm
Electrode holder diameter
25 mm
Cylinder stroke
60 mm
Services
Input air pressure
0.5 MPa
Cooling water
≥ 3.5 L/min
Size
Dimensions (L × W × H)
940 × 640 × 1560 mm
Weight
350 kg

Welding capability is quoted for two sheets of mild steel. Stainless, coated and dissimilar sheets, and projection welding of fasteners, are confirmed on sample parts by our technical team. Specifications as published by CRUXWELD.

Accessories

Scope of supply

What comes with the machine

ProSpot 3500 pneumatic spot welder, front view with pointed electrodes
  • 1ProSpot 3500 pneumatic spot welder, 35 kVA, with water-cooled arms and electrode holders
  • 2Microcomputer resistance weld controller mounted on the column
  • 3Pneumatic cylinder, solenoid valve, air tank and F.R.L. unit fitted and piped
  • 4Foot pedal switch for hands-free starting
  • 5One set of copper electrodes and the controller manual
Options: flat electrode bars for mesh, projection die sets for nuts and bolts, and the AquaWeld 20 water cooling unit where mains water cannot be used. Not included: fixtures and jigs for your parts.
Spares

Consumables and replacement parts

ProSpot 3500 Electrode tips and holders

Electrode tips and holders

Pointed and flat tips, 25 mm holders, copper alloy.

ProSpot 3500 F.R.L. unit and copper shunt

F.R.L. unit and copper shunt

Filter-regulator-lubricator; laminated copper shunt.

ProSpot 3500 Weld controller

Weld controller

Replacement microcomputer resistance controller.

Description

About the product

ProSpot 3500 pneumatic spot welding machine, 35 kVA

The CRUXWELD ProSpot 3500 is a 35 kVA pedestal-type pneumatic spot and projection welding machine built for repetitive fabrication work. It welds two sheets of mild steel up to 3 mm each with a maximum welding current of 16,000 A, and its pneumatic cylinder applies up to 6200 N of electrode force on every weld. Because the force comes from the cylinder and the timing from the controller, each spot is made the same way whoever is on the pedal.

A microcomputer resistance weld controller sets the whole cycle in mains cycles: pre-pressing, squeeze, pre-heat, slow rise, weld, slow fall, temper, hold and off. Sixteen schedules are stored, so a shop running several parts switches by number instead of re-entering values. Constant-current control holds the welding current steady as the arms warm up, a counter tallies the welds, and eight fault codes stop the machine and tell the operator what went wrong.

Spot, wire and projection work on one machine

The 50 mm arms carry 25 mm electrode holders that take pointed tips for sheet, flat bars for wire and mesh, and die sets for projection welding nuts and bolts. Changeover is quick, which is why the same machine serves sheet-metal enclosures, wire baskets and fastener welding in a general fabrication shop. Water-cooled holders and arms, fed at 3.5 litres a minute or more, keep the machine at its rating through a full shift.

Air and control on board

An air tank with an inbuilt compressor sits on top of the column, feeding the cylinder through a solenoid valve and an F.R.L. unit that filters the air, sets the working pressure and lubricates the cylinder. A foot pedal starts each weld, and single or repeat mode is chosen on the panel. The machine measures 940 × 640 × 1560 mm, weighs 350 kg and has lifting eyes for installation.

The ProSpot 3500 sits in the Resistance Welding range beside the ROKR 16K pedal-operated spot welder, the DuoFlex 20K spot and seam welder and the AeroSpot 35 hanging spot welder. Our technical team sets up electrodes and schedules for your parts on WhatsApp and video call.

Question & Answers

FAQ

Pneumatic Spot Welding Machine — Frequently Asked Questions

▸What is the ProSpot 3500 used for?
Resistance spot welding of sheet metal, wire and mesh, and projection welding of nuts and bolts. It is a 35 kVA pedestal machine for production shops that need the same weld every time: enclosures, brackets, baskets, grills, automotive parts and kitchen equipment.
▸What thickness can it weld?
Two sheets of mild steel up to 3 mm each. Stainless and coated sheet, and unequal combinations, depend on the material and are confirmed on sample parts by our technical team.
▸What is the difference between a pneumatic and a pedal spot welder?
On a pedal machine such as the ROKR 16K the operator supplies the electrode force and much of the timing with the foot. On the ProSpot 3500 a pneumatic cylinder supplies a set force, up to 6200 N, and the controller times every stage in cycles. Welds are more consistent, the operator tires less and the machine suits faster repeat work.
▸Does it need a separate compressor?
No. The air tank with inbuilt compressor sits on the machine and feeds the cylinder through the F.R.L. unit. The input air pressure is 0.5 MPa. If your shop already has an air line, it can be connected instead.
▸Can it do projection welding?
Yes. With flat electrodes or a die set it welds projection nuts, bolts and studs to sheet, and crossing wires in mesh. The flat electrode option is listed under scope of supply.
▸What does the controller do?
It times the whole weld in mains cycles: pre-pressing, squeeze, pre-heat, slow rise, weld, slow fall, temper, hold and off. It stores 16 schedules, holds the current constant, counts welds and stops the machine with a fault code if something is wrong.
▸Does it need water cooling?
Yes. The electrode holders and arms are water cooled and need 3.5 litres a minute or more. Mains water with a drain works; where that is not possible, pair it with the AquaWeld 20 closed-loop cooling unit.
▸What power supply does it need?
A 380 V, 50 or 60 Hz supply rated for 35 kVA. Our technical team will confirm the cable size and protection for your site.
▸How big is it and how is it moved?
940 mm long, 640 mm wide and 1560 mm high, 350 kg. Lifting eyes on top of the column take a sling or hoist; it stands on a level concrete floor and is bolted down through the base.
▸How do I get a quotation?
Send a photo or drawing of the part, the sheet thickness or wire size and your city on WhatsApp to +91 88008 82983. Our technical team replies with the electrode set-up, price and delivery.

0 replies on “Pneumatic Spot Welding Machine ProSpot 3500 | 35 kVA Spot & Projection Welder”

WhatsApp chat