Submerged arc welding · IGBT inverter · two models
1250 A or 1000 A. One Operator, Seams Without Stops.
The CRUXWELD FLUXOR is an inverter SAW welding machine in two sizes: the FLUXOR 1250 (100–1250 A, 60 kVA) and the FLUXOR 1000 (100–1000 A, 52 kVA). Each pairs an IGBT power source with a self-propelled welding tractor that lays 2.4 to 6.0 mm wire under flux, continuously, at full rated current. Girders, I-beams, tanks, pressure vessels and ship panels: wherever the seam is long enough that deposition rate decides the job, this is the machine. Both are GeM Registered OEM Manufacturer supply, engineered, assembled and tested in India.
A SAW welding machine buries the arc under a blanket of granular flux. No spatter, no arc flash, almost no fume — and because the arc is shielded so completely, it runs at currents no hand process can touch. One SAW tractor deposits more weld metal in a shift than several MMA welders, with deeper, more predictable penetration.
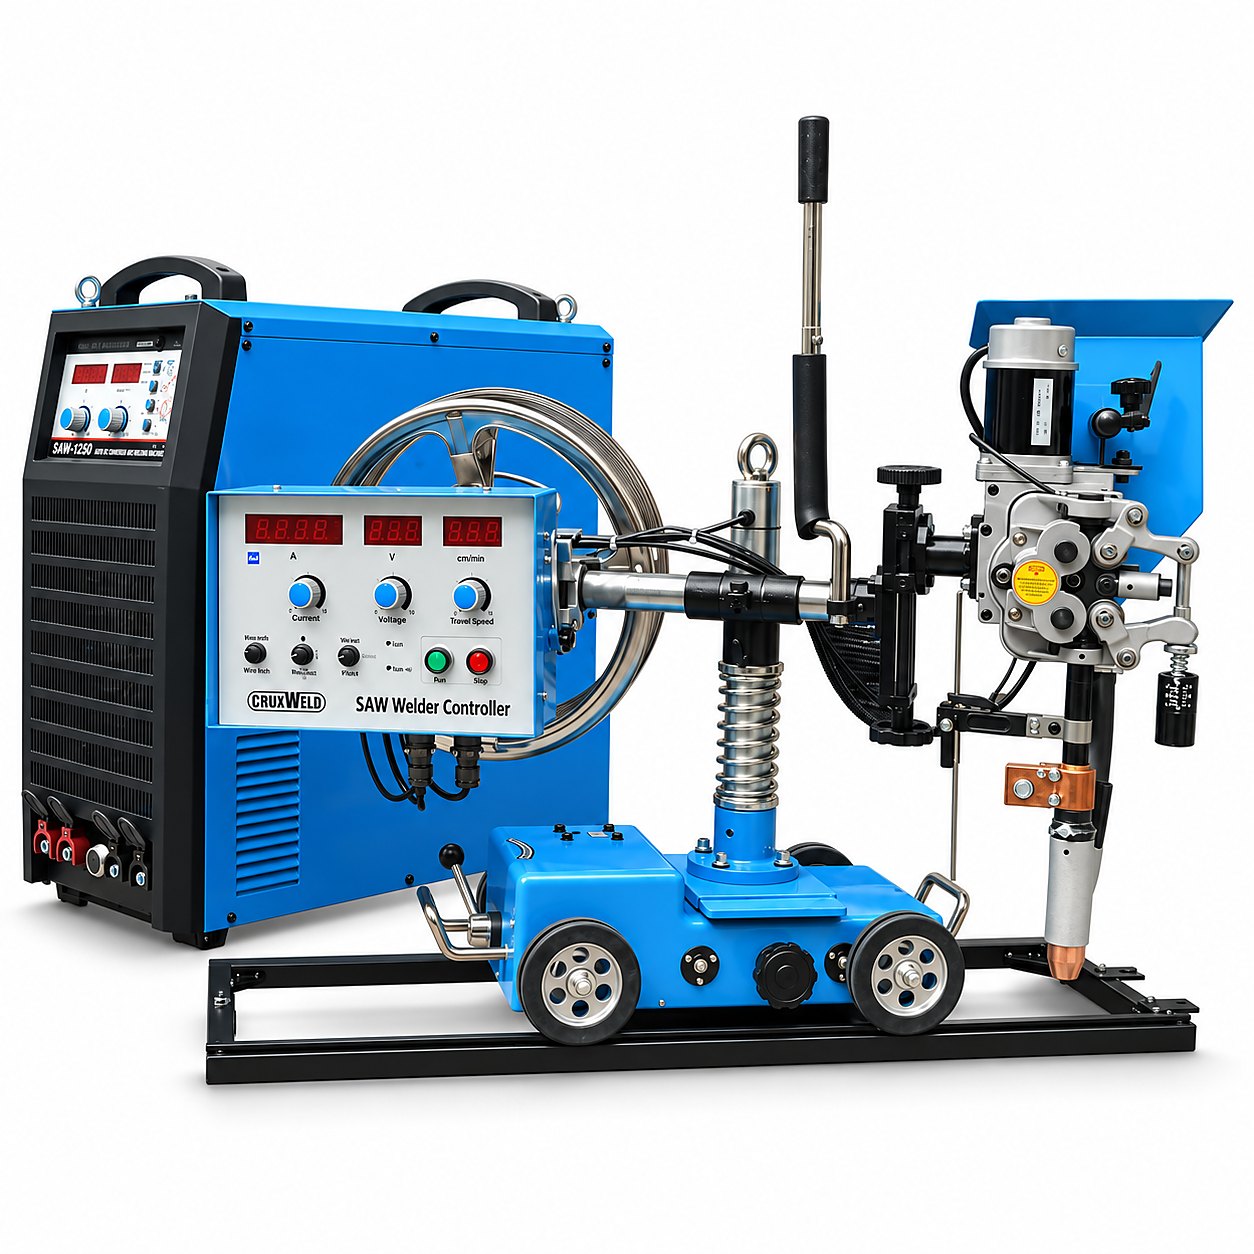
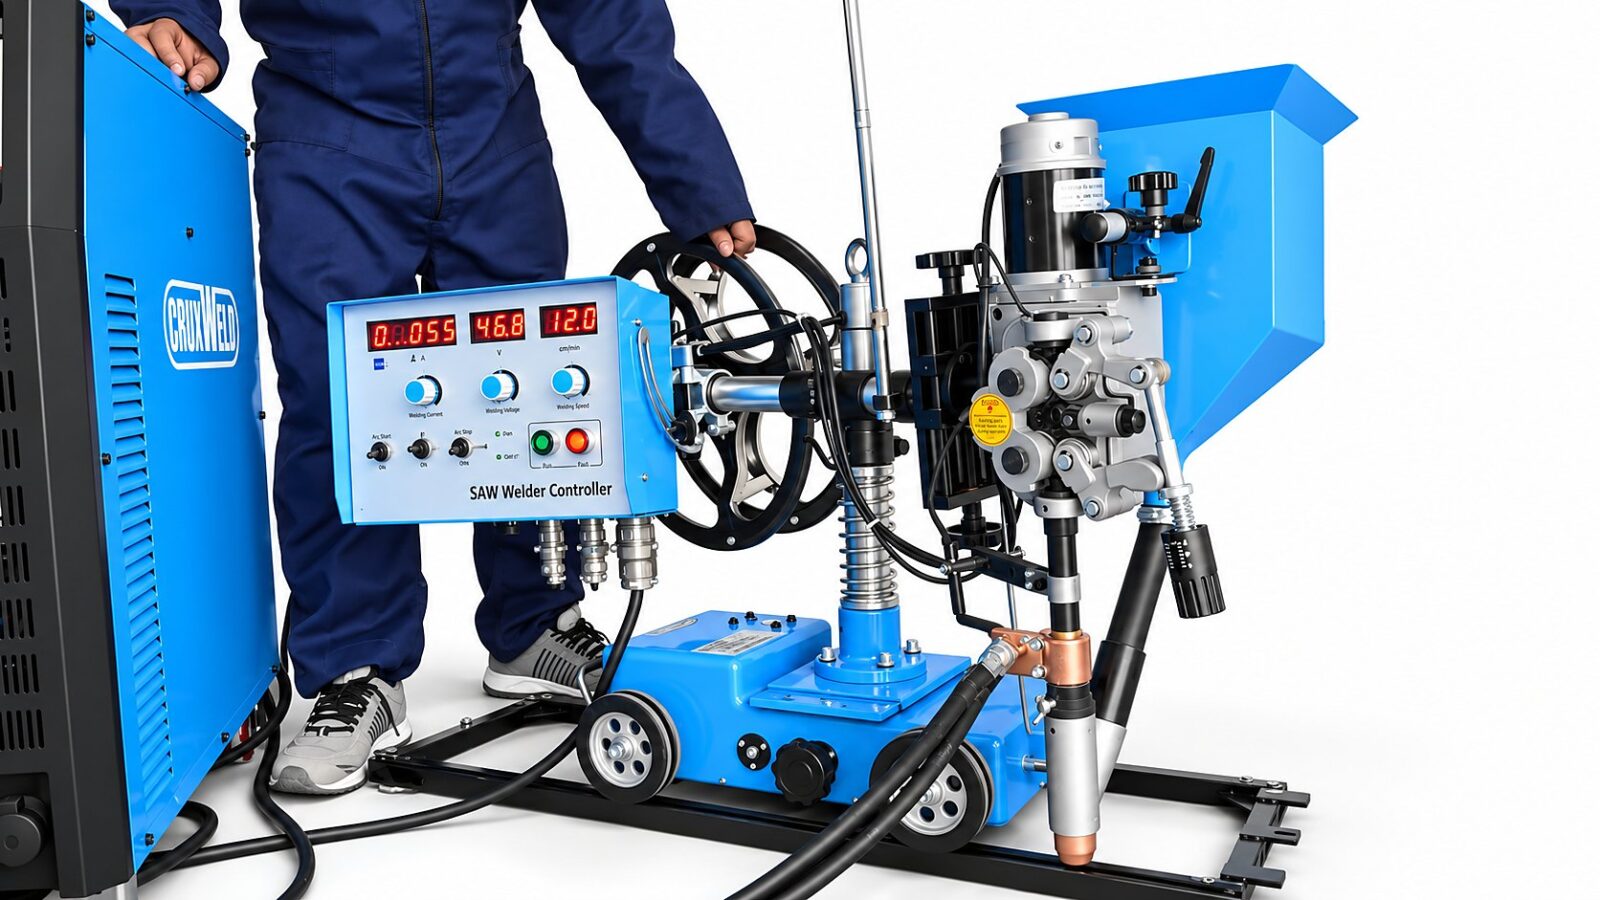
The FLUXOR packages the whole system: an IGBT inverter power source, a digital controller for current, voltage and travel speed, and a tractor carrying the 25 kg wire reel, the 10-litre flux hopper and the welding head. Set the parameters, press start, and the tractor drives itself along the seam at constant speed with a constant arc. The operator supervises; the machine welds.
1250 A or 1000 A output
High current for deep, wide seams on thick plate; the tractor carries the torch while the operator supervises.
Three processes, one source
CC/CV output covers submerged arc, MMA electrodes to 6.3 mm and air carbon arc gouging to 12 mm (5 mm and 10 mm on the FLUXOR 1000).
Inverter efficiency
85% efficiency and 0.93 power factor — far below the input a transformer SAW of this output draws.
Full-range protection
Over-current, over-heat, over-voltage, under-voltage, phase-loss and thermal protection built into the power source.
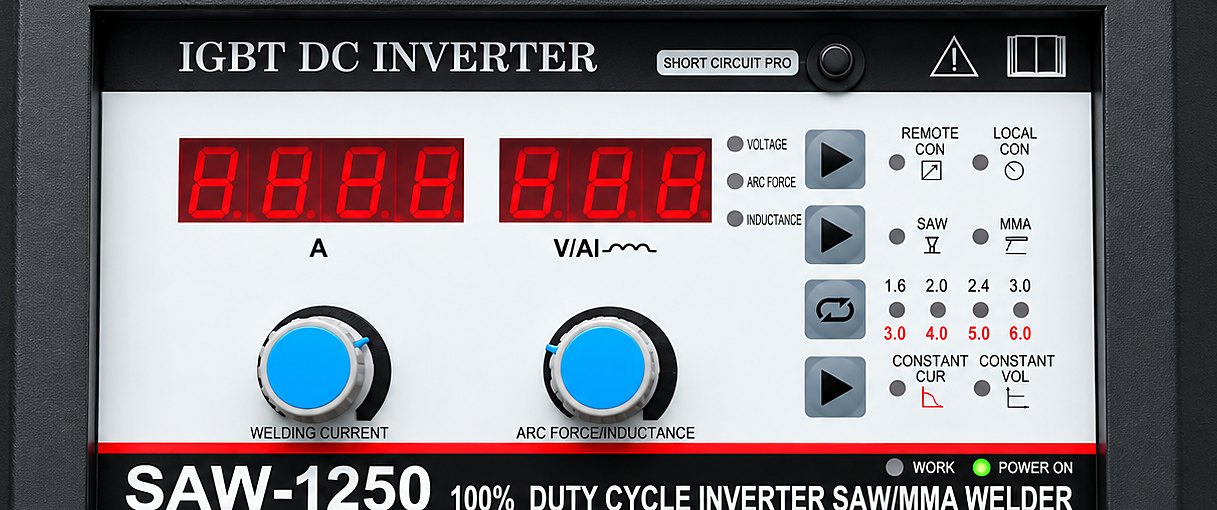
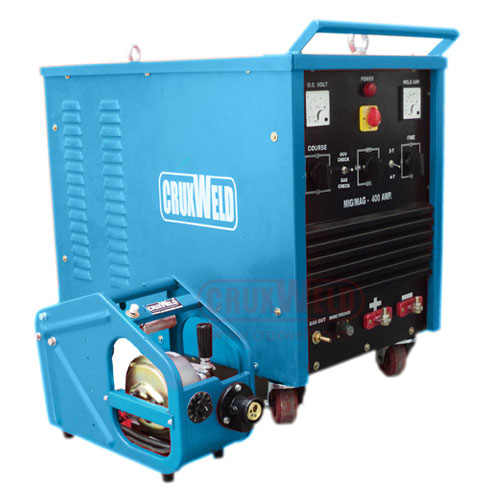
FLUXOR 1250: IGBT power source, digital controller and welding tractor.
The system
Three Parts, One Seam
1IGBT inverter power source
Digital A / V display, CC/CV selection, SAW or MMA mode, remote or local control, arc-force and inductance setting.
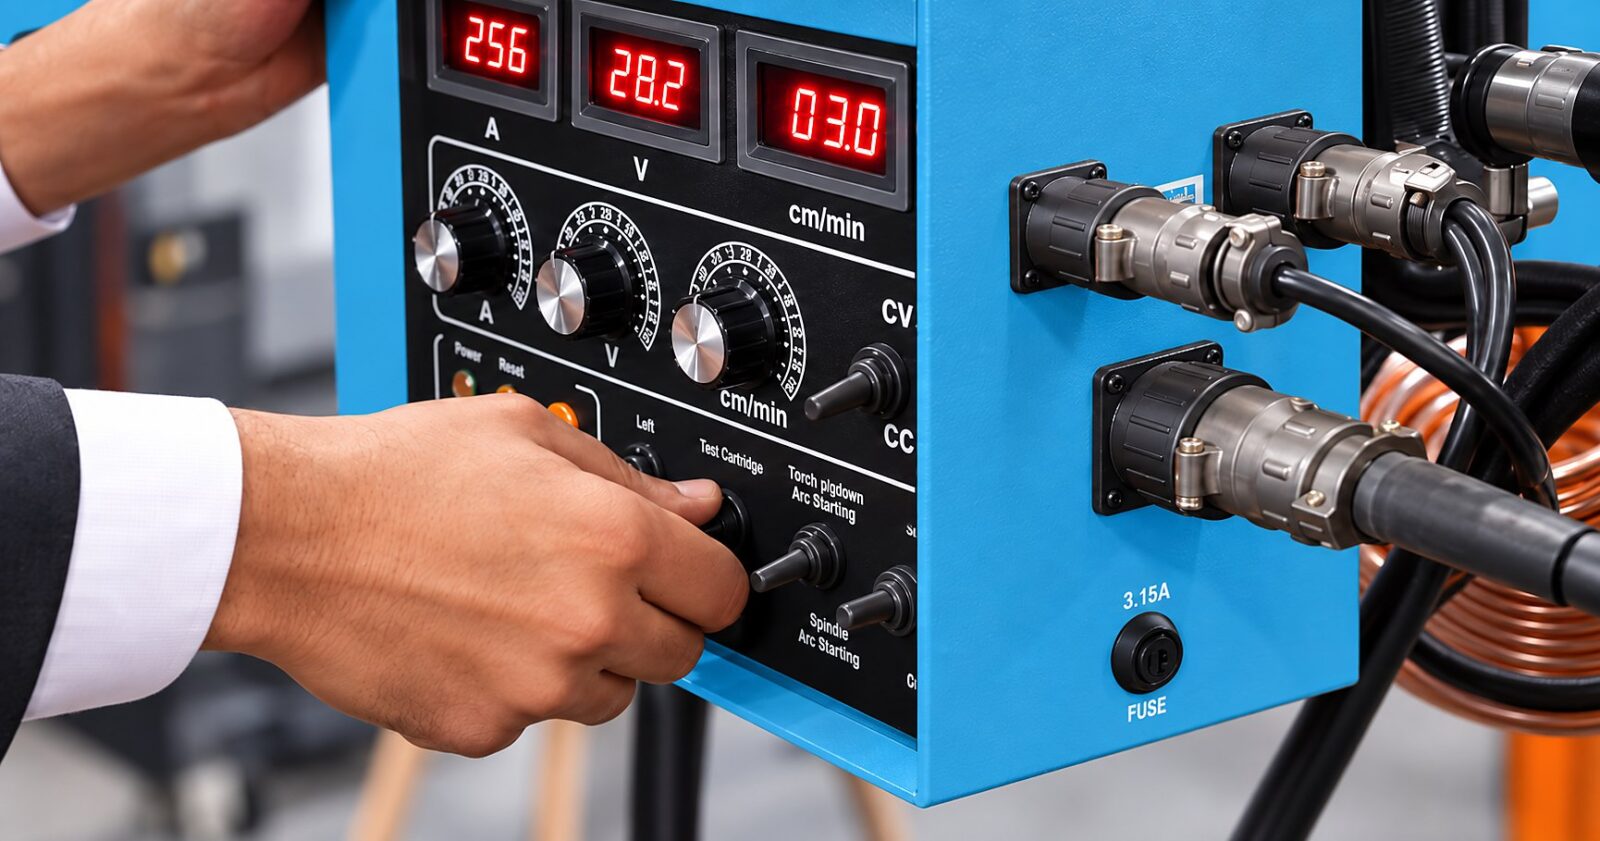
2Digital tractor controller
Preset current, voltage and travel speed in cm/min; wire inch, test cartridge and arc-start modes on one panel the operator can read from the seam.
3Self-propelled tractor
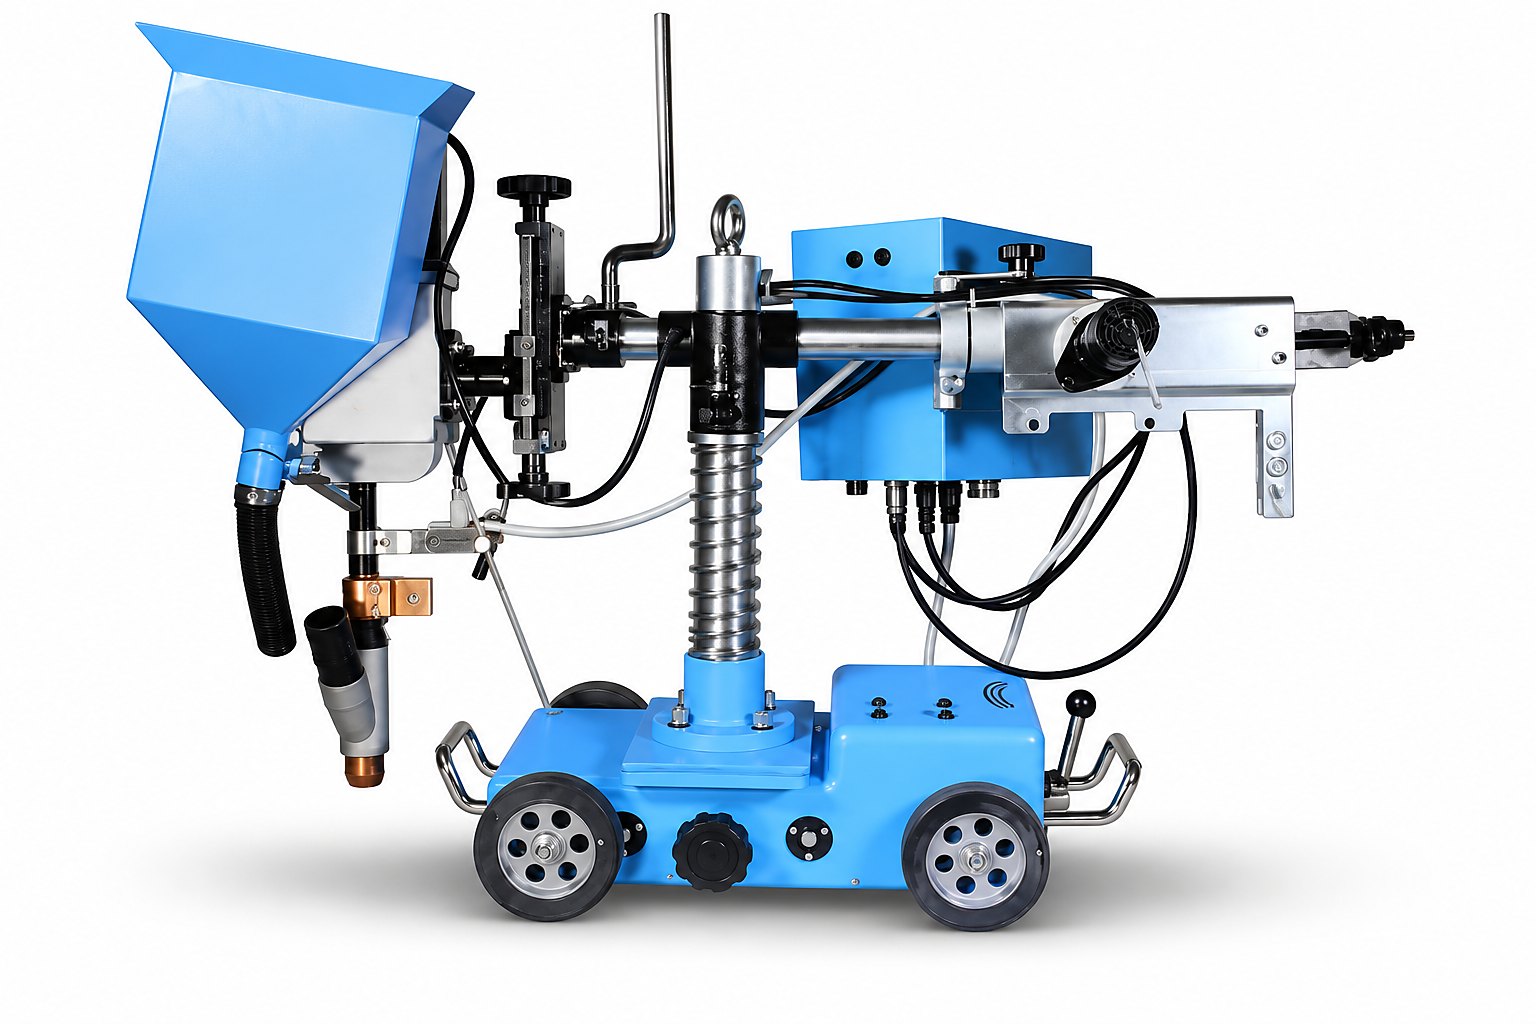
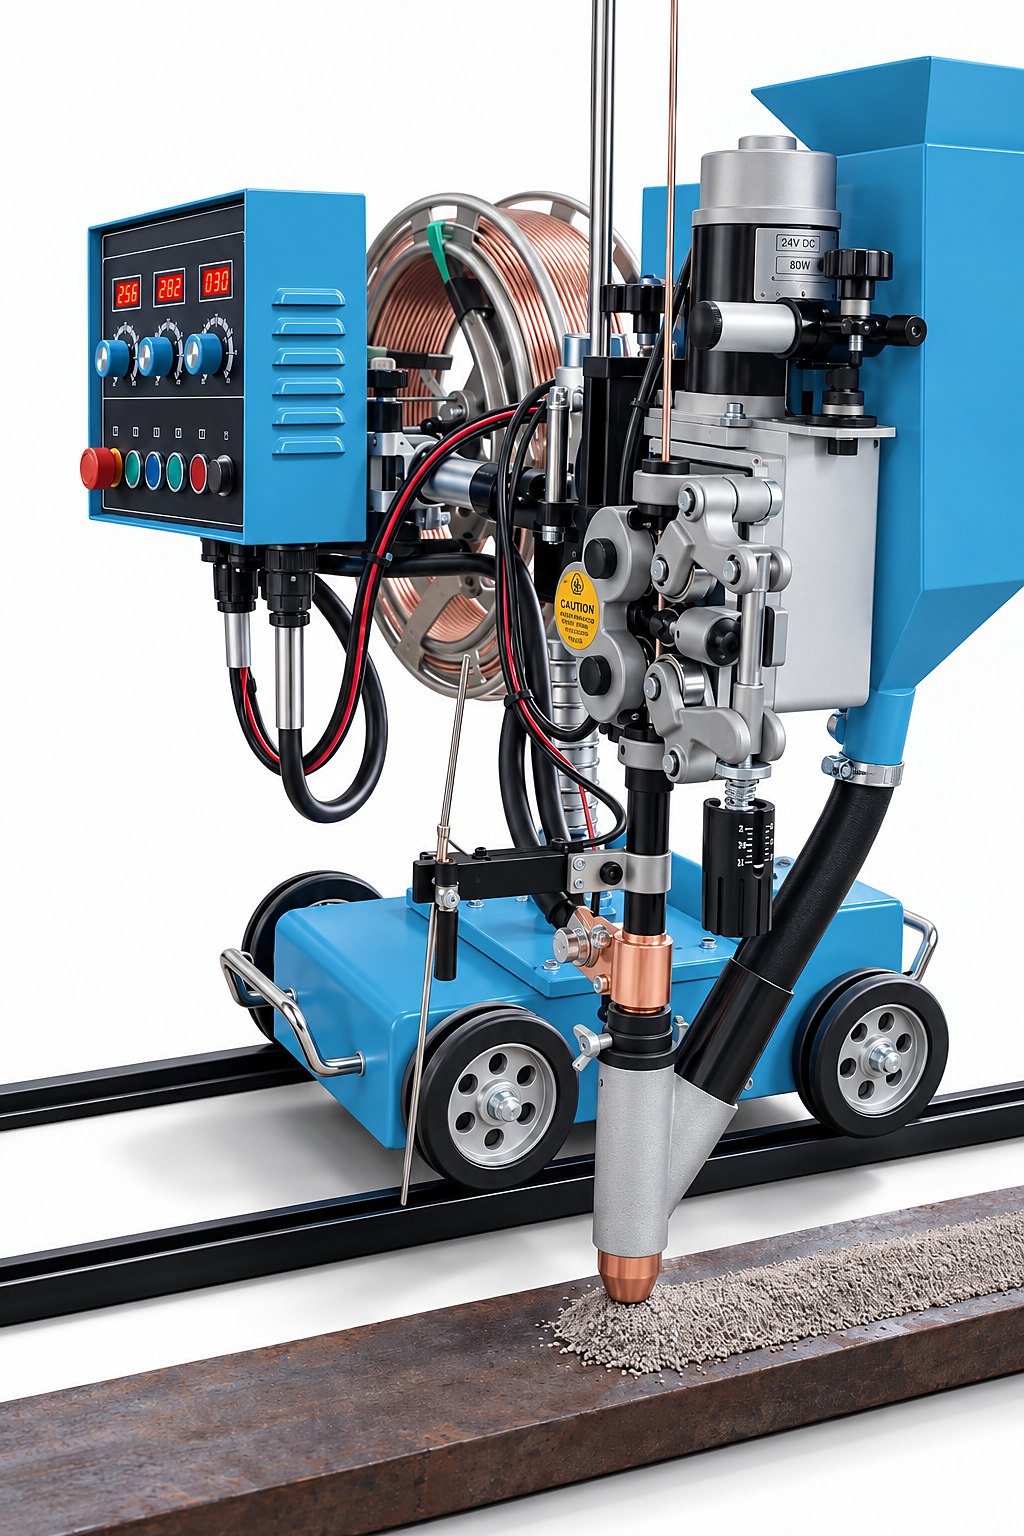
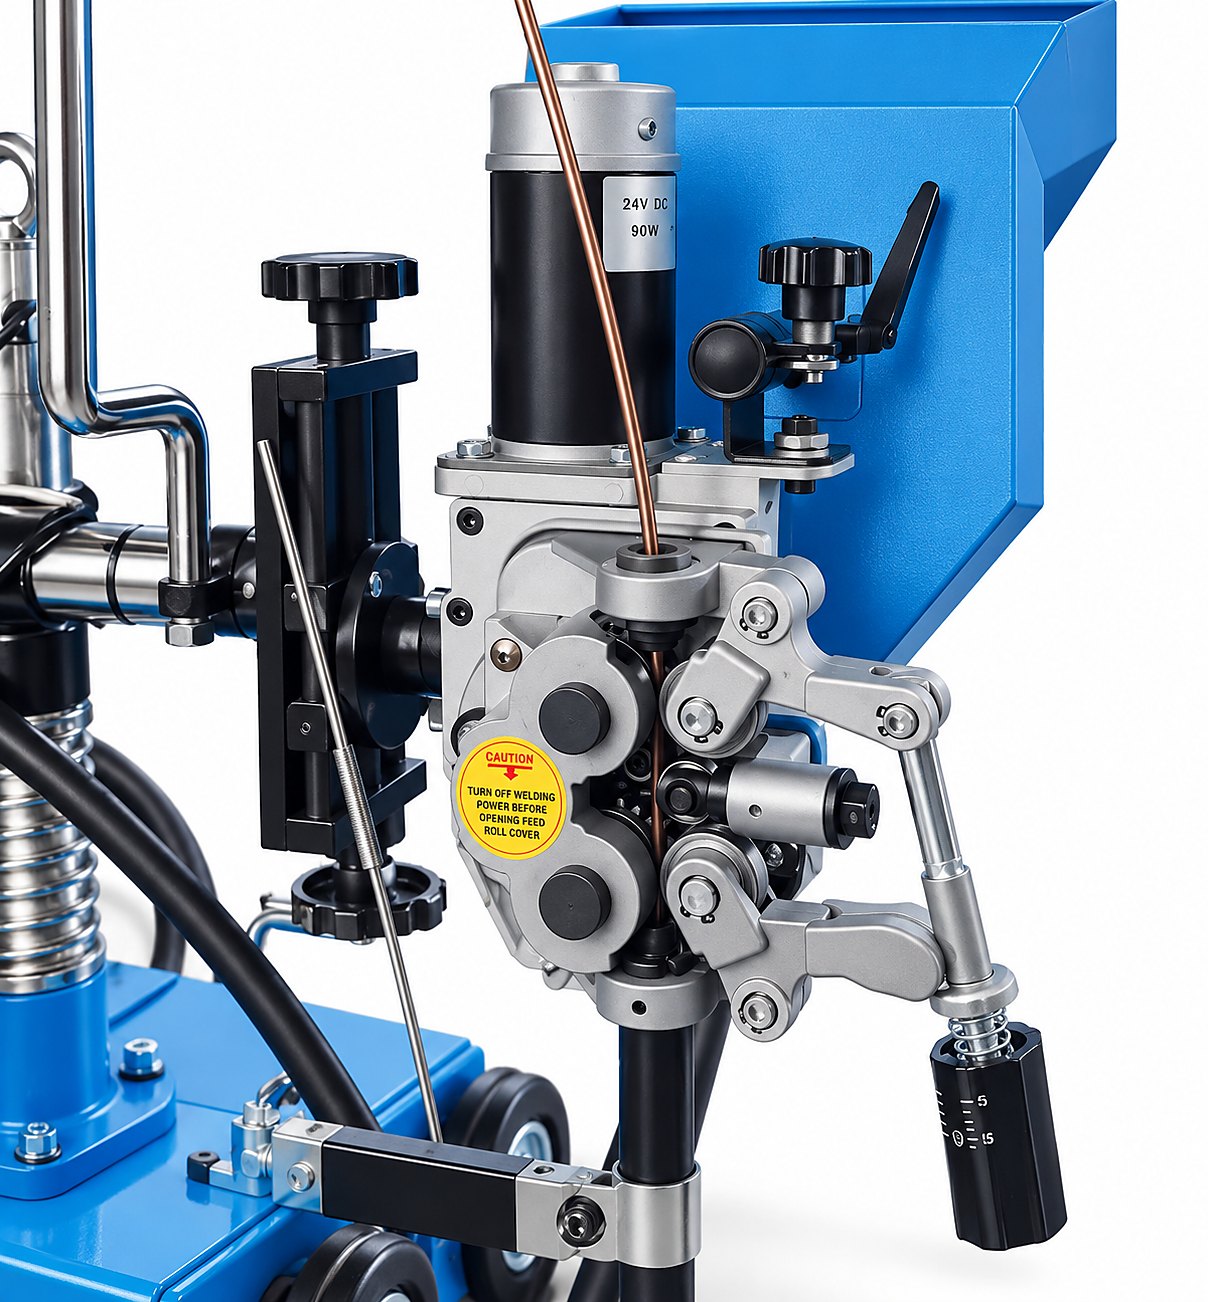
Four-wheel drive carriage, lifting column, cantilever arm, 24 V DC geared feed motor, 25 kg reel holder and 10 L flux hopper — integrated into one rigid unit.
On this SAW welding machine, horizontal adjustment is on a moving plate, vertical adjustment on a large-range column, and the conductive rod can be extended, so the head reaches the joint on plate girders, box sections and vessel seams without rebuilding the fixture.
Built into the tractor
The Details That Keep the Bead Straight
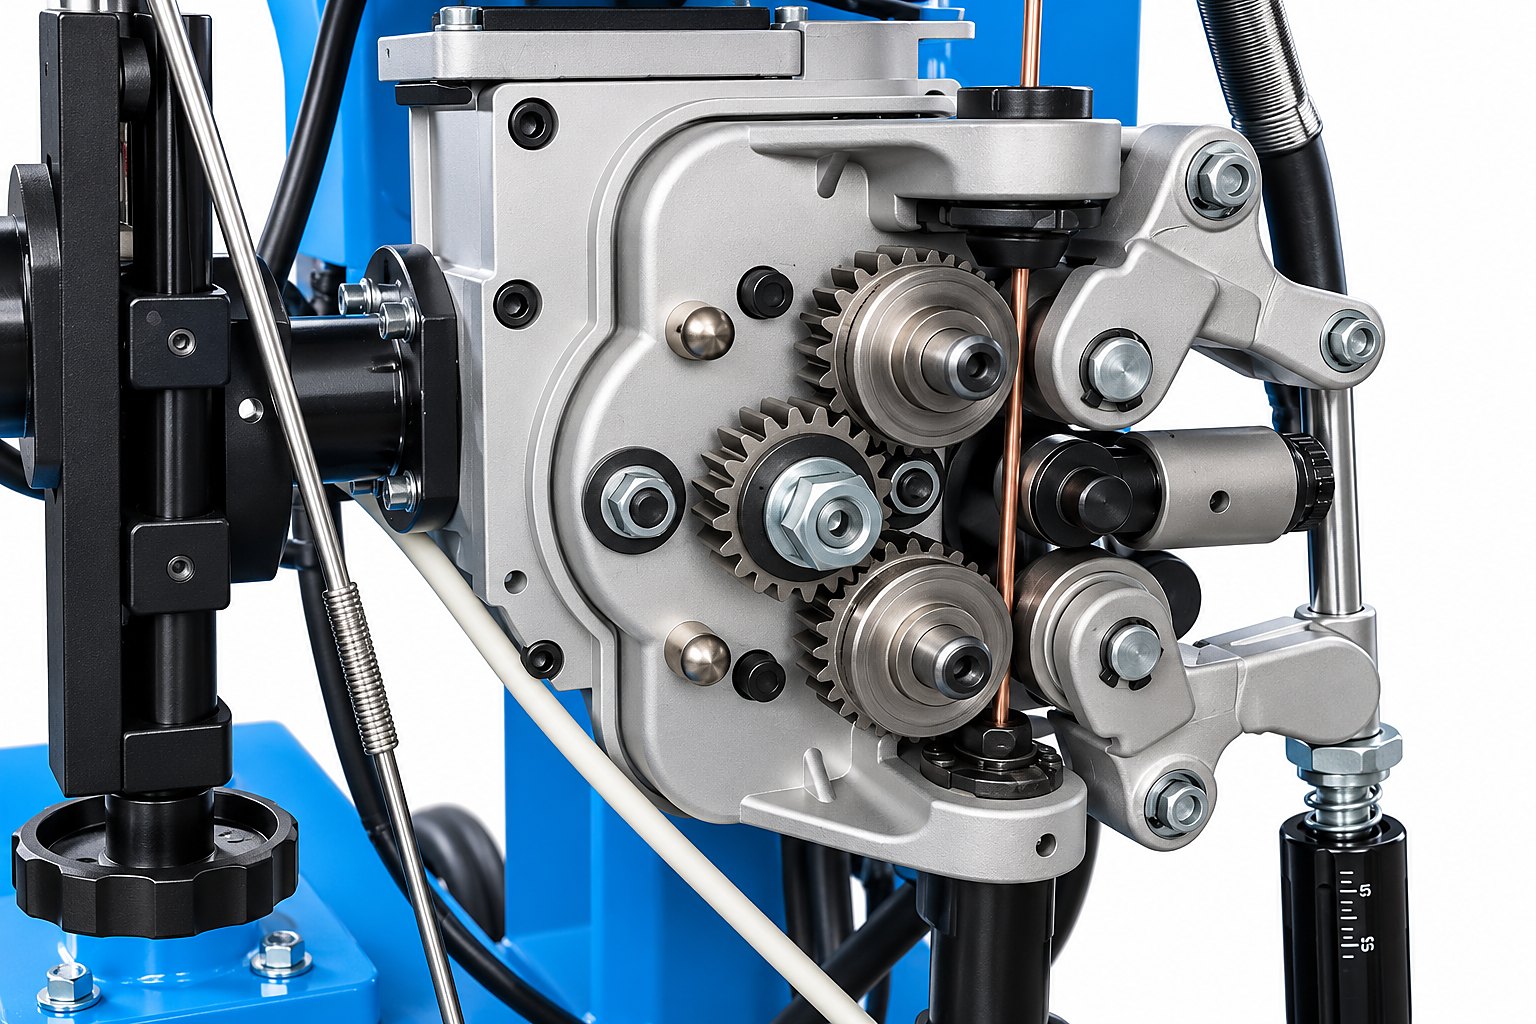
Geared four-roll wire drive
Hardened, geared feed rolls grip 2.4 to 6.0 mm wire without slip; feed rate 0.5–2.5 m/min from the 24 V DC 90 W motor.
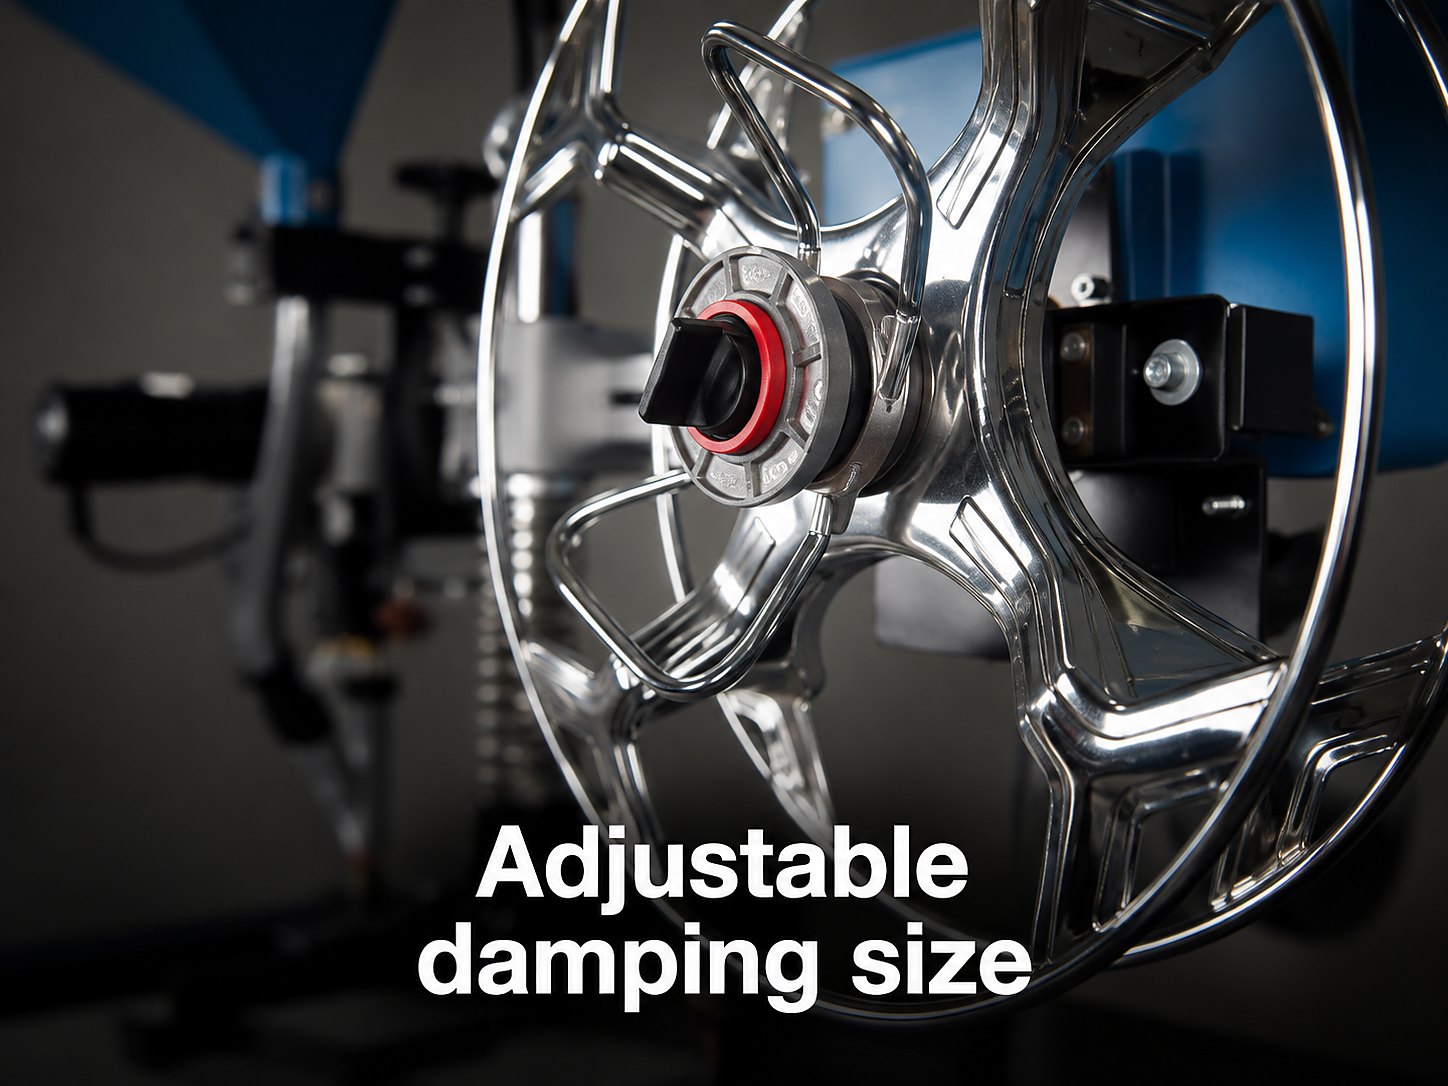
Adjustable reel damping
Brake tension on the 25 kg reel is set by hand so heavy wire neither overruns nor drags on the feed rolls.
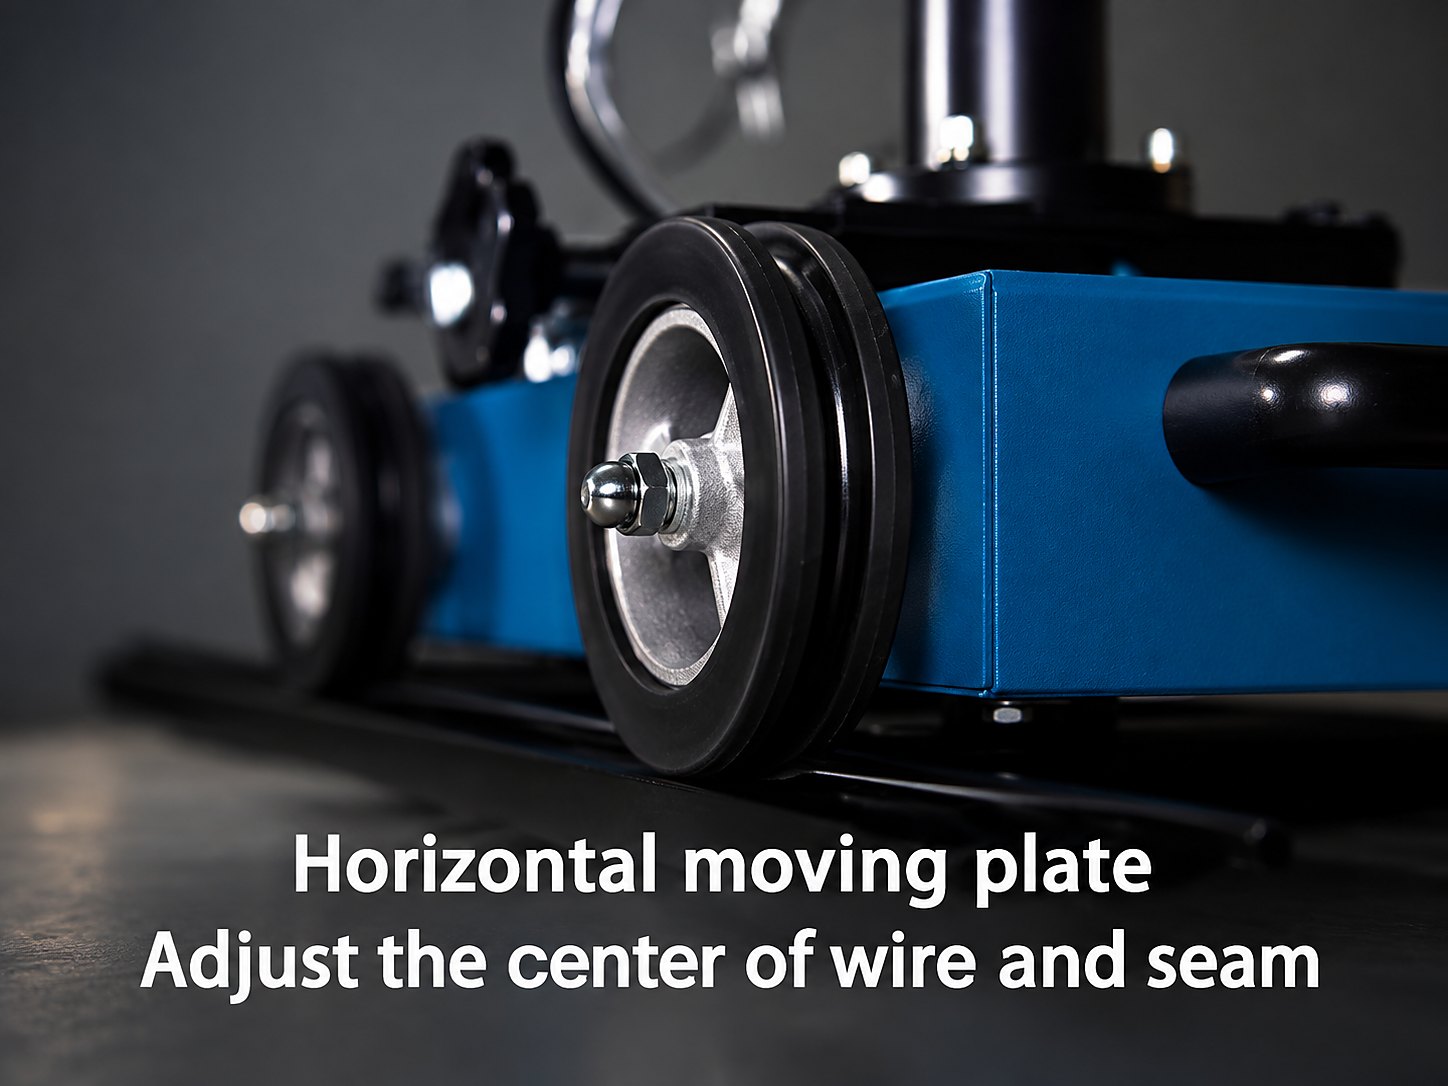
Horizontal moving plate
Centres the wire on the seam with a hand knob while the tractor sits on the rail — no re-positioning of the carriage.
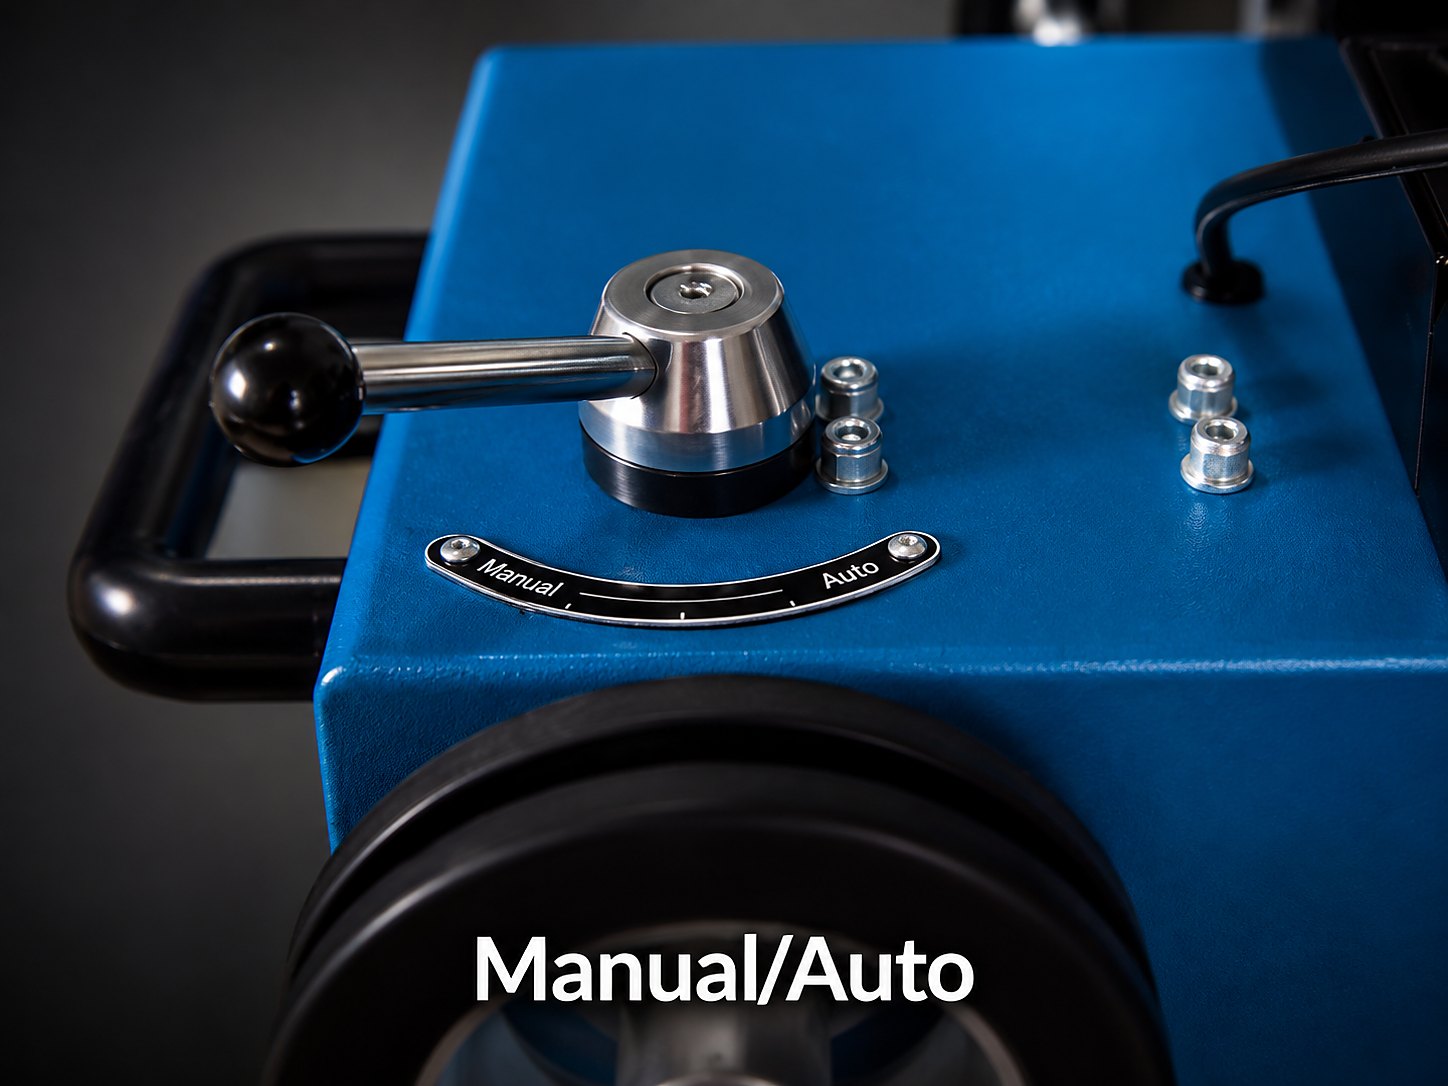
Manual / Auto clutch
Disengage the drive to push the tractor to the start of the joint by hand; engage for motor-driven travel at the set speed.
Adjustable welding head
Head angle to 45° for fillet or butt seams, laser pointer and weld indicator to simulate the trajectory before striking.
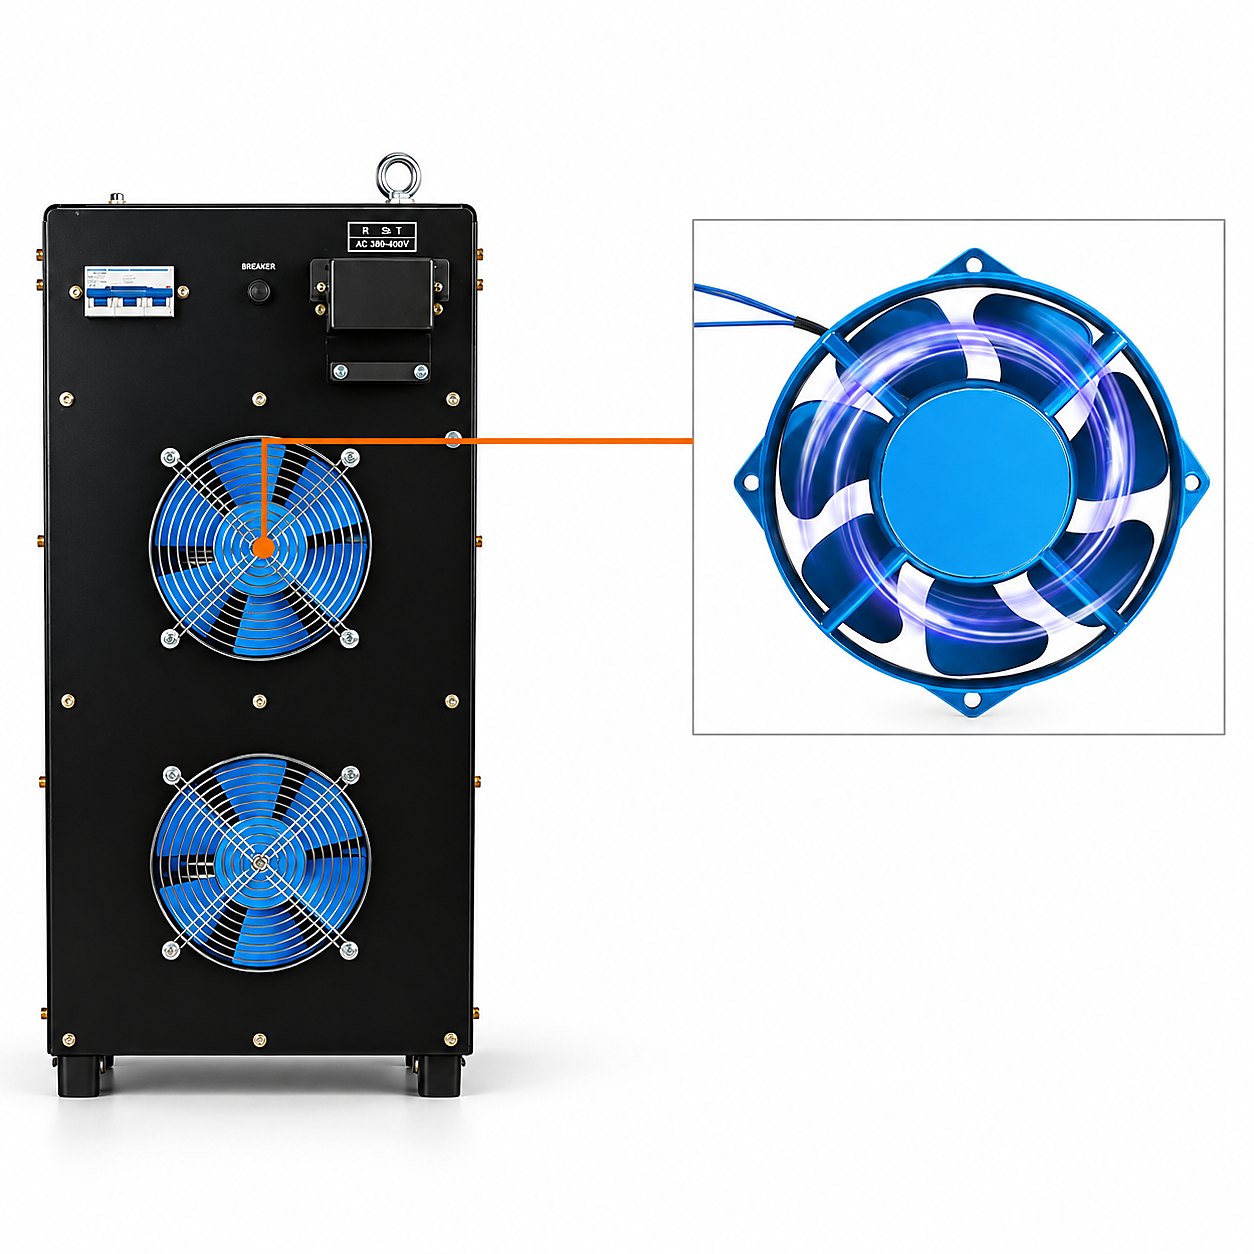
Three-duct forced-air cooling
Separate air ducts over the IGBT module, rectifier and transformer keep the power source cool in a hot shop.
How it works
Flux In, Wire Down, Seam Done
1Set up on the joint
Place the SAW welding machine tractor on the plate or guide rail, load the reel, fill the hopper and align the wire to the seam with the moving plate and laser pointer.
2Set the parameters
Current, voltage and travel speed on the digital controller. Wire-inch and test buttons check the set-up before the arc is struck.
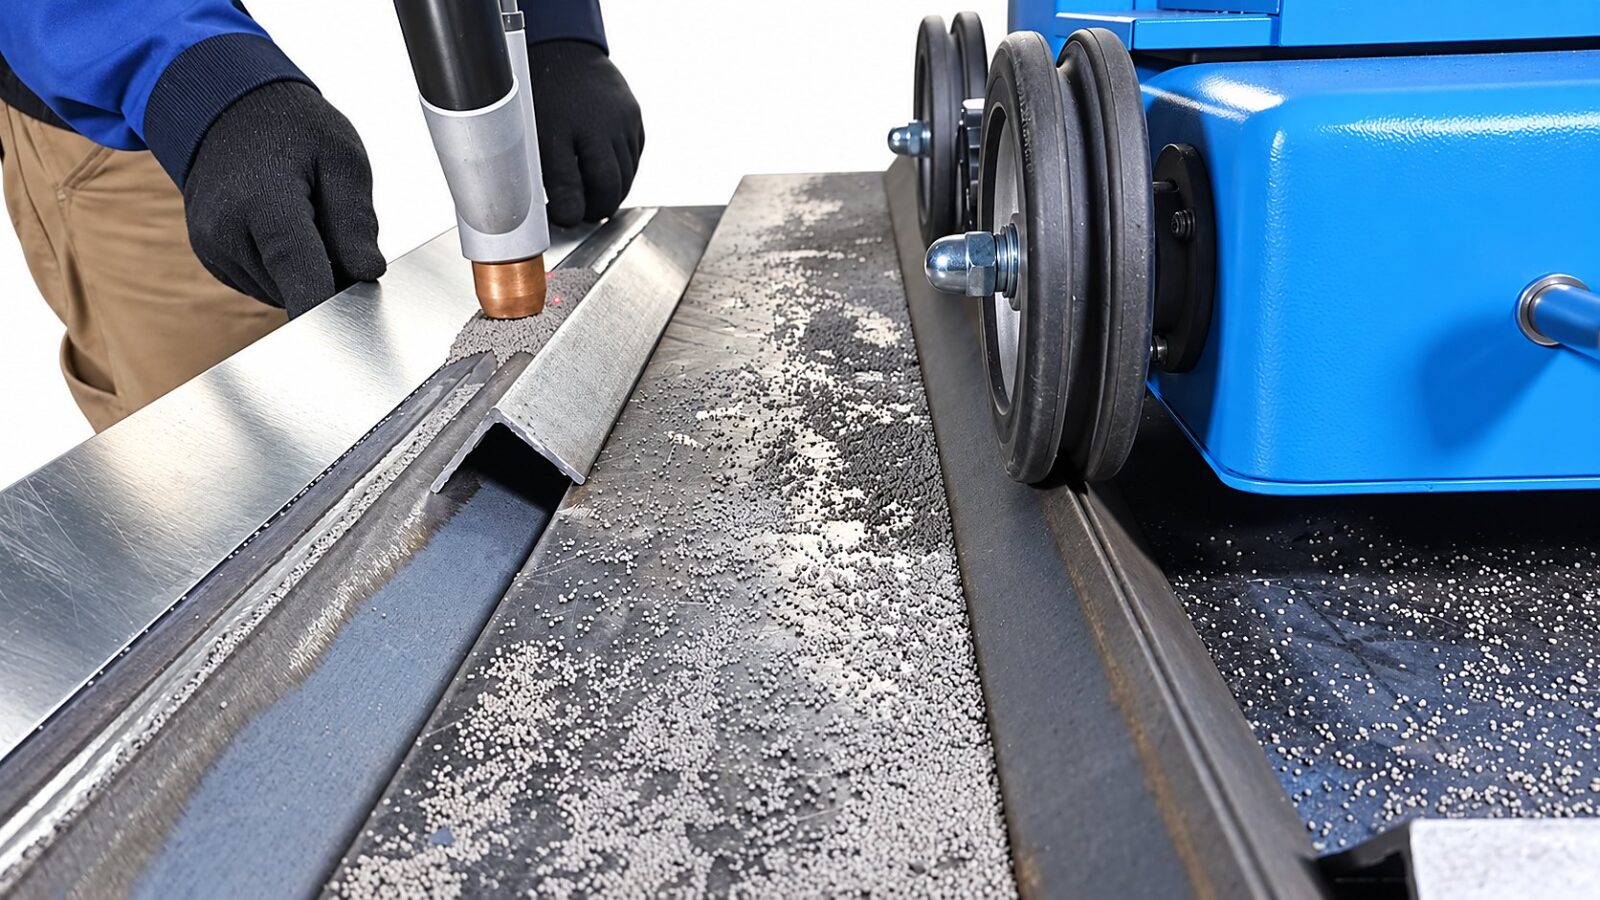
3Weld under flux
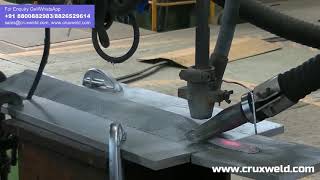
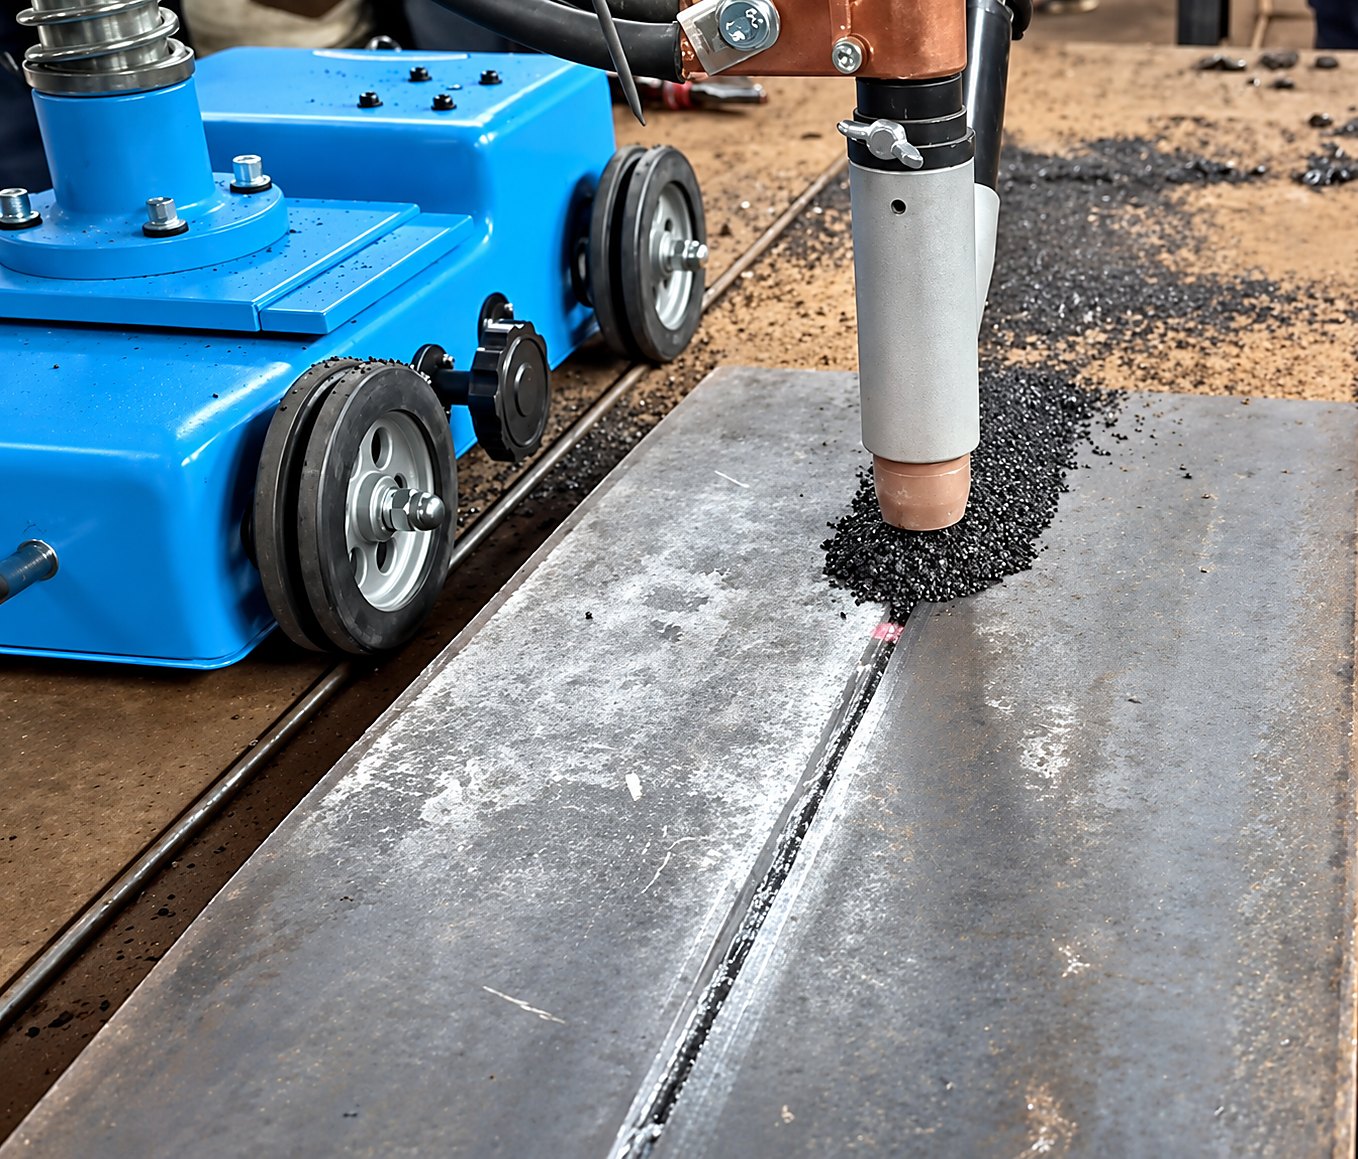
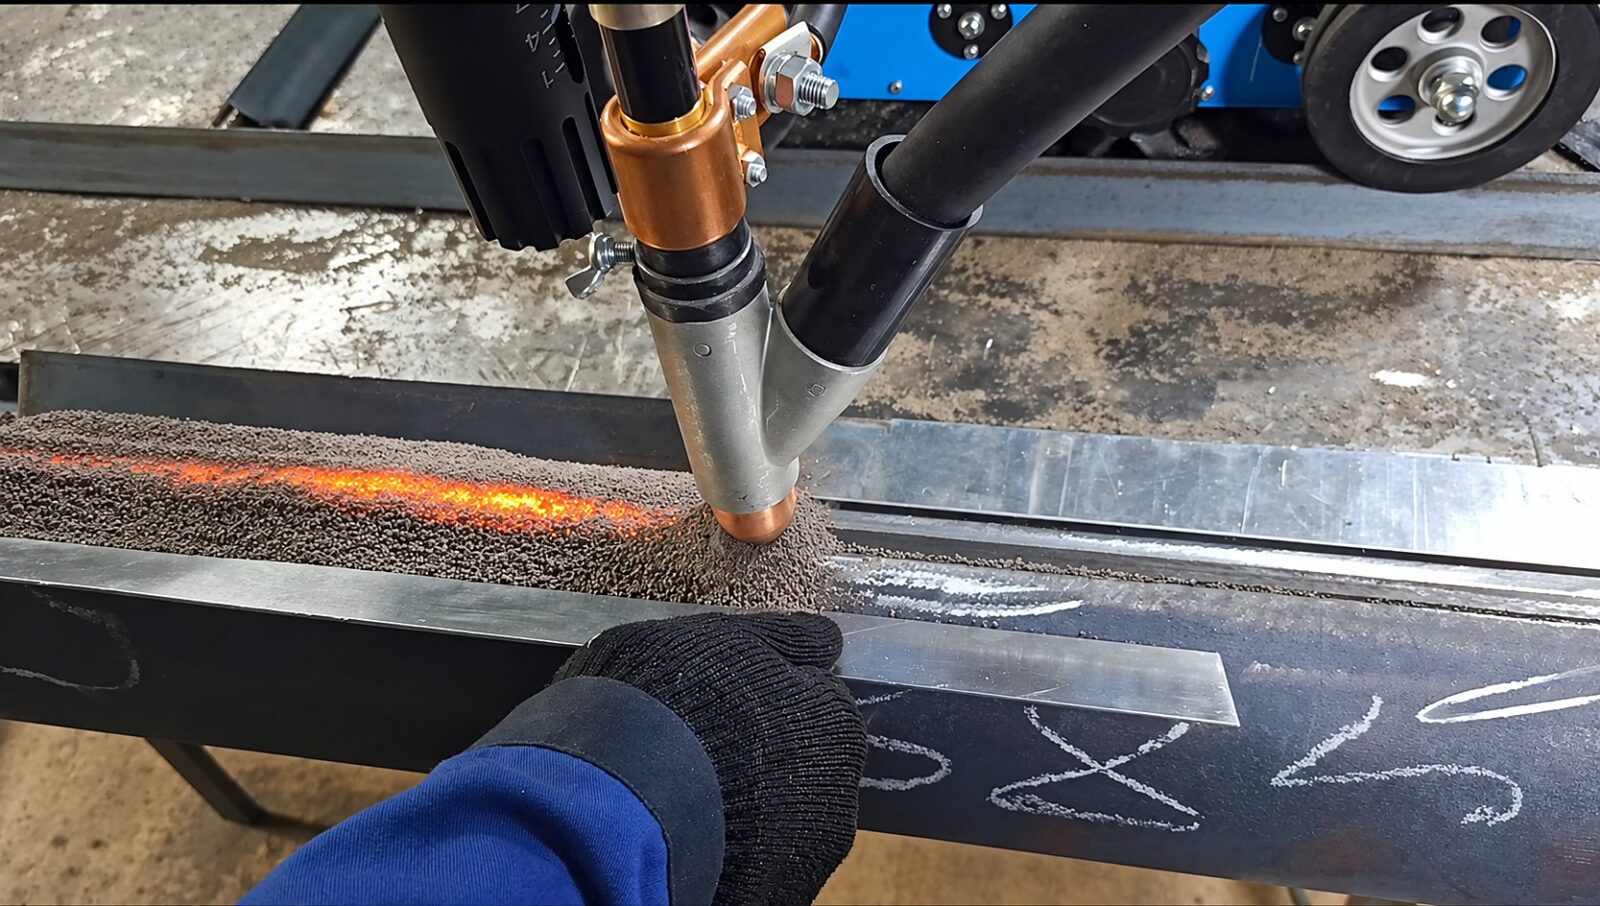
Flux flows ahead of the wire, the arc runs beneath it and the tractor travels the seam at constant speed. The operator watches the flux cover, not an arc.
4Recover and inspect
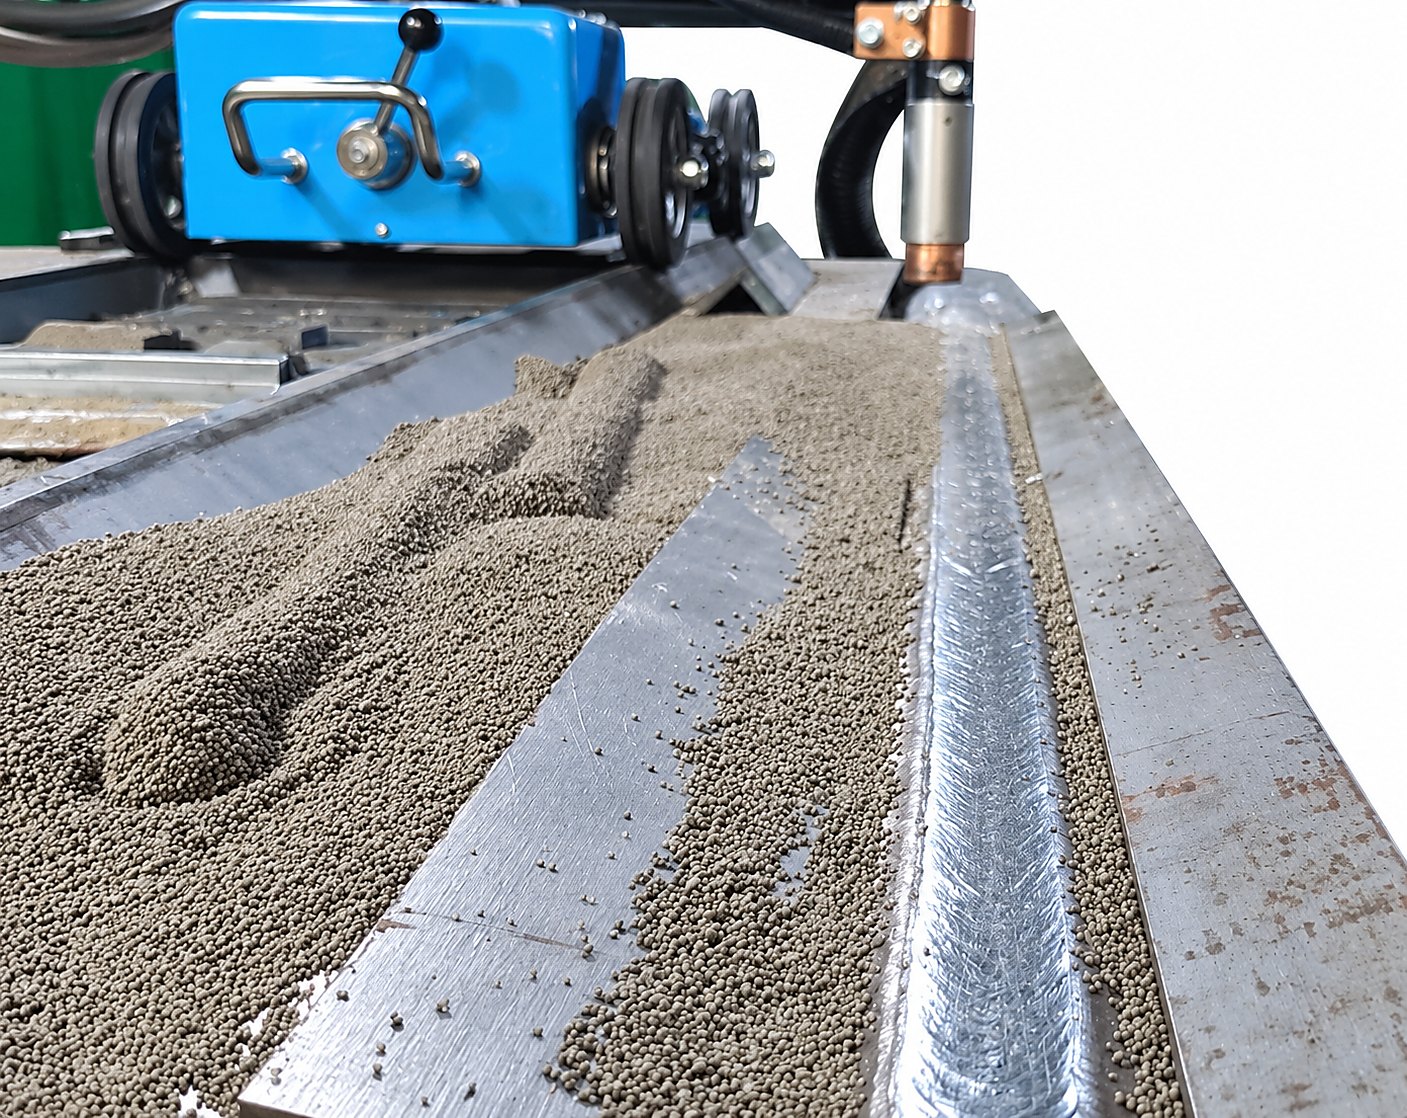
Unfused flux is swept and reused; slag lifts off a bright, smooth bead. Multi-pass joints run the same way, pass after pass.
100–1250 A, 30–44 V, 60 kVA. For 5 and 6 mm wire, double-V joints on 25 mm+ plate, girders and pressure-vessel seams where the highest deposition rate pays back fastest.
FLUXOR 1000
100–1000 A, 24–44 V, 52 kVA. 1000 A, for 2.5 to 4 mm wire on structural fabrication, tanks and general plate work with a smaller power source.
Both SAW welding machine models share the same tractor, controller, wire reel and flux hopper, carry the same full-range protections, and run MMA and carbon-arc gouging between SAW jobs (6.3 mm electrodes and 12 mm gouging on the 1250; 5 mm and 10 mm on the 1000). Tell us plate thickness, joint type and seam length and we will size the machine.
Why fabricators choose it
What Changes on the Shop Floor
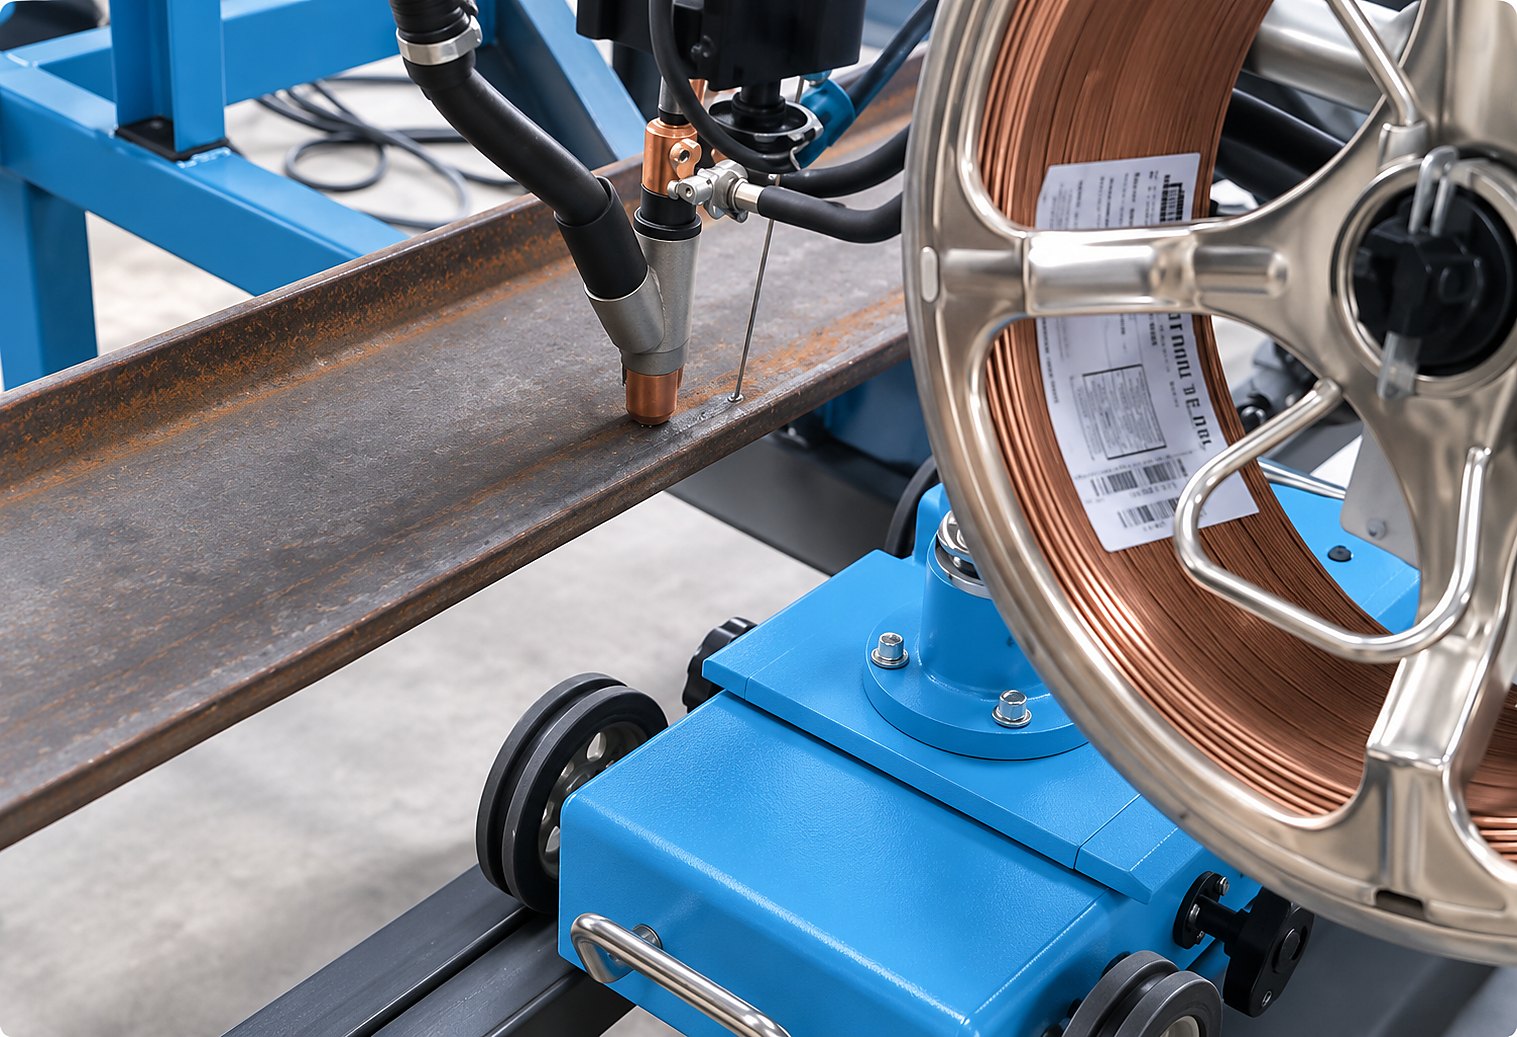
Butt seam on plate: one pass, one operator.
✓Deposition rate. At 1250 A with 5 or 6 mm wire the FLUXOR fills a double-V joint in a fraction of the passes a hand process needs — 30% higher deposition at the same parameters is typical.
✓Consistent quality. Constant current, voltage and travel speed give a uniform bead with deep, predictable penetration — the basis of repeatable radiography results.
✓Less heat, less distortion. Controlled heat input keeps long panels flat and preserves mechanical properties in the heat-affected zone.
✓Operator comfort. No arc flash, negligible fume, no spatter: one operator supervises long seams without fatigue.
✓Lower cost per metre. 85% efficiency, 0.93 power factor, flux recovery and fewer passes cut the cost of every metre welded.
✓Three processes. The same source runs MMA electrodes and carbon-arc gouging between SAW jobs (6.3 mm / 12 mm on the 1250, 5 mm / 10 mm on the 1000).
Carbon and low-alloy steels are the everyday work of a SAW welding machine; stainless and other alloys are welded with matching wire and flux. Our technical team will recommend consumables for your base material and joint design.
Scope of supply
What Arrives with the FLUXOR
✓IGBT inverter power source, FLUXOR 1250 or FLUXOR 1000
✓Self-propelled welding tractor with 24 V DC wire feed motor and welding head
✓Digital controller with interconnecting cable
✓25 kg wire reel holder with adjustable damping
✓10-litre flux hopper with flux hose and nozzle
✓Welding and earth cables and a test certificate
Connect the SAW welding machine to a three-phase 415 V feeder sized for 60 kVA (FLUXOR 1250) or 52 kVA (FLUXOR 1000) and the system is ready to weld. Wire, flux and guide rails are ordered separately; the exact scope is confirmed on the quotation. See the full range on our products page.
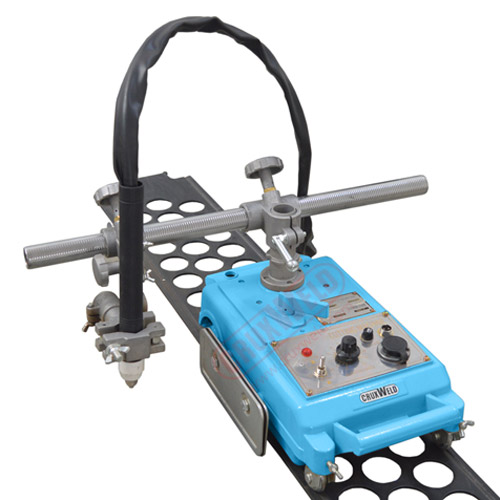
Tractor with hopper, column, feed unit and head, ready for the joint.
Why buy from CRUXWELD
Engineered in India, Supported Worldwide
45+ years of welding expertise
An established manufacturer: the FLUXOR is engineered, assembled and tested by CRUXWELD engineers in India; our technical team answers on WhatsApp.
ISO 9001:2015
Every SAW welding machine power source is load tested at rated current and every tractor run on a test seam before dispatch.
GeM Registered OEM Manufacturer
Tender-ready documentation for government, PSU, railway and shipyard buyers.
Pan-India supply, export ready
Dispatch across India and export packing for overseas orders; contact tips, feed rolls and spares in stock.
Laser pointer, weld indicator, wire inch, test cartridge
Tractor weight
58 kg
Specifications are subject to improvement without notice; the quotation and test certificate supplied with the machine are the governing documents. Warranty terms are stated on the quotation / invoice.
Long, heavy welds where deposition rate matters: web-to-flange fillets on plate girders and I-beams, longitudinal and circumferential seams on tanks and vessels, ship panel butt welds, bridge sections and heavy equipment frames. The same power source also works as an MMA welder (electrodes to 6.3 mm on the 1250, 5 mm on the 1000) and a carbon-arc gouging source (12 mm / 10 mm).
What is the difference between FLUXOR 1250 and FLUXOR 1000?
Output. The FLUXOR 1250 SAW welding machine delivers 100–1250 A from a 60 kVA source and runs wire up to 6.0 mm, MMA to 6.3 mm and gouging to 12 mm; the FLUXOR 1000 delivers 100–1000 A from a 52 kVA source and runs wire up to 4.0 mm, MMA to 5 mm and gouging to 10 mm. Tractor, controller, reel and flux hopper are the same on both.
Which wire sizes and flux does it use?
Solid SAW wire from 2.4 to 6.0 mm (FLUXOR 1250) or 2.5 to 4.0 mm (FLUXOR 1000) on a 25 kg reel, fed at 0.5–2.5 m/min, with agglomerated or fused flux from the 10-litre hopper. Our technical team will recommend wire and flux grades for your base material.
What power supply does the SAW welding machine need?
A three-phase 415 V supply (±15%), 50/60 Hz. Rated input is 60 kVA for the FLUXOR 1250 and 52 kVA for the FLUXOR 1000, so provide a dedicated feeder with a suitably rated breaker.
Does the tractor need a rail or track?
The SAW welding machine tractor is self-propelled on its own wheels and runs directly on the plate for straight seams; a guide rail is used for long or precise runs. Our technical team can advise on fixtures and rails for your joints.
Can it weld stainless steel or alloy steel?
Yes, with the appropriate wire and flux combination. Carbon and low-alloy steels are the most common; stainless and other alloys are welded with matching consumables.
What is included with the machine?
Inverter power source, welding tractor with wire-feed motor, digital controller, reel holder, flux hopper and adjustable head, interconnecting and earth cables and a test certificate. Wire, flux and guide rails are ordered separately; the exact scope is confirmed on the quotation.
How do I get the SAW welding machine price and delivery time?
Request a quote on this page or message +91 88008 82983 on WhatsApp with your plate thickness, joint type and typical seam length. You will receive a GST quotation with delivery time, usually the same working day.
Plate thickness, joint type, seam length — send us three numbers and we will size the machine.




what type of rectifier are you using in this machine.
Can we weld the beam with this Submerged Arc Welder?
Please we need the price dor this item