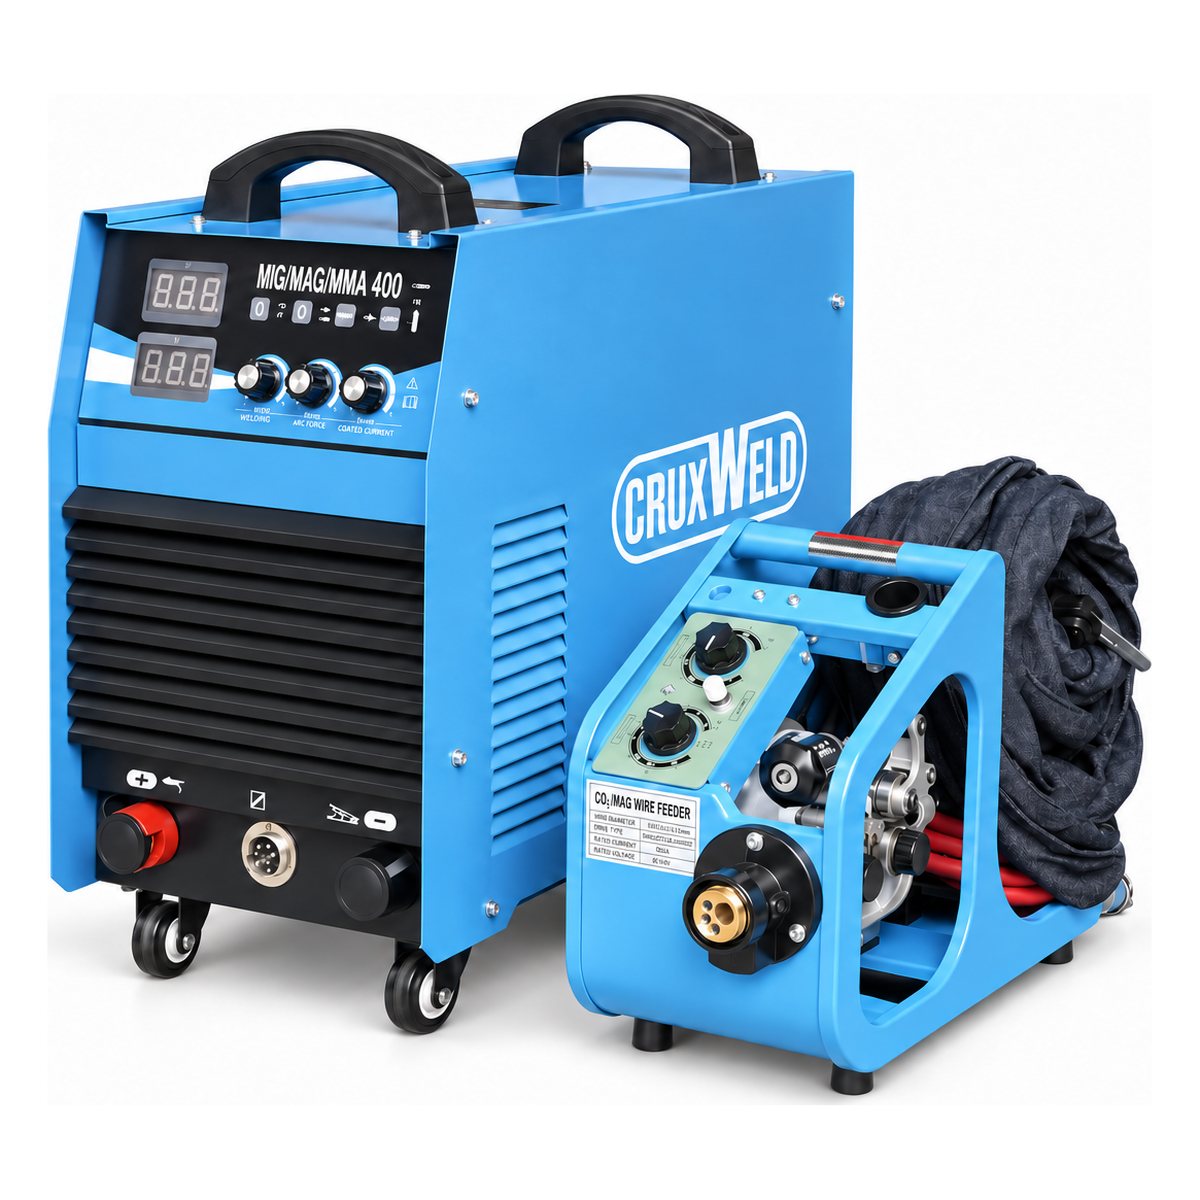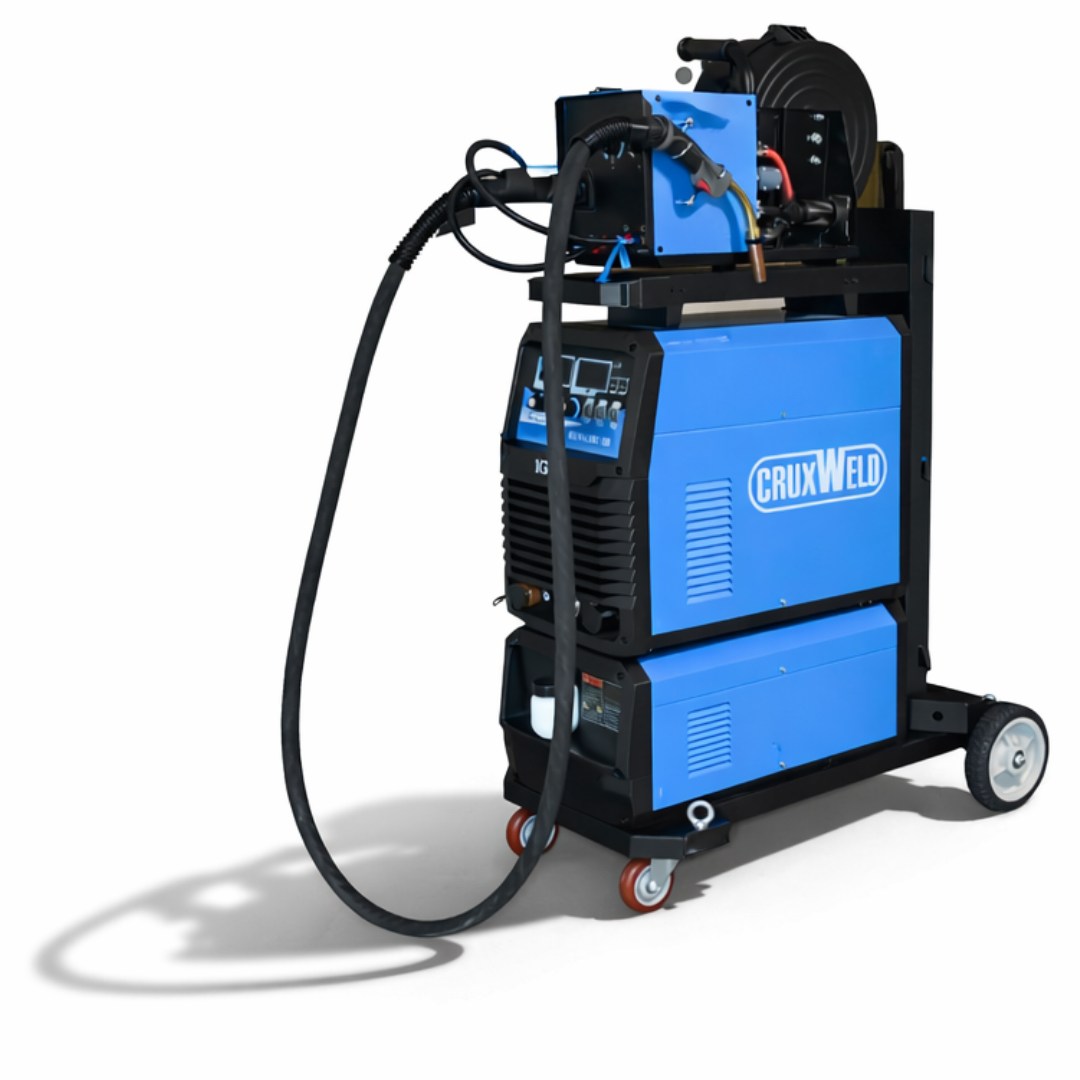
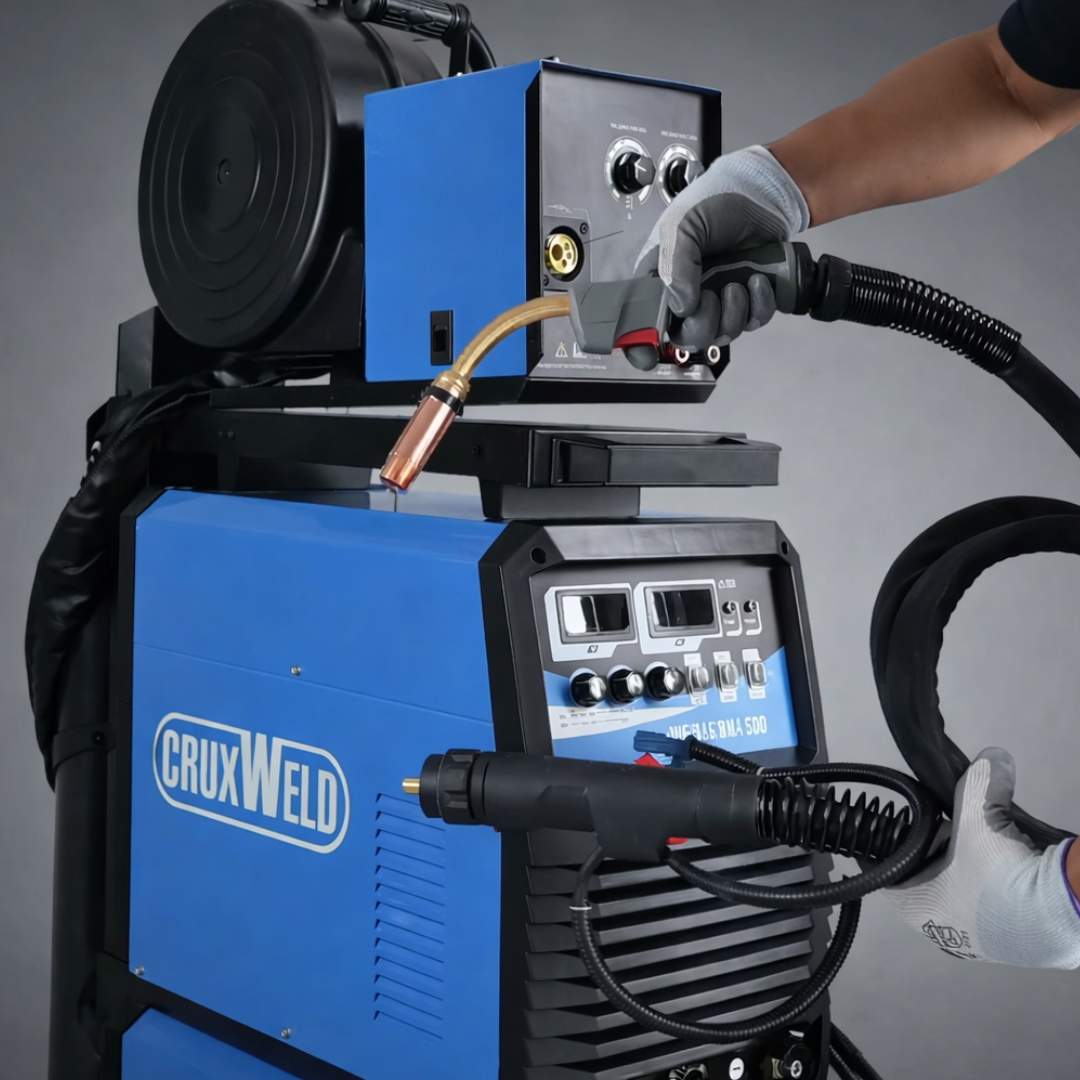
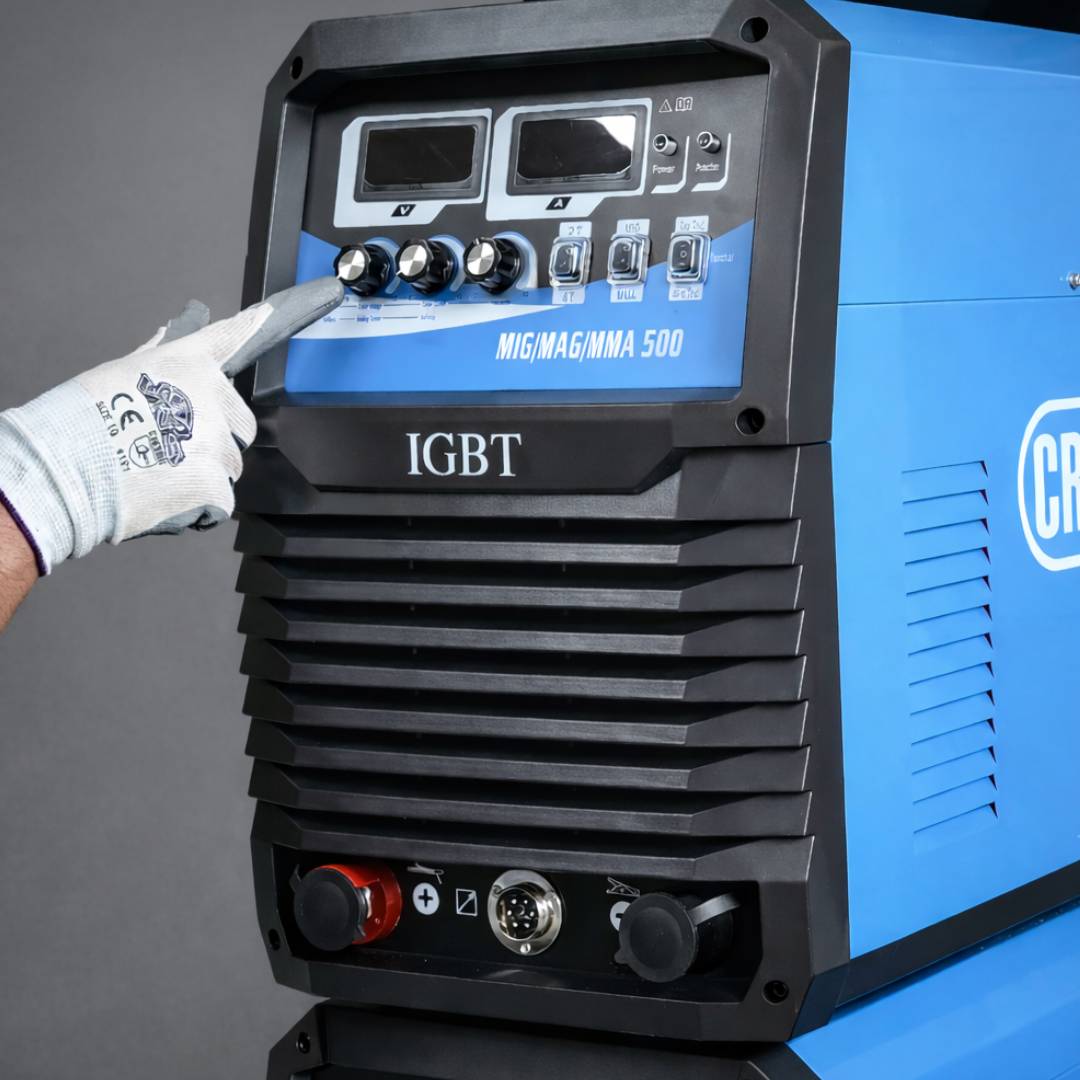
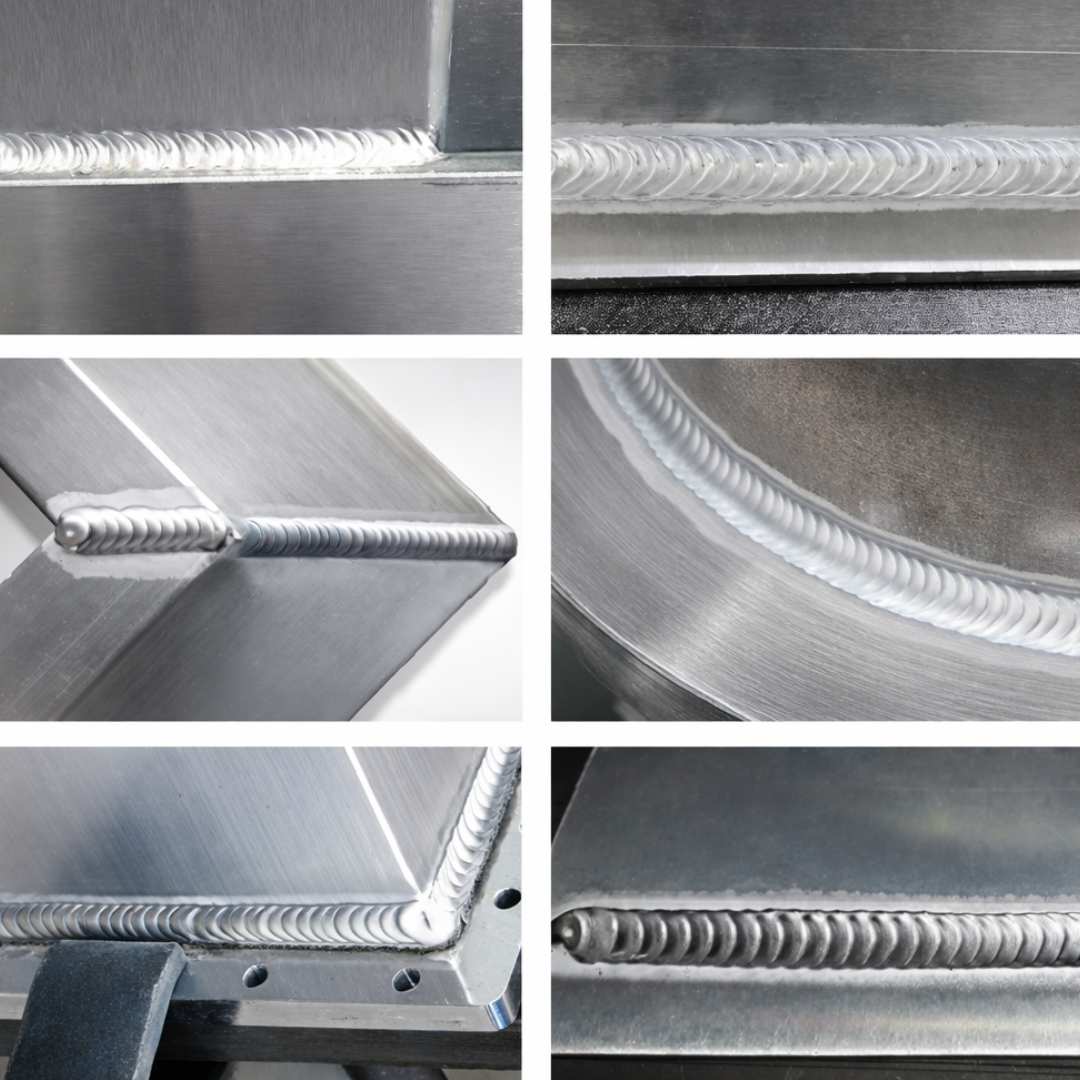
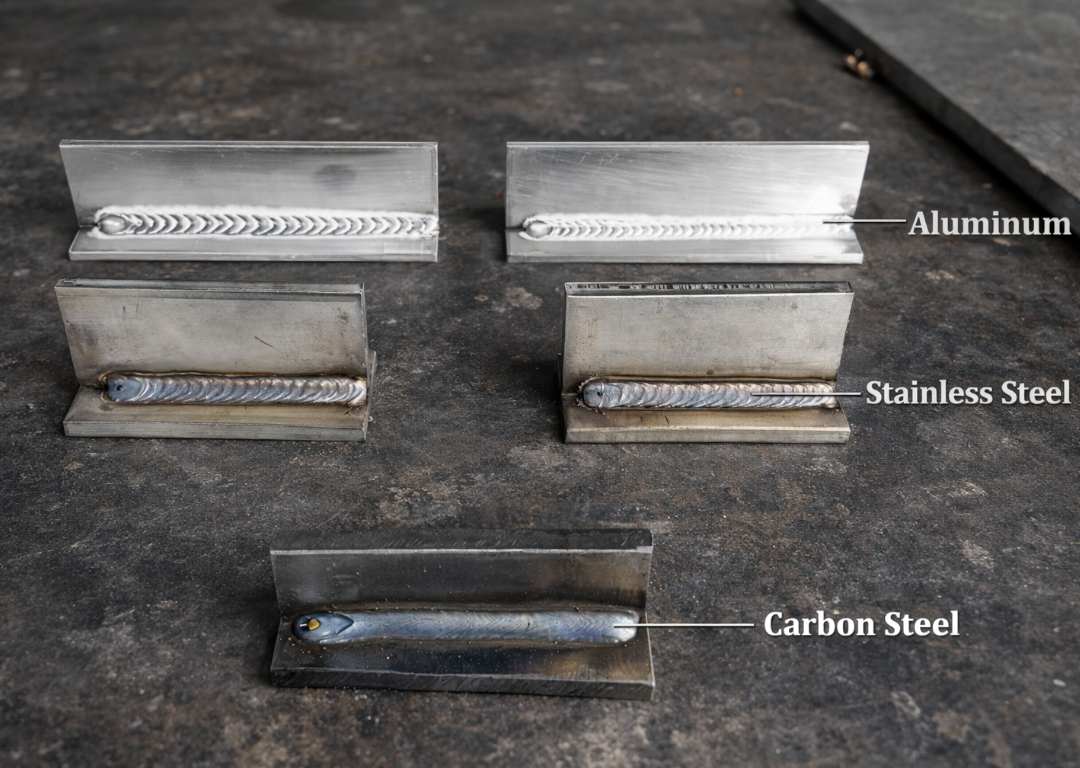
The CRUXWELD CWMIG500P is a MIG 500 water cooled welding system for heavy fabrication: an IGBT inverter power source, a built-in cooling unit for the water-cooled torch and a 4-roll wire feeder, all on one trolley. MIG/MAG, flux-cored and stick from the same machine.
GeM Registered OEM Manufacturer · Supported Worldwide · 45+ years of welding expertise
Price, delivery & technical help — get a fast response.
At 300, 400, 500 A an air-cooled torch runs hot, and the welder stops before the job does. The CWMIG500P sends coolant through a water-cooled torch, so you can keep the arc on heavy plate, multi-pass fillets and flux-cored runs for the whole shift.
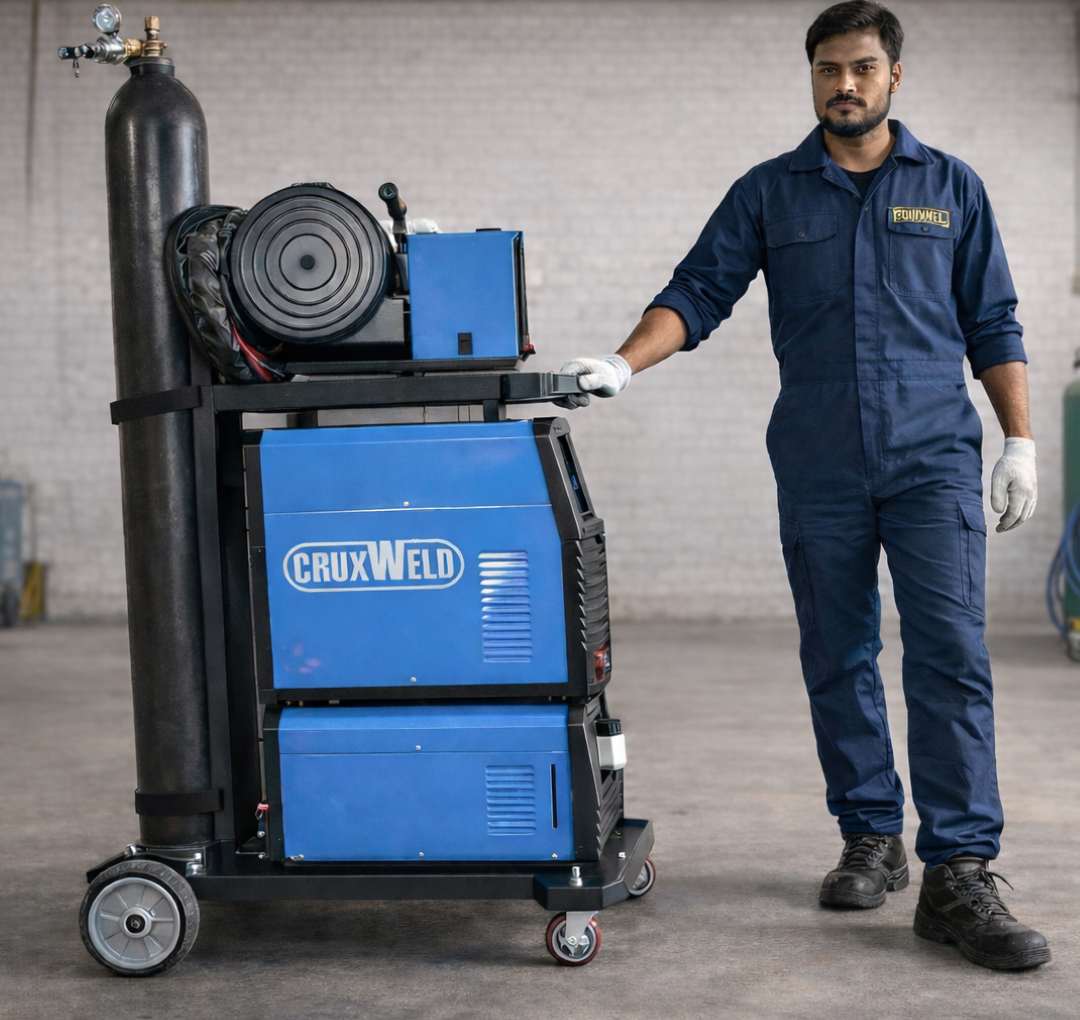
Everything stacks on one trolley: feeder on top, inverter power source in the middle, cooling unit below, gas cylinder on the back, so the whole station rolls to the job as one unit.
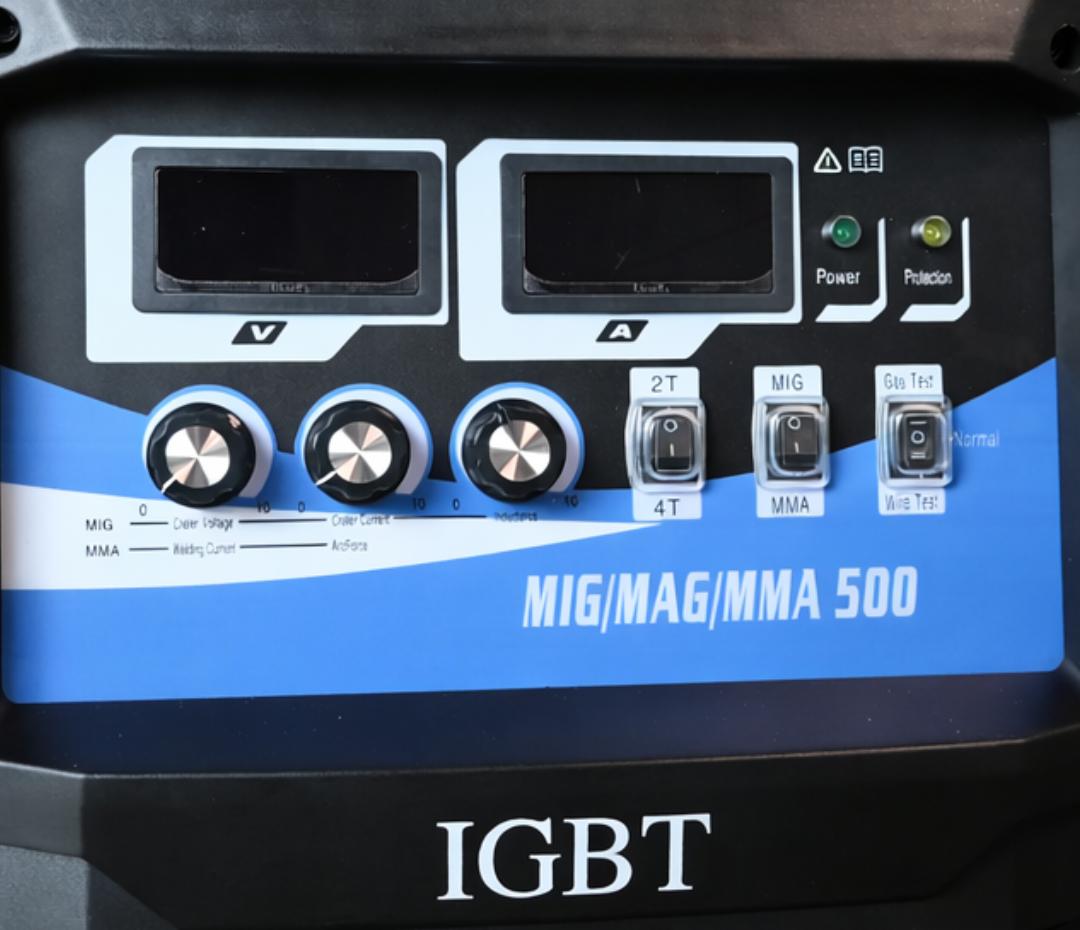
Gas check / wire check: purge the gas line and set flow, or inch the wire through the torch with no welding voltage, then return the switch to centre.
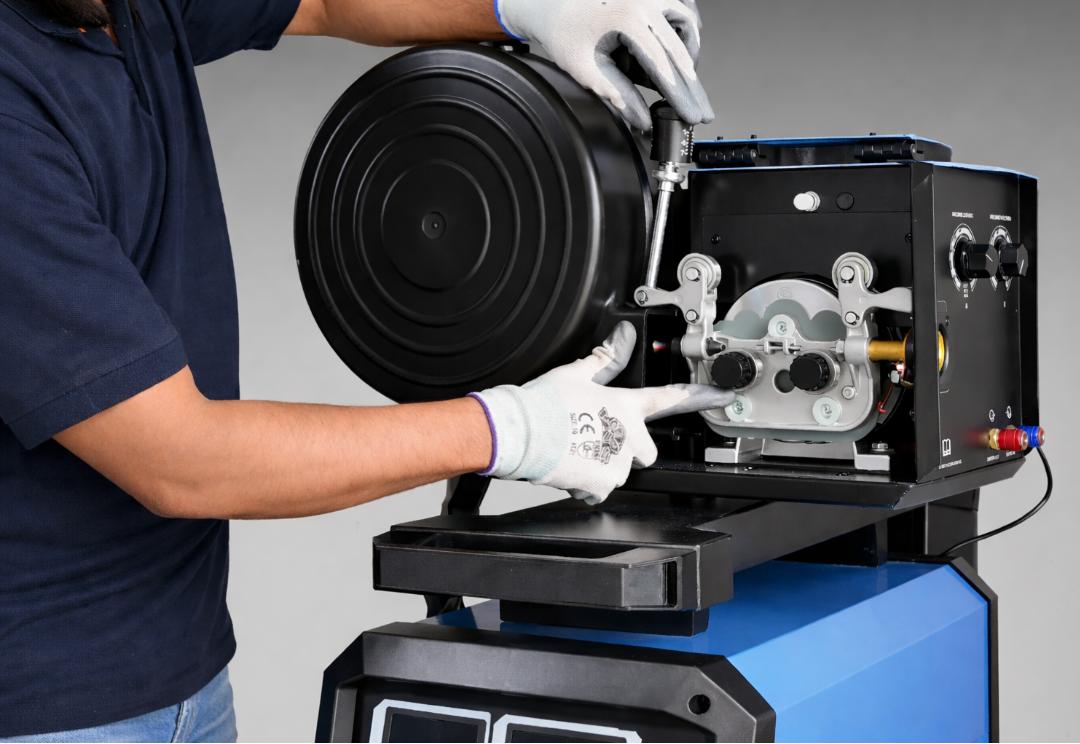
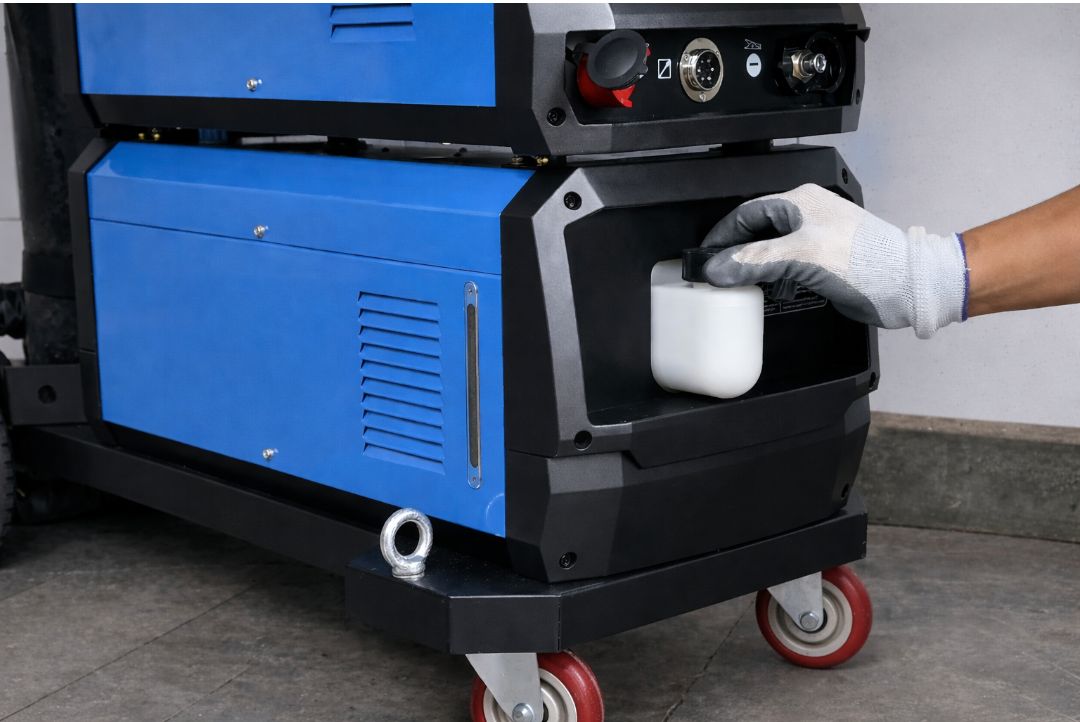
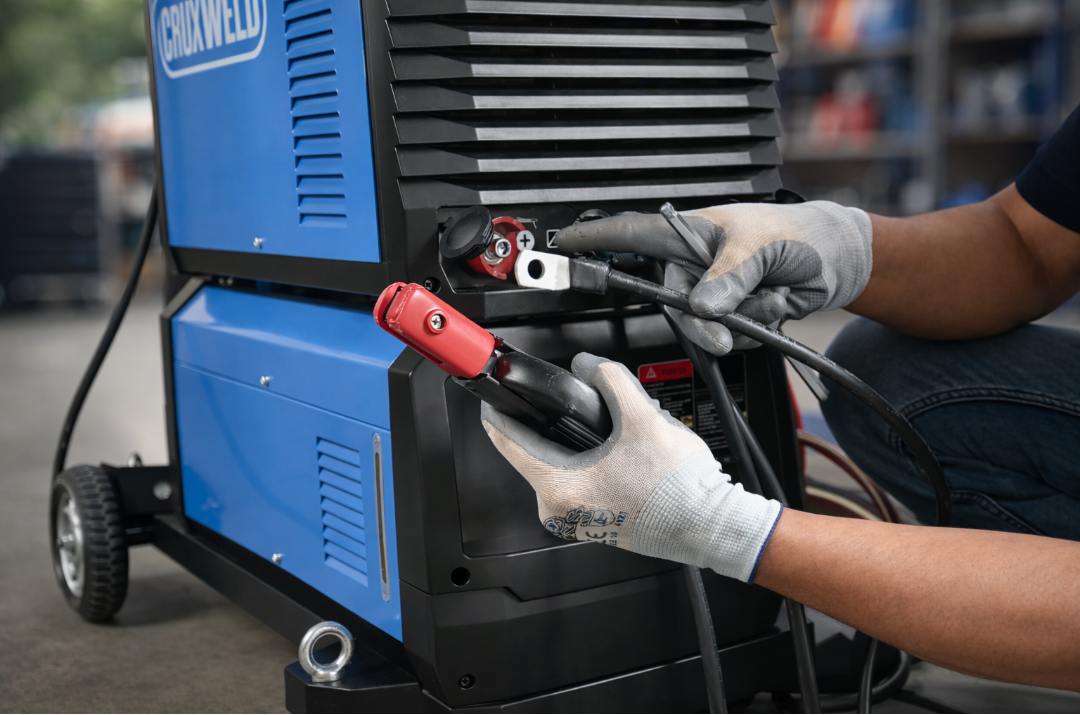
The built-in cooling unit circulates coolant through the torch and back, carrying away the heat that a 500 A arc puts into the neck and cable. Red and blue quick couplings on the feeder make the hose connections simple: blue to blue, red to red.
Tap to compare the torch on a long run.
Coolant runs down the torch and back to the cooling unit, carrying the heat of the arc away, so you can keep welding heavy plate and long seams.
At 300, 400, 500 A an air-cooled torch runs hot, and the welder stops before the job does.
Never weld with the tank empty or the hoses disconnected: a water-cooled torch can be damaged within seconds.
MIG, CO2 or mixed gas, mild steel. Tap a current band to see the matching voltage, wire and gas flow.
80–130 ACurrent
18–21 VVoltage
1.0 mmWire
15–20 L/minGas flow
130–200 ACurrent
20–24 VVoltage
1.0 mmWire
15–20 L/minGas flow
200–250 ACurrent
24–27 VVoltage
1.0 / 1.2 mmWire
15–20 L/minGas flow
250–350 ACurrent
26–32 VVoltage
1.2 / 1.6 mmWire
20–25 L/minGas flow
350–500 ACurrent
31–39 VVoltage
1.2 / 1.6 mmWire
20–25 L/minGas flow
| Current | Voltage | Wire |
|---|---|---|
| 80–130 A | 18–21 V | 1.0 mm |
| 130–200 A | 20–24 V | 1.0 mm |
| 200–250 A | 24–27 V | 1.0 / 1.2 mm |
| 250–350 A | 26–32 V | 1.2 / 1.6 mm |
| 350–500 A | 31–39 V | 1.2 / 1.6 mm |
These are starting points: confirm with a trial weld. For your plate and joint, send the details on WhatsApp and our technical team will suggest settings.


| Supply | 3-phase 400 V ±15%, 50/60 Hz; no missing phase |
| Input | 24.2 kVA, 37 A rated |
| Isolator / breaker | 63 A |
| Supply cable | At least 6 mm², 4-core copper |
| Earth | Machine must be earthed |
| Clearance | 50 cm front and rear, 20 cm at the sides |
| Working temperature | −10 to +40 °C |
| Wind at the arc | Not more than 1 m/s; screen outdoors |
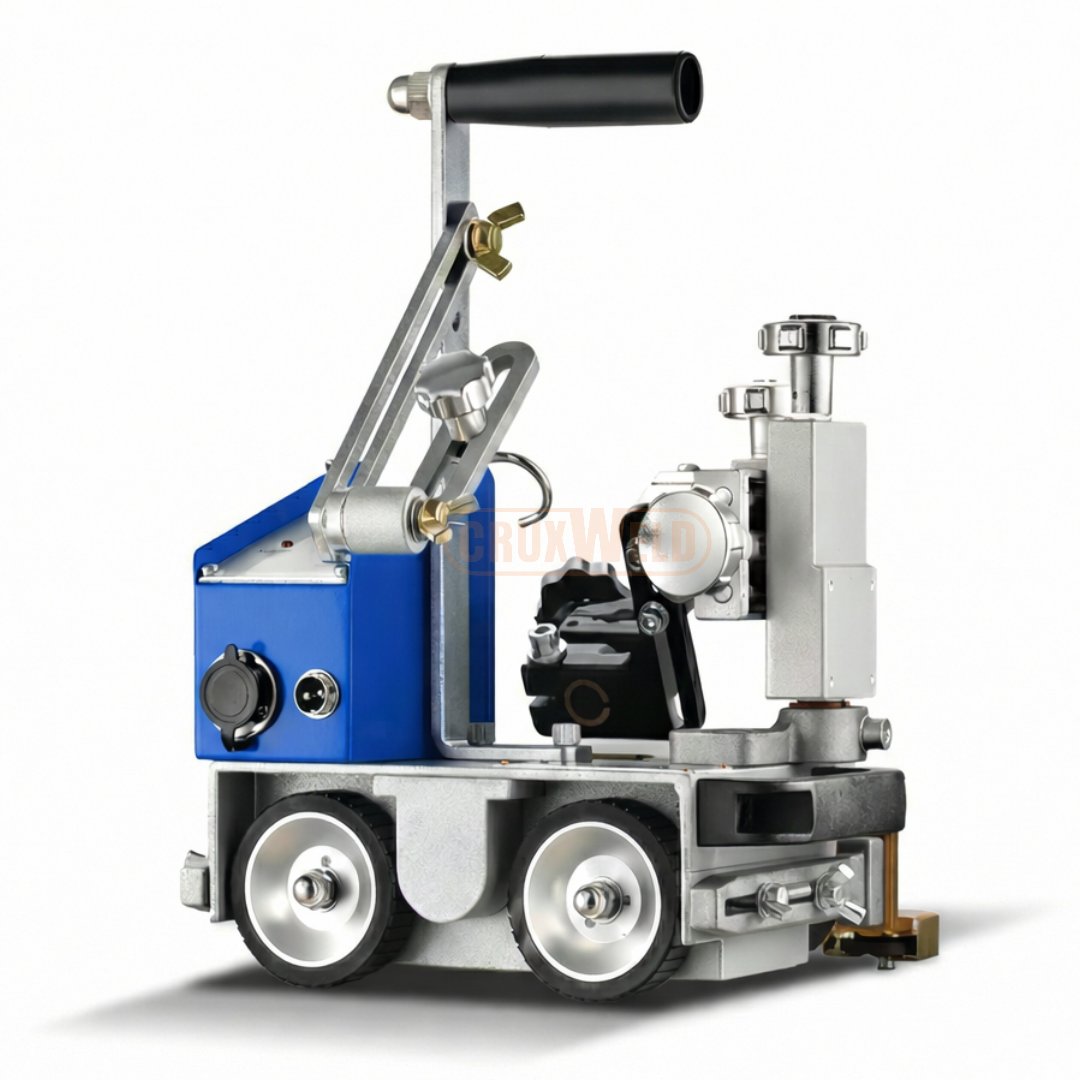
Automating long welds? Mount the torch on a WeldyFi fillet carriage or a DynaTwin 200M dual-torch carriage.
Tell us your material and plate thickness: we will suggest the setup and send a quotation.