Heat in Tiny Doses. Thin Stainless Stays Flat and Bright.
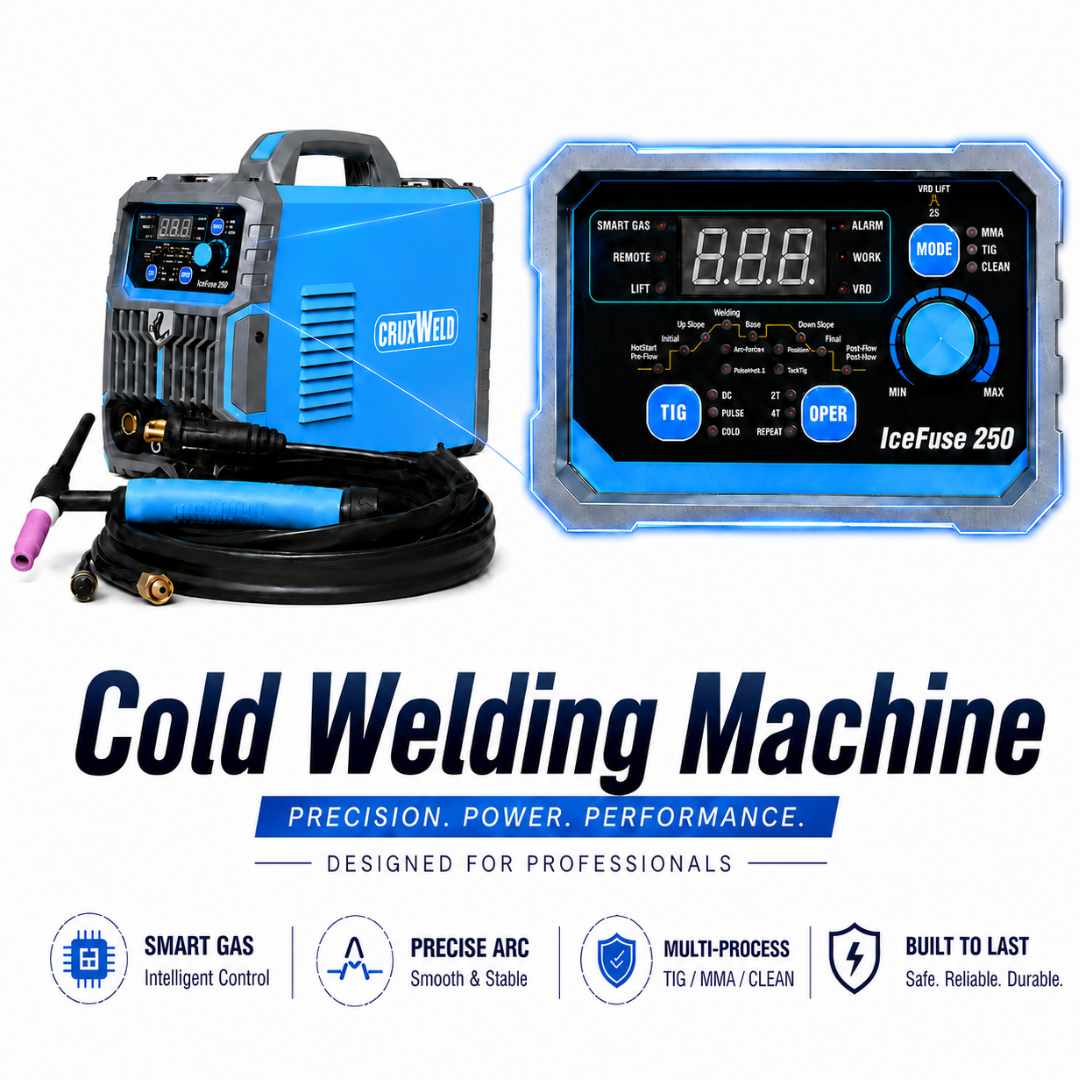
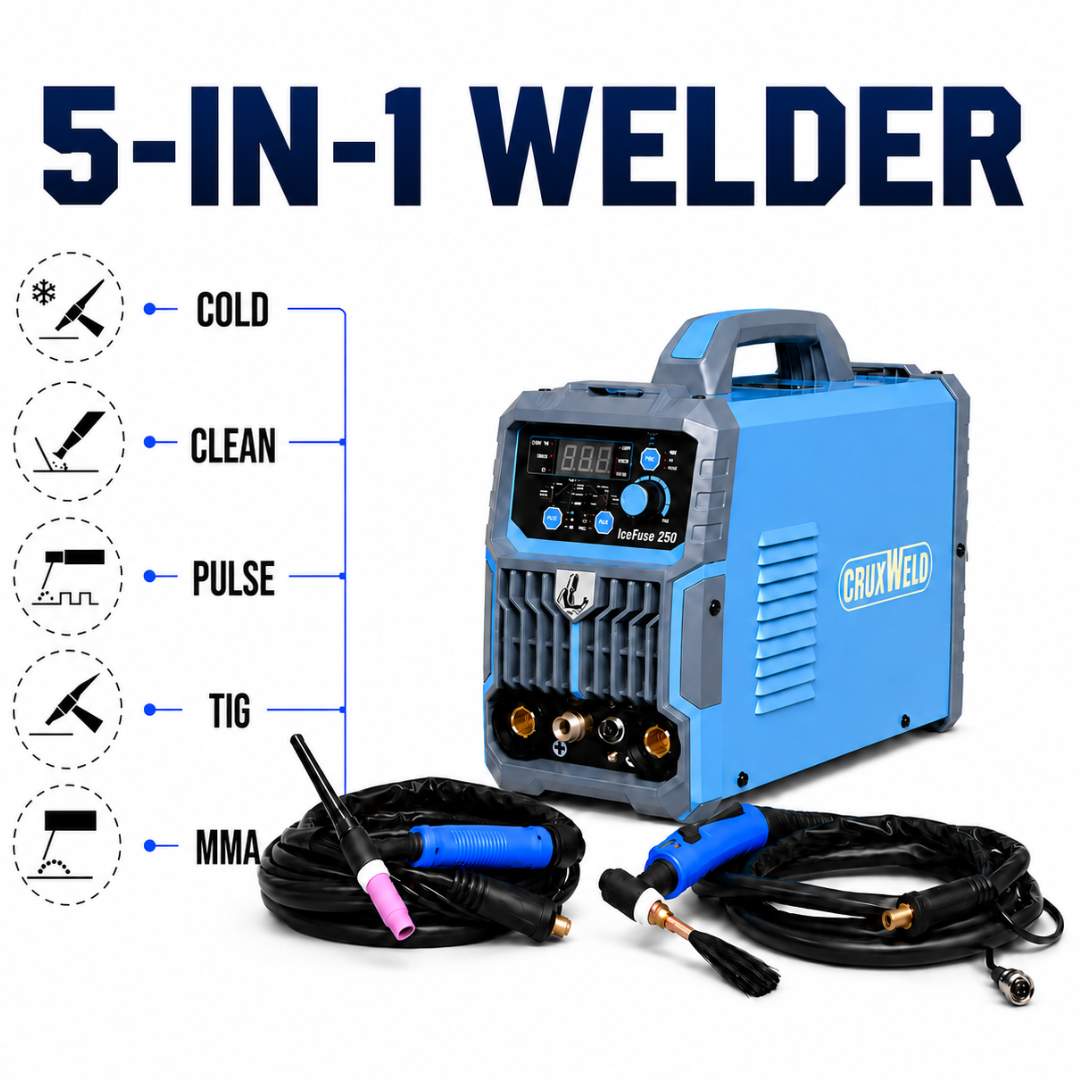
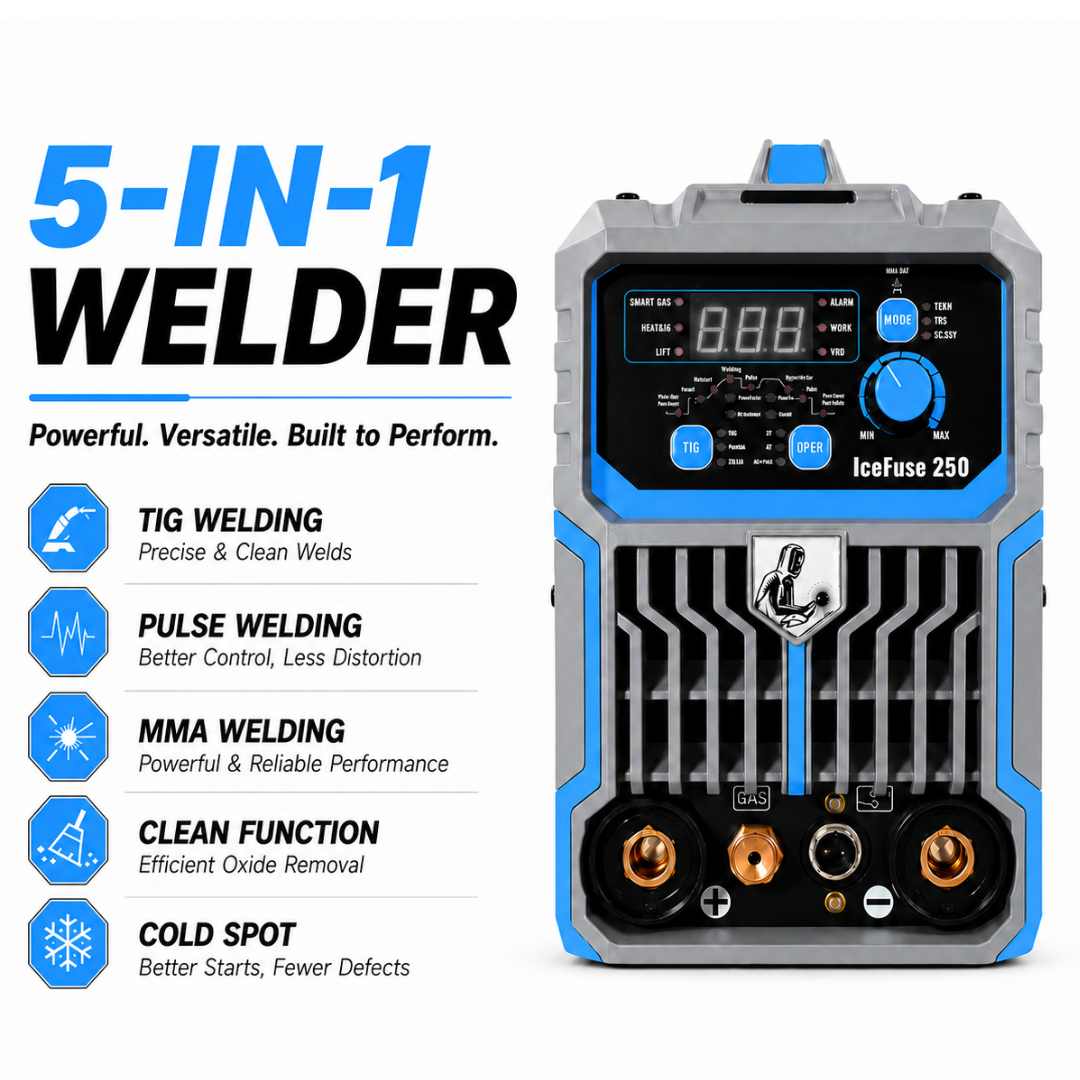
The CRUXWELD IceFuse 250 is a 5-in-1 cold welding machine: a DC inverter that welds in short, timed bursts of 1–999 ms so thin sheet barely warms, then switches to HF TIG, Pulse TIG, MMA, and a cleaning mode that brightens the bead afterwards.
5-in-1
processes
1–999 ms
cold weld time
220 / 110 V
single phase
10 + 10
memory sets
✓HF or LIFT arc start; 2T, 4T and repeat trigger
✓Smart Gas matches gas time and flow to the current
One Inverter for the Jobs That Punish Too Much Heat
Thin stainless, polished trim and finished parts do not forgive heat. A continuous arc warps the sheet, burns through the thinnest gauge and leaves a rainbow of heat tint that has to be ground and polished away.
The IceFuse 250 attacks that problem from two sides. Its cold mode welds in short, timed pulses with a pause between each one, so the heat never builds up. Its cleaning mode then lifts heat tint and oxide from the bead. Around those two sit a full HF TIG, Pulse TIG and MMA welder — five processes in one compact, dual-voltage machine.
Cold mode
Timed weld bursts with a set pause between them.
Clean mode
Brightens the bead after welding.
TIG + Pulse
HF or LIFT start, slopes, pulse up to 200 Hz.
MMA
1.6–4.0 mm electrodes with VRD.
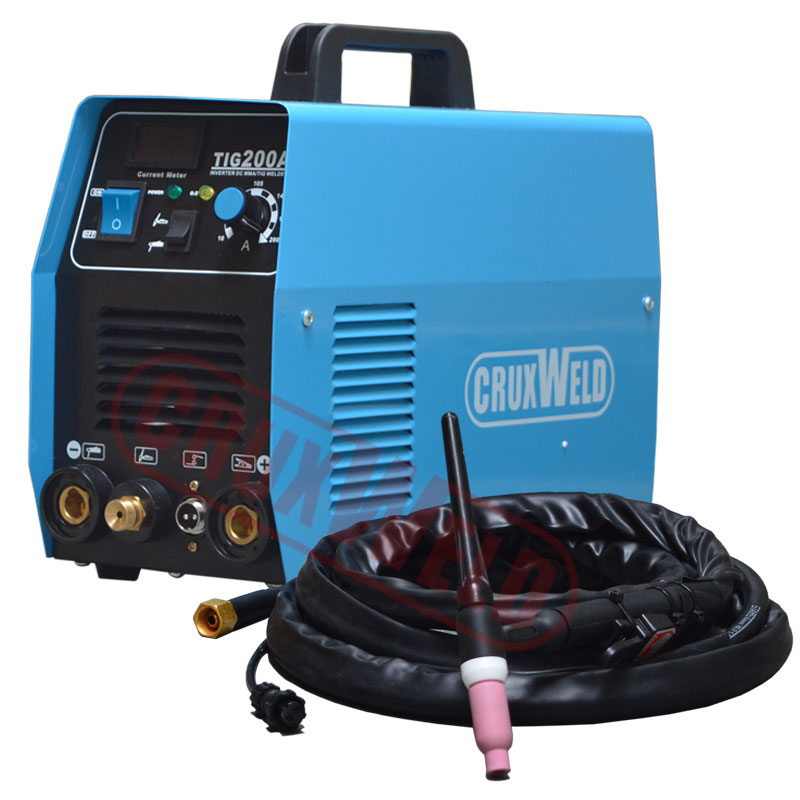
IceFuse 250 with TIG torch
02 · Why it stays cool
Heat in Tiny Doses Instead of a Steady Stream
A continuous arc keeps pouring energy into the joint, and on thin sheet that heat spreads, warps the panel and discolours the surface. In cold mode the IceFuse 250 fires a short weld burst of 1–999 ms, then pauses for up to 10 s before the next one. Each burst fuses a small spot; the pause lets the heat leave before the next.
What “cold welding” means here: low-heat fusion welding with a TIG arc — a true melted weld, delivered in small doses. It is not the solid-state pressure process of the same name.
Cold welding a mould-corner defect
03 · Five processes
Five Machines’ Worth of Welding in One Box
Cold
Short timed bursts for thin sheet, trim and defect repair.
1–999 ms weld0–10 s pauseup to 220 A
TIG (HF)
Non-contact HF start, or LIFT start where HF interference is a problem.
5–200 Aslopes 0–15 s2T / 4T / repeat
Pulse TIG
Peak and base current alternate for tight heat control and a rippled bead.
0.2–200 Hzduty 5–95%base 10–100%
Clean
A cleaning pen and low current lift heat tint and oxide from the bead.
10–40 A2–3 cm² contact
MMA
Stick welding for brackets, frames and repairs.
20–180 A1.6–4.0 mmhot start / arc force
04 · Shape the arc
Dial In the Heat, Pulse by Pulse
TIG timing, start to finish
Pre-flow
0.1–15 s
Up-slope
0–15 s
Weld
set current
Down-slope
0–15 s
Post-flow
0.5–15 s
Initial / final current 10–100%Spot time 0.1–15 s2T · 4T · repeatFoot pedal in 2T
05 · Smart panel
Set It Once, Recall It Every Time
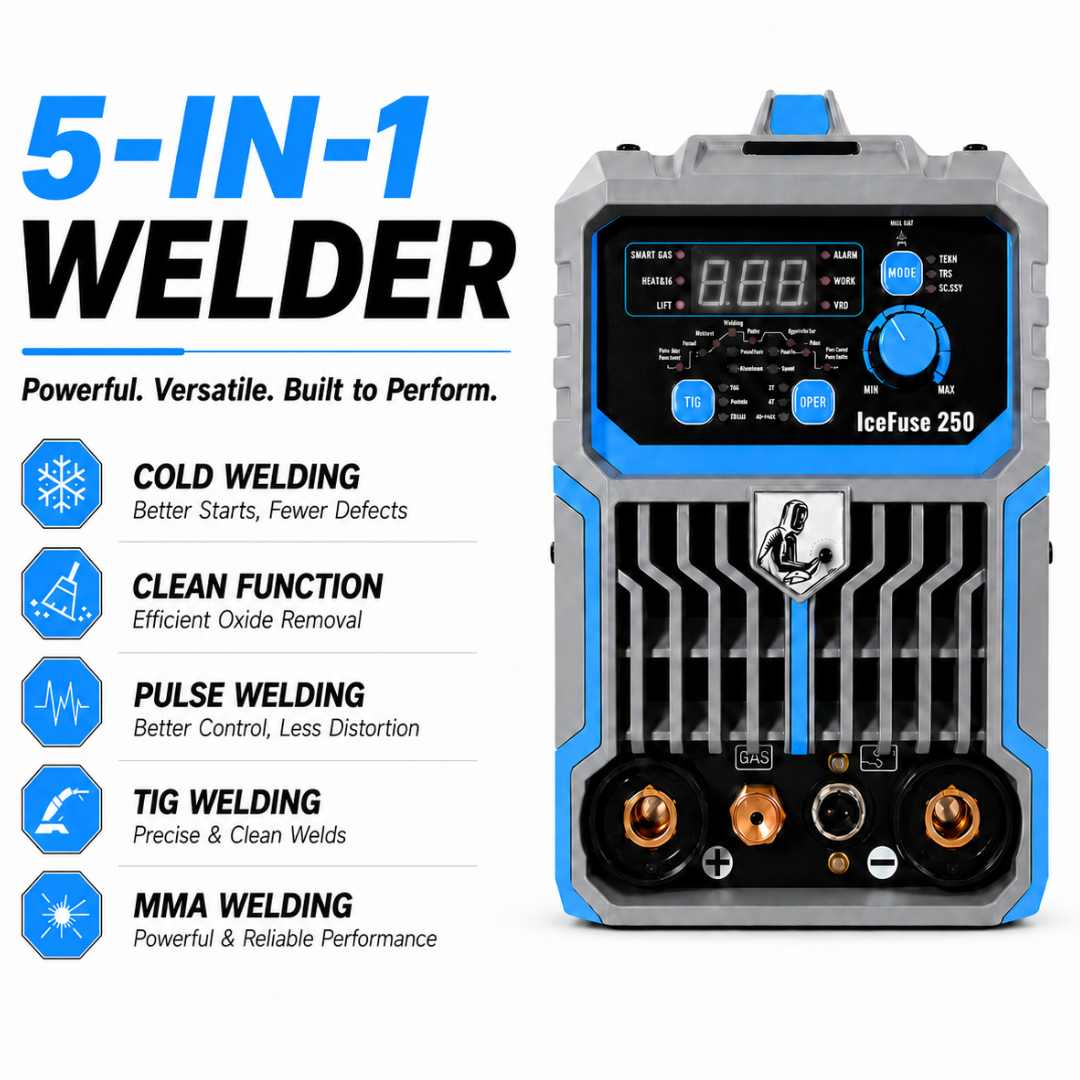
Front panel and outputs
Smart Gas
Matches gas pre- and post-flow to the set current, so argon is not wasted.
10 + 10 memory
Save ten parameter sets for TIG and ten for MMA.
VRD
Holds MMA open-circuit voltage below 15 V when idle.
LIFT start
Touch-and-lift TIG start with no HF interference.
Foot pedal
Set current from a pedal, within the panel maximum (2T).
Alarm display
Over-current, overheat and over-voltage show on the panel.
06 · Clean mode
From Heat Tint to Bright Metal on the Same Machine
1
Weld
Finish the joint in cold, TIG or pulse mode.
2
Switch to CLEAN
Select the cleaning mode and set 10–40 A.
3
Wipe the bead
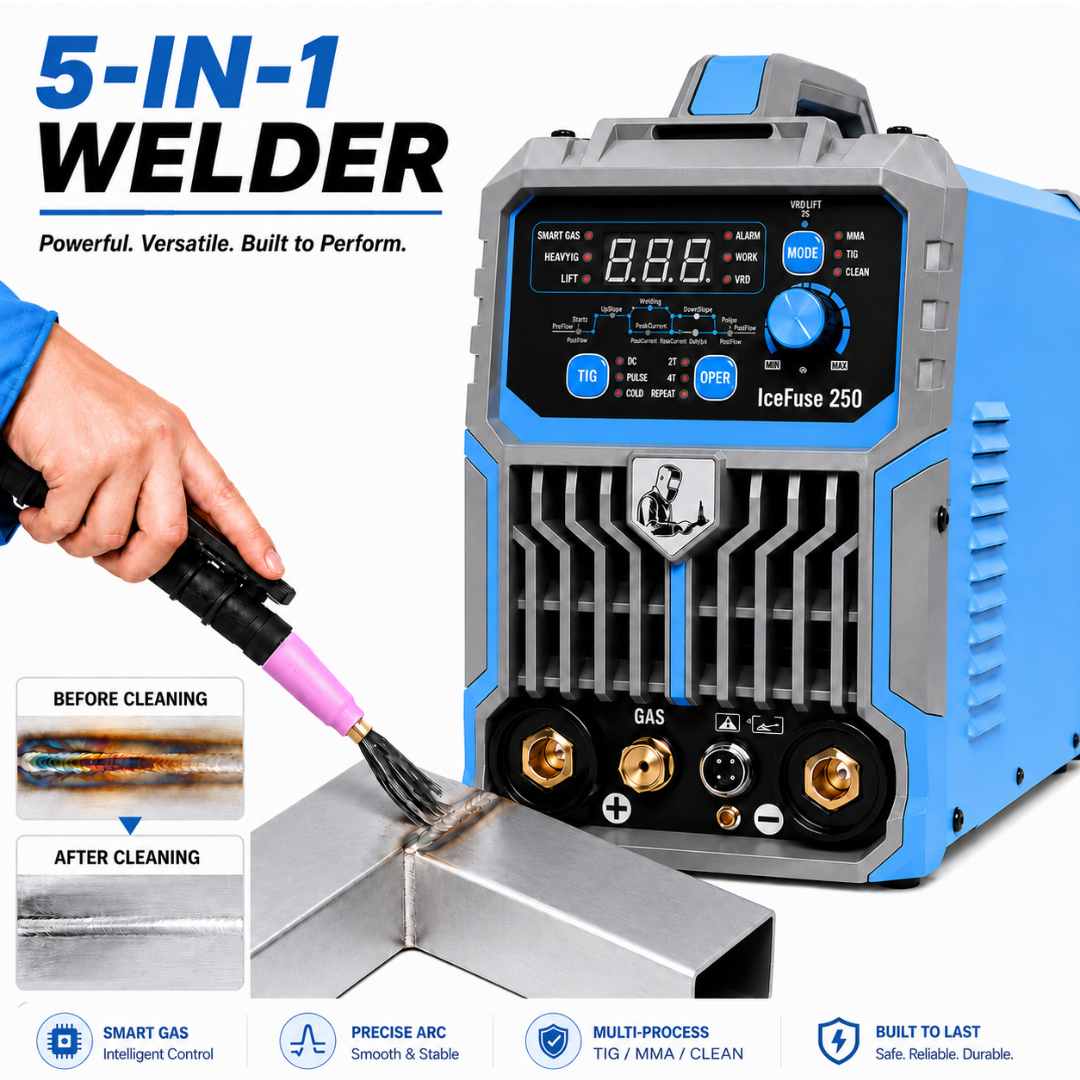
Work the cleaning pen along the weld — about 2–3 cm² at a time.
4
Inspect
Heat tint and oxide lift away for a bright finish.
Less grinding and polishing after welding, and no second machine on the bench for cleaning.
Before and after cleaning
07 · Power and protection
Plugs In Almost Anywhere, Looks After Itself
Dual voltage
1 × 220–240 V or 1 × 110–120 V, 50/60 Hz.
7.1 kVA, 38 A
Power capacity and maximum input current.
85% / 0.93
Efficiency and power factor.
Over-current
Output cuts and the alarm shows.
Overheat
Output cuts, then resets itself after cooling.
Over-voltage
Trips on an unstable supply; switch off for 2–3 minutes before restarting.
IP23, class F
For indoor workshop use — keep it out of the rain.
PriceThe quotation changes with the torch and accessories you choose and with quantity. There is no process option to pay extra for — Cold, TIG, Pulse TIG, Clean and MMA are all in the one machine.
PowerSingle phase 220–240 V (or 110–120 V), 50/60 Hz, 7.1 kVA, maximum input current 38 A. Plan a socket and cabling rated for that 38 A input; no three-phase supply is needed.
LimitsTIG 5–200 A, Cold 5–220 A, MMA 20–180 A. For 415 V three-phase production welding above 200 A, look at the TIG welding machines range.
DeliveryDelivery time depends on stock and is confirmed with the quotation. Every machine is tested before dispatch.
Warranty and sparesWarranty terms are stated in the quotation. Torch consumables and spares are available from Cruxweld, with set-up help on WhatsApp and video call.
Specifications are subject to improvement without notice; the quotation supplied with the machine is the governing document. Warranty terms are stated on the quotation / invoice.
A welder that joins metal with very low heat input. In cold mode the CRUXWELD IceFuse 250 fires short weld bursts of 1–999 ms with a pause of up to 10 s between them, so thin sheet does not build up heat, warp or discolour.
Is it a real weld or solid-state cold welding?
It is a true fusion weld made with a TIG arc — just delivered in small, timed doses. It is not the solid-state pressure process that shares the name.
What are the five processes?
Cold welding, HF TIG (with a LIFT start option), Pulse TIG, Clean (weld-bead cleaning) and MMA stick welding.
What power supply does it need?
Single phase: 1 × 220–240 V or 1 × 110–120 V, 50/60 Hz, with a power capacity of 7.1 kVA and a maximum input current of 38 A.
Can it weld aluminium?
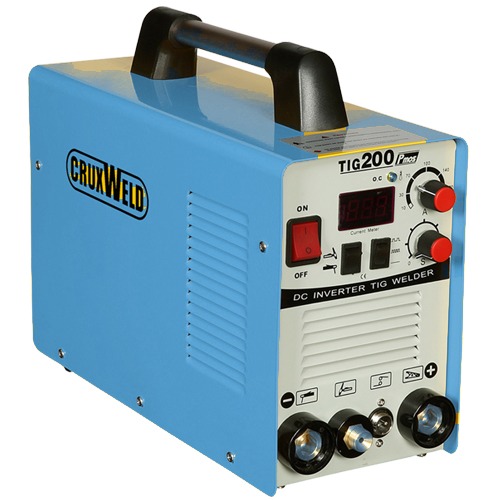
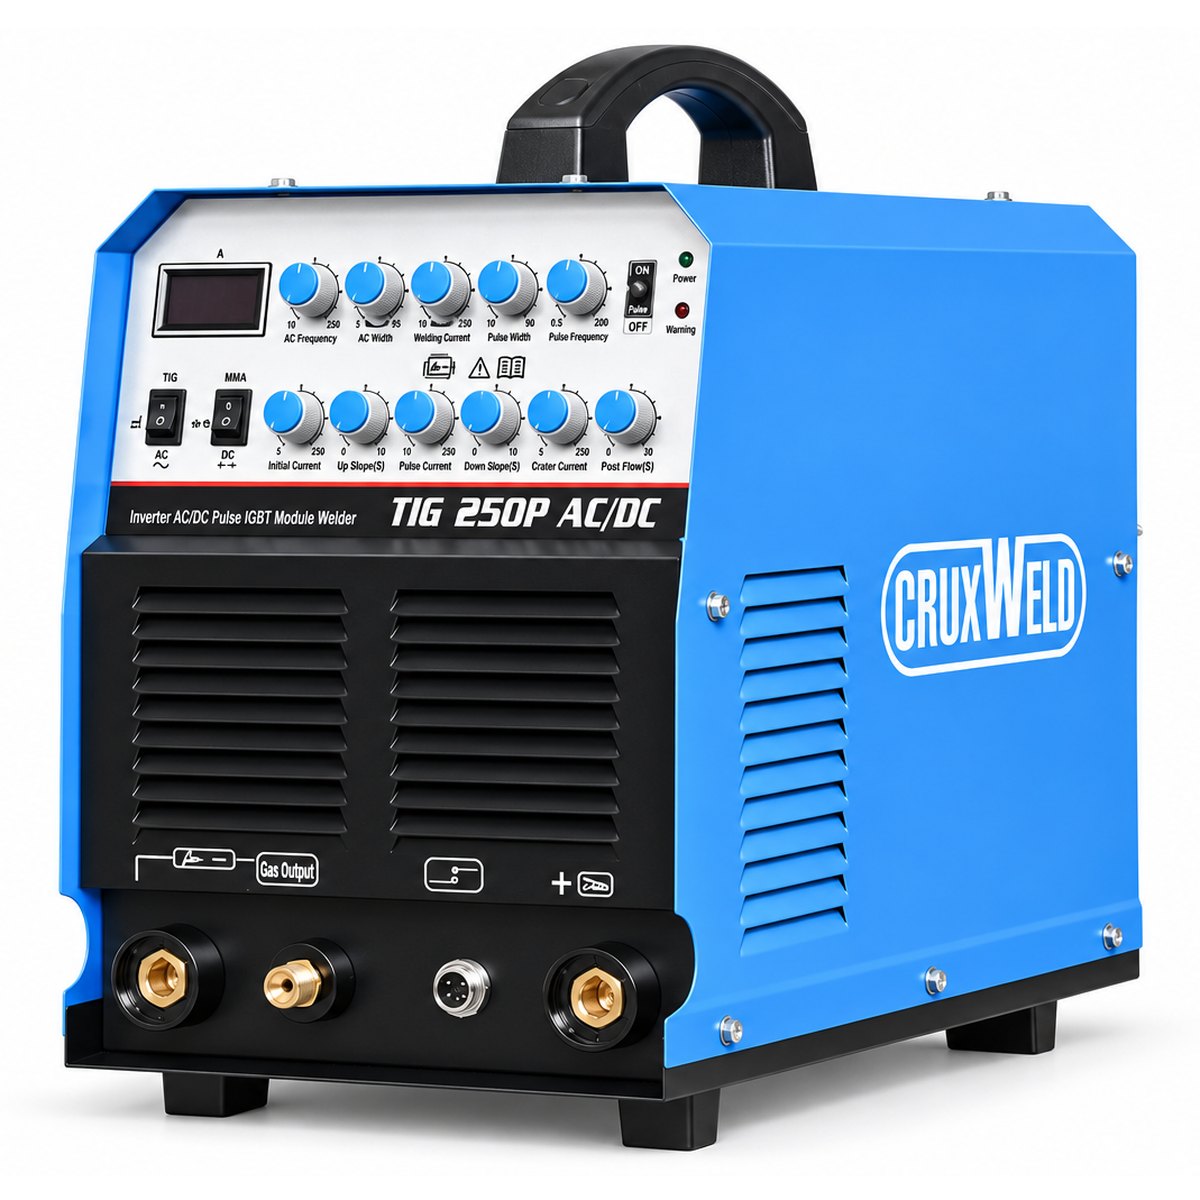
No. It is a DC machine for stainless, carbon and mild steel. For aluminium you need AC TIG, such as the CRUXWELD TIG 200 AC/DC.
What does the Clean mode do?
It uses a cleaning pen at 10–40 A to lift heat tint and oxide from the weld bead, giving a bright finish without a second machine.
Does it save gas?
Yes. Smart Gas matches gas pre- and post-flow to the set current, so you do not waste argon on long post-flow at low current.
How do I get the IceFuse 250 price and delivery time?
Request a quote on this page or message +91 88008 82983 on WhatsApp with the material and thickness you weld. You will receive a GST quotation with delivery time, usually the same working day.
Tell us the metal and thickness — we will suggest settings and quote today.